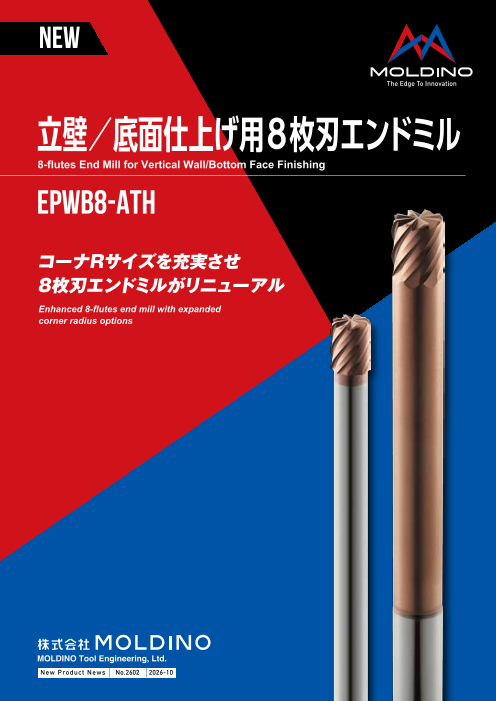


コーナRサイズを充実させ 8枚刃エンドミルがリニューアル
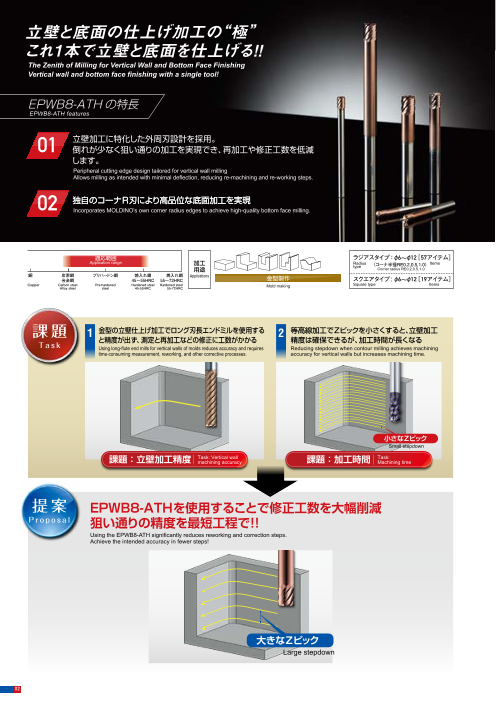
立壁と底面の仕上げ加工の“極”
これ1本で立壁と底面を仕上げる!!
◼︎01 立壁加工に特化した外周刃設計を採用。
倒れが少なく狙い通りの加工を実現でき、再加工や修正工数を低減
します。
◼︎02 独自のコーナR刃により高品位な底面加工を実現
◆詳細はカタログをダウンロードのうえご覧いただくか、お気軽にお問い合わせください。
このカタログについて
| ドキュメント名 | 立壁/底面仕上げ用8枚刃エンドミル EPWB8-ATH |
|---|---|
| ドキュメント種別 | 製品カタログ |
| ファイルサイズ | 1.9Mb |
| 登録カテゴリ | |
| 取り扱い企業 | 株式会社MOLDINO (この企業の取り扱いカタログ一覧) |
この企業の関連カタログ

このカタログの内容
Page1
NEW
立壁/底面仕上げ用8枚刃エンドミル
8-flutes End Mill for Vertical Wall/Bottom Face Finishing
EPWB8-ATH
コーナRサイズを充実させ
図、表等のデータは試験結果の一例であり、保証値ではありません。 8枚刃エンドミルがリニューアル
「 」は株式会社MOLDINOの登録商標です。
The diagrams and table data are examples of test results, and are not guaranteed values. Enhanced 8-flutes end mill with expanded
“ ” is a registered trademark of MOLDINO Tool Engineering, Ltd. corner radius options
安 全 上 の ご 注 意 Attentions on Safety
1. 取扱上のご注意 1. Cautions regarding handling
(1)工具をケース(梱包)から取り出す際は、工具の飛び出し、落下にご注意ください。特に工具刃部との接 (1) When removing the tool from its case (packaging), be careful that the tool does not pop out or is
触には十分ご注意をお願いします。 dropped. Be particularly careful regarding contact with the tool flutes.
(2)鋭利な切れ刃を有する工具を取扱う際は、切れ刃を素手で直接触れないように注意してください。 (2) When handling tools with sharp cutting flutes, be careful not to touch the cutting flutes directly with
2. 取付け時のご注意 your bare hands.
(1)ご使用前に、工具の傷・割れ等の外観確認を行っていただき、コレットチャック等への取付けは確実に 2. Cautions regarding mounting
行ってください。 (1) Before use, check the outside appearance of the tool for scratches, cracks, etc. and that it is firmly
(2)ご使用中に、異常な振動等が発生した場合は、直ちに機械を停止させて、その振動の原因を取り除い mounted in the collet chuck, etc.
てください。 (2) If abnormal chattering, etc. occurs during use, stop the machine immediately and remove the cause
3. 使用上のご注意 of the chattering.
(1)切削工具あるいは被削材の寸法・回転の方向は、あらかじめ確認しておいてください。 3. Cautions during use
(2)標準切削条件表の数値は、新しい作業の立上げの目安としてご利用ください。切込みが大きい場合、 (1) Before use, confirm the dimensions and direction of rotation of the tool and milling work material.
使用機械の剛性が小さい場合あるいは被加工物の性状に応じて切削条件を適正に調整してご使用 (2) The numerical values in the standard cutting conditions table should be used as criteria when starting
ください。 new work. The cutting conditions should be adjusted as appropriate when the cutting depth is large,
(3)切削工具材料は硬質の材料です。ご使用中に破損して飛散する場合があります。また、切りくずが飛 the rigidity of the machine being used is low, or according to the conditions of the work material.
散することがあります。これらの飛散物等は作業者を切傷させ、火傷あるいは目に入って負傷させる恐 (3) Cutting tools are made of a hard material. During use, they may break and fly off. In addition, cutting
れがありますので、工具をご使用中はその周囲に安全カバーを取付け、保護めがね等の保護具を着用 chips may also fly off. Since there is a danger of injury to workers, fire, or eye damage from such
して安全な環境下での作業をお願いいたします。 flying pieces, a safety cover should be attached when work is performed and safety equipment such
(4)切削中に発生する火花や、破損による発熱や、切りくずによる引火・火災の危険があります。引火や as safety goggles should be worn to create a safe environment for work.
爆発の危険のあるところでは使用しないでください。不水溶性切削液をご使用される場合は防火対 (4) There is a risk of fire or inflammation due to sparks, heat due to breakage, and cutting chips. Do not
策を必ず行なってください。 use where there is a risk of fire or explosion. Please caution of fire while using oil base coolant, fire
(5)工具を本来の目的以外にはご使用にならないでください。 prevention is necessary.
4. 再研削時のご注意 (5) Do not use the tool for any purpose other than that for which it is intended.
(1)再研削時期が不適当であると工具が破損する恐れがあります。適正な工具と交換するか、再研削を 4. Cautions regarding regrinding
行ってください。
(2)工具を再研削しますと粉塵が発生します。再研削時にはその周囲に安全カバーを取付け、保護め (1) If regrinding is not performed at the proper time, there is a risk of the tool breaking. Replace the tool
がね等の保護具を着用してください。 with one in good condition, or perform regrinding.
(3)本製品には特定化学物質に指定された コバルト及びその無機化合物が含まれています。再研削等の (2) Grinding dust will be created when regrinding a tool. When regrinding, be sure to attach a safety
加工を加える場合は特定化学物質障害予防規則(特化則)に従った取扱いをしてください。 cover over the work area and wear safety clothes such as safety goggles, etc.
(3) This product contains the specified chemical substance cobalt and its inorganic compounds. When
5. 工具に関して、安全上の問題点・不明の点・その他相談がありましたら フ リ ーダ イ ヤ ル 技 術 相 談 へ performing regrinding or similar processing, be sure to handle the processing in accordance with
ご相談ください。 thelocal laws and regulations regarding prevention of hazards due to specified chemical substances.
ホームページ フリーダイヤル技術相談
https://www.moldino.com
MOLDINO Tool Engineering, Ltd.
本社 〒130-0026 東京都墨田区両国4-31-11(ヒューリック両国ビル8階) 工具選定データベース【 TOOLSEARCH】
03-6890-5101 FAX 03-6890-5134
International Sales Dept .: +81-3-6890-5103 FAX +81-3-6890-5128
営業企画部 ☎03-6890-5102 FAX03-6890-5134 海外営業部 ☎03-6890-5103 FAX03-6890-5128
東京営業所 ☎03-6890-5110 FAX03-6890-5133 静岡営業所 ☎054-273-0360 FAX054-273-0361
東北営業所 ☎022-208-5100 FAX022-208-5102 名古屋営業所 ☎052-687-9150 FAX052-687-9144
新潟営業所 ☎0258-87-1224 FAX0258-87-1158 大阪営業所 ☎06-7668-0190 FAX06-7668-0194
東関東営業所 ☎0294-88-9430 FAX0294-88-9432 中四営業所 ☎082-536-2001 FAX082-536-2003
長野営業所 ☎0276-59-6001 FAX0276-59-6005 九州営業所 ☎092-289-7010 FAX092-289-7012
北関東営業所 ☎0276-59-6001 FAX0276-59-6005
神奈川営業所 ☎046-400-9429 FAX046-400-9435
ヨーロッパ/MOLDINO Tool Engineering Europe GmbH Itterpark 12, 40724 Hilden, Germany. TEL : +49-(0)2103-24820, FAX : +49-(0)2103-248230
アメリカ/MITSUBISHI MATERIALS U.S.A. CORPORATION Detroit office c/o RFM Inc. Customer service 2001 Orndorf Drive, Brighton, MI 48116 U.S.A. TEL : +1(248)308-2620, FAX :+1(248)308-2627
メキシコ/MITSUBISHI MATERIALS MÉXICO S.A. DE C.V. Av. La Cañada No.16, Parque Industrial Bernardo Quintana, El Marques, Querétaro, CP 76246, México TEL : +52-442-1926800 MOLDINO Tool Engineering, Ltd.
ブラジル/MITSUBISHI MATERIALS BRASIL LTDA. Rua Cincinato Braga, 340 13° andar.Bela Vista – CEP 01333-010 São Paulo – SP ., Brasil TEL : +55(11)3506-5600 FAX : +55(11)3506-5677
タ イ/MITSUBISHI MATERIALS (THAILAND) CO., LTD. 139/3 Moo 2, Tambon Khlong Chik, Amphoe Bang Pa-in, Phra Nakhon Si Ayutthaya 13160, Thailand TEL:+66-3525-8024
イ ン ド/Mitsubishi Materials India Private Limited H.O.: Prasad Enclave, #118/119, 1st Floor, 2nd Stage, 5th main, BBMP Ward #11, (New #38), Industrial Suburb, Yeshwanthpura, Bengaluru, 560 022, Karnataka, India. Tel : +91-80-2204-3600 New Produc t News No.2602 2026-10
予告なく、改良・改善のために仕様変更することがあります。
Specifications for the products listed in this catalog are subject to change without notice due to ベジタブルインクで印刷しています。 2026-10(K)HT4
replacement or modification. Printed using vegetable oil ink. Printed in JAPAN 2026-10:FP
Page2
立壁と底面の仕上げ加工の“極”
これ1本で立壁と底面を仕上げる!
The Zenith of Milling for Vertical Wall and Bottom Face Finishing
Vertical wall and bottom face finishing with a single tool!
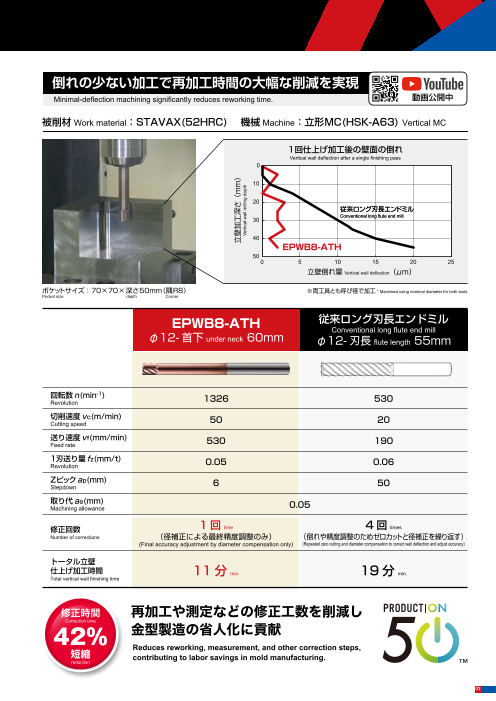
倒れの少ない加工で再加工時間の大幅な削減を実現
EPWB8-ATHの特長 Minimal-deflection machining significantly reduces reworking time. 動画公開中
EPWB8-ATH features
被削材 Work material:STAVAX(52HRC) 機械 Machine:立形MC(HSK-A63) Vertical MC
01 立壁加工に特化した外周刃設計を採用。
倒れが少なく狙い通りの加工を実現でき、再加工や修正工数を低減 1回仕上げ加工後の壁面の倒れ
します。 Vertical wall deflection after a single finishing pass
0
Peripheral cutting edge design tailored for vertical wall milling
Allows milling as intended with minimal deflection, reducing re-machining and re-working steps.
10
02 独自のコーナR刃により高品位な底面加工を実現 20
Incorporates MOLDINO's own corner radius edges to achieve high-quality bottom face milling. 従来ロング刃長エンドミル
Conventional long flute end mill
30
40
EPWB8-ATH
適応範囲 ラジアスタイプ:φ6~φ12[ 57ア イテム] 50
Application range 加工 Radius 0 5 10 15 20 25
用途 type (コーナ半径RE0.2, 0.5, 1.0) Items
Corner radius RE0.2, 0.5, 1.0
銅 炭素鋼 プリハードン鋼 焼入れ鋼 焼入れ鋼 立壁倒れ量 Vertical wall deflection(μm)
Applications
合金鋼 45~55HRC 55~72HRC 金型製作 スクエアタイプ : φ6~φ12[ 19ア イテム]
Copper Carbon steel Pre-hardened Hardened steel Hardened steel
Alloy steel steel 45̃55HRC 55̃72HRC
Mold making Square type Items
ポケットサイズ:70×70×深さ50mm(隅R8) ※両工具とも呼び径で加工 * Machined using nominal diameter for both tools
Pocket size depth Corner
EPWB8-ATH 従来ロング刃長エンドミル
課題 1 金型の立壁仕上げ加工でロング刃長エンドミルを使用する 2 等高線加工でZピックを小さくすると、立壁加工 Conventional long flute end mill
と精度が出ず、測定と再加工などの修正に工数がかかる 精度は確保できるが、加工時間が長くなる φ12- 首下 under neck 60mm
T a s k φ12- 刃長 flute length 55mm
Using long-flute end mills for vertical walls of molds reduces accuracy and requires Reducing stepdown when contour milling achieves machining
time-consuming measurement, reworking, and other corrective processes. accuracy for vertical walls but increases machining time.
回転数 n(min-1)
Revolution 1326 530
切削速度 vc(m/min)
Cutting speed 50 20
小さなZピック 送り速度 vf(mm/min)
Small stepdown Feed rate 530 190
課題:立壁加工精度 Task: Vertical wall
machining accuracy 課題:加工時間 Task:
Machining time 1刃送り量 fz(mm/t)
Revolution 0.05 0.06
Zピックap(mm)
Stepdown 6 50
提案 取り代 ae(mm)
EPWB8-ATHを使用することで修正工数を大幅削減 Machining allowance 0.05
P r o p o s a l 狙い通りの精度を最短工程で!! 修正回数 1回 time 4回 times
Using the EPWB8-ATH significantly reduces reworking and correction steps. Number of corrections (径補正による最終精度調整のみ) (倒れや精度調整のためゼロカットと径補正を繰り返す)
Achieve the intended accuracy in fewer steps! (Final accuracy adjustment by diameter compensation only) (Repeated zero cutting and diameter compensation to correct wall deflection and adjust accuracy)
トータル立壁
仕上げ加工時間 11分 min. 19分 min.
Total vertical wall finishing time
修正時間 再加工や測定などの修正工数を削減し
Correction time
金型製造の省人化に貢献
大きなZピック 42%
Large stepdown 短縮 Reduces reworking, measurement, and other correction steps,
contributing to labor savings in mold manufacturing.
reduction
02 03
立壁加工深さ(mm)
Vertical wall milling depth
Page3
立壁と底面の仕上げ加工の“極”
これ1本で立壁と底面を仕上げる!
The Zenith of Milling for Vertical Wall and Bottom Face Finishing
Vertical wall and bottom face finishing with a single tool!
倒れの少ない加工で再加工時間の大幅な削減を実現
EPWB8-ATHの特長 Minimal-deflection machining significantly reduces reworking time. 動画公開中
EPWB8-ATH features
被削材 Work material:STAVAX(52HRC) 機械 Machine:立形MC(HSK-A63) Vertical MC
01 立壁加工に特化した外周刃設計を採用。
倒れが少なく狙い通りの加工を実現でき、再加工や修正工数を低減 1回仕上げ加工後の壁面の倒れ
します。 Vertical wall deflection after a single finishing pass
0
Peripheral cutting edge design tailored for vertical wall milling
Allows milling as intended with minimal deflection, reducing re-machining and re-working steps.
10
02 独自のコーナR刃により高品位な底面加工を実現 20
Incorporates MOLDINO's own corner radius edges to achieve high-quality bottom face milling. 従来ロング刃長エンドミル
Conventional long flute end mill
30
40
EPWB8-ATH
適応範囲 ラジアスタイプ:φ6~φ12[ 57ア イテム] 50
Application range 加工 Radius 0 5 10 15 20 25
用途 type (コーナ半径RE0.2, 0.5, 1.0) Items
Corner radius RE0.2, 0.5, 1.0
銅 炭素鋼 プリハードン鋼 焼入れ鋼 焼入れ鋼 立壁倒れ量 Vertical wall deflection(μm)
Applications
合金鋼 45~55HRC 55~72HRC 金型製作 スクエアタイプ : φ6~φ12[ 19ア イテム]
Copper Carbon steel Pre-hardened Hardened steel Hardened steel
Alloy steel steel 45̃55HRC 55̃72HRC
Mold making Square type Items
ポケットサイズ:70×70×深さ50mm(隅R8) ※両工具とも呼び径で加工 * Machined using nominal diameter for both tools
Pocket size depth Corner
EPWB8-ATH 従来ロング刃長エンドミル
課題 1 金型の立壁仕上げ加工でロング刃長エンドミルを使用する 2 等高線加工でZピックを小さくすると、立壁加工 Conventional long flute end mill
と精度が出ず、測定と再加工などの修正に工数がかかる 精度は確保できるが、加工時間が長くなる φ12- 首下 under neck 60mm
T a s k φ12- 刃長 flute length 55mm
Using long-flute end mills for vertical walls of molds reduces accuracy and requires Reducing stepdown when contour milling achieves machining
time-consuming measurement, reworking, and other corrective processes. accuracy for vertical walls but increases machining time.
回転数 n(min-1)
Revolution 1326 530
切削速度 vc(m/min)
Cutting speed 50 20
小さなZピック 送り速度 vf(mm/min)
Small stepdown Feed rate 530 190
課題:立壁加工精度 Task: Vertical wall
machining accuracy 課題:加工時間 Task:
Machining time 1刃送り量 fz(mm/t)
Revolution 0.05 0.06
Zピックap(mm)
Stepdown 6 50
提案 取り代 ae(mm)
EPWB8-ATHを使用することで修正工数を大幅削減 Machining allowance 0.05
P r o p o s a l 狙い通りの精度を最短工程で!! 修正回数 1回 time 4回 times
Using the EPWB8-ATH significantly reduces reworking and correction steps. Number of corrections (径補正による最終精度調整のみ) (倒れや精度調整のためゼロカットと径補正を繰り返す)
Achieve the intended accuracy in fewer steps! (Final accuracy adjustment by diameter compensation only) (Repeated zero cutting and diameter compensation to correct wall deflection and adjust accuracy)
トータル立壁
仕上げ加工時間 11分 min. 19分 min.
Total vertical wall finishing time
修正時間 再加工や測定などの修正工数を削減し
Correction time
金型製造の省人化に貢献
大きなZピック 42%
Large stepdown 短縮 Reduces reworking, measurement, and other correction steps,
contributing to labor savings in mold manufacturing.
reduction
02 03
立壁加工深さ(mm)
Vertical wall milling depth
Page4
特長 ラインナップ
Features Line up
特長 立壁加工に特化した外周刃設計
Features 01 スクエア Square
Peripheral cutting edge design tailored for vertical wall milling
EPWB8-ATHによる立壁仕上げ加工 従来ロング刃長エンドミルの立壁仕上げ加工 APMX APMX
LU
LF LF
Vertical wall finishing using EPWB8-ATH Vertical wall finishing with conventional long-flute end mill Aタイプ A type Bタイプ B type
ねじれ 0 0
38° -0.015 -0.02
EPWB8 - -ATH 超硬
Carbide Helix angle φ6 φ7~φ12 φ6,8,10,12 φ7,9,11
刃長 寸 法 Size(mm)
Flute
length 商品コード 在庫 外径 刃長 首下長 首径 全長 シャンク径 形状 備考
刃長 Item code Stock Tool dia. Flute length Under neck length Neck dia. Overall length Shank dia.
Shape Note
Flute DC APMX LU DN LF DCONMS
length EPWB8060-20-ATH ● 6 20 5.88 58 6 A
EPWB8060-30-ATH ● 6 30 5.88 68 6 A
6
EPWB8060-40-ATH ● 6 40 5.88 78 6 A
・短刃長で高剛性⇒たわみを抑制 ・突き出し(刃長)が長い⇒たわみ発生
ソリューション EPWB8060-50-ATH ● 6 50 5.88 88 6 A
・接触ポイントが少ない工具設計⇒振動抑制 課題 ・接触ポイントが多い⇒振動大
Solution ・ EPWB8070-ATH ● 7 7 - - 90 6 B
Short flute gives high rigidity => Minimizes deflection T a s k ・Extended overhang length (flute length) => Deflection
・Tool design with few contact points => Minimizes vibration ・Multiple contact points=> Increased vibration EPWB8080-30-ATH ● 8 30 7.84 68 8 A
EPWB8080-40-ATH ● 8 40 7.84 78 8 A
● 8
切削抵抗の比較 EPWB8080-50-ATH 8 50 7.84 88 8 A
Comparison of cutting force
EPWB8080-60-ATH ● 8 60 7.84 98 8 A
被削材 Work material:SKD61(48HRC) 機械 Machine:立型 Vertical MC(BT40) クーラント Coolant:エアーブロー Air blow 突き出し量 Overhang:30mm(L/D=5) EPWB8090-ATH ● 9 9 - - 100 8 B
EPWB8-ATH 従来ロング刃長エンドミル EPWB8100-35-ATH ● 10 35 9.8 77 10 A
Conventional long flute end mill
EPWB8100-50-ATH ● 10 50 9.8 92 10 A
EPWB8100-60-ATH ● 10
10 60 9.8 102 10 A
EPWB8100-80-ATH ● 10 80 9.8 122 10 A
EPWB8110-ATH ● 11 11 - - 110 10 B
使用工具:EPWB8060-30-ATH
(φ6刃長6㎜ 首下長30㎜) 使用工具:6枚刃ロング刃長 EPWB8120-40-ATH ● 12 40 11.8 87 12 A
Tool : EPWB8060-30-ATH (φ6刃長25mm)
(φ6, Flute length 6mm, Under neck length 30mm) Tool : 6flutes long flute (φ6, Flute length 25mm)
最大合力:70N 切削条件:n=2650min-1 最大合力:384N EPWB8120-60-ATH ● 12 60 11.8 107 12 A
Maximum total force Maximum total force 切削条件:n=2650min-1 ● 12
Cut ting (vc50m/min) Cut ting EPWB8120-80-ATH
conditions conditi ons (vc50m/min) 12 80 11.8 127 12 A
vf=636mm/min vf477mm/min
( EPWB8120-100-ATH ●
fz0.03mm/t) 12 100 11.8 147 12 A
(fz0.03mm/t)
ap3mm ae0.1mm ap25mm ae0.1mm
切削抵抗と振動の低減 切削抵抗が大きく振動が発生
Reduced cutting force and vibration Large cutting force, resulting in vibration
ここが ポイント! 切削抵抗と振動を低減する独自の設計により倒れの少ない狙い通りの ES8WB-ATH、ER8WB-ATH、は2026年10月をもって
This is the point 加工が可能になります。 生産を終了します。
The unique design reducing cutting force and vibration allows milling as intended with minimal deflection. 本商品の刃径・首下長が同一のアイテムへの切り替えを
特長 独自のコーナR刃設計 お願いいたします。
※ラジアスタイプのみ
Features 02 MOLDINO's unique corner radius cutting edge design * Radius type only The ES8WB-ATH and ER8WB-ATH will be discontinued in October 2026.
Please switch to the corresponding items in this series with the same cutting
すくい面視
View on cutting face EPWB8-ATH 従来4枚刃ラジアスエンドミル diameter and under-neck length.
Conventional 4flutes radius end mill
送り方向 送り方向 ※EPWB8-ATHはER8WB・ES8WBと全長寸法が異なります(Bタイプを除く)。
Feed direction Feed direction
工具選定の際は寸法をご確認ください。
R刃
R cutting edge * The overall length of the EPWB8-ATH differs from that of the ER8WB-ATH and ES8WB-ATH, except for B-type items.
Please verify the dimensions before tool selection.
底刃
Bottom cutting edge
1mm 1mm
0.5mm 0.1mm 光沢があり 加工面が白濁
均一なカッターマーク 不均一なカッターマーク
Shiny appearance Milled surface appears cloudy.
with uniform cutter marks Uneven cutter marks
底刃とR刃をスムーズにつなぐことで
被削材 Work material:S50C 機械 Machine:立型 Vertical MC(BT40)
高品位な底面加工を実現 クーラント Coolant:エアーブロー Air blow 突き出し量 Overhang:60mm(L/D=5)
使用工具:従来4枚刃ラジアスエンドミル EPWB8120-60-10-ATH(φ12)
Smooth interface between bottom and radius cutting edges Tool : Conventional 4flutes radius end mill, EPWB8120-60-10-ATH (φ12)
ensures high-quality bottom face milling. 切削条件:n=5310min-1(vc200m/min) fz=0.06mm/t ap0.05mm ae6mm
Cutting conditions ●印:標準在庫品です。●:Stocked items.
04 05
3方向合力値(N)
Total resulting force
加工ワーク
Work
3方向合力値(N)
Total resulting force
加工ワーク
Work
DC
DN
DCONMS
DC
DCONMS
Page5
特長 ラインナップ
Features Line up
特長 立壁加工に特化した外周刃設計
Features 01 スクエア Square
Peripheral cutting edge design tailored for vertical wall milling
EPWB8-ATHによる立壁仕上げ加工 従来ロング刃長エンドミルの立壁仕上げ加工 APMX APMX
LU
LF LF
Vertical wall finishing using EPWB8-ATH Vertical wall finishing with conventional long-flute end mill Aタイプ A type Bタイプ B type
ねじれ 0 0
38° -0.015 -0.02
EPWB8 - -ATH 超硬
Carbide Helix angle φ6 φ7~φ12 φ6,8,10,12 φ7,9,11
刃長 寸 法 Size(mm)
Flute
length 商品コード 在庫 外径 刃長 首下長 首径 全長 シャンク径 形状 備考
刃長 Item code Stock Tool dia. Flute length Under neck length Neck dia. Overall length Shank dia.
Shape Note
Flute DC APMX LU DN LF DCONMS
length EPWB8060-20-ATH ● 6 20 5.88 58 6 A
EPWB8060-30-ATH ● 6 30 5.88 68 6 A
6
EPWB8060-40-ATH ● 6 40 5.88 78 6 A
・短刃長で高剛性⇒たわみを抑制 ・突き出し(刃長)が長い⇒たわみ発生
ソリューション EPWB8060-50-ATH ● 6 50 5.88 88 6 A
・接触ポイントが少ない工具設計⇒振動抑制 課題 ・接触ポイントが多い⇒振動大
Solution ・ EPWB8070-ATH ● 7 7 - - 90 6 B
Short flute gives high rigidity => Minimizes deflection T a s k ・Extended overhang length (flute length) => Deflection
・Tool design with few contact points => Minimizes vibration ・Multiple contact points=> Increased vibration EPWB8080-30-ATH ● 8 30 7.84 68 8 A
EPWB8080-40-ATH ● 8 40 7.84 78 8 A
● 8
切削抵抗の比較 EPWB8080-50-ATH 8 50 7.84 88 8 A
Comparison of cutting force
EPWB8080-60-ATH ● 8 60 7.84 98 8 A
被削材 Work material:SKD61(48HRC) 機械 Machine:立型 Vertical MC(BT40) クーラント Coolant:エアーブロー Air blow 突き出し量 Overhang:30mm(L/D=5) EPWB8090-ATH ● 9 9 - - 100 8 B
EPWB8-ATH 従来ロング刃長エンドミル EPWB8100-35-ATH ● 10 35 9.8 77 10 A
Conventional long flute end mill
EPWB8100-50-ATH ● 10 50 9.8 92 10 A
EPWB8100-60-ATH ● 10
10 60 9.8 102 10 A
EPWB8100-80-ATH ● 10 80 9.8 122 10 A
EPWB8110-ATH ● 11 11 - - 110 10 B
使用工具:EPWB8060-30-ATH
(φ6刃長6㎜ 首下長30㎜) 使用工具:6枚刃ロング刃長 EPWB8120-40-ATH ● 12 40 11.8 87 12 A
Tool : EPWB8060-30-ATH (φ6刃長25mm)
(φ6, Flute length 6mm, Under neck length 30mm) Tool : 6flutes long flute (φ6, Flute length 25mm)
最大合力:70N 切削条件:n=2650min-1 最大合力:384N EPWB8120-60-ATH ● 12 60 11.8 107 12 A
Maximum total force Maximum total force 切削条件:n=2650min-1 ● 12
Cut ting (vc50m/min) Cut ting EPWB8120-80-ATH
conditions conditi ons (vc50m/min) 12 80 11.8 127 12 A
vf=636mm/min vf477mm/min
( EPWB8120-100-ATH ●
fz0.03mm/t) 12 100 11.8 147 12 A
(fz0.03mm/t)
ap3mm ae0.1mm ap25mm ae0.1mm
切削抵抗と振動の低減 切削抵抗が大きく振動が発生
Reduced cutting force and vibration Large cutting force, resulting in vibration
ここが ポイント! 切削抵抗と振動を低減する独自の設計により倒れの少ない狙い通りの ES8WB-ATH、ER8WB-ATH、は2026年10月をもって
This is the point 加工が可能になります。 生産を終了します。
The unique design reducing cutting force and vibration allows milling as intended with minimal deflection. 本商品の刃径・首下長が同一のアイテムへの切り替えを
特長 独自のコーナR刃設計 お願いいたします。
※ラジアスタイプのみ
Features 02 MOLDINO's unique corner radius cutting edge design * Radius type only The ES8WB-ATH and ER8WB-ATH will be discontinued in October 2026.
Please switch to the corresponding items in this series with the same cutting
すくい面視
View on cutting face EPWB8-ATH 従来4枚刃ラジアスエンドミル diameter and under-neck length.
Conventional 4flutes radius end mill
送り方向 送り方向 ※EPWB8-ATHはER8WB・ES8WBと全長寸法が異なります(Bタイプを除く)。
Feed direction Feed direction
工具選定の際は寸法をご確認ください。
R刃
R cutting edge * The overall length of the EPWB8-ATH differs from that of the ER8WB-ATH and ES8WB-ATH, except for B-type items.
Please verify the dimensions before tool selection.
底刃
Bottom cutting edge
1mm 1mm
0.5mm 0.1mm 光沢があり 加工面が白濁
均一なカッターマーク 不均一なカッターマーク
Shiny appearance Milled surface appears cloudy.
with uniform cutter marks Uneven cutter marks
底刃とR刃をスムーズにつなぐことで
被削材 Work material:S50C 機械 Machine:立型 Vertical MC(BT40)
高品位な底面加工を実現 クーラント Coolant:エアーブロー Air blow 突き出し量 Overhang:60mm(L/D=5)
使用工具:従来4枚刃ラジアスエンドミル EPWB8120-60-10-ATH(φ12)
Smooth interface between bottom and radius cutting edges Tool : Conventional 4flutes radius end mill, EPWB8120-60-10-ATH (φ12)
ensures high-quality bottom face milling. 切削条件:n=5310min-1(vc200m/min) fz=0.06mm/t ap0.05mm ae6mm
Cutting conditions ●印:標準在庫品です。●:Stocked items.
04 05
3方向合力値(N)
Total resulting force
加工ワーク
Work
3方向合力値(N)
Total resulting force
加工ワーク
Work
DC
DN
DCONMS
DC
DCONMS
Page6
ラインナップ
Line up
ラジアス Radius
RE APMX RE APMX
LU
LF LF
Aタイプ A type Bタイプ B type
C R ねじれ 0 0
38° -0.015 -0.02 C R ねじれ 0 0
38° -0.015 -0.02
EPWB8 - - -ATH 超硬 EPWB8 - - -ATH 超硬
Carbide Helix angle φ6 φ7~φ12 φ6,8,10,12 φ7,9,11 Carbide Helix angle φ6 φ7~φ12 φ6,8,10,12 φ7,9,11
寸 法 Size(mm) 寸 法 Size(mm)
商品コード 在庫 外径 コーナ半径 刃長 首下長 首径 全長 シャンク径 形状 備考 商品コード 在庫 外径 コーナ半径 刃長 首下長 首径 全長 シャンク径 形状 備考
Item code Stock Tool dia. Corner radius Flute length Under neck length Neck dia. Overall length Shank dia. Shape Note Item code Stock Tool dia. Corner radius Flute length Under neck length Neck dia. Overall length Shank dia. Shape Note
DC RE APMX LU DN LF DCONMS DC RE APMX LU DN LF DCONMS
EPWB8060-20-02-ATH ● 0.2 7 20 5.88 58 6 A EPWB8110-02-ATH ● 0.2 12 - - 110 10 B
EPWB8060-20-05-ATH ● 0.5 7 20 5.88 58 6 A EPWB8110-05-ATH ● 11 0.5 12 - - 110 10 B
EPWB8060-20-10-ATH ● 1 7 20 5.88 58 6 A EPWB8110-10-ATH ● 1 12 - - 110 10 B
EPWB8060-30-02-ATH ● 0.2 7 30 5.88 68 6 A EPWB8120-40-02-ATH ● 0.2 13 40 11.8 87 12 A
EPWB8060-30-05-ATH ● 0.5 7 30 5.88 68 6 A EPWB8120-40-05-ATH ● 0.5 13 40 11.8 87 12 A
EPWB8060-30-10-ATH ● 1 7 30 5.88 68 6 A EPWB8120-40-10-ATH ● 1 13 40 11.8 87 12 A
6
EPWB8060-40-02-ATH ● 0.2 7 40 5.88 78 6 A EPWB8120-60-02-ATH ● 0.2 13 60 11.8 107 12 A
EPWB8060-40-05-ATH ● 0.5 7 40 5.88 78 6 A EPWB8120-60-05-ATH ● 0.5 13 60 11.8 107 12 A
EPWB8060-40-10-ATH ● 1 7 40 5.88 78 6 A EPWB8120-60-10-ATH ● 1 13 60 11.8 107 12 A
12
EPWB8060-50-02-ATH ● 0.2 7 50 5.88 88 6 A EPWB8120-80-02-ATH ● 0.2 13 80 11.8 127 12 A
EPWB8060-50-05-ATH ● 0.5 7 50 5.88 88 6 A EPWB8120-80-05-ATH ● 0.5 13 80 11.8 127 12 A
EPWB8060-50-10-ATH ● 1 7 50 5.88 88 6 A EPWB8120-80-10-ATH ● 1 13 80 11.8 127 12 A
EPWB8070-02-ATH ● 0.2 8 - - 90 6 B EPWB8120-100-02-ATH ● 0.2 13 100 11.8 147 12 A
EPWB8070-05-ATH ● 7 0.5 8 - - 90 6 B EPWB8120-100-05-ATH ● 0.5 13 100 11.8 147 12 A
EPWB8070-10-ATH ● 1 8 - - 90 6 B EPWB8120-100-10-ATH ● 1 13 100 11.8 147 12 A
EPWB8080-30-02-ATH ● 0.2 9 30 7.84 68 8 A
EPWB8080-30-05-ATH ● 0.5 9 30 7.84 68 8 A
EPWB8080-30-10-ATH ● 1 9 30 7.84 68 8 A
EPWB8080-40-02-ATH ● 0.2 9 40 7.84 78 8 A
EPWB8080-40-05-ATH ● 0.5 9 40 7.84 78 8 A
EPWB8080-40-10-ATH ● 1 9 40 7.84 78 8 A
8
EPWB8080-50-02-ATH ● 0.2 9 50 7.84 88 8 A
EPWB8080-50-05-ATH ● 0.5 9 50 7.84 88 8 A
EPWB8080-50-10-ATH ● 1 9 50 7.84 88 8 A
EPWB8080-60-02-ATH ● 0.2 9 60 7.84 98 8 A
EPWB8080-60-05-ATH ● 0.5 9 60 7.84 98 8 A
EPWB8080-60-10-ATH ● 1 9 60 7.84 98 8 A
EPWB8090-02-ATH ● 0.2 10 - - 100 8 B
EPWB8090-05-ATH ● 9 0.5 10 - - 100 8 B
EPWB8090-10-ATH ● 1 10 - - 100 8 B
EPWB8100-35-02-ATH ● 0.2 11 35 9.8 77 10 A
EPWB8100-35-05-ATH ● 0.5 11 35 9.8 77 10 A
EPWB8100-35-10-ATH ● 1 11 35 9.8 77 10 A
EPWB8100-50-02-ATH ● 0.2 11 50 9.8 92 10 A
EPWB8100-50-05-ATH ● 0.5 11 50 9.8 92 10 A
EPWB8100-50-10-ATH ● 1 11 50 9.8 92 10 A
10 再研磨対応範囲一覧表 Regrinding compatibility range table
EPWB8100-60-02-ATH ● 0.2 11 60 9.8 102 10 A
EPWB8100-60-05-ATH ● 0.5 11 60 9.8 102 10 A 商品コード 商品名称 ラインナップ 形 状 再研磨対応外径範囲(㎜)
Re-grinding compatibility range
EPWB8100-60-10-ATH ● 1 11 60 9.8 102 10 A Item code Product name 外径(㎜)
Line up tool dia. Shape 外周 Outer dia. エンド End
EPWB8100-80-02-ATH ● 0.2 11 80 9.8 122 10 A EPWB8-ATH 立壁/底面仕上げ用8枚刃エンドミル スクエアタイプ
8-flutes End Mill for Vertical Wall/Bottom Face Finishing (Square type) 6 ~12 6~12 6~12
EPWB8100-80-05-ATH ● 0.5 11 80 9.8 122 10 A
EPWB8-CR-ATH 立壁/底面仕上げ用8枚刃エンドミル ラジアスタイプ
EPWB8100-80-10-ATH ● 1 11 80 9.8 122 10 A 8-flutes End Mill for Vertical Wall/Bottom Face Finishing (Radius type) 6~12 6~12 6~12
●印:標準在庫品です。●:Stocked items.
06 07
DC
DN
DCONMS
DC
DCONMS
Page7
ラインナップ
Line up
ラジアス Radius
RE APMX RE APMX
LU
LF LF
Aタイプ A type Bタイプ B type
C R ねじれ 0 0
38° -0.015 -0.02 C R ねじれ 0 0
38° -0.015 -0.02
EPWB8 - - -ATH 超硬 EPWB8 - - -ATH 超硬
Carbide Helix angle φ6 φ7~φ12 φ6,8,10,12 φ7,9,11 Carbide Helix angle φ6 φ7~φ12 φ6,8,10,12 φ7,9,11
寸 法 Size(mm) 寸 法 Size(mm)
商品コード 在庫 外径 コーナ半径 刃長 首下長 首径 全長 シャンク径 形状 備考 商品コード 在庫 外径 コーナ半径 刃長 首下長 首径 全長 シャンク径 形状 備考
Item code Stock Tool dia. Corner radius Flute length Under neck length Neck dia. Overall length Shank dia. Shape Note Item code Stock Tool dia. Corner radius Flute length Under neck length Neck dia. Overall length Shank dia. Shape Note
DC RE APMX LU DN LF DCONMS DC RE APMX LU DN LF DCONMS
EPWB8060-20-02-ATH ● 0.2 7 20 5.88 58 6 A EPWB8110-02-ATH ● 0.2 12 - - 110 10 B
EPWB8060-20-05-ATH ● 0.5 7 20 5.88 58 6 A EPWB8110-05-ATH ● 11 0.5 12 - - 110 10 B
EPWB8060-20-10-ATH ● 1 7 20 5.88 58 6 A EPWB8110-10-ATH ● 1 12 - - 110 10 B
EPWB8060-30-02-ATH ● 0.2 7 30 5.88 68 6 A EPWB8120-40-02-ATH ● 0.2 13 40 11.8 87 12 A
EPWB8060-30-05-ATH ● 0.5 7 30 5.88 68 6 A EPWB8120-40-05-ATH ● 0.5 13 40 11.8 87 12 A
EPWB8060-30-10-ATH ● 1 7 30 5.88 68 6 A EPWB8120-40-10-ATH ● 1 13 40 11.8 87 12 A
6
EPWB8060-40-02-ATH ● 0.2 7 40 5.88 78 6 A EPWB8120-60-02-ATH ● 0.2 13 60 11.8 107 12 A
EPWB8060-40-05-ATH ● 0.5 7 40 5.88 78 6 A EPWB8120-60-05-ATH ● 0.5 13 60 11.8 107 12 A
EPWB8060-40-10-ATH ● 1 7 40 5.88 78 6 A EPWB8120-60-10-ATH ● 1 13 60 11.8 107 12 A
12
EPWB8060-50-02-ATH ● 0.2 7 50 5.88 88 6 A EPWB8120-80-02-ATH ● 0.2 13 80 11.8 127 12 A
EPWB8060-50-05-ATH ● 0.5 7 50 5.88 88 6 A EPWB8120-80-05-ATH ● 0.5 13 80 11.8 127 12 A
EPWB8060-50-10-ATH ● 1 7 50 5.88 88 6 A EPWB8120-80-10-ATH ● 1 13 80 11.8 127 12 A
EPWB8070-02-ATH ● 0.2 8 - - 90 6 B EPWB8120-100-02-ATH ● 0.2 13 100 11.8 147 12 A
EPWB8070-05-ATH ● 7 0.5 8 - - 90 6 B EPWB8120-100-05-ATH ● 0.5 13 100 11.8 147 12 A
EPWB8070-10-ATH ● 1 8 - - 90 6 B EPWB8120-100-10-ATH ● 1 13 100 11.8 147 12 A
EPWB8080-30-02-ATH ● 0.2 9 30 7.84 68 8 A
EPWB8080-30-05-ATH ● 0.5 9 30 7.84 68 8 A
EPWB8080-30-10-ATH ● 1 9 30 7.84 68 8 A
EPWB8080-40-02-ATH ● 0.2 9 40 7.84 78 8 A
EPWB8080-40-05-ATH ● 0.5 9 40 7.84 78 8 A
EPWB8080-40-10-ATH ● 1 9 40 7.84 78 8 A
8
EPWB8080-50-02-ATH ● 0.2 9 50 7.84 88 8 A
EPWB8080-50-05-ATH ● 0.5 9 50 7.84 88 8 A
EPWB8080-50-10-ATH ● 1 9 50 7.84 88 8 A
EPWB8080-60-02-ATH ● 0.2 9 60 7.84 98 8 A
EPWB8080-60-05-ATH ● 0.5 9 60 7.84 98 8 A
EPWB8080-60-10-ATH ● 1 9 60 7.84 98 8 A
EPWB8090-02-ATH ● 0.2 10 - - 100 8 B
EPWB8090-05-ATH ● 9 0.5 10 - - 100 8 B
EPWB8090-10-ATH ● 1 10 - - 100 8 B
EPWB8100-35-02-ATH ● 0.2 11 35 9.8 77 10 A
EPWB8100-35-05-ATH ● 0.5 11 35 9.8 77 10 A
EPWB8100-35-10-ATH ● 1 11 35 9.8 77 10 A
EPWB8100-50-02-ATH ● 0.2 11 50 9.8 92 10 A
EPWB8100-50-05-ATH ● 0.5 11 50 9.8 92 10 A
EPWB8100-50-10-ATH ● 1 11 50 9.8 92 10 A
10 再研磨対応範囲一覧表 Regrinding compatibility range table
EPWB8100-60-02-ATH ● 0.2 11 60 9.8 102 10 A
EPWB8100-60-05-ATH ● 0.5 11 60 9.8 102 10 A 商品コード 商品名称 ラインナップ 形 状 再研磨対応外径範囲(㎜)
Re-grinding compatibility range
EPWB8100-60-10-ATH ● 1 11 60 9.8 102 10 A Item code Product name 外径(㎜)
Line up tool dia. Shape 外周 Outer dia. エンド End
EPWB8100-80-02-ATH ● 0.2 11 80 9.8 122 10 A EPWB8-ATH 立壁/底面仕上げ用8枚刃エンドミル スクエアタイプ
8-flutes End Mill for Vertical Wall/Bottom Face Finishing (Square type) 6 ~12 6~12 6~12
EPWB8100-80-05-ATH ● 0.5 11 80 9.8 122 10 A
EPWB8-CR-ATH 立壁/底面仕上げ用8枚刃エンドミル ラジアスタイプ
EPWB8100-80-10-ATH ● 1 11 80 9.8 122 10 A 8-flutes End Mill for Vertical Wall/Bottom Face Finishing (Radius type) 6~12 6~12 6~12
●印:標準在庫品です。●:Stocked items.
06 07
DC
DN
DCONMS
DC
DCONMS
Page8
標準切削条件表
Recommended Cut t ing Condi t ions
立壁仕上げ Vertical wall finishing 底面仕上げ Bottom face finishing
※底面仕上げはラジアスタイプをご使用ください。 A radius type should be used for bottom face finishing.
被削材 炭素鋼・合金鋼 工具鋼 プリハードン鋼 焼入れ鋼
Carbon steels, Alloy steels Tool steels Pre-hardened steels Hardened steels 被削材 炭素鋼・合金鋼 工具鋼 プリハードン鋼 焼入れ鋼
Carbon steels, Alloy steels Tool steels Pre-hardened steels Hardened steels
Work material (180~250HB) (25~35HRC) (35~45HRC) (45~55HRC) Work material (180~250HB) (25~35HRC) (35~45HRC) (45~55HRC)
商品コード 軸切込み 径切込み 回転数 送り速度 回転数 送り速度 回転数 送り速度 回転数 送り速度
ap ae n v f n v f n v f n v f 商品コード 軸切込み 径切込み 回転数 送り速度 回転数 送り速度 回転数 送り速度 回転数 送り速度
ap ae n v f n v f n v f n v f
Item code (mm) (mm) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) Item code (mm) (mm) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min)
EPWB8060-20-(○○)-ATH 3 ≦0.1 7960 1910 6370 1530 4770 1140 3180 760 EPWB8060-20-○○-ATH 0.05~0.1 3~6 9550 2290 7960 1910 6370 1530 4770 1140
EPWB8060-30-(○○)-ATH 3 ≦0.1 6630 1590 5310 1270 3980 960 2650 640 EPWB8060-30-○○-ATH 0.05~0.1 3~6 7960 1910 6630 1590 5310 1270 3980 960
EPWB8060-40-(○○)-ATH 3 ≦0.1 4640 780 3710 620 2790 470 1860 310 EPWB8060-40-○○-ATH 0.05~0.1 3~6 5570 940 4640 780 3710 620 2790 470
EPWB8060-50-(○○)-ATH 3 ≦0.1 3320 400 2650 320 1990 240 1330 160 EPWB8060-50-○○-ATH 0.05~0.1 3~6 3980 480 3320 400 2650 320 1990 240
EPWB8070-(○○)-ATH 3.5 ≦0.1 5680 1590 4550 1270 3410 950 2270 640 EPWB8070-○○-ATH 0.05~0.1 3.5~7 6820 1910 5680 1590 4550 1270 3410 950
EPWB8080-30-(○○)-ATH 4 ≦0.1 5970 1910 4770 1530 3580 1150 2390 760 EPWB8080-30-○○-ATH 0.05~0.1 4~8 7160 2290 5970 1910 4770 1530 3580 1150
EPWB8080-40-(○○)-ATH 4 ≦0.1 4970 1590 3980 1270 2980 950 1990 640 EPWB8080-40-○○-ATH 0.05~0.1 4~8 5970 1910 4970 1590 3980 1270 2980 950
EPWB8080-50-(○○)-ATH 4 ≦0.1 3480 890 2790 620 2090 540 1390 360 EPWB8080-50-○○-ATH 0.05~0.1 4~8 4180 1070 3480 890 2790 710 2090 540
EPWB8080-60-(○○)-ATH 4 ≦0.1 2490 400 1990 320 1490 240 990 160 EPWB8080-60-○○-ATH 0.05~0.1 4~8 2980 480 2490 400 1990 320 1490 240
EPWB8090-(○○)-ATH 4.5 ≦0.1 4420 1590 3540 1270 2650 950 1770 640 EPWB8090-○○-ATH 0.05~0.1 4.5~9 5310 1910 4420 1590 3540 1270 2650 950
EPWB8100-35-(○○)-ATH 5 ≦0.1 4770 1910 3820 1530 2860 1140 1910 760 EPWB8100-35-○○-ATH 0.05~0.1 5~10 5730 2290 4770 1910 3820 1530 2860 1140
EPWB8100-50-(○○)-ATH 5 ≦0.1 3980 1590 3180 1270 2390 960 1590 640 EPWB8100-50-○○-ATH 0.05~0.1 5~10 4770 1910 3980 1590 3180 1270 2390 960
EPWB8100-60-(○○)-ATH 5 ≦0.1 2790 890 2230 620 1670 530 1110 360 EPWB8100-60-○○-ATH 0.05~0.1 5~10 3340 1070 2790 890 2230 710 1670 530
EPWB8100-80-(○○)-ATH 5 ≦0.1 1990 400 1590 320 1190 240 800 160 EPWB8100-80-○○-ATH 0.05~0.1 5~10 2390 480 1990 400 1590 320 1190 240
EPWB8110-(○○)-ATH 5.5 ≦0.1 3620 1510 2890 1210 2170 910 1450 610 EPWB8110-○○-ATH 0.05~0.1 5.5~11 4340 1810 3620 1510 2890 1210 2170 910
EPWB8120-40-(○○)-ATH 6 ≦0.1 3980 1720 3180 1370 2390 1030 1590 690 EPWB8120-40-○○-ATH 0.05~0.1 6~12 4770 2060 3980 1720 3180 1370 2390 1030
EPWB8120-60-(○○)-ATH 6 ≦0.1 3320 1430 2650 1140 1990 860 1330 570 EPWB8120-60-○○-ATH 0.05~0.1 6~12 3980 1720 3320 1430 2650 1140 1990 860
EPWB8120-80-(○○)-ATH 6 ≦0.1 2320 700 1860 560 1390 420 930 280 EPWB8120-80-○○-ATH 0.05~0.1 6~12 2790 840 2320 700 1860 560 1390 420
EPWB8120-100-(○○)-ATH 6 ≦0.1 1660 360 1330 290 990 210 660 140 EPWB8120-100-○○-ATH 0.05~0.1 6~12 1990 430 1660 360 1330 290 990 210
※スクエア・ラジアス同じ条件でご使用いただけます。 ○○はラジアスサイズです。 ※○○はラジアスサイズです。
* Identical cutting conditions are applicable to both square and radius types. ○○ indicates the corner radius size. * ○○ indicates the corner radius size.
※ロングシャンクタイプ(φ7,9,11)の切削条件は工具突き出し量が5D(工具径×5倍)時の条件です。突き出し量を変更する場合は下記補正値を参考に条件を設定ください。 ※ロングシャンクタイプ(φ7,9,11)の切削条件は工具突き出し量が5D(工具径×5倍)時の条件です。突き出し量を変更する場合は下記補正値を参考に条件を設定ください。
* Cutting conditions for the long-shank type (∅7/9/11) are for a tool overhang of 5DC (tool diameter × 5). Modify the conditions using the following correction factors if the overhang amount changes. * Cutting conditions for the long-shank type (∅7/9/11) are for a tool overhang of 5DC (tool diameter × 5). Modify the conditions using the following correction factors if the overhang amount changes.
ロングシャンクタイプの切削条件補正値 Cutting condition correction factors for long-shank type (%) ロングシャンクタイプの切削条件補正値 Cutting condition correction factors for long-shank type (%)
被削材 炭素鋼・合金鋼 工具鋼 プリハードン鋼 焼入れ鋼
Carbon steels, Alloy steels Tool steels Pre-hardened steels Hardened steels 被削材 炭素鋼・合金鋼 工具鋼 プリハードン鋼 焼入れ鋼
Carbon steels, Alloy steels Tool steels Pre-hardened steels Hardened steels
Work material (180~250HB) (25~35HRC) (35~45HRC) (45~55HRC) Work material (180~250HB) (25~35HRC) (35~45HRC) (45~55HRC)
突出し量 軸切込み 径切込み 回転数 送り速度 回転数 送り速度 回転数 送り速度 回転数 送り速度
ap ae n v f n v f n v f n v f 突出し量 軸切込み 径切込み 回転数 送り速度 回転数 送り速度 回転数 送り速度 回転数 送り速度
ap ae n v f n v f n v f n v f
Overhang (mm) (mm) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) Overhang (mm) (mm) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min)
5DC 100% 100% 100% 100% 100% 100% 100% 100% 100% 100% 5DC 100% 100% 100% 100% 100% 100% 100% 100% 100% 100%
6DC 100% 100% 70% 60% 70% 60% 70% 60% 70% 60% 6DC 100% 100% 70% 60% 70% 60% 70% 60% 70% 60%
7DC 100% 100% 70% 50% 70% 50% 70% 50% 70% 50% 7DC 100% 100% 70% 50% 70% 50% 70% 50% 70% 50%
【注意】①被削材、加工形状に合わせて、適切なクーラントを使用してください。 【注意】①被削材、加工形状に合わせて、適切なクーラントを使用してください。
②できるだけ高剛性、高精度の機械をご使用ください。 ②できるだけ高剛性、高精度の機械をご使用ください。
③この切削条件表は切削条件の目安を示すものです。実際の加工では加工形状、目的、使用機械等により条件を調整してください。 ③この切削条件表は切削条件の目安を示すものです。実際の加工では加工形状、目的、使用機械等により条件を調整してください。
④機械の回転数が足りない場合は、回転数と送り速度を同じ比率で下げてください。 ④機械の回転数が足りない場合は、回転数と送り速度を同じ比率で下げてください。
【Note】① Use the appropriate coolant for the work material and machining shape. ⑤溝切削の場合、送り速度を50%を目安に調整してください。
② Use a highly rigid and accurate machine as possible. ⑥傾斜切削の場合、傾斜角は0.5°以下、送り速度を50%を目安に調整してください。
③ These Recommended Cutting Conditions indicate only the rule of a thumb for the cutting conditions. In actual machining, the condition should be adjusted according to 【Note】① Use the appropriate coolant for the work material and machining shape.
the machining shape, purpose and the machine type. ② Use a highly rigid and accurate machine as possible.
④ If the rpm available is lower than that recommended please reduce the feed rate to the same ratio. ③ These Recommended Cutting Conditions indicate only the rule of a thumb for the cutting conditions. In actual machining, the condition should be adjusted according to
the machining shape, purpose and the machine type.
④ If the rpm available is lower than that recommended please reduce the feed rate to the same ratio.
⑤ For slotting, adjust the feed rate to 50% as general criteria.
⑥ For ramping, adjust the ramp angle to 0.5° or less and the feed rate to 50% as general criteria.
08 09
Page9
標準切削条件表
Recommended Cut t ing Condi t ions
立壁仕上げ Vertical wall finishing 底面仕上げ Bottom face finishing
※底面仕上げはラジアスタイプをご使用ください。 A radius type should be used for bottom face finishing.
被削材 炭素鋼・合金鋼 工具鋼 プリハードン鋼 焼入れ鋼
Carbon steels, Alloy steels Tool steels Pre-hardened steels Hardened steels 被削材 炭素鋼・合金鋼 工具鋼 プリハードン鋼 焼入れ鋼
Carbon steels, Alloy steels Tool steels Pre-hardened steels Hardened steels
Work material (180~250HB) (25~35HRC) (35~45HRC) (45~55HRC) Work material (180~250HB) (25~35HRC) (35~45HRC) (45~55HRC)
商品コード 軸切込み 径切込み 回転数 送り速度 回転数 送り速度 回転数 送り速度 回転数 送り速度
ap ae n v f n v f n v f n v f 商品コード 軸切込み 径切込み 回転数 送り速度 回転数 送り速度 回転数 送り速度 回転数 送り速度
ap ae n v f n v f n v f n v f
Item code (mm) (mm) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) Item code (mm) (mm) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min)
EPWB8060-20-(○○)-ATH 3 ≦0.1 7960 1910 6370 1530 4770 1140 3180 760 EPWB8060-20-○○-ATH 0.05~0.1 3~6 9550 2290 7960 1910 6370 1530 4770 1140
EPWB8060-30-(○○)-ATH 3 ≦0.1 6630 1590 5310 1270 3980 960 2650 640 EPWB8060-30-○○-ATH 0.05~0.1 3~6 7960 1910 6630 1590 5310 1270 3980 960
EPWB8060-40-(○○)-ATH 3 ≦0.1 4640 780 3710 620 2790 470 1860 310 EPWB8060-40-○○-ATH 0.05~0.1 3~6 5570 940 4640 780 3710 620 2790 470
EPWB8060-50-(○○)-ATH 3 ≦0.1 3320 400 2650 320 1990 240 1330 160 EPWB8060-50-○○-ATH 0.05~0.1 3~6 3980 480 3320 400 2650 320 1990 240
EPWB8070-(○○)-ATH 3.5 ≦0.1 5680 1590 4550 1270 3410 950 2270 640 EPWB8070-○○-ATH 0.05~0.1 3.5~7 6820 1910 5680 1590 4550 1270 3410 950
EPWB8080-30-(○○)-ATH 4 ≦0.1 5970 1910 4770 1530 3580 1150 2390 760 EPWB8080-30-○○-ATH 0.05~0.1 4~8 7160 2290 5970 1910 4770 1530 3580 1150
EPWB8080-40-(○○)-ATH 4 ≦0.1 4970 1590 3980 1270 2980 950 1990 640 EPWB8080-40-○○-ATH 0.05~0.1 4~8 5970 1910 4970 1590 3980 1270 2980 950
EPWB8080-50-(○○)-ATH 4 ≦0.1 3480 890 2790 620 2090 540 1390 360 EPWB8080-50-○○-ATH 0.05~0.1 4~8 4180 1070 3480 890 2790 710 2090 540
EPWB8080-60-(○○)-ATH 4 ≦0.1 2490 400 1990 320 1490 240 990 160 EPWB8080-60-○○-ATH 0.05~0.1 4~8 2980 480 2490 400 1990 320 1490 240
EPWB8090-(○○)-ATH 4.5 ≦0.1 4420 1590 3540 1270 2650 950 1770 640 EPWB8090-○○-ATH 0.05~0.1 4.5~9 5310 1910 4420 1590 3540 1270 2650 950
EPWB8100-35-(○○)-ATH 5 ≦0.1 4770 1910 3820 1530 2860 1140 1910 760 EPWB8100-35-○○-ATH 0.05~0.1 5~10 5730 2290 4770 1910 3820 1530 2860 1140
EPWB8100-50-(○○)-ATH 5 ≦0.1 3980 1590 3180 1270 2390 960 1590 640 EPWB8100-50-○○-ATH 0.05~0.1 5~10 4770 1910 3980 1590 3180 1270 2390 960
EPWB8100-60-(○○)-ATH 5 ≦0.1 2790 890 2230 620 1670 530 1110 360 EPWB8100-60-○○-ATH 0.05~0.1 5~10 3340 1070 2790 890 2230 710 1670 530
EPWB8100-80-(○○)-ATH 5 ≦0.1 1990 400 1590 320 1190 240 800 160 EPWB8100-80-○○-ATH 0.05~0.1 5~10 2390 480 1990 400 1590 320 1190 240
EPWB8110-(○○)-ATH 5.5 ≦0.1 3620 1510 2890 1210 2170 910 1450 610 EPWB8110-○○-ATH 0.05~0.1 5.5~11 4340 1810 3620 1510 2890 1210 2170 910
EPWB8120-40-(○○)-ATH 6 ≦0.1 3980 1720 3180 1370 2390 1030 1590 690 EPWB8120-40-○○-ATH 0.05~0.1 6~12 4770 2060 3980 1720 3180 1370 2390 1030
EPWB8120-60-(○○)-ATH 6 ≦0.1 3320 1430 2650 1140 1990 860 1330 570 EPWB8120-60-○○-ATH 0.05~0.1 6~12 3980 1720 3320 1430 2650 1140 1990 860
EPWB8120-80-(○○)-ATH 6 ≦0.1 2320 700 1860 560 1390 420 930 280 EPWB8120-80-○○-ATH 0.05~0.1 6~12 2790 840 2320 700 1860 560 1390 420
EPWB8120-100-(○○)-ATH 6 ≦0.1 1660 360 1330 290 990 210 660 140 EPWB8120-100-○○-ATH 0.05~0.1 6~12 1990 430 1660 360 1330 290 990 210
※スクエア・ラジアス同じ条件でご使用いただけます。 ○○はラジアスサイズです。 ※○○はラジアスサイズです。
* Identical cutting conditions are applicable to both square and radius types. ○○ indicates the corner radius size. * ○○ indicates the corner radius size.
※ロングシャンクタイプ(φ7,9,11)の切削条件は工具突き出し量が5D(工具径×5倍)時の条件です。突き出し量を変更する場合は下記補正値を参考に条件を設定ください。 ※ロングシャンクタイプ(φ7,9,11)の切削条件は工具突き出し量が5D(工具径×5倍)時の条件です。突き出し量を変更する場合は下記補正値を参考に条件を設定ください。
* Cutting conditions for the long-shank type (∅7/9/11) are for a tool overhang of 5DC (tool diameter × 5). Modify the conditions using the following correction factors if the overhang amount changes. * Cutting conditions for the long-shank type (∅7/9/11) are for a tool overhang of 5DC (tool diameter × 5). Modify the conditions using the following correction factors if the overhang amount changes.
ロングシャンクタイプの切削条件補正値 Cutting condition correction factors for long-shank type (%) ロングシャンクタイプの切削条件補正値 Cutting condition correction factors for long-shank type (%)
被削材 炭素鋼・合金鋼 工具鋼 プリハードン鋼 焼入れ鋼
Carbon steels, Alloy steels Tool steels Pre-hardened steels Hardened steels 被削材 炭素鋼・合金鋼 工具鋼 プリハードン鋼 焼入れ鋼
Carbon steels, Alloy steels Tool steels Pre-hardened steels Hardened steels
Work material (180~250HB) (25~35HRC) (35~45HRC) (45~55HRC) Work material (180~250HB) (25~35HRC) (35~45HRC) (45~55HRC)
突出し量 軸切込み 径切込み 回転数 送り速度 回転数 送り速度 回転数 送り速度 回転数 送り速度
ap ae n v f n v f n v f n v f 突出し量 軸切込み 径切込み 回転数 送り速度 回転数 送り速度 回転数 送り速度 回転数 送り速度
ap ae n v f n v f n v f n v f
Overhang (mm) (mm) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) Overhang (mm) (mm) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min) (min-1) (mm/min)
5DC 100% 100% 100% 100% 100% 100% 100% 100% 100% 100% 5DC 100% 100% 100% 100% 100% 100% 100% 100% 100% 100%
6DC 100% 100% 70% 60% 70% 60% 70% 60% 70% 60% 6DC 100% 100% 70% 60% 70% 60% 70% 60% 70% 60%
7DC 100% 100% 70% 50% 70% 50% 70% 50% 70% 50% 7DC 100% 100% 70% 50% 70% 50% 70% 50% 70% 50%
【注意】①被削材、加工形状に合わせて、適切なクーラントを使用してください。 【注意】①被削材、加工形状に合わせて、適切なクーラントを使用してください。
②できるだけ高剛性、高精度の機械をご使用ください。 ②できるだけ高剛性、高精度の機械をご使用ください。
③この切削条件表は切削条件の目安を示すものです。実際の加工では加工形状、目的、使用機械等により条件を調整してください。 ③この切削条件表は切削条件の目安を示すものです。実際の加工では加工形状、目的、使用機械等により条件を調整してください。
④機械の回転数が足りない場合は、回転数と送り速度を同じ比率で下げてください。 ④機械の回転数が足りない場合は、回転数と送り速度を同じ比率で下げてください。
【Note】① Use the appropriate coolant for the work material and machining shape. ⑤溝切削の場合、送り速度を50%を目安に調整してください。
② Use a highly rigid and accurate machine as possible. ⑥傾斜切削の場合、傾斜角は0.5°以下、送り速度を50%を目安に調整してください。
③ These Recommended Cutting Conditions indicate only the rule of a thumb for the cutting conditions. In actual machining, the condition should be adjusted according to 【Note】① Use the appropriate coolant for the work material and machining shape.
the machining shape, purpose and the machine type. ② Use a highly rigid and accurate machine as possible.
④ If the rpm available is lower than that recommended please reduce the feed rate to the same ratio. ③ These Recommended Cutting Conditions indicate only the rule of a thumb for the cutting conditions. In actual machining, the condition should be adjusted according to
the machining shape, purpose and the machine type.
④ If the rpm available is lower than that recommended please reduce the feed rate to the same ratio.
⑤ For slotting, adjust the feed rate to 50% as general criteria.
⑥ For ramping, adjust the ramp angle to 0.5° or less and the feed rate to 50% as general criteria.
08 09
Page10
加工事例
Field data
ダイカスト型入れ子モデルの立壁仕上げ加工 プラスチック金型 ブッシュ穴仕上げ加工事例
Vertical wall finishing of a die-cast mold insert model Example for plastic molds and bushing hole finishing
被削材 Work material:SKD61(48HRC) 機械 Machine:立型MC(BT50)Vertical MC クーラント Coolant:エアーブロー Air blow 被削材 Work material:STAVAX(52HRC) 機械 Machine:立型MC(BT40)Vertical MC
突き出し量 Overhang:84mm(L/D=7) クーラント Coolant:油性切削液 Oil base coolant 突き出し量 Overhang:50mm(L/D=5)
使用工具 Tool:EPWB8120-80-10-ATH、従来4枚刃ロングシャンクエンドミル Conventional 4flutes long shank end mill (φ12(R1.0) -刃長 Flute length18mm) 使用工具 Tool:EPWB8100-50-ATH(φ10)、従来ロング刃長エンドミル Conventional long flute end mill 穴径 Hole dia.:42mm 深さ Depth:37mm
切削条件:n=930min-1(vc=35m/min) fz=0.037mm/t ap=6mm ae=0.05mm ワークサイズ Work size: 50×50×深さ depth 35mm 切削条件: EPWB8-ATH 従来6枚刃ロング刃長エンドミル Conventional 6-flutes long flute end mill
Cut ting EPWB8-ATH:vf=280mm/min 従来品 Conventional:vf=140mm/min Cutting
conditions n=1,592min-1(vc=50m/min) v f=318mm/min( fz=0.025mm/t) n=600min-1(vc=19m/min) v f=80mm/min( fz=0.022mm/t)
conditions ap =5mm ae =0.05mm ap =20mm ae =0.05mm
EPWB8-ATH 従来品 ※両工具ともに仕上げ加工は呼び径で加工 * Machined using finishing machining with nominal diameter for both tools
Conventional
測 断面曲線 測 断面曲線
定 Surface Profile 定 Surface Profile
方 方 【仕上げ加工時間の比較】Comparison of finishing time
向 向
仕上げ 仕上げ 仕上げ加工 Finishing
加工範囲 加工範囲
Finishing Finishing 測定 Measurement
area area EPWB8-ATH 17min 仕上げ加工時間70%削減 再加工(ゼロカットと補正)
Finishing time reduced by 70% Reworking
ワーク外観 (zero cut / dimensional adjustment)
Work appearance
従来6枚刃ロング刃長
エンドミル
Conventional 6-flutes long flute end mill 58min
Zピック方向表面粗さ Ra0.255μm Zピック方向表面粗さ Ra0.928μm
Surface roughness in stepdown direction Surface roughness in stepdown direction
光沢のある加工面 段差のある白濁した加工面 0 10 20 30 40 50 60 70
Shiny machined surface Cloudy machined surface with visible steps
時間 Time (min)
倒れ量
Deflection 3μm 10μm
EPWB8-ATHは能率2倍で従来品に対して良好な加工精度と加工面を実現 EPWB8-ATH ・ロング刃長エンドミルは倒れ量と寸法調整でトータル6回の
EPWB8-ATH allows good machining accuracy and machining surface with double the efficiency for conventional tools. ゼロカットや補正が必要
・Long-flute end mill requires total of 6 zero cuts and corrections for deflection and dimensional
adjustment.
構造部のポケット立壁仕上げ加工 ・EPWB8-ATHはゼロカット無しで倒れ量3μm以下を達成
Vertical wall finishing of a pocket in a structural section 最終1回の寸法調整のみで完成
・EPWB8-ATH achieves deflection of less than 3 μm, even without zero cutting.
被削材 Work material:S50C 機械 Machine:立型MC(BT40)Vertical MC Completed with just one final dimensional adjustment.
クーラント Coolant:水溶性切削液 Water base coolant 突き出し量 Overhang:50mm(L/D=5) EPWB8-ATH
使用工具 Tool:EPWB8100-50-ATH(φ10)、
従来4枚刃ロング刃長エンドミル Conventional 4flutes long flute end mill (φ10-刃長50mm)
ポケットサイズ Pocket size:50×50×50mm(隅R6 Corner R6) Flute length
ポケット幅公差 Pocket width tolerance:±0.005mm
※両工具ともに実径で加工 Zピック方向表面粗さ Ra:0.216μm Rz:0.924μm
* Machined using actual diameter for both tools
Surface roughness in stepdown direction
従来ロング刃長エンドミル
EPWB8-ATH 4枚刃 (φ10刃長50mm) 5mm 加工能率同等で修正工数を大幅低減 ⇒ 加工費84%削減
Conventional long flute end mill Significantly reduces correction steps while maintaining the same machining efficiency. ⇒ Machining cost reduced by 84%
4-flutes (φ10, flute length 50mm) ピック方向表面粗さRa0.117μm
回転数 n(min-1) Surface roughness in stepdown direction
Revolution 3980 1500
切削速度 vc(m/min)
Cutting speed 125 47 従来品 Conventional
送り速度 vf(mm/min)
Feed rate 800 200
1刃送り量 fz(mm/t)
Feed per tooth 0.025 0.033
Zピック ap(mm)
Stepdown 5 20
取り代 ae(mm)
Machining allowance 0.05
倒れ量 5mm
Deflection 2μm 10μm
修正回数 ピック方向表面粗さRa0.592μm
Number of corrections 0回 times 2回 times Surface roughness in stepdown direction
トータル仕上加工時間 2分39秒 6分39秒
Total finishing time 図 ポケット加工外観と加工面粗さ
2 min. 39 sec. 6 min. 39 sec. Pocket appearance and machined surface roughness
修正なしで削り残り量5μm以下を達成
Achieves a remaining stock of 5 μm or less without correction.
10 11
Measurement
direction
Measurement
direction
10.0
5.0
0.0
-5.0
-10.0
0㎜ 10.0 20.0 30.0
10.0
5.0
0.0
-5.0
-10.0
0㎜ 10.0 20.0 30.0
Page11
加工事例
Field data
ダイカスト型入れ子モデルの立壁仕上げ加工 プラスチック金型 ブッシュ穴仕上げ加工事例
Vertical wall finishing of a die-cast mold insert model Example for plastic molds and bushing hole finishing
被削材 Work material:SKD61(48HRC) 機械 Machine:立型MC(BT50)Vertical MC クーラント Coolant:エアーブロー Air blow 被削材 Work material:STAVAX(52HRC) 機械 Machine:立型MC(BT40)Vertical MC
突き出し量 Overhang:84mm(L/D=7) クーラント Coolant:油性切削液 Oil base coolant 突き出し量 Overhang:50mm(L/D=5)
使用工具 Tool:EPWB8120-80-10-ATH、従来4枚刃ロングシャンクエンドミル Conventional 4flutes long shank end mill (φ12(R1.0) -刃長 Flute length18mm) 使用工具 Tool:EPWB8100-50-ATH(φ10)、従来ロング刃長エンドミル Conventional long flute end mill 穴径 Hole dia.:42mm 深さ Depth:37mm
切削条件:n=930min-1(vc=35m/min) fz=0.037mm/t ap=6mm ae=0.05mm ワークサイズ Work size: 50×50×深さ depth 35mm 切削条件: EPWB8-ATH 従来6枚刃ロング刃長エンドミル Conventional 6-flutes long flute end mill
Cut ting EPWB8-ATH:vf=280mm/min 従来品 Conventional:vf=140mm/min Cutting
conditions n=1,592min-1(vc=50m/min) v f=318mm/min( fz=0.025mm/t) n=600min-1(vc=19m/min) v f=80mm/min( fz=0.022mm/t)
conditions ap =5mm ae =0.05mm ap =20mm ae =0.05mm
EPWB8-ATH 従来品 ※両工具ともに仕上げ加工は呼び径で加工 * Machined using finishing machining with nominal diameter for both tools
Conventional
測 断面曲線 測 断面曲線
定 Surface Profile 定 Surface Profile
方 方 【仕上げ加工時間の比較】Comparison of finishing time
向 向
仕上げ 仕上げ 仕上げ加工 Finishing
加工範囲 加工範囲
Finishing Finishing 測定 Measurement
area area EPWB8-ATH 17min 仕上げ加工時間70%削減 再加工(ゼロカットと補正)
Finishing time reduced by 70% Reworking
ワーク外観 (zero cut / dimensional adjustment)
Work appearance
従来6枚刃ロング刃長
エンドミル
Conventional 6-flutes long flute end mill 58min
Zピック方向表面粗さ Ra0.255μm Zピック方向表面粗さ Ra0.928μm
Surface roughness in stepdown direction Surface roughness in stepdown direction
光沢のある加工面 段差のある白濁した加工面 0 10 20 30 40 50 60 70
Shiny machined surface Cloudy machined surface with visible steps
時間 Time (min)
倒れ量
Deflection 3μm 10μm
EPWB8-ATHは能率2倍で従来品に対して良好な加工精度と加工面を実現 EPWB8-ATH ・ロング刃長エンドミルは倒れ量と寸法調整でトータル6回の
EPWB8-ATH allows good machining accuracy and machining surface with double the efficiency for conventional tools. ゼロカットや補正が必要
・Long-flute end mill requires total of 6 zero cuts and corrections for deflection and dimensional
adjustment.
構造部のポケット立壁仕上げ加工 ・EPWB8-ATHはゼロカット無しで倒れ量3μm以下を達成
Vertical wall finishing of a pocket in a structural section 最終1回の寸法調整のみで完成
・EPWB8-ATH achieves deflection of less than 3 μm, even without zero cutting.
被削材 Work material:S50C 機械 Machine:立型MC(BT40)Vertical MC Completed with just one final dimensional adjustment.
クーラント Coolant:水溶性切削液 Water base coolant 突き出し量 Overhang:50mm(L/D=5) EPWB8-ATH
使用工具 Tool:EPWB8100-50-ATH(φ10)、
従来4枚刃ロング刃長エンドミル Conventional 4flutes long flute end mill (φ10-刃長50mm)
ポケットサイズ Pocket size:50×50×50mm(隅R6 Corner R6) Flute length
ポケット幅公差 Pocket width tolerance:±0.005mm
※両工具ともに実径で加工 Zピック方向表面粗さ Ra:0.216μm Rz:0.924μm
* Machined using actual diameter for both tools
Surface roughness in stepdown direction
従来ロング刃長エンドミル
EPWB8-ATH 4枚刃 (φ10刃長50mm) 5mm 加工能率同等で修正工数を大幅低減 ⇒ 加工費84%削減
Conventional long flute end mill Significantly reduces correction steps while maintaining the same machining efficiency. ⇒ Machining cost reduced by 84%
4-flutes (φ10, flute length 50mm) ピック方向表面粗さRa0.117μm
回転数 n(min-1) Surface roughness in stepdown direction
Revolution 3980 1500
切削速度 vc(m/min)
Cutting speed 125 47 従来品 Conventional
送り速度 vf(mm/min)
Feed rate 800 200
1刃送り量 fz(mm/t)
Feed per tooth 0.025 0.033
Zピック ap(mm)
Stepdown 5 20
取り代 ae(mm)
Machining allowance 0.05
倒れ量 5mm
Deflection 2μm 10μm
修正回数 ピック方向表面粗さRa0.592μm
Number of corrections 0回 times 2回 times Surface roughness in stepdown direction
トータル仕上加工時間 2分39秒 6分39秒
Total finishing time 図 ポケット加工外観と加工面粗さ
2 min. 39 sec. 6 min. 39 sec. Pocket appearance and machined surface roughness
修正なしで削り残り量5μm以下を達成
Achieves a remaining stock of 5 μm or less without correction.
10 11
Measurement
direction
Measurement
direction
10.0
5.0
0.0
-5.0
-10.0
0㎜ 10.0 20.0 30.0
10.0
5.0
0.0
-5.0
-10.0
0㎜ 10.0 20.0 30.0
Page12
NEW
立壁/底面仕上げ用8枚刃エンドミル
8-flutes End Mill for Vertical Wall/Bottom Face Finishing
EPWB8-ATH
コーナRサイズを充実させ
図、表等のデータは試験結果の一例であり、保証値ではありません。 8枚刃エンドミルがリニューアル
「 」は株式会社MOLDINOの登録商標です。
The diagrams and table data are examples of test results, and are not guaranteed values. Enhanced 8-flutes end mill with expanded
“ ” is a registered trademark of MOLDINO Tool Engineering, Ltd. corner radius options
安 全 上 の ご 注 意 Attentions on Safety
1. 取扱上のご注意 1. Cautions regarding handling
(1)工具をケース(梱包)から取り出す際は、工具の飛び出し、落下にご注意ください。特に工具刃部との接 (1) When removing the tool from its case (packaging), be careful that the tool does not pop out or is
触には十分ご注意をお願いします。 dropped. Be particularly careful regarding contact with the tool flutes.
(2)鋭利な切れ刃を有する工具を取扱う際は、切れ刃を素手で直接触れないように注意してください。 (2) When handling tools with sharp cutting flutes, be careful not to touch the cutting flutes directly with
2. 取付け時のご注意 your bare hands.
(1)ご使用前に、工具の傷・割れ等の外観確認を行っていただき、コレットチャック等への取付けは確実に 2. Cautions regarding mounting
行ってください。 (1) Before use, check the outside appearance of the tool for scratches, cracks, etc. and that it is firmly
(2)ご使用中に、異常な振動等が発生した場合は、直ちに機械を停止させて、その振動の原因を取り除い mounted in the collet chuck, etc.
てください。 (2) If abnormal chattering, etc. occurs during use, stop the machine immediately and remove the cause
3. 使用上のご注意 of the chattering.
(1)切削工具あるいは被削材の寸法・回転の方向は、あらかじめ確認しておいてください。 3. Cautions during use
(2)標準切削条件表の数値は、新しい作業の立上げの目安としてご利用ください。切込みが大きい場合、 (1) Before use, confirm the dimensions and direction of rotation of the tool and milling work material.
使用機械の剛性が小さい場合あるいは被加工物の性状に応じて切削条件を適正に調整してご使用 (2) The numerical values in the standard cutting conditions table should be used as criteria when starting
ください。 new work. The cutting conditions should be adjusted as appropriate when the cutting depth is large,
(3)切削工具材料は硬質の材料です。ご使用中に破損して飛散する場合があります。また、切りくずが飛 the rigidity of the machine being used is low, or according to the conditions of the work material.
散することがあります。これらの飛散物等は作業者を切傷させ、火傷あるいは目に入って負傷させる恐 (3) Cutting tools are made of a hard material. During use, they may break and fly off. In addition, cutting
れがありますので、工具をご使用中はその周囲に安全カバーを取付け、保護めがね等の保護具を着用 chips may also fly off. Since there is a danger of injury to workers, fire, or eye damage from such
して安全な環境下での作業をお願いいたします。 flying pieces, a safety cover should be attached when work is performed and safety equipment such
(4)切削中に発生する火花や、破損による発熱や、切りくずによる引火・火災の危険があります。引火や as safety goggles should be worn to create a safe environment for work.
爆発の危険のあるところでは使用しないでください。不水溶性切削液をご使用される場合は防火対 (4) There is a risk of fire or inflammation due to sparks, heat due to breakage, and cutting chips. Do not
策を必ず行なってください。 use where there is a risk of fire or explosion. Please caution of fire while using oil base coolant, fire
(5)工具を本来の目的以外にはご使用にならないでください。 prevention is necessary.
4. 再研削時のご注意 (5) Do not use the tool for any purpose other than that for which it is intended.
(1)再研削時期が不適当であると工具が破損する恐れがあります。適正な工具と交換するか、再研削を 4. Cautions regarding regrinding
行ってください。
(2)工具を再研削しますと粉塵が発生します。再研削時にはその周囲に安全カバーを取付け、保護め (1) If regrinding is not performed at the proper time, there is a risk of the tool breaking. Replace the tool
がね等の保護具を着用してください。 with one in good condition, or perform regrinding.
(3)本製品には特定化学物質に指定された コバルト及びその無機化合物が含まれています。再研削等の (2) Grinding dust will be created when regrinding a tool. When regrinding, be sure to attach a safety
加工を加える場合は特定化学物質障害予防規則(特化則)に従った取扱いをしてください。 cover over the work area and wear safety clothes such as safety goggles, etc.
(3) This product contains the specified chemical substance cobalt and its inorganic compounds. When
5. 工具に関して、安全上の問題点・不明の点・その他相談がありましたら フ リ ーダ イ ヤ ル 技 術 相 談 へ performing regrinding or similar processing, be sure to handle the processing in accordance with
ご相談ください。 thelocal laws and regulations regarding prevention of hazards due to specified chemical substances.
ホームページ フリーダイヤル技術相談
https://www.moldino.com
MOLDINO Tool Engineering, Ltd.
本社 〒130-0026 東京都墨田区両国4-31-11(ヒューリック両国ビル8階) 工具選定データベース【 TOOLSEARCH】
03-6890-5101 FAX 03-6890-5134
International Sales Dept .: +81-3-6890-5103 FAX +81-3-6890-5128
営業企画部 ☎03-6890-5102 FAX03-6890-5134 海外営業部 ☎03-6890-5103 FAX03-6890-5128
東京営業所 ☎03-6890-5110 FAX03-6890-5133 静岡営業所 ☎054-273-0360 FAX054-273-0361
東北営業所 ☎022-208-5100 FAX022-208-5102 名古屋営業所 ☎052-687-9150 FAX052-687-9144
新潟営業所 ☎0258-87-1224 FAX0258-87-1158 大阪営業所 ☎06-7668-0190 FAX06-7668-0194
東関東営業所 ☎0294-88-9430 FAX0294-88-9432 中四営業所 ☎082-536-2001 FAX082-536-2003
長野営業所 ☎0276-59-6001 FAX0276-59-6005 九州営業所 ☎092-289-7010 FAX092-289-7012
北関東営業所 ☎0276-59-6001 FAX0276-59-6005
神奈川営業所 ☎046-400-9429 FAX046-400-9435
ヨーロッパ/MOLDINO Tool Engineering Europe GmbH Itterpark 12, 40724 Hilden, Germany. TEL : +49-(0)2103-24820, FAX : +49-(0)2103-248230
アメリカ/MITSUBISHI MATERIALS U.S.A. CORPORATION Detroit office c/o RFM Inc. Customer service 2001 Orndorf Drive, Brighton, MI 48116 U.S.A. TEL : +1(248)308-2620, FAX :+1(248)308-2627
メキシコ/MITSUBISHI MATERIALS MÉXICO S.A. DE C.V. Av. La Cañada No.16, Parque Industrial Bernardo Quintana, El Marques, Querétaro, CP 76246, México TEL : +52-442-1926800 MOLDINO Tool Engineering, Ltd.
ブラジル/MITSUBISHI MATERIALS BRASIL LTDA. Rua Cincinato Braga, 340 13° andar.Bela Vista – CEP 01333-010 São Paulo – SP ., Brasil TEL : +55(11)3506-5600 FAX : +55(11)3506-5677
タ イ/MITSUBISHI MATERIALS (THAILAND) CO., LTD. 139/3 Moo 2, Tambon Khlong Chik, Amphoe Bang Pa-in, Phra Nakhon Si Ayutthaya 13160, Thailand TEL:+66-3525-8024
イ ン ド/Mitsubishi Materials India Private Limited H.O.: Prasad Enclave, #118/119, 1st Floor, 2nd Stage, 5th main, BBMP Ward #11, (New #38), Industrial Suburb, Yeshwanthpura, Bengaluru, 560 022, Karnataka, India. Tel : +91-80-2204-3600 New Produc t News No.2602 2026-10
予告なく、改良・改善のために仕様変更することがあります。
Specifications for the products listed in this catalog are subject to change without notice due to ベジタブルインクで印刷しています。 2026-10(K)HT4
replacement or modification. Printed using vegetable oil ink. Printed in JAPAN 2026-10:FP