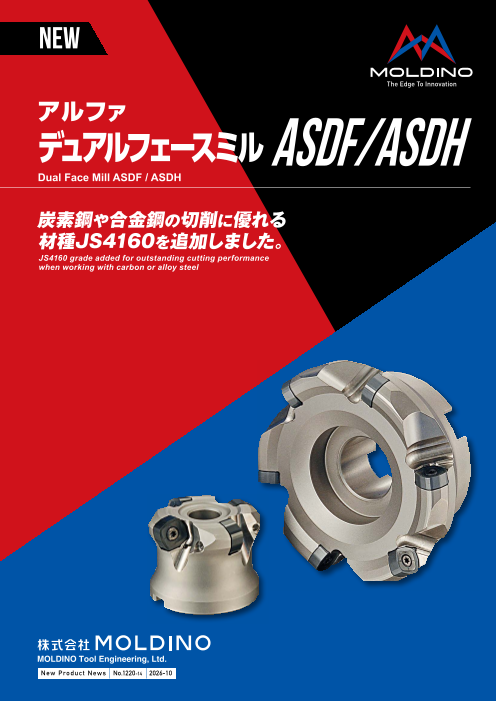


炭素鋼や合金鋼の切削に優れる材種JS4160を追加しました。
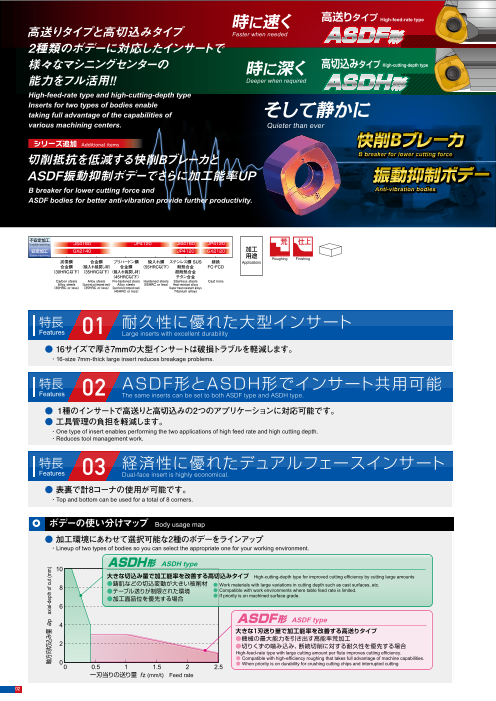
高送りタイプと高切込みタイプ2種類のボデーに対応したインサートで 様々なマシニングセンターの能力をフル活用!!
◆耐久性に優れた大型インサート
◆ASDF形とASDH形でインサート共用可能
◆経済性に優れたデュアルフェースインサート
◆詳細はカタログをダウンロードしご覧いただくか、お気軽にお問い合わせ下さい。
このカタログについて
| ドキュメント名 | アルファ デュアルフェースミル ASDF/ASDH |
|---|---|
| ドキュメント種別 | 製品カタログ |
| ファイルサイズ | 2.7Mb |
| 登録カテゴリ | |
| 取り扱い企業 | 株式会社MOLDINO (この企業の取り扱いカタログ一覧) |
この企業の関連カタログ


このカタログの内容
Page1
NEW
アルファ
デュアルフェースミルASDF/ASDH
Dual Face Mill ASDF / ASDH
炭素鋼や合金鋼の切削に優れる
材種JS4160を追加しました。
JS4160 grade added for outstanding cutting performance
when working with carbon or alloy steel
MOLDINO Tool Engineering, Ltd.
New Produc t News No.1220-14 2026-10
Page2
時に速く 高送りタイプ High-feed-rate type
高送りタイプと高切込みタイプ Faster when needed ASDF形 ラインナップ
2種類のボデーに対応したインサートで Line Up
様々なマシニングセンターの 時に深く 高切込みタイプ High-cutting-depth type 快削Bブレーカ B breaker for lower cutting force 振動抑制ボデー Anti-vibration body ASDF5 R(M)- U
能力をフル活用! Deeper when required ASDH形 快削Bブレーカ追加による切削抵抗低減 不等分割ピッチによるビビリ振動対策
High-feed-rate type and high-cutting-depth type B breaker for lower cutting force is now available. Anti-vibration bodies by unequal pitch.
Inserts for two types of bodies enable ● 切れ刃形状をポジティブ設定にすることで、切削抵 ● インサートを不等分割ピッチで配列することによ
taking full advantage of the capabilities of そして静かに 抗を従来形状に比べ10%低減。 り、ビビリ振動の主要因である自励振動を抑制。
various machining centers. Quieter than ever ● 切削抵抗低減により、剛性が低い加工環境下にお ● 従来品に比べ、ビビリ振動を抑制することで、切込み限界を
いても、良好な切削を実現。 改善する事が可能。
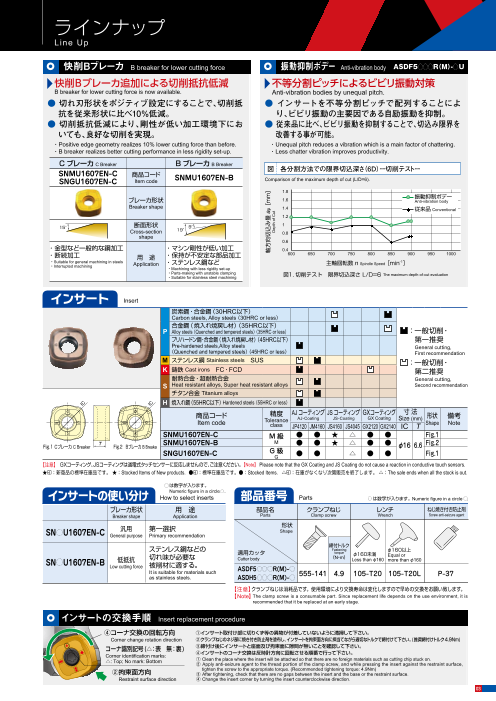
シリーズ追加 Additional items 快削Bブレーカ ・Positive edge geometry realizes 10% lower cutting force than before. ・Unequal pitch reduces a vibration which is a main factor of chattering.
・B breaker realizes better cutting performance in less rigidity set-up. ・Less chatter vibration improves productivity.
切削抵抗を低減する快削Bブレーカと Cブレーカ C Breaker Bブレーカ B Breaker
ASDF振動抑制ボデーでさらに加工能率UP 振動抑制ボデー SNMU1607EN-C 図 各分割方法での限界切込深さ(6D)ー切削テストー
商品コード
SNGU1607EN-C Item code SNMU1607EN-B Comparison of the maximum depth of cut (L/D=6).
B breaker for lower cutting force and 1.8
ASDF bodies for better anti-vibration provide further productivity. ブレーカ形状 1.6 振動抑制ボデー
Anti-vibration body
Breaker shape 1.4 従来品 Conventional
1.2
15° 断面形状 9° 1
Cross-section 19°
0.8
shape
不安定加工 0.6
Unstable machining JS4160 JP4120 JM4160 JP4120 荒 仕上
安定加工 GX2140 JP4120 GX2120 加工 ・金型など一般的な鋼加工 ・マシン剛性が低い加工 0.4
Stable machining 用途 Roughing Finishing ・断続加工 600 650 700 750 800 850 900 950 1000
用 途 ・保持が不安定な部品加工
炭素鋼 合金鋼 プリハードン鋼 焼入れ鋼 ステンレス鋼 SUS 鋳鉄 Applications ・Suitable for general machining in steels
合金鋼 (焼入れ焼戻し材) 合金鋼 (55HRC以下) 耐熱合金 FC・FCD ・Interrupted machining Application ・ステンレス鋼など 主軸回転数 n Spindle Speed[ min-1]
・Machining with less rigidity set-up
(30HRC以下)(35HRC以下)(焼入れ焼戻し材) 超耐熱合金 ・Parts-making with unstable clamping
(45HRC以下) チタン合金 imum depth-of-cut evaluation
・Suitable for stainless steel machining 図1. 切削テスト 限界切込深さ L/D=6 The max
Carbon steels Alloy steels Pre-hardened steels Hardened steels Stainless steels Cast irons
Alloy steels (Quenched and tempered steels) Alloy steels (55HRC or less) Heat resistant alloys
(30HRC or less) (35HRC or less)(Quenched and tempered steels) Super heat resistant alloys
(45HRC or less) Titanium alloys
特長 耐久性に優れた大型インサート
Features 01 Large inserts with excellent durability
● 16サイズで厚さ7mmの大型インサートは破損トラブルを軽減します。
・16-size 7mm-thick large insert reduces breakage problems.
特長 DF形とASDH形でインサート共用可能
Features 02 AS
The same inserts can be set to both ASDF type and ASDH type.
● 1種のインサートで高送りと高切込みの2つのアプリケーションに対応可能です。
● 工具管理の負担を軽減します。
・One type of insert enables performing the two applications of high feed rate and high cutting depth.
・Reduces tool management work.
特長 性に優れたデュアルフェースインサート
Features 03 経済
Dual-face insert is highly economical.
● 表裏で計8コーナの使用が可能です。
・Top and bottom can be used for a total of 8 corners.
ボデーの使い分けマップ Body usage map
● 加工環境にあわせて選択可能な2種のボデーをラインアップ
・Lineup of two types of bodies so you can select the appropriate one for your working environment.
ASDH 形 ASDH type
10
大きな切込み量で加工能率を改善する高切込みタイプ High-cutting-depth type for improved cutting efficiency by cutting large amounts
●鋳肌などの切込変動が大きい被削材
8 ● Work materials with large variations in cutting depth such as cast surfaces, etc.
●テーブル送りが制限された環境 ● Compatible with work environments where table feed rate is limited.
●加工面品位を優先する場合 ● If priority is on machined surface grade.
6
ASDF 形 ASDF type インサートの交換手順 Insert replacement procedure
4
大きな1刃送り量で加工能率を改善する高送りタイプ ④コーナ交換の回転方向 ①インサート取付け部に切りくず等の異物が付着していないように清掃して下さい。
●機械の最大能力を引き出す高能率荒加工 rotation direction
2 Corner change ②クランプねじのネジ部に焼き付き防止剤を塗布し、インサートを拘束面方向に押当てながら適切なトルクで締付けて下さい。(推奨締付けトルク4.9Nm)
●切りくずの噛み込み、断続切削に対する耐久性を優先する場合 コーナ識別記号(△:表 無:裏) ③締付け後にインサートと座面及び拘束面に隙間が無いことを確認して下さい。
High-feed-rate type with large cutting amount per flute improves cutting efficiency. Corner identification marks: ④インサートのコーナ交換は反時計方向に回転させる順番で行って下さい。
● Compatible with high-efficiency roughing that takes full advantage of machine capabilities.
0 △: Top; No mark: Bottom ① Clean the place where the insert will be attached so that there are no foreign materials such as cutting chip stuck on.
0 0.5 1 1.5 2 2.5 ● When priority is on durability for crushing cutting chips and interrupted cutting ② Apply anti-seizure agent to the thread portion of the clamp screw, and while pressing the insert against the restraint surface,
②拘束面方向 tighten the screw to the appropriate torque. (Recommended tightening torque: 4.9Nm)
一刃当りの送り量 fz (mm/t) Feed rate ③ After tightening, check that there are no gaps between the insert and the base or the restraint surface.
Restraint surface direction ④ Change the insert corner by turning the insert counterclockwise direction.
02
軸方向切込み量 ap axial-depth of cut (mm)
軸方向切込み量 ap[ mm]
Depth of Cut
Page3
時に速く 高送りタイプ High-feed-rate type
高送りタイプと高切込みタイプ Faster when needed ASDF形 ラインナップ
2種類のボデーに対応したインサートで Line Up
様々なマシニングセンターの 時に深く 高切込みタイプ High-cutting-depth type 快削Bブレーカ B breaker for lower cutting force 振動抑制ボデー Anti-vibration body ASDF5 R(M)- U
能力をフル活用! Deeper when required ASDH形 快削Bブレーカ追加による切削抵抗低減 不等分割ピッチによるビビリ振動対策
High-feed-rate type and high-cutting-depth type B breaker for lower cutting force is now available. Anti-vibration bodies by unequal pitch.
Inserts for two types of bodies enable ● 切れ刃形状をポジティブ設定にすることで、切削抵 ● インサートを不等分割ピッチで配列することによ
taking full advantage of the capabilities of そして静かに 抗を従来形状に比べ10%低減。 り、ビビリ振動の主要因である自励振動を抑制。
various machining centers. Quieter than ever ● 切削抵抗低減により、剛性が低い加工環境下にお ● 従来品に比べ、ビビリ振動を抑制することで、切込み限界を
いても、良好な切削を実現。 改善する事が可能。
シリーズ追加 Additional items 快削Bブレーカ ・Positive edge geometry realizes 10% lower cutting force than before. ・Unequal pitch reduces a vibration which is a main factor of chattering.
・B breaker realizes better cutting performance in less rigidity set-up. ・Less chatter vibration improves productivity.
切削抵抗を低減する快削Bブレーカと Cブレーカ C Breaker Bブレーカ B Breaker
ASDF振動抑制ボデーでさらに加工能率UP 振動抑制ボデー SNMU1607EN-C 図 各分割方法での限界切込深さ(6D)ー切削テストー
商品コード
SNGU1607EN-C Item code SNMU1607EN-B Comparison of the maximum depth of cut (L/D=6).
B breaker for lower cutting force and 1.8
ASDF bodies for better anti-vibration provide further productivity. ブレーカ形状 1.6 振動抑制ボデー
Anti-vibration body
Breaker shape 1.4 従来品 Conventional
1.2
15° 断面形状 9° 1
Cross-section 19°
0.8
shape
不安定加工 0.6
Unstable machining JS4160 JP4120 JM4160 JP4120 荒 仕上
安定加工 GX2140 JP4120 GX2120 加工 ・金型など一般的な鋼加工 ・マシン剛性が低い加工 0.4
Stable machining 用途 Roughing Finishing ・断続加工 な部品加工 600 650 700 750 800 850 900 950 1000
用 途 ・保持が不安定
炭素鋼 合金鋼 プリハードン鋼 焼入れ鋼 ステンレス鋼 SUS 鋳鉄 Applications ・Suitable for general machining in steels
合金鋼 (焼入れ焼戻し材) 合金鋼 (55HRC以下) 耐熱合金 FC・FCD ・Interrupted machining Application ・ステンレス鋼など 主軸回転数 n Spindle Speed[ min-1]
・Machining with less rigidity set-up
(30HRC以下)(35HRC以下)(焼入れ焼戻し材) 超耐熱合金 ・Parts-making with unstable clamping
(45HRC以下) チタン合金 図1. 切削テスト 限界切込深さ L/D=6 The maximum depth-of-cut evaluation
・Suitable for stainless steel machining
Carbon steels Alloy steels Pre-hardened steels Hardened steels Stainless steels Cast irons
Alloy steels (Quenched and tempered steels) Alloy steels (55HRC or less) Heat resistant alloys
(30HRC or less) (35HRC or less)(Quenched and tempered steels) Super heat resistant alloys
(45HRC or less) Titanium alloys
インサート Insert
炭素鋼・合金鋼(30HRC以下)
特長 耐久性に優れた大型インサート Carbon steels, Alloy steels(30HRC or less)
合金鋼(焼入れ焼戻し材)(35HRC以下)
Features 01 Large inserts with excellent durability P Alloy steels(Quenched and tempered steels)(35HRC or less) :一般切削・
プリハードン鋼・合金鋼(焼入れ焼戻し材)(45HRC以下) 第一推奨
● 16サイズで厚さ7mmの大型インサートは破損トラブルを軽減します。 Pre-hardened steels,Alloy steels General cutting,
(Quenched and tempered steels)(45HRC or less) First recommendation
・16-size 7mm-thick large insert reduces breakage problems. M ステンレス鋼 Stainless steels SUS :一般切削・
K 鋳鉄 Cast irons FC・FCD 第二推奨
特長 耐熱合金・超耐熱合金 General cutting,
S Heat resistant alloys, Super heat resistant alloys Second recommendation
Features 02 ASDF形とASDH形でインサート共用可能
The same inserts can be set to both ASDF type and ASDH type. チタン合金 Titanium alloys
IC IC H 焼入れ鋼(55HRC以下) Hardened steels(55HRC or less)
● 1種のインサートで高送りと高切込みの2つのアプリケーションに対応可能です。 商品コード 精度 AJコーティング JSコーティング GXコーティング 寸 法
● 工具管理の負担を軽減します。 ating JS-Coating GX Coating Size (mm) 形状 備考
Item code Tolerance AJ-Co
class JP4120 JM4160 JS4160 JS4045 GX2120 GX2140 IC T Shape Note
・One type of insert enables performing the two applications of high feed rate and high cutting depth.
・Reduces tool management work. SNMU1607EN-C M 級 ● ● ★ △ ● ● Fig.1
M
Fig.1 Cブレーカ T ブレーカ SNMU1607EN-B ● ● ★ △ ● ●
C Breaker Fig.2 B B Breaker φ16 6.6 Fig.2
SNGU1607EN-C G 級
G ● ● △ ● ● Fig.1
特長 たデュアルフェースインサート 【注意】 GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんので、ご注意ください。【Note】 Please note that the GX Coating and JS Coating do not cause a reaction in conductive touch sensors.
Features 03 経済性に優れ
Dual-face insert is highly economical. ★印:新商品の標準在庫品です。 ★:Stocked Items of New products. ●印:標準在庫品です。●:Stocked Items. △印:在庫がなくなり次第販売を終了します。 △:The sale ends when all the stock is out.
● 表裏で計8コーナの使用が可能です。 は数字が入ります。
・Top and bottom can be used for a total of 8 corners. インサートの使い分け Numeric figure in a circle .
How to select inserts 部品番号 Parts は数字が入ります。 Numeric figure in a circle .
ブレーカ形状 用 途 部品名 クランプねじ レンチ ねじ焼き付き防止剤
Breaker shape Application Parts Clamp screw Wrench Screw anti-seizure agent
ボデーの使い分けマップ Body usage map 形状
SN U1607EN-C 汎用 第一選択 Shape
● 加工環境にあわせて選択可能な2種のボデーをラインアップ General purpose Primary recommendation
・Lineup of two types of bodies so you can select the appropriate one for your working environment. ステンレス鋼などの 締付トルク
適用カッタ Fastening
torque φ160以上
ASDH 形 切れ味が必要な (N・m) φ160未満 Equal or
ASDH type SN U1607EN-B 低抵抗 Cutter body Less than φ160 more than φ160
10 Low cutting force 被削材に適する。
大きな切込み量で加工能率を改善する高切込みタイプ It is suitable for materials such ASDF5 R(M)-
High-cutting-depth type for improved cutting efficiency by cutting large amounts as stainless steels. ASDH5 R(M)- 555-141 4.9 105-T20 105-T20L P-37
●鋳肌などの切込変動が大きい被削材
8 ● Work materials with large variations in cutting depth such as cast surfaces, etc.
●テーブル送りが制限された環境 ● Compatible with work environments where table feed rate is limited. 【注意】 クランプねじは消耗品です。使用環境により交換寿命は変化しますので早めの交換をお願い致します。
●加工面品位を優先する場合 ● If priority is on machined surface grade. 【Note】 The clamp screw is a consumable part. Since replacement life depends on the use environment, it is
recommended that it be replaced at an early stage.
6
ASDF 形 ASDF type インサートの交換手順 Insert replacement procedure
4
大きな1刃送り量で加工能率を改善する高送りタイプ ④コーナ交換の回転方向 ①インサート取付け部に切りくず等の異物が付着していないように清掃して下さい。
●機械の最大能力を引き出す高能率荒加工 Corner change rotation direction ②クランプねじのネジ部に焼き付き防止剤を塗布し、インサートを拘束面方向に押当てながら適切なトルクで締付けて下さい。(推奨締付けトルク4.9Nm)
2 ●切りくずの噛み込み、断続切削に対する耐久性を優先する場合 コーナ識別記号(△:表 無:裏) ③締付け後にインサートと座面及び拘束面に隙間が無いことを確認して下さい。
High-feed-rate type with large cutting amount per flute improves cutting efficiency. Corner identification marks: ④インサートのコーナ交換は反時計方向に回転させる順番で行って下さい。
● Compatible with high-efficiency roughing that takes full advantage of machine capabilities.
0 △: Top; No mark: Bottom ① Clean the place where the insert will be attached so that there are no foreign materials such as cutting chip stuck on.
0 0.5 1 1.5 2 2.5 ● When priority is on durability for crushing cutting chips and interrupted cutting ② Apply anti-seizure agent to the thread portion of the clamp screw, and while pressing the insert against the restraint surface,
②拘束面方向 tighten the screw to the appropriate torque. (Recommended tightening torque: 4.9Nm)
一刃当りの送り量 fz (mm/t) Feed rate ③ After tightening, check that there are no gaps between the insert and the base or the restraint surface.
Restraint surface direction ④ Change the insert corner by turning the insert counterclockwise direction.
03
軸方向切込み量 ap axial-depth of cut (mm)
軸方向切込み量 ap[ mm]
Depth of Cut
Page4
ASDF ASDF type
ラインナ形ッ【プ高送りタイプ】 ラインナップ 標準切削条件表
Line Up 【 High-feed-rate type】 Line Up Recommended Cut t ing Condi t ions
※赤字は第一推奨材種です。
ASDF5 (R M)-(U) ASDF形 ASDF type【高送りタイプ】 High-feed-rate type Red indicates primary recommended grade.
は数字が入ります。 Numeric figure in a circle .
φ20
Fig.1(エアー穴付き)(With air hole) Fig.2(エアー穴無し)(Without air hole) Fig.3(エアー穴無し)(Without air hole)
DHUB DHUB DHUB
DCONMS DCONMS DCONMS
KWW KWW KWW
b b b
CBDP CBDP CBDP
LF LF LF
APMX APMX APMX
DCCB DCCB DCCB
DC DC DC
DCX DCX DCX
寸 法 Size (mm) Y-100 ラインナップ
商品コード 在庫 刃数 工具径 キー幅 適用
Tool dia. Line Up
DHUB LF CB インサート 備考
Item code Stock No.of Key width
DP DCONMS DCCB APMX 形状 重量
Figure Weight
flutes Inserts Note
DC DCX KWW b (kg)
ASDF5063R-4 ● 4 42 63 60 50 19 8.4 5 22.225 17 3 Fig.1 0.7
ASDF5063R-4U ● 4 42 63 60 50 19 8.4 5 22.225 17 3 Fig.1 0.7
ASDF5080R-4 ● 4 59 80 76 63 32 12.7 8 31.75 26 3 Fig.1 1.3
ASDF5080R-4U ● 4 59 80 76 63 32 12.7 8 31.75 26 3 Fig.1 1.3
ASDF5100R-5 ● 5 79 100 96 63 32 12.7 8 31.75 26 3 Fig.1 2.4
ASDF5100R-5U ● 5 79 100 96 63 32 12.7 8 31.75 26 3 Fig.1 2.4
ASDF5125R-6 ● 6 104 125 100 63 38 15.9 10 38.1 60 3 Fig.2 3.0
ASDF5125R-6U ● 6 104 125 100 63 38 15.9 10 38.1 60 3 Fig.2 3.0 【注意】①GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。 ae
②被削材、加工形状に合わせて、適切なクーラントを使用してください。
ASDF5125R-8U ● 8 104 125 100 63 38 15.9 10 38.1 60 3 Fig.2 3.0 ③この切削条件表は切削条件の目安を示すものです。実際の加工では、加工形状、目的、使用機械等により条件を調整してください。
④インサートの交換は早めに行い、過度の使用による破損を防止してください。
ASDF5160R-8 ● 8 139 160 105 63 38 19.1 11 50.8 80 3 Fig.3 4.3 ⑤排出した切りくずは、飛散し作業者を切傷させ、やけどあるいは目に入って負傷させる恐れがありますので、ご使用に際してはその周囲に安全カバーを ap
ASDF5160R-8U ● 8 139 160 105 63 38 19.1 11 50.8 80 3 Fig.3 4.3 取付け、保護メガネなどの保護具を着用し、安全な環境で作業されることをお願い致します。
ASDF5160R-10U ● 10 139 160 105 63 38 19.1 11 50.8 80 3 Fig.3 4.3 SNMU1607EN-C 【Note】①Please note that the GX Coating and JS Coating don't cause a
SNGU1607EN-C reaction in conductive touch sensors. ASDF形を形状加工で使用する場合 When using ASDF type for shaping cutting
ASDF5063RM-4 ● 4 42 63 60 50 20 10.4 6.3 22 17 3 Fig.1 0.7 SNMU1607EN-B ②Use the appropriate coolant for the work material and machining
shape. プログラム上の刃先形状定義は下記を参照ください。
ASDF5063RM-4U ● 4 42 63 60 50 20 10.4 6.3 22 17 3 Fig.1 0.7 ③These conditions are for general guidance; in actual machining Refer to the following for the flute tip condition definitions for programming.
ASDF5080RM-4 ● 4 59 80 76 63 22 12.4 7 27 20 3 Fig.1 1.5 conditions adjust the parameters according to your actual
machine and work-piece conditions. プログラミングR Programming R definition = R6
ASDF5080RM-4U ● 4 59 80 76 63 22 12.4 7 27 20 3 Fig.1 1.5 ④In order to avoid of insert breakage, please change insert earlier. 削り残し量 Remains 1.33mm
⑤The steel chips may cause cuts, burns or damages to eyes. Be
ASDF5100RM-5 ● 5 79 100 96 63 32 14.4 8 32 26 3 Fig.1 2.4 sure to install the safety cover around the tool and wear the ※傾斜加工はφ63,φ80で0.5°以下。φ100以上では行わないで下さい。
safety glasses when carrying out any works.
ASDF5100RM-5U ● 5 79 100 96 63 32 14.4 8 32 26 3 Fig.1 2.4 ※工具突出しが長い場合(L / D ≧ 3)はapを調整して下さい。
R6 ※For slanted cutting using ∅63 or ∅80, perform at 0.5° or less.
ASDF5125RM-6 ● 6 104 125 100 63 30 16.4 9 40 56 3 Fig.2 3.0 Do not perform using ∅100 or larger.
削り残し量 Remains 1.33mm ※When tool overhang length is long (L / D ≧ 3), adjust ap .
ASDF5125RM-6U ● 6 104 125 100 63 30 16.4 9 40 56 3 Fig.2 3.0
ASDF5125RM-8U ● 8 104 125 100 63 30 16.4 9 40 56 3 Fig.2 3.0
ASDF5160RM-8 ● 8 139 160 105 63 30 16.4 9 40 68 3 Fig.3 4.3 切削性能
ASDF5160RM-8U ● 8 139 160 105 63 30 16.4 9 40 68 3 Fig.3 4.3 Cutt ing performance
ASDF5160RM-10U ● 10 139 160 105 63 30 16.4 9 40 68 3 Fig.3 4.3
●印:標準在庫品です。●:Stocked Items. 【注意】アーバ用ねじは付属しません。【Note】Arbor screw is not included.
※ASDF形は「工具最外径DCX」を刃径基準としています。ASDH形とは異なるので注意してください。 01 炭素鋼 S50C(220HB)Carbon 02 プリハードン鋼(42HRC) Pre-Hardened
steels steels 03 ステンレス鋼(SUS304) Stainless
steels
※ASDF type uses the maximum tool diameter DCX as the flute diameter standard. This is different than for ASDH type, so care should be taken.
商品コード末尾に「U」があるアイテムは、不等分割ピッチとなります。Items with a "U" at the end of the item code have an unequal pitch. 工具 Tool:ASDF5063R-4 工具 Tool:ASDF5063R-4 工具 Tool:ASDF5063R-4
切削条件 インサート Insert:SNMU1607EN-C 切削条件 インサート Insert:SNMU1607EN-C 切削条件 インサート Insert:SNMU1607EN-C
工具径と切削動力 Cutting (JS4160相当 Equivalent to JS4160) Cutting (JP4120相当 Equivalent to JP4120) Cutting (JM4160相当 Equivalent to JM4160)
Tool diameter and cutting power Conditions vc = 184m/min fz = 1.5mm/t Conditions vc = 100m/min fz = 1.0mm/t Conditions vc = 90m/min fz = 0.8mm/t
ap×ae = 1 × 40mm エアブロー Air-blow ap×ae = 1 × 40mm エアブロー Air-blow ap×ae = 1 × 40mm エアブロー Air-blow
1000 25 0.6 0.6 0.6
900 参考切削条件 ASDF形(高送り) ASDF type (High-feed-rate type)
Pc[鋳鉄 FC250] Cast irons
800 Pc[炭素鋼 S50C] Carbon steels 20 Reference vc = 180m/min fz = 1.5mm/t ap×ae = 1.0 × 0.7DCX mm 従来品
0.5 0.5 Conventional 0.5
700 Q cutting condition エアブロー Air-blow 従来品
0.4
600 15 Conventional 0.4 0.4
ASDF ASDF ASDF
500 参考切削条件における各工具径ごとの必要切削動力Pcの算出結果です。工具径選
0.3 0.3 0.3
400 10 定の目安としてご使用ください。
300 本数値は一般的な機械条件で算出している為、実際の数値と異なる場合があります。 0.2 0.2 0.2
200 5 The chart shows the calculated results for required cutting power Pc for each tool diameter 0.1 0.1 0.1
100 under the reference cutting conditions. Please use as criteria when selecting tool diameter. 150min後 70min後 48min後
0 0 These values are calculated from general machinery conditions, and may be different from 0 0 0
0 63-4NT 80-4NT 100-5NT 125-6NT 160-8NT actual values. 0 20 40 60 80 100 120 140 160 0 20 40 60 80 100 120 140 160 0 20 40 60 80 100 120 140 160
工具径 DCX(mm) Tool dia. 切削時間 Cutting time (min) 切削時間 Cutting time (min) 切削時間 Cutting time (min)
※図、表等のデータは試験結果の一例です。 ※Drawings, data in tables, etc. are examples of test results.
04
ボアタイプ Bore type
切りくず排出量 Q(cm3/min)
Metal removal rate 内径ミリサイズ Internal diameter mm size 内径インチサイズ Internal diameter inch size
φ14 φ66.7
逃げ面摩耗幅 VBmax
Flank wear (mm)
逃げ面摩耗幅 VBmax
Flank wear (mm)
逃げ面摩耗幅 VBmax
Flank wear (mm)
切削動力 Pc(kw)
Cutting power
Page5
A SDF type
ラSイDンF A
ナ形ッ【プ高送りタイプ】 ラインナップ 標準切削条件表
Line Up 【 High-feed-rate type】 Line Up Recommended Cut t ing Condi t ions
) ※赤字は第一推奨材種です。
ASDF5 (R M -(U) ASDF形 ASDF type【高送りタイプ】 High-feed-rate type Red indicates primary recommended grade.
は数字が入ります。 Numeric figure in a circle .
被削材 推奨材種 切削速度 一刃当りの送り
Cutting speed Feed per tooth 工具径 DCX φ63(4枚刃)φ80(4枚刃)φ100(5枚刃)φ125(6枚刃)φ160(8枚刃)
Work material Recommended
inserts grade Vc( m/min) fz( mm/t) Tool dia. 4 Flutes 4 Flutes 5 Flutes 6 Flutes 8 Flutes
n (min-1) 710 560 450 360 280
炭素鋼・合金鋼 ※ Vc(m/min) 140 140 140 140 140
V f (mm/min) 4,260 3,360 3,380 3,240 3,360
(30HRC以下) GX2140 100 ~ 180 1.0 ~ 2.0 fz(mm/t) 1.5 1.5 1.5 1.5 1.5
Carbon steels, Alloy steels (mm) 1.5 1.5 1.5 1.5 1.5
(30HRC or less) JS4160 ap
ae(mm) 44 56 70 88 112
Q(cm3/min) 281 282 355 428 564
φ20 n (min-1) 610 480 380 310 240
合金鋼(焼入れ焼戻し材) Vc(m/min) 120 120 120 120 120
(35HRC以下) JS4160 Vf(mm/min) 3,660 2,880 2,850 2,790 2,880
Alloy steels 0 1.0 ~ 2.0 fz(mm/t) 1.5 1.5 1.5 1.5 1.5
(Quenched and tempered steels) GX2140 100 ~ 16
ap(mm) 1.5 1.5 1.5 1.5 1.5
(35HRC or less) ae(mm) 44 56 70 88 112
Q(cm3/min) 242 242 299 368 484
Fig.1(エアー穴付き)(With air hole) Fig.2(エアー穴無し)(Without air hole) Fig.3(エアー穴無し)(Without air hole) n (min-1) 450 360 290 230 180
プリハードン鋼・合金鋼
DHUB DHUB DHUB Vc(m/min) 90 90 90 90 90
50 1,160 1,100 1,150
DCONMS DCONMS DCONMS (焼入れ焼戻し材)(45HRC以下) V f (mm/min) 1,440 1,1
P4120 80 ~ 120 0.4 ~ 0.8 fz(mm/t) 0.8 0.8 0.8 0.8 0.8
KWW KWW KWW Pre-hardened steels, Alloy steels J
(Quenched and tempered steels) ap(mm) 1.0 1.0 1.0 1.0 1.0
(45HRC or less) ae(mm) 44 56 70 88 112
b b b Q(cm3/min) 63 64 81 97 129
n (min-1) 350 280 220 180 140
CBDP CBDP CBDP 焼入れ鋼 Vc(m/min) 70 70 70 70 70
min) 560 450 440 430 450
LF LF (55HRC以下) Vf(mm/
JP4120 60 ~ 100 0.3 ~ 0.6 fz(mm/t) 0.4 0.4 0.4 0.4 0.4
LF Hardened steels ap(mm) 0.8 0.8 0.8 0.8 0.8
(55HRC or less) ae(mm) 44 56 70 88 112
Q(cm3/min)
APMX APMX 20 20 25 30 40
APMX n (min-1) 450 360 290 230 180
Vc(m/min) 90 90 90 90 90
DCCB DCCB DCCB ステンレス鋼 JM4160 V f (mm/min) 1,800 1,440 1,450 1,380 1,440
DC DC DC Stainless steels 1.0 1.0
DCX DCX DCX Y-100 JP4120 80 ~ 100 0.8 ~ 1.2 fz(mm/t) 1.0 1.0 1.0
ap(mm) 1.0 1.0 1.0 1.0 1.0
ラSイUSンナップ ae(mm) 44 56 70 88 112
Q(cm3/min) 79 81 102 121 161
n (min-1) 810 640 510 410 320
Line鋳 U鉄
Vc(m/min) 160 160 160 160 160
p JP4120 V f (mm/min) 4,860 3,840 3,830 3,690 3,840
Cast irons fz(mm/t) 1.5 1.5 1.5 1.5 1.5
FC・FCD GX2120 100 ~ 180 1.0 ~ 2.0
ap(mm) 1.5 1.5 1.5 1.5 1.5
ae(mm) 44 56 70 88 112
Q(cm3/min) 321 323 402 487 645
n (min-1) 180 140 110 90 70
耐熱合金 Vc(m/min) 35 35 35 35 35
超耐熱合金 JM4160 V f (mm/min) 290 220 220 220 220
fz(mm/t) 0.4 0.4 0.4 0.4 0.4
Heat resistant alloys JP4120 25 ~ 50 0.2 ~ 0.8
ap(mm) 1.0 1.0 1.0 1.0 1.0
Super heat resistant alloys ae(mm) 44 56 70 88 112
Q(cm3/min) 13 12 15 19 25
n (min-1) 250 200 160 130 100
Vc(m/min) 50 50 50 50 50
チタン合金 JM4160 V f (mm/min) 400 320 320 310 320
fz(mm/t) 0.4 0.4 0.4 0.4 0.4
Titanium alloys JP4120 40 ~ 60 0.2 ~ 0.8
ap(mm) 1.0 1.0 1.0 1.0 1.0
ae(mm) 44 56 70 88 112
Q(cm3/min) 18 18 22 27 36
【注意】①GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。 ae
②被削材、加工形状に合わせて、適切なクーラントを使用してください。
③この切削条件表は切削条件の目安を示すものです。実際の加工では、加工形状、目的、使用機械等により条件を調整してください。
④インサートの交換は早めに行い、過度の使用による破損を防止してください。
⑤排出した切りくずは、飛散し作業者を切傷させ、やけどあるいは目に入って負傷させる恐れがありますので、ご使用に際してはその周囲に安全カバーを ap
取付け、保護メガネなどの保護具を着用し、安全な環境で作業されることをお願い致します。
【Note】①Please note that the GX Coating and JS Coating don't cause a
reaction in conductive touch sensors. ASDF形を形状加工で使用する場合 When using ASDF type for shaping cutting
②Use the appropriate coolant for the work material and machining
shape. プログラム上の刃先形状定義は下記を参照ください。
③These conditions are for general guidance; in actual machining Refer to the following for the flute tip condition definitions for programming.
conditions adjust the parameters according to your actual
machine and work-piece conditions. プログラミングR Programming R definition = R6
④In order to avoid of insert breakage, please change insert earlier. 削り残し量 Remains 1.33mm
⑤The steel chips may cause cuts, burns or damages to eyes. Be
sure to install the safety cover around the tool and wear the ※傾斜加工はφ63,φ80で0.5°以下。φ100以上では行わないで下さい。
safety glasses when carrying out any works. ※工具突出しが長い場合(L / D ≧ 3)はapを調整して下さい。
R6 ※For slanted cutting using ∅63 or ∅80, perform at 0.5° or less.
Do not perform using ∅100 or larger.
削り残し量 Remains 1.33mm ※When tool overhang length is long (L / D ≧ 3), adjust ap .
切削性能
Cutt ing performance
●印:標準在庫品です。●:Stocked Items. 【注意】アーバ用ねじは付属しません。【Note】Arbor screw is not included. Hardened
※ASDF形は「工具最外径DCX」を刃径基準としています。ASDH形とは異なるので注意してください。 01 炭素鋼 S50C(220HB)Carbon
steels 02 プリハードン鋼(42HRC) Pre-
steels 03 ステンレス鋼(SUS304) Stainless
steels
※ASDF type uses the maximum tool diameter DCX as the flute diameter standard. This is different than for ASDH type, so care should be taken.
商品コード末尾に「U」があるアイテムは、不等分割ピッチとなります。Items with a "U" at the end of the item code have an unequal pitch. 工具 Tool:ASDF5063R-4 工具 Tool:ASDF5063R-4 工具 Tool:ASDF5063R-4
切削条件 インサート Insert:SNMU1607EN-C 切削条件 インサート Insert:SNMU1607EN-C 切削条件 インサート Insert:SNMU1607EN-C
工具径と切削動力 Cutting (JS4160相当 Equivalent to JS4160) Cutting (JP4120相当 Equivalent to JP4120) Cutting (JM4160相当 Equivalent to JM4160)
Tool diameter and cutting power Conditions vc = 184m/min fz = 1.5mm/t Conditions vc = 100m/min fz = 1.0mm/t Conditions vc = 90m/min fz = 0.8mm/t
ap×ae = 1 × 40mm エアブロー Air-blow ap×ae = 1 × 40mm エアブロー Air-blow ap×ae = 1 × 40mm エアブロー Air-blow
1000 25 0.6 0.6 0.6
900 50] Cast irons 参考切削条件 ASDF形(高送り) ASDF type (High-feed-rate type)
Pc[鋳鉄 FC2
800 Pc[炭素鋼 S50C] Carbon steels 20 Reference vc = 180m/min fz = 1.5mm/t ap×ae = 1.0 × 0.7DCX mm 従来品
0.5 0.5 Conventional 0.5
700 Q cutting condition エアブロー Air-blow 従来品
0.4 4
600 15 Conventional 0.4 0.
参考切削条件における各工具径ごとの必要切削動力Pcの算出結果です。工具径選 ASDF ASDF ASDF
500 0.3 0.3 0.3
400 10 定の目安としてご使用ください。
300 本数値は一般的な機械条件で算出している為、実際の数値と異なる場合があります。 0.2 0.2 0.2
200 5 The chart shows the calculated results for required cutting power Pc for each tool diameter 0.1 0.1 0.1
100 under the reference cutting conditions. Please use as criteria when selecting tool diameter. 150min後 70min後 48min後
0 0 These values are calculated from general machinery conditions, and may be different from 0 0 0
0 63-4NT 80-4NT 100-5NT 125-6NT 160-8NT actual values. 0 20 40 60 80 100 120 140 160 0 20 40 60 80 100 120 140 160 0 20 40 60 80 100 120 140 160
工具径 DCX(mm) Tool dia. 切削時間 Cutting time (min) 切削時間 Cutting time (min) 切削時間 Cutting time (min)
※図、表等のデータは試験結果の一例です。 ※Drawings, data in tables, etc. are examples of test results.
05
切りくず排出量 Q(cm3/min)
Metal removal rate
φ14 φ66.7
逃げ面摩耗幅 VBmax
Flank wear (mm)
逃げ面摩耗幅 VBmax
Flank wear (mm)
逃げ面摩耗幅 VBmax
Flank wear (mm)
切削動力 Pc(kw)
Cutting power
Page6
ASDH ASDH type
形【高切込みタイプ】 ラインナップ 標準切削条件表
【 High-cutting-depth type】 Line Up Recommended Cut t ing Condi t ions
ASDH ※赤字は第一推奨材種です。
ASDH5 (R M)- 形 ASDH type【高切込みタイプ】 High-cutting-depth type Red indicates primary recommended grade.
は数字が入ります。 Numeric figure in a circle .
φ20
Fig.1(エアー穴付き)(With air hole) Fig.2(エアー穴無し)(Without air hole) Fig.3(エアー穴無し)(Without air hole)
DHUB DHUB DHUB
DCONMS DCONMS DCONMS
KWW KWW KWW
b b b
CBDP CBDP CBDP
LF LF LF
APMX
APMX APMX
DCCB DCCB DCCB
DC DC DC
DCX DCX DCX
寸 法 Size(㎜)
商品コード 在庫 刃数 工具径 キー幅 形状 重量 適用インサート
Shape Weight 備考
Item code Stock No.of Tool dia. D Key width
flutes HUB LF CBDP DCONMS DCCB APMX (kg) Inserts Note
DC DCX KWW b
ASDH5063R-4 ● 4 63 75 60 50 19 8.4 5 22.225 17 10 Fig.1 0.9
ASDH5080R-4 ● 4 80 92 76 63 32 12.7 8 31.75 26 10 Fig.1 1.7
ASDH5100R-5 ● 5 100 112 96 63 32 12.7 8 31.75 26 10 Fig.1 2.8
ASDH5125R-6 ● 6 125 137 100 63 38 15.9 10 38.1 60 10 Fig.2 3.6
ASDH5125R-8 ● 8 125 137 100 63 38 15.9 10 38.1 60 10 Fig.2 3.6
ASDH5160R-8 ● 8 160 172 105 63 38 19.1 11 50.8 80 10 Fig.2 5.2
SNMU1607EN-C
ASDH5160R-10 ● 10 160 172 105 63 38 19.1 11 50.8 80 10 Fig.2 5.1 SNGU1607EN-C 【注意】①GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。 ae
ASDH5063RM-4 ● 4 63 75 60 50 20 10.4 6.3 22 17 10 Fig.1 0.9 SNMU1607EN-B ②被削材、加工形状に合わせて、適切なクーラントを使用してください。
③この切削条件表は切削条件の目安を示すものです。実際の加工では、加工形状、目的、使用機械等により条件を調整してください。
ASDH5080RM-4 ● 4 80 92 76 63 22 12.4 7 27 20 10 Fig.1 1.8 ④インサートの交換は早めに行い、過度の使用による破損を防止してください。
ASDH5100RM-5 ● ⑤排出した切りくずは、飛散し作業者を切傷させ、やけどあるいは目に入って負傷させる恐れがありますので、ご使用に際してはその周囲に安全カバー
5 100 112 96 63 32 14.4 8 32 26 10 Fig.1 2.8 を取付け、保護メガネなどの保護具を着用し、安全な環境で作業されることをお願い致します。 ap
ASDH5125RM-6 ● 6 125 137 100 63 30 16.4 9 40 56 10 Fig.2 3.6 【Note】①Please note that the GX Coating and JS Coating don't cause a reaction in conductive touch sensors.
②Use the appropriate coolant for the work material and machining shape.
ASDH5125RM-8 ● 8 125 137 100 63 30 16.4 9 40 56 10 Fig.2 3.5 ③These conditions are for general guidance; in actual machining conditions adjust the parameters according to your actual machine and work-piece conditions.
④In order to avoid of insert breakage, please change insert earlier.
ASDH5160RM-8 ● 8 160 172 105 63 30 16.4 9 40 68 10 Fig.3 5.2 ⑤The steel chips may cause cuts, burns or damages to eyes. Be sure to install the safety cover around the tool and wear the safety glasses when carrying out any works.
ASDH5160RM-10 ● 10 160 172 105 63 30 16.4 9 40 68 10 Fig.3 5.1
●印:標準在庫品です。●:Stocked Items. 【注意】アーバ用ねじは付属しません。【Note】Arbor screw is not included.
※ASDH形は「工具先端径DC」を刃径基準としています。ASDF形とは異なるので注意してください。 切削性能
※ASDH type uses the tool tip diameter DC as the flute diameter standard. This is different than for ASDF type, so care should be taken.
※ASDH形は形状加工には使用できません。 Cutt ing performance
※ASDH type cannot be used for shaping cutting.
01 炭素鋼 S50C(220HB) Carbon steels 02 鋳鉄 FC250 Cast irons
工具径と切削動力 Tool diameter and cutting power
切削条件 工具 Tool:ASDH5063R-4 切削条件 工具 Tool:ASDH5063R-4
1000 25
900 参考切削条件 ASDH形(高切込み)ASDH type (High-cutting-depth type) Cutting インサート Insert:SNMU1607EN-C(GX2140) Cutting インサート Insert:SNMU1607EN-C(GX2120)
Pc[鋳鉄 FC250] Cast irons
800 Pc[炭素鋼 Reference vc = 150m/min fz = 0.3mm/t Conditions vc = 220m/min fz = 0.2mm/t ap×ae = 2.0 × 40mm Conditions vc = 220m/min fz = 0.2mm/t ap×ae = 2.0 × 40mm
S50C] Carbon steels 20
cutting condition ap×ae = 5.0 × 0.7DC mm エアブロー Air-blow エアブロー Air-blow エアブロー Air-blow
700 Q
600 15 参考切削条件における各工具径ごとの必要切削動力Pcの 0.6 0.6
500 算出結果です。工具径選定の目安としてご使用ください。
400 10 GX2140 GX2120
本数値は一般的な機械条件で算出している為、実際の数値 0.5 0.5 従来品A,B,C
300 と異なる場合があります。 従来品A,B,C,D Conventional A,B,C
200 5 0.4
The chart shows the calculated results for required cutting power Pc for Conventional A,B,C,D 0.4
89min後 70min後
100 each tool diameter under the reference cutting conditions. Please use 0.3 0.3
0 0 as criteria when selecting tool diameter.
0 63-4NT 80-4NT 100-5NT 125-6NT 125-8NT 160-8NT 160-10NT These values are calculated from general machinery conditions, and
工具径 DC(mm) Tool dia. may be different from actual values. 0.2 0.2
0.1 ASDH 0.1 ASDH
0 0
0 20 40 60 80 100 120 140 160 0 20 40 60 80 100 120 140 160
切削時間 Cutting time (min) 切削時間 Cutting time (min)
※図、表等のデータは試験結果の一例です。 ※Drawings, data in tables, etc. are examples of test results.
06
切りくず排出量 Q(cm3/min) ボアタイプ Bore type
Metal removal rate 内径ミリサイズ Internal diameter mm size 内径インチサイズ Internal diameter inch size
φ14
逃げ面摩耗幅 VBmax
Flank wear (mm)
逃げ面摩耗幅 VBmax
Flank wear (mm)
6.7
φ6
切削動力 Pc(kw)
Cutting power
Page7
ASDH ASDH type
形【高切込みタイプ】 ラインナップ 標準切削条件表
【 High-cutting-depth type】 Line Up Recommended Cut t ing Condi t ions
ASDH ※赤字は第一推奨材種です。
ASDH5 (R M)- 形 ASDH type【高切込みタイプ】 High-cutting-depth type Red indicates primary recommended grade.
は数字が入ります。 Numeric figure in a circle .
被削材 推奨材種 切削速度 一刃当りの送り
Cutting speed Feed per tooth 工具径 DC φ63(4枚刃)φ80(4枚刃)φ100(5枚刃)φ125(6枚刃)φ160(8枚刃)
Work material Recommended
inserts grade Vc( m/min) fz( mm/t) Tool dia. 4 Flutes 4 Flutes 5 Flutes 6 Flutes 8 Flutes
n (min-1) 710 560 450 360 280
Vc(m/min) 140 140 140 140 140
炭素鋼・合金鋼 ※ V f (mm/min) 850 670 680 650 670
(30HRC以下) GX2140 100 ~ 180 0.1 ~ 0.5 fz(mm/t) 0.3 0.3 0.3 0.3 0.3
Carbon steels, Alloy steels
(30HRC or less) JS4160 ap(mm) 4.0 4.0 4.0 4.0 4.0
ae(mm) 44 56 70 88 112
Q(cm3/min) 150 150 190 229 300
φ20 n (min-1) 610 480 380 310 240
合金鋼(焼入れ焼戻し材) Vc(m/min) 120 120 120 120 120
(35HRC以下) JS4160 Vf(mm/min) 490 380 380 370 380
Alloy steels fz(mm/t) 0.2 0.2 0.2 0.2 0.2
(Quenched and tempered steels) GX2140 100 ~ 160 0.1 ~ 0.3
ap(mm) 4.0 4.0 4.0 4.0 4.0
(35HRC or less) ae(mm) 44 56 70 88 112
Fig.1(エアー穴付き)(With air hole) Fig.2(エアー穴無し)(Without air hole) Fig.3(エアー穴無し)(Without air hole) Q(cm3/min) 86 85 106 130 170
DHUB DHUB DHUB n (min-1) 450 360 290 230 180
DCONMS DCONMS DCONMS プリハードン鋼・合金鋼 Vc(m/min) 90 90 90 90 90
KWW KWW KWW (焼入れ焼戻し材)(45HRC以下) V f (mm/min) 220 170 170 170 170
b b b Pre-hardened steels, Alloy steels JP4120 80 ~ 120 0.1 ~ 0.15 fz(mm/t) 0.12 0.12 0.12 0.12 0.12
(Quenched and tempered steels) ap(mm) 3.0 3.0 3.0 3.0 3.0
CBDP CBDP CBDP (45HRC or less) ae(mm) 44 56 70 88 112
Q(cm3/min) 29 29 36 45 57
LF LF LF n (min-1) 350 280 220 180 140
APMX Vc(m/min) 70 70 70 70 70
焼入れ鋼
APMX APMX Vf(mm/min) 170 130 130 130 130
(55HRC以下)
DCCB DCCB DCCB JP4120 60 ~ 100 0.1 ~ 0.15 fz(mm/t) 0.12 0.12 0.12 0.12 0.12
Hardened steels
DC DC DC (55HRC or less) ap(mm) 2.0 2.0 2.0 2.0 2.0
DCX DCX DCX ae(mm) 44 56 70 88 112
Q(cm3/min) 15 15 18 23 29
寸 法 Size(㎜) n (min-1) 450 360 290 230 180
商品コード 在庫 刃数 工具径 キー幅 形状 重量 Vc(m/min) 90 90 90 90 90
Weight 適用インサート 備考
Item code Stock No.of Tool dia. DHUB LF CBDP Key width DCCB Shape ステンレス鋼
flutes DCONMS APMX
DC DCX JM4160 V f (mm/min) 540 430 440 410 430
KWW b (kg) Inserts Note
Stainless steels fz(mm/t) 0.3 0.3 0.3 0.3 0.3
ASDH5063R-4 ● 4 63 75 60 50 19 8.4 5 22.225 17 10 Fig.1 0.9 SUS JP4120 80 ~ 100 0.1 ~ 0.4
ap(mm) 3.0 3.0 3.0 3.0 3.0
ae(mm) 44 56 70 88 112
ASDH5080R-4 ● 4 80 92 76 63 32 12.7 8 31.75 26 10 Fig.1 1.7 Q(cm3/min) 71 72 92 108 144
n (min-1) 810 640 510 410 320
ASDH5100R-5 ● 5 100 112 96 63 32 12.7 8 31.75 26 10 Fig.1 2.8 Vc(m/min) 160 160 160 160 160
ASDH5125R-6 ● 6 125 137 100 63 38 15.9 10 38.1 60 10 Fig.2 3.6 鋳鉄 JP4120 V f (mm/min) 970 770 770 740 770
Cast irons fz(mm/t) 0.3 0.3 0.3 0.3 0.3
ASDH5125R-8 ● 8 125 137 100 63 38 15.9 10 38.1 60 10 Fig.2 3.6 FC・FCD GX2120 100 ~ 180 0.1 ~ 0.5
ap(mm) 5.0 5.0 5.0 5.0 5.0
ASDH5160R-8 ● 8 160 172 105 63 38 19.1 11 50.8 80 10 Fig.2 5.2 ae(mm) 44 56 70 88 112
SNMU1607EN-C Q(cm3/min) 213 216 270 326 431
ASDH5160R-10 ● 10 160 172 105 63 38 19.1 11 50.8 80 10 Fig.2 5.1 SNGU1607EN-C 【注意】①GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。 ae
ASDH5063RM-4 ● 4 63 75 60 50 20 10.4 6.3 22 17 10 Fig.1 0.9 SNMU1607EN-B ②被削材、加工形状に合わせて、適切なクーラントを使用してください。
③この切削条件表は切削条件の目安を示すものです。実際の加工では、加工形状、目的、使用機械等により条件を調整してください。
ASDH5080RM-4 ● 4 80 92 76 63 22 12.4 7 27 20 10 Fig.1 1.8 ④インサートの交換は早めに行い、過度の使用による破損を防止してください。
ASDH5100RM-5 ● ⑤排出した切りくずは、飛散し作業者を切傷させ、やけどあるいは目に入って負傷させる恐れがありますので、ご使用に際してはその周囲に安全カバー
5 100 112 96 63 32 14.4 8 32 26 10 Fig.1 2.8 を取付け、保護メガネなどの保護具を着用し、安全な環境で作業されることをお願い致します。 ap
ASDH5125RM-6 ● 6 125 137 100 63 30 16.4 9 40 56 10 Fig.2 3.6 【Note】①Please note that the GX Coating and JS Coating don't cause a reaction in conductive touch sensors.
②Use the appropriate coolant for the work material and machining shape.
ASDH5125RM-8 ● 8 125 137 100 63 30 16.4 9 40 56 10 Fig.2 3.5 ③These conditions are for general guidance; in actual machining conditions adjust the parameters according to your actual machine and work-piece conditions.
④In order to avoid of insert breakage, please change insert earlier.
ASDH5160RM-8 ● 8 160 172 105 63 30 16.4 9 40 68 10 Fig.3 5.2 ⑤The steel chips may cause cuts, burns or damages to eyes. Be sure to install the safety cover around the tool and wear the safety glasses when carrying out any works.
ASDH5160RM-10 ● 10 160 172 105 63 30 16.4 9 40 68 10 Fig.3 5.1
●印:標準在庫品です。●:Stocked Items. 【注意】アーバ用ねじは付属しません。【Note】Arbor screw is not included.
※ASDH形は「工具先端径DC」を刃径基準としています。ASDF形とは異なるので注意してください。 切削性能
※ASDH type uses the tool tip diameter DC as the flute diameter standard. This is different than for ASDF type, so care should be taken.
※ASDH形は形状加工には使用できません。 Cutt ing performance
※ASDH type cannot be used for shaping cutting.
01 炭素鋼 S50C(220HB) Carbon steels 02 鋳鉄 FC250 Cast irons
工具径と切削動力 Tool diameter and cutting power
切削条件 工具 Tool:ASDH5063R-4 切削条件 工具 Tool:ASDH5063R-4
1000 25
900 参考切削条件 ASDH形(高切込み)ASDH type (High-cutting-depth type) Cutting インサート Insert:SNMU1607EN-C(GX2140) Cutting インサート Insert:SNMU1607EN-C(GX2120)
Pc[鋳鉄 FC250] Cast irons 0m/min fz = 0.3mm/t
800 Conditions vc = 220m/min fz = 0.2mm/t ap×ae = 2.0 × 40mm Conditions vc = 220m/min fz = 0.2mm/t ap×ae = 2.0 × 40mm
Pc[炭素鋼 S50C] Carbon steels 20 Reference vc = 15
cutting condition ap×ae = 5.0 × 0.7DC mm エアブロー Air-blow エアブロー Air-blow エアブロー Air-blow
700 Q
600 15 参考切削条件における各工具径ごとの必要切削動力Pcの 0.6 0.6
500 算出結果です。工具径選定の目安としてご使用ください。
400 10 GX2140 GX2120
本数値は一般的な機械条件で算出している為、実際の数値 0.5 0.5 従来品A,B,C
300 と異なる場合があります。 従来品
0.4 A,B,C,D Conventional A,B,C
200 5 The chart shows the calculated results for required cutting power Pc for Conventional A,B,C,D 0.4
89min後 70min後
100 each tool diameter under the reference cutting conditions. Please use 0.3 0.3
0 0 as criteria when selecting tool diameter.
0 63-4NT 80-4NT 100-5NT 125-6NT 125-8NT 160-8NT 160-10NT These values are calculated from general machinery conditions, and
工具径 DC(mm) Tool dia. may be different from actual values. 0.2 0.2
0.1 ASDH 0.1 ASDH
0 0
0 20 40 60 80 100 120 140 160 0 20 40 60 80 100 120 140 160
切削時間 Cutting time (min) 切削時間 Cutting time (min)
※図、表等のデータは試験結果の一例です。 ※Drawings, data in tables, etc. are examples of test results.
07
切りくず排出量 ボアタイプ Bore typeQ(cm3/min)
Metal removal rate 内径ミリサイズ Internal diameter mm size 内径インチサイズ Internal diameter inch size
φ14
逃げ面摩耗幅 VBmax
Flank wear (mm)
逃げ面摩耗幅 VBmax
Flank wear (mm)
6.7
φ6
切削動力 Pc(kw)
Cutting power
Page8
図、表等のデータは試験結果の一例であり、保証値ではありません。
「 」は株式会社MOLDINOの登録商標です。
The diagrams and table data are examples of test results, and are not guaranteed values.
“ ” is a registered trademark of MOLDINO Tool Engineering, Ltd.
安 全 上 の ご 注 意 Attentions on Safety
1. 取扱上のご注意 1. Attentions regarding handling
(1)工具をケース(梱包)から取り出す際は、足元への落下あるいは素手の指先へ落して怪我をしないよ (1) When removing the tool from the case (package), be careful not to drop it on your foot or
うに十分なご注意をお願いします。 drop it onto the tips of your bare fingers.
(2)インサートをセットして実際にご使用する場合は、切れ刃を素手で直接触れないように注意してください。 (2) When actually setting the inserts, be careful not to touch the cutting flute directly with
2. 取付け時のご注意 your bare hands.
(1)ご使用にあたって、インサートのセッティングは確実に行っていただき、アーバ等への取付けも確実に 2. Attentions regarding mounting
行ってください。 (1) When preparing for use, be sure that the inserts are firmly mounted in place and that they
(2)ご使用中に、異常な振動等が発生した場合は、直ちに機械を停止させて、その振動の原因を除いて are firmly mounted on the arbor, etc.
ください。 (2) If abnormal chattering occurs during use, stop the machine immediately and remove the
cause of the chattering.
3. 使用上のご注意
(1)切削工具あるいは被削材の寸法・回転の方向は、あらかじめ確認しておいてください。 3. Attentions during use
(1) Before use, confirm the dimensions and direction of rotation of the tool and milling work
(2)標準切削条件表の数値は、新しい作業の立上げの目安としてご利用ください。切込みが大きい場合、 material.
使用機械の剛性が小さい場合あるいは被加工物の性状に応じて切削条件を適正に調整してご使用 (2) The numerical values in the standard cutting conditions table should be used as criteria when
ください。 starting new work. The cutting conditions should be adjusted as appropriate when the cutting
(3)インサートは硬質の材料です。ご使用中に破損して飛散する場合があります。また、切りくずが飛散す depth is large, the rigidity of the machine being used is low, or according to the conditions of
ることがあります。これらの飛散物等は作業者を切傷させ、火傷あるいは目に入って負傷させる恐れが the work material.
ありますので、工具をご使用中はその周囲に安全カバーを取付け、保護めがね等の保護具を着用し (3) The inserts are made of a hard material. During use, they may break and fly off. In addition,
て安全な環境下での作業をお願いいたします。 cutting chips may also fly off. Since there is a danger of injury to workers, fire, or eye damage
・引火や爆発の危険のあるところでは使用しないでください。 from such flying pieces, a safety cover should be installed and safety equipment such as
・不水溶性切削油は、火災の恐れがありますので使用しないでください。 safety glasses should be worn to create a safe environment for work.
(4)工具を本来の目的以外に使用したり、改造したりしないでください。 ・Do not use where there is a risk of fire or explosion.
・Do not use non-water-soluble cutting oils. Such oils may result in fire.
4. 工具に関して、安全上の問題点・不明の点・その他ご相談がありましたら フリーダイヤル技術相談 へ (4) Do not use the tool for any purpose other than that for which it is intended, and do not modify it.
お問い合わせください。
ホームページ フリーダイヤル技術相談
https://www.moldino.com
MOLDINO Tool Engineering, Ltd.
本社 〒130-0026 東京都墨田区両国4-31-11(ヒューリック両国ビル8階) 工具選定データベース【 TOOLSEARCH】
03-6890-5101 FAX 03-6890-5134
International Sales Dept .: +81-3-6890-5103 FAX +81-3-6890-5128
営業企画部 ☎03-6890-5102 FAX03-6890-5134 海外営業部 ☎03-6890-5103 FAX03-6890-5128
東京営業所 ☎03-6890-5110 FAX03-6890-5133 静岡営業所 ☎054-273-0360 FAX054-273-0361
東北営業所 ☎022-208-5100 FAX022-208-5102 名古屋営業所 ☎052-687-9150 FAX052-687-9144
新潟営業所 ☎0258-87-1224 FAX0258-87-1158 大阪営業所 ☎06-7668-0190 FAX06-7668-0194
東関東営業所 ☎0294-88-9430 FAX0294-88-9432 中四営業所 ☎082-536-2001 FAX082-536-2003
長野営業所 ☎0276-59-6001 FAX0276-59-6005 九州営業所 ☎092-289-7010 FAX092-289-7012
北関東営業所 ☎0276-59-6001 FAX0276-59-6005
神奈川営業所 ☎046-400-9429 FAX046-400-9435
ヨーロッパ/MOLDINO Tool Engineering Europe GmbH Itterpark 12, 40724 Hilden, Germany. TEL : +49-(0)2103-24820, FAX : +49-(0)2103-248230
アメリカ/MITSUBISHI MATERIALS U.S.A. CORPORATION Detroit office c/o RFM Inc. Customer service 2001 Orndorf Drive, Brighton, MI 48116 U.S.A. TEL : +1(248)308-2620, FAX :+1(248)308-2627
メキシコ/MITSUBISHI MATERIALS MÉXICO S.A. DE C.V. Av. La Cañada No.16, Parque Industrial Bernardo Quintana, El Marques, Querétaro, CP 76246, México TEL : +52-442-1926800
ブラジル/MITSUBISHI MATERIALS BRASIL LTDA. Rua Cincinato Braga, 340 13° andar.Bela Vista – CEP 01333-010 São Paulo – SP ., Brasil TEL : +55(11)3506-5600 FAX : +55(11)3506-5677
タ イ/MITSUBISHI MATERIALS (THAILAND) CO., LTD. 139/3 Moo 2, Tambon Khlong Chik, Amphoe Bang Pa-in, Phra Nakhon Si Ayutthaya 13160, Thailand TEL:+66-3525-8024
イ ン ド/Mitsubishi Materials India Private Limited H.O.: Prasad Enclave, #118/119, 1st Floor, 2nd Stage, 5th main, BBMP Ward #11, (New #38), Industrial Suburb, Yeshwanthpura, Bengaluru, 560 022, Karnataka, India. Tel : +91-80-2204-3600
予告なく、改良・改善のために仕様変更することがあります。
Specifications for the products listed in this catalog are subject to change without notice due to ベジタブルインクで印刷しています。 2026-10(ME)
replacement or modification. Printed using vegetable oil ink. Printed in JAPAN 2012-8:FP