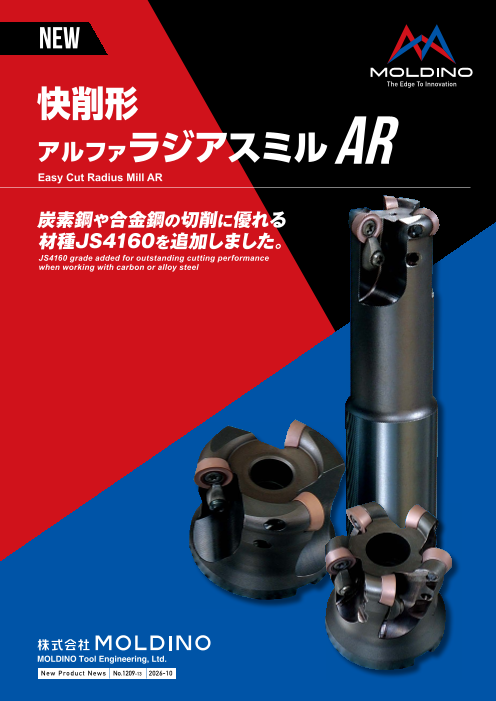


炭素鋼や合金鋼の切削に優れる材種JS4160を追加しました。
◆直彫り加工のエース
◆三次元荒加工に好適!
◆詳細はカタログをダウンロードしご覧いただくか、お気軽にお問い合わせ下さい。
このカタログについて
| ドキュメント名 | 快削形 アルファ ラジアスミル AR |
|---|---|
| ドキュメント種別 | 製品カタログ |
| ファイルサイズ | 2.9Mb |
| 登録カテゴリ | |
| 取り扱い企業 | 株式会社MOLDINO (この企業の取り扱いカタログ一覧) |
この企業の関連カタログ


このカタログの内容
Page1
NEW
快削形
アルファラジアスミルAR
Easy Cut Radius Mill AR
炭素鋼や合金鋼の切削に優れる
材種JS4160を追加しました。
JS4160 grade added for outstanding cutting performance
when working with carbon or alloy steel
MOLDINO Tool Engineering, Ltd.
New Produc t News No.1209-13 2026-10
Page2
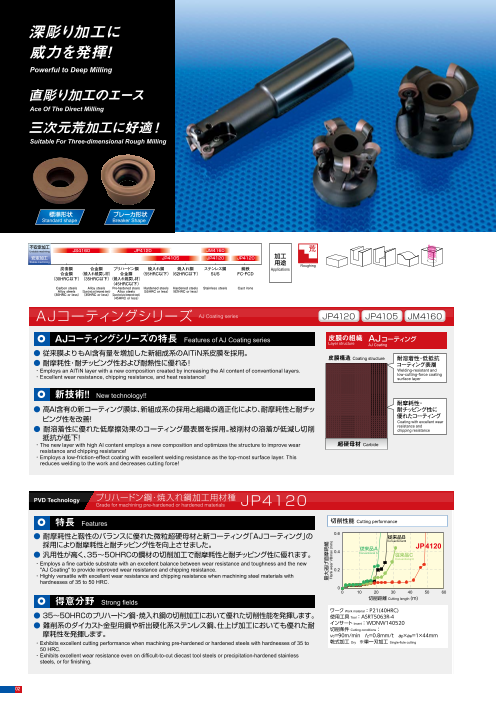
深彫り加工に テクノロジー
Technology
威力を発揮!
Powerful to Deep Milling
直彫り加工のエース PVD Technology ステンレス鋼系材料加工用材種
Ace Of The Direct Milling Grade for machining stainless-steel materials JM4160
三次元荒加工に好適! 特長 Features 切削性能 Cutting performance
0.6
従来品 Conventional
Suitable For Three-dimensional Rough Milling ● 靱性に優れた超硬母材と新コーティング「AJコーティング」の採用により、ステンレス鋼系材
料の切削加工に対して耐摩耗性と耐チッピング性を向上させました。 0.4
● 耐溶着性に優れる「AJコーティング」の採用により、ステンレス鋼系材料の加工で発生する JM4160
被削材の溶着を低減しました。 0.2
・Employs a carbide substrate with high toughness and the new "AJ Coating" to improve wear resistance and
chipping resistance when machining stainless-steel materials.
・ Employs AJ Coating with excellent welding resistance to reduce the welding to work material that occurs when 0
machining stainless steel materials. 0 4 8 12
切削距離 Cutting length (m)
標準形状 ブレーカ形状 ワーク Work material:SUS304
Standard shape Breaker Shape 得意分野 Strong fields 使用工具 Tool:ASRS2032R-5
インサート Insert:EPMT0603EN-8LF
● ステンレス鋼系材料の加工全般において長寿命を実現します。 切削条件 Cutting conditions:
・Provides long tool life for general processing of stainless-steel materials vc=180m/min fz=0.5mm/t ap×ae=0.8×21mm
不安定加工 湿式加工 Wet ※単一刃加工 Single-flute cutting
Unstable machining JS4160 JP4120 JM4160 荒
安定加工 JP4105 JP4120 JP4120 加工
Stable machining 用途 Roughing
炭素鋼 合金鋼 プリハードン鋼 焼入れ鋼 焼入れ鋼 ステンレス鋼 鋳鉄 Applications
合金鋼 (焼入れ焼戻し材) 合金鋼 (55HRC以下)(62HRC以下) SUS FC・FCD
(30HRC以下)(35HRC以下)(焼入れ焼戻し材)
(45HRC以下)
Carbon steels Alloy steels Pre-hardened steels Hardened steels Hardened steels Stainless steels Cast irons
Alloy steels (Quenched and tempered steels) Alloy steels (55HRC or less)(62HRC or less)
(30HRC or less) (35HRC or less)(Quenched and tempered steels) PVD Technology 高硬度材加工用材種
(45HRC or less) Grade for machining high-hardness materials JP4105
AJコーティングシリーズ AJ Coating series JP4120 JP4105 JM4160 特長 Features 切削性能 Cutting performance
0.6
● 耐摩耗性に優れた超微粒超硬母材と新コーティング「AJコーティング」の採用により
AJコーティングシリーズの特長 Features of AJ Coating series 皮膜の組織 AJコーティング 耐摩耗性を向上させました。
Layer structure 0.4 従来品
AJ Coating Conventional JP4105
● 従来膜よりもAl含有量を増加した新組成系のAlTiN系皮膜を採用。 ● 50HRC~の高硬度材の切削加工で耐摩耗性に優れます。
皮膜構造 Coating structure 耐溶着性・低抵抗 ・Employs an ultra-fine cemented carbide substrate and the new "AJ Coating" to improve wear resistance.
● 耐摩耗性・耐チッピング性および耐熱性に優れる! 0.2
コーティング表層 ・Excellent wear resistance when machining high hardness materials of 50HRC or higher.
・Employs an AlTiN layer with a new composition created by increasing the Al content of conventional layers. Welding-resistant and
・Excellent wear resistance, chipping resistance, and heat resistance! low-cutting-force coating
surface layer 得意分野 0
Strong fields 0 5 10 15
切削距離 Cutting length (m)
新技術!! New technology!! ●焼入れ鋼(50~60HRC):SKD11,SKD61,SKH,SUS420系等 ワーク Work material:SKD11(61HRC) 使用工具 Tool:ASRS2032-5
耐摩耗性・
● 高Al含有の新コーティング膜は、新組成系の採用と組織の適正化により、耐摩耗性と耐チッ インサート Insert:EPNW0603TN-8
耐チッピング性に ・Hardened steels (50 to 60 HRC): SKD11, SKD61, SKH, SUS420, etc.
切削条件 Cutting conditions:
ピング性を改善! 優れたコーティング vc=80m/min fz=0.2mm/t ap×ae=0.5×21mm
Coating with excellent wear 乾式加工 Dry ※単一刃加工 Single-flute cutting
● 耐溶着性に優れた低摩擦効果のコーティング最表層を採用。被削材の溶着が低減し切削 resistance and
chipping resistance
抵抗が低下!
・The new layer with high Al content employs a new composition and optimizes the structure to improve wear 超硬母材 Carbide
resistance and chipping resistance!
・Employs a low-friction-effect coating with excellent welding resistance as the top-most surface layer. This
reduces welding to the work and decreases cutting force!
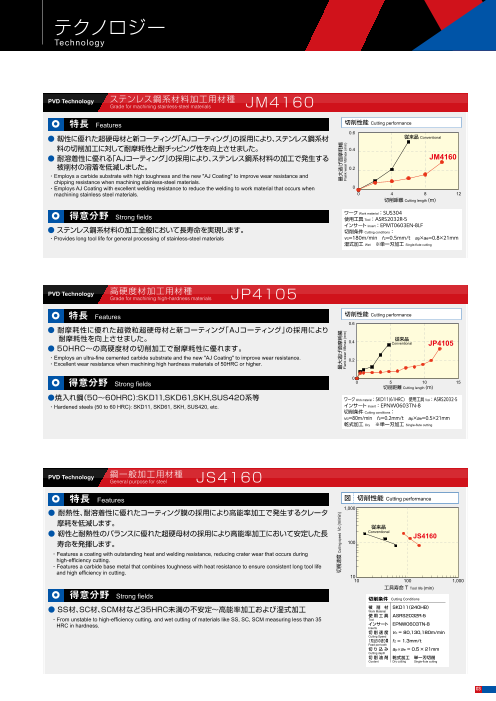
PVD Technology 鋼一般加工用材種
General purpose for steel JS4160
PVD Technology プリハードン鋼・焼入れ鋼加工用材種 特長 Features 図 切削性能 Cutting performance
Grade for machining pre-hardened or hardened materials JP4120
1,000
● 耐熱性、耐溶着性に優れたコーティング膜の採用により高能率加工で発生するクレータ
特長 Features 切削性能 Cutting performance 摩耗を低減します。 従来品
● 耐摩耗性と靱性のバランスに優れた微粒超硬母材と新コーティング「AJコーティング」の 0.6
従来品B ● 靭性と耐熱性のバランスに優れた超硬母材の採用により高能率加工において安定した長 Conventional
JS4160
Conventional B
採用により耐摩耗性と耐チッピング性を向上させました。 寿命を発揮します。 100
従来品A JP4120
● 汎用性が高く、35~50HRCの鋼材の切削加工で耐摩耗性と耐チッピング性に優れます。 0.4 Conventional A 従来品C ・Features a coating with outstanding heat and welding resistance, reducing crater wear that occurs during
Conventional C
・Employs a fine carbide substrate with an excellent balance between wear resistance and toughness and the new high-efficiency cutting.
"AJ Coating" to provide improved wear resistance and chipping resistance. ・Features a carbide base metal that combines toughness with heat resistance to ensure consistent long tool life
0.2
・ Highly versatile with excellent wear resistance and chipping resistance when machining steel materials with and high efficiency in cutting.
10
hardnesses of 35 to 50 HRC. 10 100 1,000
0 工具寿命T Tool life (min)
0 10 20 30 40 50 60
得意分野 切削距離 Cutting length (m) 得意分野 Strong fields
Strong fields 切削条件 Cutting Conditions
ワーク Work material:P21(40HRC) ● SS材、SC材、SCM材など35HRC未満の不安定~高能率加工および湿式加工 被 削 材 SKD11(240HB)
Work Material
● 35~50HRCのプリハードン鋼・焼入れ鋼の切削加工において優れた切削性能を発揮します。 使用工具 Tool:ASRT5063R-4 使用工具 ASRS2032R-5
インサート ・From unstable to high-efficiency cutting, and wet cutting of materials like SS, SC, SCM measuring less than 35 Tool
● 難削系のダイカスト金型用鋼や析出硬化系ステンレス鋼、仕上げ加工においても優れた耐 Insert:WDNW140520
切削条件 HRC in hardness. インサート EPNW0603TN-8
Cutting conditions: Inserts
摩耗性を発揮します。 vc=90m/min fz=0.8mm/t ap×ae=1×44mm 切 削 速 度 vc = 80,130,180m/min
Cutting Speed
・Exhibits excellent cutting performance when machining pre-hardened or hardened steels with hardnesses of 35 to 乾式加工 Dry ※単一刃加工 Single-flute cutting 1刃当りの送り量 fz = 1.3mm/t
Feed per tooth
50 HRC. 切り込 み ap×ae = 0.5 × 21mm
・ Exhibits excellent wear resistance even on difficult-to-cut diecast tool steels or precipitation-hardened stainless Cutting depth
切 削 油 剤 乾式加工 単一刃切削
steels, or for finishing. Coolant Dry cutting Single-flute cutting
02
最大逃げ面摩耗幅
Flank wear VBmax (mm)
切削速度 Cutting speed Vc (m/min) 最大逃げ面摩耗幅 最大逃げ面摩耗幅
Flank wear VBmax (mm) Flank wear VBmax (mm)
Page3
深彫り加工に テクノロジー
Technology
威力を発揮!
Powerful to Deep Milling
直彫り加工のエース PVD Technology ステンレス鋼系材料加工用材種
Ace Of The Direct Milling Grade for machining stainless-steel materials JM4160
三次元荒加工に好適! 特長 Features 切削性能 Cutting performance
0.6
従来品 Conventional
Suitable For Three-dimensional Rough Milling ● 靱性に優れた超硬母材と新コーティング「AJコーティング」の採用により、ステンレス鋼系材
料の切削加工に対して耐摩耗性と耐チッピング性を向上させました。 0.4
● 耐溶着性に優れる「AJコーティング」の採用により、ステンレス鋼系材料の加工で発生する JM4160
被削材の溶着を低減しました。 0.2
・Employs a carbide substrate with high toughness and the new "AJ Coating" to improve wear resistance and
chipping resistance when machining stainless-steel materials.
・ Employs AJ Coating with excellent welding resistance to reduce the welding to work material that occurs when 0
machining stainless steel materials. 0 4 8 12
切削距離 Cutting length (m)
標準形状 ブレーカ形状 ワーク Work material:SUS304
Standard shape Breaker Shape 得意分野 Strong fields 使用工具 Tool:ASRS2032R-5
インサート Insert:EPMT0603EN-8LF
● ステンレス鋼系材料の加工全般において長寿命を実現します。 切削条件 Cutting conditions:
・Provides long tool life for general processing of stainless-steel materials vc=180m/min fz=0.5mm/t ap×ae=0.8×21mm
不安定加工 湿式加工 Wet ※単一刃加工 Single-flute cutting
Unstable machining JS4160 JP4120 JM4160 荒
安定加工 JP4105 JP4120 JP4120 加工
Stable machining 用途 Roughing
炭素鋼 合金鋼 プリハードン鋼 焼入れ鋼 焼入れ鋼 ステンレス鋼 鋳鉄 Applications
合金鋼 (焼入れ焼戻し材) 合金鋼 (55HRC以下)(62HRC以下) SUS FC・FCD
(30HRC以下)(35HRC以下)(焼入れ焼戻し材)
(45HRC以下)
Carbon steels Alloy steels Pre-hardened steels Hardened steels Hardened steels Stainless steels Cast irons
Alloy steels (Quenched and tempered steels) Alloy steels (55HRC or less)(62HRC or less)
(30HRC or less) (35HRC or less)(Quenched and tempered steels) PVD Technology 高硬度材加工用材種
(45HRC or less) Grade for machining high-hardness materials JP4105
AJコーティングシリーズ AJ Coating series JP4120 JP4105 JM4160 特長 Features 切削性能 Cutting performance
0.6
● 耐摩耗性に優れた超微粒超硬母材と新コーティング「AJコーティング」の採用により
AJコーティングシリーズの特長 Features of AJ Coating series 皮膜の組織 AJコーティング 耐摩耗性を向上させました。
Layer structure 0.4 従来品
AJ Coating Conventional JP4105
● 従来膜よりもAl含有量を増加した新組成系のAlTiN系皮膜を採用。 ● 50HRC~の高硬度材の切削加工で耐摩耗性に優れます。
皮膜構造 Coating structure 耐溶着性・低抵抗 ・Employs an ultra-fine cemented carbide substrate and the new "AJ Coating" to improve wear resistance.
● 耐摩耗性・耐チッピング性および耐熱性に優れる! 0.2
コーティング表層 ・Excellent wear resistance when machining high hardness materials of 50HRC or higher.
・Employs an AlTiN layer with a new composition created by increasing the Al content of conventional layers. Welding-resistant and
・Excellent wear resistance, chipping resistance, and heat resistance! low-cutting-force coating
surface layer 得意分野 0
Strong fields 0 5 10 15
切削距離 Cutting length (m)
新技術!! New technology!! ●焼入れ鋼(50~60HRC):SKD11,SKD61,SKH,SUS420系等 ワーク Work material:SKD11(61HRC) 使用工具 Tool:ASRS2032-5
耐摩耗性・
● 高Al含有の新コーティング膜は、新組成系の採用と組織の適正化により、耐摩耗性と耐チッ インサート Insert:EPNW0603TN-8
耐チッピング性に ・Hardened steels (50 to 60 HRC): SKD11, SKD61, SKH, SUS420, etc.
切削条件 Cutting conditions:
ピング性を改善! 優れたコーティング vc=80m/min fz=0.2mm/t ap×ae=0.5×21mm
Coating with excellent wear 乾式加工 Dry ※単一刃加工 Single-flute cutting
● 耐溶着性に優れた低摩擦効果のコーティング最表層を採用。被削材の溶着が低減し切削 resistance and
chipping resistance
抵抗が低下!
・The new layer with high Al content employs a new composition and optimizes the structure to improve wear 超硬母材 Carbide
resistance and chipping resistance!
・Employs a low-friction-effect coating with excellent welding resistance as the top-most surface layer. This
reduces welding to the work and decreases cutting force!
PVD Technology 鋼一般加工用材種
General purpose for steel JS4160
PVD Technology プリハードン鋼・焼入れ鋼加工用材種 特長 Features 図 切削性能 Cutting performance
Grade for machining pre-hardened or hardened materials JP4120
1,000
● 耐熱性、耐溶着性に優れたコーティング膜の採用により高能率加工で発生するクレータ
特長 Features 切削性能 Cutting performance 摩耗を低減します。 従来品
● 耐摩耗性と靱性のバランスに優れた微粒超硬母材と新コーティング「AJコーティング」の 0.6
従来品B ● 靭性と耐熱性のバランスに優れた超硬母材の採用により高能率加工において安定した長 Conventional
JS4160
Conventional B
採用により耐摩耗性と耐チッピング性を向上させました。 寿命を発揮します。 100
従来品A JP4120
● 汎用性が高く、35~50HRCの鋼材の切削加工で耐摩耗性と耐チッピング性に優れます。 0.4 Conventional A 従来品C ・Features a coating with outstanding heat and welding resistance, reducing crater wear that occurs during
Conventional C
・Employs a fine carbide substrate with an excellent balance between wear resistance and toughness and the new high-efficiency cutting.
"AJ Coating" to provide improved wear resistance and chipping resistance. ・Features a carbide base metal that combines toughness with heat resistance to ensure consistent long tool life
0.2
・ Highly versatile with excellent wear resistance and chipping resistance when machining steel materials with and high efficiency in cutting.
10
hardnesses of 35 to 50 HRC. 10 100 1,000
0 工具寿命T Tool life (min)
0 10 20 30 40 50 60
得意分野 切削距離 Cutting length (m) 得意分野 Strong fields
Strong fields 切削条件 Cutting Conditions
ワーク Work material:P21(40HRC) ● SS材、SC材、SCM材など35HRC未満の不安定~高能率加工および湿式加工 被 削 材 SKD11(240HB)
Work Material
● 35~50HRCのプリハードン鋼・焼入れ鋼の切削加工において優れた切削性能を発揮します。 使用工具 Tool:ASRT5063R-4 使用工具 ASRS2032R-5
インサート ・From unstable to high-efficiency cutting, and wet cutting of materials like SS, SC, SCM measuring less than 35 Tool
● 難削系のダイカスト金型用鋼や析出硬化系ステンレス鋼、仕上げ加工においても優れた耐 Insert:WDNW140520
切削条件 HRC in hardness. インサート EPNW0603TN-8
Cutting conditions: Inserts
摩耗性を発揮します。 vc=90m/min fz=0.8mm/t ap×ae=1×44mm 切 削 速 度 vc = 80,130,180m/min
Cutting Speed
・Exhibits excellent cutting performance when machining pre-hardened or hardened steels with hardnesses of 35 to 乾式加工 Dry ※単一刃加工 Single-flute cutting 1刃当りの送り量 fz = 1.3mm/t
Feed per tooth
50 HRC. 切り込 み ap×ae = 0.5 × 21mm
・ Exhibits excellent wear resistance even on difficult-to-cut diecast tool steels or precipitation-hardened stainless Cutting depth
切 削 油 剤 乾式加工 単一刃切削
steels, or for finishing. Coolant Dry cutting Single-flute cutting
03
最大逃げ面摩耗幅
Flank wear VBmax (mm)
切削速度 Cutting speed Vc (m/min) 最大逃げ面摩耗幅 最大逃げ面摩耗幅
Flank wear VBmax (mm) Flank wear VBmax (mm)
Page4
ラインナップ
Line Up
シャンクタイプ AR (R ) は数字、 は英文字が入ります。
Shank type Numeric figure in a circle and alphabetical character comes in a square . モジュラータイプ Modular Type ARM R- は数字が入ります。 Numeric figure in a circle .
LF THSZMS DRVS(二面幅)
r LH LS
LF
r LH LS
Fig.1 Fig.2 LF
商品コード 在庫 刃数 寸 法 Size(mm)
No.of 形状 適用インサート 備考
Item code Stock flutes DCX DC LF DCONMS r LH LS D3 Shape Inserts Note
L1
RDHW0802M0TN r L2
※ARS0020R ● 2 20 12 130 20 4 50 80 18 RDMT0802M0TN
RDMT0802M0EN 商品コード 在庫 刃数 寸 法 Size(mm) 適用インサート 備考
※ARS3025R ● 2 25 15 140 25 5 60 80 21 Fig.1 Item code Stock No.of
RDHW10T3M0TN flutes DCX r LF DCONMS THSZMS DHUB L1 L2 DRVS Inserts Note
※ARS3030R ● 3 30 20 150 32 5 70 80 26 RDMT10T3M0TN
RDMT10T3M0EN ※1 ARM0512R-2 ● 2 12 2.5 20 6.5 M6 9.8 5.5 14.5 7
レ ※ARS3032R ● 3 32 22 150 32 5 70 80 28 RDMW0501M0EN
ギ ※1
ュ ARM0512R-3 ● 3 12 2.5 20 6.5 M6 9.8 5.5 14.5 7
※ARS4040R ● 3 40 28 150 32 6 50 100 35
ラ RDHW1204M0TN
ー ※ARS4050R ● 3 50 38 150 32 6 50 100 45 RDMT1204M0TN ARM0716R-2 ● 2 16 3.5 25 8.5 M8 12.8 5.5 17 10 RDMW0702M0EN
RDMT1204M0EN
※ARS4050R42 ● 4 50 38 150 42 6 50 100 45 ARM0020R-2 ● 2 20 4 30 10.5 M10 17.8 5.5 19 15 RDHW0802M0TN
ARS5040R ● 2 40 24 150 32 8 50 100 35 RDMT0802M0TN
Fig.2 ※ ARM0022R-2 ● 2 22 4 30 10.5 M10 17.8 5.5 19 15 RDMT0802M0EN
ARS5050R ● 3 50 34 150 32 8 50 100 44 RDHW1604M0TN
ス RDMX1604M0TN ARM3025R-2 ● 2 25 5 35 12.5 M12 20.8 5.5 22 17
ト ARS5050R42 ● 3 50 34 150 42 8 50 100 44 RDMX1604M0EN
レ RDMT1604M0TN
● 3 63 47 150 32 8 50 100 58 RDMT1604M0EN ※ ARM3028R-2 ● 2 28 5 35 12.5 M12 23 5.5 22 17
ー ARS5063R
ト ARS5063R42 ● 3 63 47 150 42 8 50 100 58 ARM3030R-3 ● 3 30 5 40 17 M16 28.8 6 23 22 RDHW10T3M0TN
シ
ャ RDHW0802M0TN RDMT10T3M0TN
ン ※ARL0020R ● 2 20 12 180 20 4 100 80 18 RDMT0802M0TN ARM3032R-2 ● 2 32 5 40 17 M16 28.8 6 23 22 RDMT10T3M0EN
ク
タ RDMT0802M0EN
イ ※ARL3025R ● 2 25 15 200 25 5 120 80 21 ARM3032R-3 ● 3 32 5 40 17 M16 28.8 6 23 22
プ Fig.1 RDHW10T3M0TN
※ARL3030R ● 3 30 20 200 32 5 120 80 26 RDMT10T3M0TN ※ ARM3040R-4 ● 4 40 5 40 17 M16 28.8 6 23 22
ロ
ン RDMT10T3M0EN
※ARL3032R ● 3 32 22 200 32 5 120 80 28 【注意】 ①※と超硬シャンクをセットで使用すると干渉がありません。②※1工具径(DCX)がφ12の場合はエアー穴が付いておりません。
グ
※ARL4032R ● 2 32 20 250 32 6 150 100 28 ③モジュラーミル及び専用シャンク、専用アーバの「工具端面」「モジュラーねじ部」にグリースなどの潤滑剤は塗布しないでください。
RDHW1204M0TN 【Note】 ①When ※ and carbide shank are used together as a set, there is no interference. ②※1 with tool dia. (DCX) of φ12 do not have air holes.
※ARL4040R ● 3 40 28 250 32 6 50 200 35 RDMT1204M0TN ③Do not apply lubricants such as grease, etc. to the “contact faces” and “modular screws” of the “modular mill”, “dedicated shanks” and “dedicated arbor”.
RDMT1204M0EN
※ARL4050R42 ● 4 50 38 250 42 6 50 200 45
ARL5040R ● 2 40 24 250 32 8 50 200 35 Fig.2 RDHW1604M0TN
RDMX1604M0TN 部品番号 Parts は数字が入ります。 Numeric figure in a circle .
ARL5050R42 ● 3 50 34 250 42 8 50 200 44 RDMX1604M0EN
RDMT1604M0TN
ARL5063R42 ● 3 63 47 250 42 8 50 200 58 部品名 クランプねじ クランプ駒セット ドライバー ねじ焼き付き防止剤
RDMT1604M0EN Parts Clamp screw Clamp piece set Screw Driver Screw anti-seizure agent
RDHW0802M0TN
エ ※ARE0020R ● 2 20 12 250 20 4 130 120 18 RDMT0802M0TN 形状
キ RDMT0802M0EN Shape
ス 締付トルク
ト ※ARE3025R ● 2 25 15 300 25 5 180 120 21 Fastening
適用カッタ torque
ラ Fig.1 RDHW10T3M0TN Cutter body (N・m)
ロ ※ARE3030R ● 2 30 20 300 32 5 180 120 26 RDMT10T3M0TN
ン RDMT10T3M0EN ARM0512R- 240-140 0.4 - 104-T6
グ ※ARE3032R ● 3 32 22 300 32 5 180 120 28 ARM0716R-2 250-141 1.1 - 104-T8
※ARE4032R ● 2 32 20 300 32 6 180 120 28
RDHW1204M0TN ARM0020R-2 T8
※ARE4040R ● 2 40 28 300 32 6 50 250 35 RDMT1204M0TN ARM0022R-2 261-140 1.1 CM3.5-141 104-
104-T15
Fig.2 RDMT1204M0EN ARM3025R-2 P-37
※ARE4050R42 ● 2 50 38 300 42 6 50 250 45 ARM3028R-2
※:エアー穴付き。※:With air-hole. ARM3030R-3 501-161 2.9 CM3.5-141 104-T15
ARM3032R-
部品番号 ARM3040R-4
Parts
部品名 クランプねじ プ駒セット クランプ駒 クランプねじ
Parts (インサート用) クラン
Clamp screw for Inserts Clamp piece set Clamp piece (クランプ駒用) バネ ドライバー/レンチ
Clamp screw for clamp piece Spring Screw driver/Wrench
形状 締付
Shape トルク
適用カッタ Fastening
torque
Cutter body 形状
(N・m) A B Shape
ARS/L/E0020R 261-140 1.1 CM3.5-141 104-T8 A
ARS/L/E3025R~ARS/L/E3032R 501-161 2.9 CM3.5-141 104-T15 A
ARS/L/E4032R~ARS/L/E4050R(42) 262-142 2.9 CM4-141 104-T15 A
ARS/L5040R~ARS/L5063R(42) 223-141 4.9 215-192 200-150 715-201 105-T20 B
【注意】 クランプねじは消耗品です。使用環境により交換寿命は変化しますので早めの交換をお願い致します。
04 【Note】 The clamp screw is a consumable part. Since replacement life depends on the use environment, it is recommended that it be replaced at an early stage.
●印:標準在庫品です。●:Stocked Items.
Straight shank type
Extra Long Long Regular
DCX
DC
D3
DCONMS
DCX
DC
D3
DCONMS
DCX
DCONMS
DHUB
Page5
ラインナップ
Line Up
シャンクタイプ AR (R ) は数字、 は英文字が入ります。
Shank type Numeric figure in a circle and alphabetical character comes in a square . モジュラータイプ Modular Type ARM R- は数字が入ります。 Numeric figure in a circle .
LF THSZMS DRVS(二面幅)
r LH LS
LF
r LH LS
Fig.1 Fig.2 LF
商品コード 在庫 刃数 寸 法 Size(mm)
No.of 形状 適用インサート 備考
Item code Stock flutes DCX DC LF DCONMS r LH LS D3 Shape Inserts Note
L1
RDHW0802M0TN r L2
※ARS0020R ● 2 20 12 130 20 4 50 80 18 RDMT0802M0TN
RDMT0802M0EN 商品コード 在庫 刃数 寸 法 Size(mm) 適用インサート 備考
※ARS3025R ● 2 25 15 140 25 5 60 80 21 Fig.1 Item code Stock No.of
RDHW10T3M0TN flutes DCX r LF DCONMS THSZMS DHUB L1 L2 DRVS Inserts Note
※ARS3030R ● 3 30 20 150 32 5 70 80 26 RDMT10T3M0TN
RDMT10T3M0EN ※1 ARM0512R-2 ● 2 12 2.5 20 6.5 M6 9.8 5.5 14.5 7
レ ※ARS3032R ● 3 32 22 150 32 5 70 80 28 RDMW0501M0EN
ギ ※1
ュ ARM0512R-3 ● 3 12 2.5 20 6.5 M6 9.8 5.5 14.5 7
※ARS4040R ● 3 40 28 150 32 6 50 100 35
ラ RDHW1204M0TN
ー ※ARS4050R ● 3 50 38 150 32 6 50 100 45 RDMT1204M0TN ARM0716R-2 ● 2 16 3.5 25 8.5 M8 12.8 5.5 17 10 RDMW0702M0EN
RDMT1204M0EN
※ARS4050R42 ● 4 50 38 150 42 6 50 100 45 ARM0020R-2 ● 2 20 4 30 10.5 M10 17.8 5.5 19 15 RDHW0802M0TN
ARS5040R ● 2 40 24 150 32 8 50 100 35 RDMT0802M0TN
Fig.2 ※ ARM0022R-2 ● 2 22 4 30 10.5 M10 17.8 5.5 19 15 RDMT0802M0EN
ARS5050R ● 3 50 34 150 32 8 50 100 44 RDHW1604M0TN
ス RDMX1604M0TN ARM3025R-2 ● 2 25 5 35 12.5 M12 20.8 5.5 22 17
ト ARS5050R42 ● 3 50 34 150 42 8 50 100 44 RDMX1604M0EN
レ RDMT1604M0TN
● 3 63 47 150 32 8 50 100 58 RDMT1604M0EN ※ ARM3028R-2 ● 2 28 5 35 12.5 M12 23 5.5 22 17
ー ARS5063R
ト ARS5063R42 ● 3 63 47 150 42 8 50 100 58 ARM3030R-3 ● 3 30 5 40 17 M16 28.8 6 23 22 RDHW10T3M0TN
シ
ャ RDHW0802M0TN RDMT10T3M0TN
ン ※ARL0020R ● 2 20 12 180 20 4 100 80 18 RDMT0802M0TN ARM3032R-2 ● 2 32 5 40 17 M16 28.8 6 23 22 RDMT10T3M0EN
ク
タ RDMT0802M0EN
イ ※ARL3025R ● 2 25 15 200 25 5 120 80 21 ARM3032R-3 ● 3 32 5 40 17 M16 28.8 6 23 22
プ Fig.1 RDHW10T3M0TN
※ARL3030R ● 3 30 20 200 32 5 120 80 26 RDMT10T3M0TN ※ ARM3040R-4 ● 4 40 5 40 17 M16 28.8 6 23 22
ロ
ン RDMT10T3M0EN
※ARL3032R ● 3 32 22 200 32 5 120 80 28 【注意】 ①※と超硬シャンクをセットで使用すると干渉がありません。②※1工具径(DCX)がφ12の場合はエアー穴が付いておりません。
グ
※ARL4032R ● 2 32 20 250 32 6 150 100 28 ③モジュラーミル及び専用シャンク、専用アーバの「工具端面」「モジュラーねじ部」にグリースなどの潤滑剤は塗布しないでください。
RDHW1204M0TN 【Note】 ①When ※ and carbide shank are used together as a set, there is no interference. ②※1 with tool dia. (DCX) of φ12 do not have air holes.
※ARL4040R ● 3 40 28 250 32 6 50 200 35 RDMT1204M0TN ③Do not apply lubricants such as grease, etc. to the “contact faces” and “modular screws” of the “modular mill”, “dedicated shanks” and “dedicated arbor”.
RDMT1204M0EN
※ARL4050R42 ● 4 50 38 250 42 6 50 200 45
ARL5040R ● 2 40 24 250 32 8 50 200 35 Fig.2 RDHW1604M0TN
RDMX1604M0TN 部品番号 Parts は数字が入ります。 Numeric figure in a circle .
ARL5050R42 ● 3 50 34 250 42 8 50 200 44 RDMX1604M0EN
RDMT1604M0TN
ARL5063R42 ● 3 63 47 250 42 8 50 200 58 部品名 クランプねじ クランプ駒セット ドライバー ねじ焼き付き防止剤
RDMT1604M0EN Parts Clamp screw Clamp piece set Screw Driver Screw anti-seizure agent
RDHW0802M0TN
エ ※ARE0020R ● 2 20 12 250 20 4 130 120 18 RDMT0802M0TN 形状
キ RDMT0802M0EN Shape
ス 締付トルク
ト ※ARE3025R ● 2 25 15 300 25 5 180 120 21 Fastening
適用カッタ torque
ラ Fig.1 RDHW10T3M0TN Cutter body (N・m)
ロ ※ARE3030R ● 2 30 20 300 32 5 180 120 26 RDMT10T3M0TN
ン RDMT10T3M0EN ARM0512R- 240-140 0.4 - 104-T6
グ ※ARE3032R ● 3 32 22 300 32 5 180 120 28 ARM0716R-2 250-141 1.1 - 104-T8
※ARE4032R ● 2 32 20 300 32 6 180 120 28
RDHW1204M0TN ARM0020R-2 T8
※ARE4040R ● 2 40 28 300 32 6 50 250 35 RDMT1204M0TN ARM0022R-2 261-140 1.1 CM3.5-141 104-
104-T15
Fig.2 RDMT1204M0EN ARM3025R-2 P-37
※ARE4050R42 ● 2 50 38 300 42 6 50 250 45 ARM3028R-2
※:エアー穴付き。※:With air-hole. ARM3030R-3 501-161 2.9 CM3.5-141 104-T15
ARM3032R-
部品番号 ARM3040R-4
Parts
【注意】 クランプねじは消耗品です。使用環境により交換寿命は変化しますので早めの交換をお願い致します。
部品名 クランプねじ プ駒セット クランプ駒 クランプねじ 【Note】 The clamp screw is a consumable part. Since replacement life depends on the use environment, it is recommended that it be replaced at an early stage.
Parts (インサート用) クラン
Clamp screw for Inserts Clamp piece set Clamp piece (クランプ駒用) バネ ドライバー/レンチ
Clamp screw for clamp piece Spring Screw driver/Wrench
形状 締付
Shape トルク
適用カッタ Fastening
torque
Cutter body 形状
(N・m) A B Shape
ARS/L/E0020R 261-140 1.1 CM3.5-141 104-T8 A
ARS/L/E3025R~ARS/L/E3032R 501-161 2.9 CM3.5-141 104-T15 A
ARS/L/E4032R~ARS/L/E4050R(42) 262-142 2.9 CM4-141 104-T15 A
ARS/L5040R~ARS/L5063R(42) 223-141 4.9 215-192 200-150 715-201 105-T20 B
05
Straight shank type
Extra Long Long Regular
DCX
DC
D3
DCONMS
DCX
DC
D3
DCONMS
DCX
DCONMS
DHUB
Page6
ラインナップ
Line Up
ボアタイプ Bore type ARB R-(M)AR5 R は数字が入ります。Numeric figure in a circle . インサート Inserts は数字が入ります。Numeric figure in a circle .
DHUB DHUB
2.38 3.97
DCONMS DCONMS 1.59 2.38
KWW KWW
M8 M10 Fig.11 15° Fig.12 15° Fig.13 15° Fig.14 15°
DCCB DCCB
4.76 5.56
DC r DC 4.76
r 8 25
DCX DCX 10 25
Fig.3 Fig.4 Fig.5 Fig.6
M16 M20 Fig.15 15° Fig.16 15° Fig.17 15°
M10 ブレーカなし ブレーカ付き
M16 Breakerless With breaker
14 35 10 35
10 30 14 36
Fig.7 Fig.8 100-211 Fig.9 Fig.10 600-211
商品コード 在庫 刃数 寸 法 Size(mm)
No.of 形状 適用インサート 備考
Item code Stock flutes DCX DC DHUB r LF DCONMS DCCB KWW b CBDP アーバ用ねじ Shape Inserts Note
Arbor screw
ARB4040R-3 ● 3 40 28 32 6 50 16 13.5 8.4 5.6 19 M8×25
(Fig.5)
ARB4050R-3 ● 3 50 38 48 6 50 22.225 17 8.4 5 19 M10×25
(Fig.6)
ARB4050R-5 ● 5 50 38 48 6 50 22.225 17 8.4 5 19 M10×25
(Fig.6)
ARB4050R-3M ● 3 50 38 48 6 50 22 17 10.4 6.3 20 M10×25
(Fig.6)
ARB4050R-5M ● 5 50 38 48 6 50 22 17 10.4 6.3 20 M10×25
(Fig.6)
ARB4063R-4 ● 4 63 51 61 6 50 22.225 17 8.4 5 19 M10×25
(Fig.6) Fig.3
最 ARB4063R-6 ● 6 63 51 6 50 22.225 17 8.4 5 19 M10×25 RDHW1204M0TN
61 (Fig.6) RDMT1204M0TN
M10×25 RDMT1204M0EN
外 ARB4063R-4M ● 4 63 51 61 6 50 22 17 10.4 6.3 20 (Fig.6)
ボ径 ● 6 51 61 6 50 22 17 10.4 6.3 20 M10×25
(Fig.6)
アタ ARB4063R-6M 63
タイ ARB4080R-4 ● 4 80 68 76 6 70 31.75 26 12.7 8 32 M16×35
(Fig.7)
イプ
●
プ ARB4080R-6 6 80 68 76 6 70 31.75 26 12.7 8 32 M16×35
(Fig.7)
ARB4100R-5 ● 5 100 88 96 6 70 31.75 26 12.7 8 32 M16×35
(Fig.7)
ARB4125R-6 ● 6 125 113 102 6 70 38.1 55 15.9 10 38 M20
(Fig.10) Fig.4
ARB5063R-3 ● 3 63 47 61 8 50 22.225 17 8.4 5 19 M10×25
(Fig.6)
ARB5080R-4 ● 4 80 64 76 8 70 31.75 26 12.7 8 32 M16×35
(Fig.7) Fig.3 RDHW1605M0TN
ARB5100R-5 ● 5 100 M16×35 RDMT1605M0TN
84 96 8 70 31.75 26 12.7 8 32 (Fig.7) RDMT1605M0EN
ARB5125R-6 ● 6 125 109 102 8 70 38.1 55 15.9 10 38 M20
(Fig.10) Fig.4
先 AR5047R ● 3 63 47 47 8 47 22.225 16.5 8.4 5 19 M10
(Fig.8)
端 M16 Fig.3 RDHW1604M0TN
径 AR5080R ● 4 96 80 65 8 63 31.75 43 12.7 8 32 (Fig.9) RDMX1604M0TN
タ ● M20 RDMX1604M0EN
イ AR5100R 5 116 100 85 8 63 38.1 53 15.9 10 38 (Fig.10) RDMT1604M0TN
Fig.4
プ AR5125R ● 6 141 125 85 8 63 38.1 60 15.9 10 38 M20 RDMT1604M0EN
(Fig.10)
【注意】カッタ取付のアーバ用ねじは、カッタ本体には付属しておりません。例外として、AR5047Rはアーバ用ねじ(100-211)が付属致します。
【Note】Arbor screws are not included with the cutter body. AR5047R exceptionally has arbor screws (100-211).
部品番号 Parts は数字が入ります。Numeric figure in a circle .
部品名 クランプねじ
Parts (インサート用) クランプ駒セット クランプ駒 クランプねじ バネ レンチ ねじ焼き付き防止剤
Clamp screw for inserts Clamp piece set Clamp piece (クランプ駒用)
Clamp screw for clamp piece Spring Wrench Screw anti-seizure agent
形状
Shape 締付
トルク
適用カッタ Fastening
Cutter body torque
(N・m)
ARB4 R- (M) 262-142 2.9 CM4-141 105-T15
ARB5 R- 263-141 4.9 CM5-147 105-T20 P-37
AR5 R 223-141 4.9 215-192 200-150 715-201 105-T20
【注意】 クランプねじは消耗品です。使用環境により交換寿命は変化しますので早めの交換をお願い致します。
【Note】 The clamp screw is a consumable part. Since replacement life depends on the use environment, it is recommended that it be replaced at an early stage.
★印:新商品の標準在庫品です。 ●印:標準在庫品です。 △印:在庫がなくなり次第販売を終了します。
06 ★:Stocked Items of New products. ●:Stocked Items. △:The sale ends when all the stock is out.
Bore type
Tip end type Outside diameter type
24 b
CBDP
LF
16
b
CBDP
40
LF
13
50
16
12
5
7
16
8
16
10
Page7
ラインナップ
Line Up
ボアタイプ Bore type ARB R-(M)AR5 R は数字が入ります。Numeric figure in a circle . インサート Inserts は数字が入ります。Numeric figure in a circle .
DHUB DHUB
DCONMS DCONMS 2.38 3.97
1.59 2.38
KWW KWW
M8 M10 Fig.11 15° Fig.12 15° Fig.13 15° Fig.14 15°
DCCB DCCB
4.76 5.56
DC 4.76
r DC r 8 25
DCX DCX 10 25
Fig.3 Fig.4 Fig.5 Fig.6
M16 M20 Fig.15 15° Fig.16 15° Fig.17 15° ブレーカなし ブレーカ付き
M16 M10
Breakerless With breaker
炭素鋼・合金鋼(30HRC以下)
Carbon steels, Alloy steels(30HRC or less)
合金鋼(焼入れ焼戻し材)(35HRC以下)
14 35 10 35
10 30 14 36 Alloy steels(Quenched and tempered steels)
Fig.7 Fig.8 100-211 Fig.9 Fig.10 600-211 P(35HRC or less)
プリハードン鋼・合金鋼
商品コード 在庫 刃数 寸 法 Size(mm) (焼入れ焼戻し材)(45HRC以下) :一般切削・第一推奨
No.of 形状 適用インサート 備考
Item code Stock Pre-hardened steels, Alloy steels General cutting, First recommendation
flutes DCX DC DHUB r LF DCONMS DCCB KWW b CBDP アーバ用ねじ Shape Inserts Note
Arbor screw (Quenched and tempered steels)(45HRC or less) :一般切削・第二推奨
ARB4040R-3 ● 3 40 28 32 6 50 16 13.5 8.4 5.6 19 M8×25 M ステンレス鋼 Stainless steels SUS General cutting, Second recommendation
(Fig.5)
ARB4050R-3 ● 3 50 38 48 6 50 22.225 17 8.4 5 19 M10×25 K 鋳鉄 Cast irons FC・FCD
(Fig.6)
焼入れ鋼(55HRC以下)
ARB4050R-5 ● 5 50 38 48 6 50 22.225 17 8.4 5 19 M10×25
(Fig.6) H Hardened steels(55HRC or less)
ARB4050R-3M ● 3 50 38 48 6 50 22 17 10.4 6.3 20 M10×25 焼入れ鋼(62HRC以下)
(Fig.6) Hardened steels(62HRC or less)
ARB4050R-5M ● 5 50 38 48 6 50 22 17 10.4 6.3 20 M10×25
(Fig.6)
ARB4063R-4 ● 4 63 51 61 6 50 22.225 17 8.4 5 19 M10×25
(Fig.6) Fig.3
最 ARB4063R-6 ● 6 63 51 61 6 50 22.225 17 8.4 5 19 M10×25 RDHW1204M0TN
(Fig.6) RDMT1204M0TN
RDMT1204M0EN 商品コード 精度 形状 適用カッタ 備考
外 ARB4063R-4M ● 4 63 51 61 6 50 22 17 10.4 6.3 20 M10×25 Item code Tolerance
(Fig.6) class Shape Cutter body Note
ボ径
タ ARB4063R-6M ● 6 63 51 61 6 50 22 17 10.4 6.3 20 M10×25
(Fig.6)
ア
タイ ARB4080R-4 ● 4 80 68 76 6 70 31.75 26 12.7 8 32 M16×35
(Fig.7)
イプ
プ ARB4080R-6 ● 6 80 68 76 6 70 31.75 26 12.7 8 32 M16×35
(Fig.7) RDMW0501M0EN M級 ブレーカなし ※ 512R-2
M breakerless ● ● ● ● Fig-11 ARM0
ARM0512R-3
ARB4100R-5 ● 5 100 88 96 6 70 31.75 26 12.7 8 32 M16×35
(Fig.7) RDMW0702M0EN M級 ブレーカなし
ARB4125R-6 ● 6 125 113 102 6 70 38.1 55 15.9 10 38 M20 M breakerless ●※ ● ● ● Fig-12 ARM0716R-2
(Fig.10) Fig.4
ARB5063R-3 ● 3 63 47 61 8 50 22.225 17 8.4 5 19 M10×25 RDHW0802M0TN H級 ブレーカなし
(Fig.6) H breakerless ● △ ● AR 0020R
ARB5080R-4 ● 4 80 64 76 8 70 31.75 26 12.7 8 32 M16×35 RDMT0802M0TN
(Fig.7) Fig.3 RDHW1605M0TN M級 ブレーカ付き ● ● ● ★ △ △ ● Fig-13 ARM0020R-2
RDMT1605M0TN
ARB5100R-5 ● 5 100 84 96 8 70 31.75 26 12.7 8 32 M16×35 RDMT0802M0EN M with breaker ARM0022R-2
●
(Fig.7) RDMT1605M0EN
ARB5125R-6 ● 6 125 109 102 8 70 38.1 55 15.9 10 38 M20
(Fig.10) Fig.4 RDHW10T3M0TN H級 ブレーカなし
H breakerless ★ △ ●
先 AR5047R ● 3 63 47 47 8 47 22.225 16.5 8.4 5 19 M10
(Fig.8) Fig-14 AR 30 R
RDMT10T3M0TN
端 Fig.3 RDHW1604M0TN M級 ブレーカ付き ● ● ● ★ △ △ ● △ ARM30 R-
径 AR5080R ● 4 96 80 65 8 63 31.75 43 12.7 8 32 M16
(Fig.9) RDMX1604M0TN RDMT10T3M0EN M with breaker ● ●
タ RDMX1604M0EN
イ AR5100R ● 5 116 100 85 8 63 38.1 53 15.9 10 38 M20
(Fig.10) RDMT1604M0TN
Fig.4 RDHW1204M0TN H級 ブレーカなし
H breakerless ★ △ ●
プ AR5125R ● 6 141 125 85 8 63 38.1 60 15.9 10 38 M20 RDMT1604M0EN
(Fig.10) RDMT1204M0TN M級 ブレーカ付き ● ● ● ★ △ △ ● Fig-15 AR 40 R(42)
ARB4 R- (M)
【注意】カッタ取付のアーバ用ねじは、カッタ本体には付属しておりません。例外として、AR5047Rはアーバ用ねじ(100-211)が付属致します。 RDMT1204M0EN M with breaker
【Note】Arbor screws are not included with the cutter body. AR5047R exceptionally has arbor screws (100-211).
RDHW1604M0TN H級 ブレーカなし
H breakerless △ ●
部品番号 MT1604M0TN M級 ブレーカ付き ● ● ● ★ △ △ ● Fig-16 AR 50 R(42)
RD AR5 R
Parts は数字が入ります。Numeric figure in a circle . RDMT1604M0EN M with breaker ● ●
部品名 クランプねじ クランプ駒セット クランプ駒 クランプねじ ねじ焼き付き防止剤 RDHW1605M0TN H級 ブレーカなし
Parts (インサート用) H breakerless △ ●
Clamp screw for inserts Clamp piece set Clamp piece (クランプ駒用) バネ レンチ
Clamp screw for clamp piece Spring Wrench Screw anti-seizure agent
RDMT1605M0TN M級 ブレーカ付き ● ● ★ △ ● Fig-17 ARB5 R-
形状 RDMT1605M0EN M with breaker
Shape 締付
トルク ※ RDMW0501M0EN; JP4105、RDMW0702M0EN;JP4105の第二推奨被削材種は、P :鋼、K:FC・FCDになります。
適用カッタ Fastening Secondary recommended work material for RDMW0501M0EN: JP4105 and RDMW0702M0EN: JP4105 are P (steel) and K (FC, FCD).
Cutter body torque
(N・m) 【注意】JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。
ARB4 R- (M) 262-142 2.9 CM4-141 105-T15 【Note】Please note that the JS Coating does not cause a reaction in conductive touch sensors.
ARB5 R- 263-141 4.9 CM5-147 105-T20 P-37
AR5 R 223-141 4.9 215-192 200-150 715-201 105-T20
07
Bore type
Tip end type Outside diameter type
24 b
CBDP
LF
16
b
CBDP
40
LF
13
50
16
12
5
JP4105
JP4120 AJコーティング AJ Coating
JM4160 7
16
JS4160
JS4045 JSコーティング JS Coating
JS4060
PTH08M TH コーティング TH Coating
CY100H C コーティング
CY250 C Coating
GF30 G コーティング G Coating
8
WH10 超硬 16Carbide
10
Page8
ラインナップ
Line Up
モジュラーミル専用シャンク The Shanks for Modular Mill モジュラーミル用アーバ Modular Mill Arbor
■ 超硬シャンク Carbide Shank ■ 鋼シャンク Steel Shank ■ HSK LB2 26 32 ■ BT30
LB2 22 48.4
LF LF LB1 THSZWS
LB1 THSZWS
LB1 LS
LB1 LS
※首部は、ユーザ様にて追加工
可能です。
THSZWS For neck section, additional
BHTA2 HSK-A63 BHTA2 BT30 machining to user
Cタイプ C type THSZWS specifications is possible.
Bタイプ B type
商品コード 在庫 寸 法 Size(mm) エアー穴
有無 備考 商品コード 在庫 寸 法 Size(mm) エアー穴
有無
LF LF Item code Stock DCONWS THSZWS BD1 φDS LB2 LB1 BHTA2 With/without
air hole Note Item code Stock DCONWS THSZWS BD1 φDS LB2 LB1 BHTA2 With/without
air hole
LB1 LS
LB1 LS HSK-A63-10.5-30-18 ● 20.8 30 - 3° BT30-6.5-30-9.7 30 5 17°
HSK-A63-10.5-70-18 ● 10.5 M10 18 25 70 10 3° BT30-6.5-55-9.7 6.5 M6 9.7 25 55 10 9.6° -
HSK-A63-10.5-70-18S 48 70 10 12° BT30-6.5-80-9.7 80 10 6.2°
THSZWS HSK-A63-10.5-120-18 ● 30.2 120 10 3° BT30-8.5-25-15 25 5 20.6°
Eタイプ E type THSZWS HSK-A63-12.5-35-21 ● 24.3 35 - 3° BT30-8.5-50-15 8.5 M8 15 30 50 10 10.6° ○
HSK-A63-12.5-65-21 ● 12.5 M12 21 27.5 65 10 3° ○ BT30-8.5-75-15 75 10 6.6°
Cタイプ (首テ-パ) C type (Tapered neck)
エ HSK-A63-12.5-65-21S 48 65 10 12° BT30-10.5-20-18 20 5 29.5°
商品コード 在庫 寸 法 Size(mm) 適用 アー穴 HSK-A63-12.5-115-21 ● 32.7 115 10 3° BT30-10.5-45-18
カッタ 有無 備考 10.5 M10 18 35 45 10 13.7° ○
Item code Stock DCONWS THSZWS LF LB1 LS BD1 DCONMS With/ Note
D1 Cutter body without LF HSK-A63-17-40-28 ● 31.8 40 - 3° BT30-10.5-70-18 70 10 8.1°
air hole
LB1 LS HSK-A63-17-60-28 ● 17 M16 28 33.9 60 10 3° BT30-12.5-15-21 15 5 32.3°
ASC12-6.5-74-24Z ● 74 24 50 HSK-A63-17-60-28S 48 60 10 9.5° BT30-12.5-40-21 40 10 17.6°
ASC12-6.5-94-44Z ● 94 44 50 HSK-A63-17-110-28 ● 39.2 110 10 3° BT30-12.5-65-21 12.5 M12 21 40 65 10 9.8° ○
● 6.5 M6 11 12 11.5 C φ12 -
ASC12-6.5-129-64Z 129 64 65 【注意】クーラントパイプは付属しております。【 Note】Coolant Pipe is attached. BT30-12.5-85-21 85 10 7.2°
BT30-17-10-28 10 5 31°
ASC12-6.5-129-24Z ● 129 24 105 BT30-17-35-28 17 M16 28 40 35 10 13.5° ○
ASC16-8.5-95-30Z ● 95 30 65 THSZWS ボアタイプ用アーバ Bore Type Arbor BT30-17-60-28 60 10 6.8°
ASC16-8.5-120-55Z ● 120 55 65 Dタイプ D type 【注意】モジュラーミル用BT30アーバご使用の際は、標準切削条件表を目安に加工条件を
決定して下さい。加工状況により振動が懸念される場合は、1.切り込み深さ(ap)を低
ASC16-8.5-140-75Z ● 8.5 M8 140 75 65 14.5 16 15.5 C φ16 ○ 減する 2.一刃当りの送り(fz)を低減する方法で調整下さい。
商品コード 在庫 寸 法 Size(mm) 適用 エアー穴 ■ アーバ Arbor
ASC16-8.5-160-95Z ● 160 95 65 カッタ 有無 備考 DCONWS
BD1 【Note】When using the BT30 arbor for modular mills, determine the processing
Item code Stock With/ Note
ASC16-8.5-160-30Z ● 160 30 130 DCONWS THSZWS LF LB1 LS BD1 DCONMS D1 Cutter body without
air hole conditions using the standard cutting conditions table as a general guide.
THSZWS If vibrations are a concern due to the processing conditions, adjust conditions
※2 ASC20-10.5-120-50Z ● 120 50 70 AS12-6.5-84-4 ● 6.5 M6 84 4 80 11 12 - B φ12 - LB1 38 by 1.reducing cutting depth (ap) or 2.reducing per-flute feed rate (fz).
(エアー穴付き With air hole)
※2 ASC20-10.5-170-90Z ● 170 90 80
10.5 M10 18.5 20 19.5 C φ20 ○ AS16-8.5-95-15 ● 8.5 M8 95 15 80 14.5 16 15.5 C φ16 ○ M20
※2 ASC20-10.5-220-120Z ● 220 120 100 φ22 M10 M16
24 50
※2 ASC20-10.5-270-150Z ● 270 150 120 AS20-10.5-100-20 ● 10.5 M10 100 20 80 18 20 - D φ20 ○ 16
φ22 ■ BT40
※2 ASC20-10.5-220-50Z ● 220 170 10 25 16 35
10.5 M10 50 φ20
18.5 20 19.5 C ○ 14 36
※2 ASC20-10.5-270-50Z ● 270 220 φ22 AS25-12.5-115-35 ● φ25 LB2 27 65.4
12.5 M12 115 35 80 23 25 - D φ28 ○
(エアー穴付き With air hole) (エアー穴付き With air hole) (エアー穴付き With air hole) LB1 THSZWS
※2 ASC25-12.5-145-65 ● 145 65 80 部品番号:100-174 部品番号:100-213 部品番号:600-211
※2 ASC25-12.5-215-115 ● 215 115 100 Parts Parts Parts
φ25 φ30 ※首部は、ユーザ様にて追加工可
12.5 M12 23 25 - E ○
※2 ASC25-12.5-265-145 ● 265 145 120 φ28 AS32-17-110-30 ● 17 M16 110 30 80 28 32 - D φ32 ○ 商品コード 在庫 寸 法 Size(mm) 能です。
重量 アーバ用ねじ 適用カッタ 備考
φ40 Item code For neck section, additional
Stock DCONWS THSZWS LB1 BD1 Weight(kgf) Arbor screw Cutter body Note
※2 ASC25-12.5-315-195 ● 315 195 120 BHTA2 BT40 machining to user
BT50-22.225- 50-50 ● 50 4.3 specifications is possible.
※2 ASC25-12.5-265-65 ● 265 200 【注意】市販のミ-リングチャックにて使用できます。 【Note】Commercial milling chucks can be used.
25 BT50-22.225-100-50 ● 100 5.0
12.5 M12 65 23 - E φ25 ○
※2 ASC25-12.5-315-65 ● 315 250 φ28 BT50-22.225-150-50 ARB4050R-3
● 22.225 M10 150 47 5.7 100-174 商品コード 在庫 寸 法 Size(mm) エアー穴
有無
ASC32-17-160-80 ● 160 80 80 BT50-22.225-200-50 200 ARB4050R-5
● 6.4 Item code Stock DCONWS THSZWS BD1 φDS LB2 LB1 BHTA2 With/without
air hole
BT40-6.5-30-9.7
ASC32-17-210-110 ● BT50-22.225-250-50 ● 250 7.1 30 5 17°
210 110 100 φ30 ■ 鋼シャンク Steel Shank BT50-22.225- 50-63 ● 50 4.8 BT40-6.5-55-9.7 6.5 M6 9.7 25 55 10 9.6° -
ASC32-17-260-140 ● 17 M16 260 140 120 28 32 - E φ32 ○ BT50-22.225-100-63 ● 100 5.9 BT40-6.5-80-9.7 80 10 6.2°
ASC32-17-310-190 ● 310 190 120 〈φ40〉 LF BT40-6.5-130-9.7 130 10 3.6°
LB1 LS BT50-22.225-150-63 ● 150 7.0 ARB4063R-4 BT40-8.5-25-15
ASC32-17-360-240 ● 360 240 120 BT50-22.225-200-63 ● 22.225 M10 25 5 20.6°
200 60 8.1 100-174
ARB4063R-6 BT40-8.5-50-15 8.5 M8 15 30 50 10 10.6°
BT40-8.5-75-15 ○
ASC32-17-260-80 ● 260 180 BT50-22.225-250-63 ● 250 9.3 75 10 6.6°
φ30 BT50-22.225-350-63 ● 350 11.5 BT40-8.5-125-15 125 10 3.7°
ASC32-17-310-80 ● 17 M16 310 80 230 28 32 - E φ32 ○ BT50-31.75- 80-80 BT40-10.5-20-18 20 5 29.5°
80
● 〈φ40〉 ● 6.8 BT40-10.5-45-18
130 10.5 M10 18 35 45 10 13.7°
ASC32-17-360-80 360 280 BT50-31.75-130-80 ● 8.5 BT40-10.5-70-18 ○
70 10 8.1°
THSZWS
【注意】①※2と※1(P5)をセットで使用すると干渉がありません。 BT50-31.75-180-80 ARB4080R-4
● 31.75 M16 180 76 10.2 100-213 BT40-10.5-120-18 120 10 4.4°
②市販のミ-リングチャック、焼ばめホルダーにて使用できます。 ※首部及び全長は、ユーザ様にて追加工可能です。 BT50-31.75-260-80 ● 260 12.9 ARB4080R-6 BT40-12.5-15-21 15 5 32.3°
③<φ40>寸法は、突き出し長さ200mm以下を目安にご使用下さい。 For neck section or total length, additional machining to user specifications is possible. BT50-31.75-330-80 ● 330 15.4 BT40-12.5-40-21 12.5 M12 21 40 40 10 17.6°
【Note】①When※2 and※1 (P5) are used together as a set, there is no interference. BT40-12.5-65-21 ○
65 10 9.8°
②Commercial milling chucks or shrink-fit holders can be used. 商品コード 在庫 寸 法 Size(mm) 適用 エアー穴 BT50-31.75- 80-100 ● 80 8.3 BT40-12.5-115-21 115 10 5.2°
③For the Ø40 size, it is recommended that the protrusion length be 200mm or less. Item code Stock カッタ 有無 備考
With/ Note BT50-31.75-130-100 130 11.1 BT40-17-10-28 10 5 45°
DCONWS THSZWS LF LB1 LS BD1 DCONMS Cutter body without BT50-31.75-180-100 ARB4100R-5
air hole ● 31.75 M16 180 96 13.9 100-213 BT40-17-35-28
BT50-31.75-260-100 ● 18.4 ARB5100R-5 BT40-17-60-28 17 48 21.8°
260 M16 28 35 10 ○
60 10 11.3°
φ30
BT50-31.75-330-100 110 10 5.7°
● 330 22.4 BT40-17-110-28
AS42-17-360-90 ● 17 M16 360 90 270 28 42 φ32 ○ BT50-38.1-180-125 ● 180 14.8
φ40 BT50-38.1-260-125 ARB4125R-6
● 38.1 M20 260 98 19.7 600-211
BT50-38.1-330-125 ● 330 24.0 ARB5125R-6
【注意】市販のミ-リングチャックにて使用できます。 【Note】Commercial milling chucks can be used.
【注意】カッタ取付のアーバ用ねじは、アーバに付属しておりますが、カッタ本体には付属しておりません。
【Note】Arbor screw is attached on an arbor. Screws for cutters as lours are not
equipped with cutter bodies.
●印:標準在庫品です。●:Stocked items.
08
DCONWS DCONWS
BD1
D1
BD1
タイプ Type DCONMS DCONMS
DCONWS DCONWS DCONWS
DCONWS
BD1 BD1
BD1
D1
BD1
タイプ Type
DCONMS
DCONMS DCONMS DCONMS
DCONWS
BD1
φDS
φ63
DCONWS DCONWS
BD1 BD1
φDS φDS
φ63 φ46
Page9
ラインナップ
Line Up
モジュラーミル専用シャンク The Shanks for Modular Mill モジュラーミル用アーバ Modular Mill Arbor
■ 超硬シャンク Carbide Shank ■ 鋼シャンク Steel Shank ■ HSK LB2 26 32 ■ BT30
LB2 22 48.4
LF LF LB1 THSZWS
LB1 THSZWS
LB1 LS
LB1 LS
※首部は、ユーザ様にて追加工
可能です。
THSZWS For neck section, additional
BHTA2 HSK-A63 BHTA2 BT30 machining to user
Cタイプ C type THSZWS specifications is possible.
Bタイプ B type
商品コード 在庫 寸 法 Size(mm) エアー穴
有無 備考 商品コード 在庫 寸 法 Size(mm) エアー穴
有無
LF LF Item code Stock DCONWS THSZWS BD1 φDS LB2 LB1 BHTA2 With/without
air hole Note Item code Stock DCONWS THSZWS BD1 φDS LB2 LB1 BHTA2 With/without
air hole
LB1 LS
LB1 LS HSK-A63-10.5-30-18 ● 20.8 30 - 3° BT30-6.5-30-9.7 30 5 17°
HSK-A63-10.5-70-18 ● 10.5 M10 18 25 70 10 3° BT30-6.5-55-9.7 6.5 M6 9.7 25 55 10 9.6° -
HSK-A63-10.5-70-18S 48 70 10 12° BT30-6.5-80-9.7 80 10 6.2°
THSZWS HSK-A63-10.5-120-18 ● 30.2 120 10 3° BT30-8.5-25-15 25 5 20.6°
Eタイプ E type THSZWS HSK-A63-12.5-35-21 ● 24.3 35 - 3° BT30-8.5-50-15 8.5 M8 15 30 50 10 10.6° ○
HSK-A63-12.5-65-21 ● 12.5 M12 21 27.5 65 10 3° ○ BT30-8.5-75-15 75 10 6.6°
Cタイプ (首テ-パ) C type (Tapered neck)
エ HSK-A63-12.5-65-21S 48 65 10 12° BT30-10.5-20-18 20 5 29.5°
商品コード 在庫 寸 法 Size(mm) 適用 アー穴 HSK-A63-12.5-115-21 ● 32.7 115 10 3° BT30-10.5-45-18
カッタ 有無 備考 10.5 M10 18 35 45 10 13.7° ○
Item code Stock DCONWS THSZWS LF LB1 LS BD1 DCONMS With/ Note
D1 Cutter body without LF HSK-A63-17-40-28 ● 31.8 40 - 3° BT30-10.5-70-18 70 10 8.1°
air hole
LB1 LS HSK-A63-17-60-28 ● 17 M16 28 33.9 60 10 3° BT30-12.5-15-21 15 5 32.3°
ASC12-6.5-74-24Z ● 74 24 50 HSK-A63-17-60-28S 48 60 10 9.5° BT30-12.5-40-21 40 10 17.6°
ASC12-6.5-94-44Z ● 94 44 50 HSK-A63-17-110-28 ● 39.2 110 10 3° BT30-12.5-65-21 12.5 M12 21 40 65 10 9.8° ○
● 6.5 M6 11 12 11.5 C φ12 -
ASC12-6.5-129-64Z 129 64 65 【注意】クーラントパイプは付属しております。【 Note】Coolant Pipe is attached. BT30-12.5-85-21 85 10 7.2°
BT30-17-10-28 10 5 31°
ASC12-6.5-129-24Z ● 129 24 105 BT30-17-35-28 17 M16 28 40 35 10 13.5° ○
ASC16-8.5-95-30Z ● 95 30 65 THSZWS ボアタイプ用アーバ Bore Type Arbor BT30-17-60-28 60 10 6.8°
ASC16-8.5-120-55Z ● 120 55 65 Dタイプ D type 【注意】モジュラーミル用BT30アーバご使用の際は、標準切削条件表を目安に加工条件を
決定して下さい。加工状況により振動が懸念される場合は、1.切り込み深さ(ap)を低
ASC16-8.5-140-75Z ● 8.5 M8 140 75 65 14.5 16 15.5 C φ16 ○ 減する 2.一刃当りの送り(fz)を低減する方法で調整下さい。
商品コード 在庫 寸 法 Size(mm) 適用 エアー穴 ■ アーバ Arbor
ASC16-8.5-160-95Z ● 160 95 65 カッタ 有無 備考 DCONWS
BD1 【Note】When using the BT30 arbor for modular mills, determine the processing
Item code Stock With/ Note
ASC16-8.5-160-30Z ● 160 30 130 DCONWS THSZWS LF LB1 LS BD1 DCONMS D1 Cutter body without
air hole conditions using the standard cutting conditions table as a general guide.
THSZWS If vibrations are a concern due to the processing conditions, adjust conditions
※2 ASC20-10.5-120-50Z ● 120 50 70 AS12-6.5-84-4 ● 6.5 M6 84 4 80 11 12 - B φ12 - LB1 38 by 1.reducing cutting depth (ap) or 2.reducing per-flute feed rate (fz).
(エアー穴付き With air hole)
※2 ASC20-10.5-170-90Z ● 170 90 80
10.5 M10 18.5 20 19.5 C φ20 ○ AS16-8.5-95-15 ● 8.5 M8 95 15 80 14.5 16 15.5 C φ16 ○ M20
※2 ASC20-10.5-220-120Z ● 220 120 100 φ22 M10 M16
24 50
※2 ASC20-10.5-270-150Z ● 270 150 120 AS20-10.5-100-20 ● 10.5 M10 100 20 80 18 20 - D φ20 ○ 16
φ22 ■ BT40
※2 ASC20-10.5-220-50Z ● 220 170 10 25 16 35
10.5 M10 50 φ20
18.5 20 19.5 C ○ 14 36
※2 ASC20-10.5-270-50Z ● 270 220 φ22 AS25-12.5-115-35 ● φ25 LB2 27 65.4
12.5 M12 115 35 80 23 25 - D φ28 ○
(エアー穴付き With air hole) (エアー穴付き With air hole) (エアー穴付き With air hole) LB1 THSZWS
※2 ASC25-12.5-145-65 ● 145 65 80 部品番号:100-174 部品番号:100-213 部品番号:600-211
※2 ASC25-12.5-215-115 ● 215 115 100 Parts Parts Parts
φ25 φ30 ※首部は、ユーザ様にて追加工可
12.5 M12 23 25 - E ○
※2 ASC25-12.5-265-145 ● 265 145 120 φ28 AS32-17-110-30 ● 17 M16 110 30 80 28 32 - D φ32 ○ 商品コード 在庫 寸 法 Size(mm) 能です。
重量 アーバ用ねじ 適用カッタ 備考
φ40 Item code For neck section, additional
Stock DCONWS THSZWS LB1 BD1 Weight(kgf) Arbor screw Cutter body Note
※2 ASC25-12.5-315-195 ● 315 195 120 BHTA2 BT40 machining to user
BT50-22.225- 50-50 ● 50 4.3 specifications is possible.
※2 ASC25-12.5-265-65 ● 265 200 【注意】市販のミ-リングチャックにて使用できます。 【Note】Commercial milling chucks can be used.
25 BT50-22.225-100-50 ● 100 5.0
12.5 M12 65 23 - E φ25 ○
※2 ASC25-12.5-315-65 ● 315 250 φ28 BT50-22.225-150-50 ARB4050R-3
● 22.225 M10 150 47 5.7 100-174 商品コード 在庫 寸 法 Size(mm) エアー穴
有無
ASC32-17-160-80 ● 160 80 80 BT50-22.225-200-50 200 ARB4050R-5
● 6.4 Item code Stock DCONWS THSZWS BD1 φDS LB2 LB1 BHTA2 With/without
air hole
BT40-6.5-30-9.7
ASC32-17-210-110 ● BT50-22.225-250-50 ● 250 7.1 30 5 17°
210 110 100 φ30 ■ 鋼シャンク Steel Shank BT50-22.225- 50-63 ● 50 4.8 BT40-6.5-55-9.7 6.5 M6 9.7 25 55 10 9.6° -
ASC32-17-260-140 ● 17 M16 260 140 120 28 32 - E φ32 ○ BT50-22.225-100-63 ● 100 5.9 BT40-6.5-80-9.7 80 10 6.2°
ASC32-17-310-190 ● 310 190 120 〈φ40〉 LF BT40-6.5-130-9.7 130 10 3.6°
LB1 LS BT50-22.225-150-63 ● 150 7.0 ARB4063R-4 BT40-8.5-25-15
ASC32-17-360-240 ● 360 240 120 BT50-22.225-200-63 ● 22.225 M10 25 5 20.6°
200 60 8.1 100-174
ARB4063R-6 BT40-8.5-50-15 8.5 M8 15 30 50 10 10.6°
BT40-8.5-75-15 ○
ASC32-17-260-80 ● 260 180 BT50-22.225-250-63 ● 250 9.3 75 10 6.6°
φ30 BT50-22.225-350-63 ● 350 11.5 BT40-8.5-125-15 125 10 3.7°
ASC32-17-310-80 ● 17 M16 310 80 230 28 32 - E φ32 ○ BT50-31.75- 80-80 BT40-10.5-20-18 20 5 29.5°
80
● 〈φ40〉 ● 6.8 BT40-10.5-45-18
130 10.5 M10 18 35 45 10 13.7°
ASC32-17-360-80 360 280 BT50-31.75-130-80 ● 8.5 BT40-10.5-70-18 ○
70 10 8.1°
THSZWS
【注意】①※2と※1(P5)をセットで使用すると干渉がありません。 BT50-31.75-180-80 ARB4080R-4
● 31.75 M16 180 76 10.2 100-213 BT40-10.5-120-18 120 10 4.4°
②市販のミ-リングチャック、焼ばめホルダーにて使用できます。 ※首部及び全長は、ユーザ様にて追加工可能です。 BT50-31.75-260-80 ● 260 12.9 ARB4080R-6 BT40-12.5-15-21 15 5 32.3°
③<φ40>寸法は、突き出し長さ200mm以下を目安にご使用下さい。 For neck section or total length, additional machining to user specifications is possible. BT50-31.75-330-80 ● 330 15.4 BT40-12.5-40-21 12.5 M12 21 40 40 10 17.6°
【Note】①When※2 and※1 (P5) are used together as a set, there is no interference. BT40-12.5-65-21 ○
65 10 9.8°
②Commercial milling chucks or shrink-fit holders can be used. 商品コード 在庫 寸 法 Size(mm) 適用 エアー穴 BT50-31.75- 80-100 ● 80 8.3 BT40-12.5-115-21 115 10 5.2°
③For the Ø40 size, it is recommended that the protrusion length be 200mm or less. Item code Stock カッタ 有無 備考
With/ Note BT50-31.75-130-100 130 11.1 BT40-17-10-28 10 5 45°
DCONWS THSZWS LF LB1 LS BD1 DCONMS Cutter body without BT50-31.75-180-100 ARB4100R-5
air hole ● 31.75 M16 180 96 13.9 100-213 BT40-17-35-28 17 21.8°
M16 28 48 35 10
BT50-31.75-260-100 ● 18.4 ARB5100R-5 BT40-17-60-28 ○
260 60 10 11.3°
φ30
BT50-31.75-330-100 110 10 5.7°
● 330 22.4 BT40-17-110-28
AS42-17-360-90 ● 17 M16 360 90 270 28 42 φ32 ○ BT50-38.1-180-125 ● 180 14.8
φ40 BT50-38.1-260-125 ARB4125R-6
● 38.1 M20 260 98 19.7 600-211
BT50-38.1-330-125 ● 330 24.0 ARB5125R-6
【注意】市販のミ-リングチャックにて使用できます。 【Note】Commercial milling chucks can be used.
【注意】カッタ取付のアーバ用ねじは、アーバに付属しておりますが、カッタ本体には付属しておりません。
【Note】Arbor screw is attached on an arbor. Screws for cutters as lours are not
equipped with cutter bodies.
●印:標準在庫品です。●:Stocked items. 無印:受注生産品です。No mark:Manufactured upon request only. 09
DCONWS DCONWS
BD1
D1
BD1
タイプ Type DCONMS DCONMS
DCONWS DCONWS DCONWS
DCONWS
BD1 BD1
BD1
D1
BD1
タイプ Type
DCONMS
DCONMS DCONMS DCONMS
DCONWS
BD1
φDS
φ63
DCONWS DCONWS
BD1 BD1
φDS φDS
φ63 φ46
Page10
ラインナップ
Line Up
レッドスクリューアーバ Red screw arbor
H ■注意事項 Caution
φC1 φC 10 ● 一部取付けできない交換式工具があります。
φC2 G H 取付け可能か「交換式工具取付部」で寸法を確認いただくか、弊社までお問合
1
わせください。
● ※の商品は、条件を工具の推奨条件の半分程度に落としてご使用ください。
機械とシャンクとの結合力に比べ、切削抵抗が大きくなり、ホルダシャンク部で
φD フレッチング現象またはホルダの抜けが発生します。
● Some of the indexable end mills cannot be attached to the RED screw arbor.
5 Please check your indexable end mills for conformance to the dimensions, or
L1 M please contact MOLDINO Tool Engineering, Ltd.
● Because cutting resistance is greater than the tool holder connection force
L モジュラーミル 取付け部 associated with the machine spindle, please reduce the recommended cutting
conditions by 50% for the RED screw arbors marked with ※. Otherwise, the tool
Dimensions for the Modular Mill mounting holder shank may experience fretting corrosion or fall out of the machine spindle.
在 寸法 Size(mm) 剛性値 在 剛性値
商品コード 庫 重量 (μm) 商品コード 庫 寸法 Size(mm) 重量 (μm)
Item code (kg) Rigidity (kg) Rigidity
value Item code
G φD H H1 φC L M L1 φC1φC2 Weight δ Weight value
G φD H H1 φC L M L1 φC1φC2 δ
BT40-RSG8-105-M25 105 80 1.4 0.6 BT50-RSG10-200-M25 200 25 175 5.6 0.5
BT40-RSG8-135-M25 135 25 110 1.8 0.7 BT50-RSG10-165-M50 165 115 4.4 0.8
BT40-RSG8-165-M25 165 140 2.1 0.8 BT50-RSG10-195-M50 195 50 145 4.7 0.9
BT40-RSG8-130-M50 130 80 1.4 1.5 BT50-RSG10-225-M50 225 175 5.7 1.0
BT40-RSG8-160-M50 160 50 110 1.8 1.7 BT50-RSG10-190-M75 190 115 4.5 1.6
BT40-RSG8-190-M50 190 140 2.1 1.8 BT50-RSG10-220-M75 220 75 145 4.8 1.7
BT40-RSG8-155-M75 155 80 1.5 3.1 BT50-RSG10-250-M75 250 175 5.8 1.8
BT40-RSG8-185-M75 M8 8.5 18 6.5 15 185 75 110 30 32 1.9 3.4 BT50-RSG10-215-M100 M10 10.5 22 6.5 19 215 115
BT40-RSG8-215-M75 215 140 2.2 3.5 36 38 4.5 2.7
BT50-RSG10-245-M100 245 100 145 4.8 2.9
BT40-RSG8-170-M90 170 80 1.5 4.5 BT50-RSG10-275-M100 275 175 5.8 2.9
BT40-RSG8-200-M90 200 90 110 1.9 4.8 BT50-RSG10-235-M120 235 115 4.6 3.9
BT40-RSG8-230-M90 230 140 2.2 4.9 BT50-RSG10-265-M120 265 120 145 4.9 4.2
BT40-RSG8-185-M105 185 80 1.6 6.2 BT50-RSG10-295-M120 295 175 5.9 4.2
BT40-RSG8-215-M105 215 105 110 2.0 6.7 BT50-RSG10-255-M140 255 115 4.7 5.5
BT40-RSG8-245-M105 245 140 2.3 6.8 BT50-RSG10-285-M140 285 140 145 5.0 5.8
BT40-RSG10-125-M25 125 100 1.8 0.4 BT50-RSG10-315-M140 315 175 6.0 5.8
BT40-RSG10-155-M25 155 25 130 2.2 0.5 BT50-RSG12-140-M25 140 115 4.6 0.2
BT40-RSG10-185-M25 185 160 2.4 0.7 BT50-RSG12-170-M25 170 25 145 5.0 0.3
BT40-RSG10-150-M50 150 100 1.9 0.8 BT50-RSG12-200-M25 200 175 5.8 0.4
BT40-RSG10-180-M50 180 50 130 2.3 1.0 BT50-RSG12-165-M50 165 115 4.7 0.5
BT40-RSG10-210-M50 210 160 2.5 1.2 BT50-RSG12-195-M50 195 50 145 5.1 0.6
BT40-RSG10-175-M75 175 100 2.0 1.6 BT50-RSG12-225-M50 225 175 5.9 0.6
BT40-RSG10-205-M75 M10 10.5 22 6.5 19 205 75 130 36 38 2.4 1.8 BT50-RSG12-190-M75 190 115 4.9 0.8
BT40-RSG10-235-M75 235 160 2.6 2.0 BT50-RSG12-220-M75 220 75 145 5.3 1.0
BT40-RSG10-200-M100 200 100 2.0 2.7 BT50-RSG12-250-M75 250 175 6.1 1.0
BT40-RSG10-230-M100 230 100 130 2.4 3.0 BT50-RSG12-215-M100 215 115 5.0 1.3
BT40-RSG10-260-M100 260 160 2.6 3.3 BT50-RSG12-245-M100 M12 12.5 22 6 24 245 100 145 43 45 5.4 1.5
BT40-RSG10-220-M120 220 100 2.1 4.0 BT50-RSG12-275-M100 275 175 6.2 1.6
BT40-RSG10-250-M120 250 120 130 2.5 4.3 BT50-RSG12-240-M125 240 115 5.2 2.1
BT40-RSG10-280-M120 280 160 2.7 4.6 BT50-RSG12-270-M125 270 125 145 5.6 2.3
BT40-RSG12-125-M25 125 100 2.0 0.3 BT50-RSG12-300-M125 300 175 6.4 2.4
BT40-RSG12-155-M25 155 25 130 2.4 0.4 BT50-RSG12-265-M150 265 115 5.3 3.0
BT40-RSG12-185-M25 185 160 2.7 0.5 BT50-RSG12-295-M150 295 150 145 5.7 3.3
BT40-RSG12-150-M50 150 100 2.1 0.5 BT50-RSG12-325-M150 325 175 6.5 3.4
BT40-RSG12-180-M50 180 50 130 2.5 0.7 BT50-RSG12-290-M175 290 115 5.5 4.2
BT40-RSG12-210-M50 210 160 2.8 0.9 BT50-RSG12-320-M175 320 175 145 5.9 4.6
BT40-RSG12-175-M75 175 100 2.3 0.9 BT50-RSG12-350-M175 350 175 6.7 4.6
BT40-RSG12-205-M75 M12 12.5 22 6 24 205 75 130 43 45 2.7 1.1 BT50-RSG16-140-M25 140 115 4.8 0.2
BT40-RSG12-235-M75 235 160 3.0 1.3 BT50-RSG16-170-M25 170 25 145 5.4 0.2
BT40-RSG12-200-M100 200 100 2.4 1.4 BT50-RSG16-200-M25 200 175 6.6 0.2
BT40-RSG12-230-M100 230 100 130 2.8 1.6 BT50-RSG16-165-M50 165 115 5.0 0.3
BT40-RSG12-260-M100 260 160 3.1 1.9 BT50-RSG16-195-M50 195 50 145 5.6 0.4
BT40-RSG12-225-M125 225 100 2.6 2.1 BT50-RSG16-225-M50 225 175 6.8 0.4
BT40-RSG12-255-M125 255 125 130 3.0 2.4 BT50-RSG16-190-M75 190 115 5.3 0.5
BT40-RSG12-285-M125 285 160 3.3 2.8 BT50-RSG16-220-M75 220 75 145 5.9 0.6
BT40-RSG16-125-M25 125 25 2.6 0.2 BT50-RSG16-250-M75 250 175 7.0 0.6
BT40-RSG16-150-M50 150 50 2.8 0.3 BT50-RSG16-215-M100 215 115 5.5 0.7
BT40-RSG16-175-M75 M16 17 25 6 29 175 75 100 52 54 3.0 0.5 BT50-RSG16-245-M100 245 100 145 6.1 0.9
BT40-RSG16-200-M100 200 100 3.2 0.8 BT50-RSG16-275-M100 275 175 7.2 0.9
BT40-RSG16-225-M125 ※ 225 125 3.4 1.2 BT50-RSG16-240-M125 240 115 5.7 1.1
BT50-RSG8-120-M25 120 95 4.0 0.6 BT50-RSG16-270-M125 M16 17 25 6 29 270 125 145 52 54 6.3 1.3
BT50-RSG8-150-M25 150 25 125 4.3 0.7 BT50-RSG16-300-M125 300 175 7.4 1.3
BT50-RSG8-180-M25 180 155 4.8 0.7 BT50-RSG16-265-M150 265 115 5.9 1.6
BT50-RSG8-145-M50 145 95 4.0 1.5 BT50-RSG16-295-M150 295 150 145 6.5 1.8
BT50-RSG8-175-M50 175 50 125 4.3 1.7 BT50-RSG16-325-M150 325 175 7.7 1.8
BT50-RSG8-205-M50 205 155 4.8 1.7 BT50-RSG16-290-M175 290 115 6.1 2.2 ■ 標準付属品 ●クーラントダクト(HSK-A) ■ Standard ● Coolant duct(HSK)
BT50-RSG8-170-M75 170 95 4.1 3.1 BT50-RSG16-320-M175 320 175 145 6.7 2.4 ■ 注 意 事 項 ●モジュラーミルは付属しません。 accessories
■ Caution ●
●プルスタッドは付属しておりません。 The Modular Mill is not a standard accessory.
BT50-RSG8-200-M75 M8 8.5 18 6.5 15 200 75 125 30 32 4.4 3.4 BT50-RSG16-350-M175 350 175 7.9 2.5 ●
●ご使用になるモジュラーミルが取付可能か「モジュラーミル取付部」で寸法をご確認ください。 Pull stud is not a standard accessory.
BT50-RSG8-230-M75 230 155 4.9 3.4 BT50-RSG16-315-M200 315 115 6.3 3.0 ● Please check your Modular Mills for conformance to the dimensions.
BT50-RSG8-185-M90 185 95 4.9 4.4 BT50-RSG16-345-M200 345 200 145 6.9 3.2
BT50-RSG8-215-M90 215 90 125 4.4 4.8 BT50-RSG16-375-M200 375 175 8.1 3.3 δ
BT50-RSG8-245-M90 245 155 4.9 4.8 BT50-RSG16-340-M225 340 115 6.5 3.9 剛性値について About the rigidity value
BT50-RSG8-200-M105 200 95 4.2 6.2 BT50-RSG16-370-M225 370 225 145 7.1 4.1
BT50-RSG8-230-M105 230 105 125 4.5 6.6 BT50-RSG16-400-M225 400 175 8.3 4.2 モジュラーミル先端に1kgf・m(9.8N)の曲げ A rigidity value represents the amount of deflection for the
BT50-RSG8-260-M105 260 155 5.0 6.6 A63-RSG8-105-M25 105 80 1.3 0.6 荷重をかけた時のホルダと工具全体がたわ entire holder and tool when a bending load of 1 kgf (9.8 N) is 1kgf (9.8N)
BT50-RSG10-140-M25 M10 10.5 22 6.5 19 140 25 115 36 38 4.3 0.4 A63-RSG8-135-M25 M8 8.5 18 6.5 15 135 25 110 30 32 1.4 0.7 む量を表しています。数値が小さい程、剛性 applied to the tip of the tool. The smaller the numerical value is, δ(μm)
BT50-RSG10-170-M25 170 145 4.6 0.5 A63-RSG8-165-M25 165 140 1.9 0.8 があり精度の高い加工が可能です。 the higher the rigidity and the more accurate the machining.
無印:受注生産品です。No mark:Manufactured upon request only. 納期は受注後10日程度になります。Delivery time is about ten days after an order received.
10
BT50 BT40
Stock
A63 BT50
Stock
Page11
ラインナップ
Line Up
在 寸法 Size(mm) 剛性値 在 寸法 Size(mm) 剛性値
商品コード 庫 重量 (μm)
Rigidity 商品コード 庫 重量 (μm)
Item code (kg) Item code (kg) Rigidity
φC L M L1 φC1φC2 Weight value
G φD H H1 δ Weight value
G φD H H1 φC L M L1 φC1φC2 δ
A63-RSG8-130-M50 130 80 1.3 1.5 A100-RSG8-230-M105
A63-RSG8-160-M50 160 50 110 1.4 1.7 60-M105 M8 8.5 18 6.5 15 230
260 105 125
155 30 32 3.1 6.7
A100-RSG8-2 3.6 6.6
A63-RSG8-190-M50 190 140 1.9 1.7 A100-RSG10-140-M25 140 115 3.1 0.4
A63-RSG8-155-M75 155 80 1.4 3.1 A100-RSG10-170-M25 170 25 145 3.5 0.5
A63-RSG8-185-M75 185 75 110 1.5 3.4 A100-RSG10-200-M25 200 175 4.4 0.5
A63-RSG8-215-M75 M8 8.5 18 6.5 15 215 140 A100-RSG10-165-M50 165 115 3.2 0.8
3-RSG8-170-M90 170 80 30 32 2.0 3.4
A6 2.0 4.4 A100-RSG10-195-M50 195 50 145 3.6 1.0
A63-RSG8-200-M90 200 90 110 1.5 4.8 A100-RSG10-225-M50 225 175 4.5 1.0
A63-RSG8-230-M90 230 140 2.0 4.9 A100-RSG10-190-M75 190 115 3.3 1.6
A63-RSG8-185-M105 185 80 1.5 6.2 A100-RSG10-220-M75 220 75 145 3.7 1.8
A63-RSG8-215-M105 215 105 110 1.6 6.6 A100-RSG10-250-M75
A63-RSG8-245-M105 245 140 2.1 6.7 M10 10.5 22 6.5 19 250 175 36 38 4.6 1.8
A100-RSG10-215-M100 215 115 3.3 2.7
A63-RSG10-125-M25 125 100 1.6 0.4 A100-RSG10-245-M100 245 100 145 3.7 2.9
A63-RSG10-155-M25 155 25 130 1.9 0.5 A100-RSG10-275-M100 275 175 4.6 2.9
A63-RSG10-185-M25 185 160 2.3 0.6 A100-RSG10-235-M120 235 115 3.4 4.0
A63-RSG10-150-M50 150 100 1.7 0.8 A100-RSG10-265-M120 265 120 145 3.8 4.2
A63-RSG10-180-M50 180 50 130 2.0 1.0 A100-RSG10-295-M120 295 175 4.7 4.2
A63-RSG10-210-M50 210 160 2.4 1.2 A100-RSG10-255-M140 255 115 3.5 5.6
A63-RSG10-175-M75 175 100 1.8 1.6 A100-RSG10-285-M140 285 140 145 3.9 5.8
A63-RSG10-205-M75 205 75 130 2.1 1.8 A100-RSG10-315-M140 315 175 4.8 5.8
A63-RSG10-235-M75 M10 10.5 22 6.5 19 235 160 36 38 2.5 2.0 A100-RSG12-140-M25 140 115 3.4 0.3
A63-RSG10-200-M100 200 100 1.8 2.7 A100-RSG12-170-M25 170 25 145 3.7 0.4
A63-RSG10-230-M100 230 100 130 2.1 2.9 A100-RSG12-200-M25 200 175 4.7 0.4
A63-RSG10-260-M100 260 160 2.5 3.2 A100-RSG12-165-M50 165 115 3.5 0.5
A63-RSG10-220-M120 220 100 1.9 4.0 A100-RSG12-195-M50 195 50 145 3.8 0.6
A63-RSG10-250-M120 250 120 130 2.2 4.2 A100-RSG12-225-M50 225 175 4.8 0.6
A63-RSG10-280-M120 280 160 2.6 4.5 A100-RSG12-190-M75 190 115 3.7 0.8
A63-RSG10-240-M140 240 100 2.0 5.6 A100-RSG12-220-M75 220 75 145 4.0 1.0
A63-RSG10-270-M140 270 140 130 2.3 5.9 A100-RSG12-250-M75 250 175 5.0 1.0
A63-RSG10-300-M140 300 160 2.7 6.2 A100-RSG12-215-M100 215 115 3.8 1.4
A63-RSG12-125-M25 125 100 1.9 0.3 A100-RSG12-245-M100 M12 12.5 22 6 24 245 100 145 43 45 4.1 1.6
A63-RSG12-155-M25 155 25 130 2.3 0.4 A100-RSG12-275-M100 275 175 5.1 1.6
A63-RSG12-185-M25 185 160 2.7 0.5 A100-RSG12-240-M125 240 115 4.0 2.1
A63-RSG12-150-M50 150 100 2.0 0.5 A100-RSG12-270-M125 270 125 145 4.3 2.4
A63-RSG12-180-M50 180 50 130 2.4 0.6 A100-RSG12-300-M125 300 175 5.3 2.4
A63-RSG12-210-M50 210 160 2.8 0.8 A100-RSG12-265-M150 265 115 4.1 3.0
A63-RSG12-175-M75 175 100 2.2 0.9 A100-RSG12-295-M150 295 150 145 4.4 3.4
A63-RSG12-205-M75 205 75 130 2.6 1.0 A100-RSG12-325-M150 325 175 5.4 3.4
A63-RSG12-235-M75 M12 12.5 22 6 24 235 160 43 45 3.0 1.3 A100-RSG12-290-M175 290 115 4.3 4.3
A63-RSG12-200-M100 200 100 2.3 1.4 A100-RSG12-320-M175 320 175 145 4.6 4.6
A63-RSG12-230-M100 230 100 130 2.7 1.6 A100-RSG12-350-M175 350 175 5.6 4.6
A63-RSG12-260-M100 260 160 3.1 1.9 A100-RSG16-140-M25 140 115 4.0 0.2
A63-RSG12-225-M125 225 100 2.5 2.1 A100-RSG16-170-M25 170 25 145 4.5 0.2
A63-RSG12-255-M125 255 125 130 2.9 2.4 A100-RSG16-200-M25 200 175 5.7 0.2
A63-RSG12-285-M125 285 160 3.3 2.7 A100-RSG16-165-M50 165 115 4.2 0.3
A63-RSG12-250-M150 250 100 2.6 3.1 A100-RSG16-195-M50 195 50 145 4.7 0.4
A63-RSG12-280-M150 280 150 130 3.0 3.4 A100-RSG16-225-M50 225 175 5.9 0.4
A63-RSG12-310-M150 310 160 3.4 3.8 A100-RSG16-190-M75 190 115 4.5 0.5
A63-RSG16-140-M25 140 25 2.8 0.2 A100-RSG16-220-M75 220 75 145 5.0 0.6
A63-RSG16-165-M50 165 50 3.2 0.4 A100-RSG16-250-M75 250 175 6.1 0.6
A63-RSG16-190-M75 190 75 3.6 0.6 A100-RSG16-215-M100 215 115 4.7 0.8
A63-RSG16-215-M100 M16 17 25 6 29 215 100 115 52 54 2.8 0.9 A100-RSG16-245-M100 245 100 145 5.2 0.9
A63-RSG16-240-M125 ※ 240 125 2.8 1.3 A100-RSG16-275-M100 275 175 6.3 0.9
A63-RSG16-265-M150 ※ 265 150 3.2 1.9 A100-RSG16-240-M125 240 115 4.9 1.1
A63-RSG16-290-M175 ※ 290 175 3.6 2.5 A100-RSG16-270-M125 M16 17 25 6 29 270 125 145 52 54 5.4 1.3
A100-RSG8-120-M25 120 95 2.6 0.6 A100-RSG16-300-M125 300 175 6.5 1.3
A100-RSG8-150-M25 150 25 125 2.9 0.8 A100-RSG16-265-M150 265 115 5.1 1.6
A100-RSG8-180-M25 180 155 3.4 0.8 A100-RSG16-295-M150 295 150 145 5.6 1.8
A100-RSG8-145-M50 145 95 2.6 1.5 A100-RSG16-325-M150 325 175 6.7 1.8
A100-RSG8-175-M50 175 50 125 2.9 1.7 A100-RSG16-290-M175 290 115 5.3 2.2
A100-RSG8-205-M50 205 155 3.4 1.7 A100-RSG16-320-M175 320 175 145 5.8 2.4
A100-RSG8-170-M75 M8 8.5 18 6.5 15 170 95 30 32 2.7 3.1 A100-RSG16-350-M175 350 175 7.0 2.5
A100-RSG8-200-M75 200 75 125 3.0 3.4 A100-RSG16-315-M200 315 115 5.5 3.0
A100-RSG8-230-M75 230 155 3.5 3.4 A100-RSG16-345-M200 345 200 145 6.0 3.2
A100-RSG8-185-M90 185 95 2.7 4.5 A100-RSG16-375-M200 375 175 7.2 3.3
A100-RSG8-215-M90 215 90 125 3.0 4.9 A100-RSG16-340-M225 340 115 5.7 3.9
A100-RSG8-245-M90 245 155 3.5 4.8 A100-RSG16-370-M225 370 225 145 6.3 4.2
A100-RSG8-200-M105 200 105 95 2.8 6.3 A100-RSG16-400-M225 400 175 7.4 4.2
■ 標準付属品 ●クーラントダクト(HSK-A) ■ Standard ● Coolant duct(HSK)
■ 注 意 事 項 ●モジュラーミルは付属しません。 accessories
は付属しておりません。 ■ Caution ● The Modular Mill is not a standard accessory.
●プルスタッド
●
●ご使用になるモジュラーミルが取付可能か「モジュラーミル取付部」で寸法をご確認ください。 Pull stud is not a standard accessory.
● Please check your Modular Mills for conformance to the dimensions.
δ
剛性値について About the rigidity value
モジュラーミル先端に1kgf・m(9.8N)の曲げ A rigidity value represents the amount of deflection for the
荷重をかけた時のホルダと工具全体がたわ entire holder and tool when a bending load of 1 kgf (9.8 N) is 1kgf (9.8N)
む量を表しています。数値が小さい程、剛性 applied to the tip of the tool. The smaller the numerical value is, δ(μm)
があり精度の高い加工が可能です。 the higher the rigidity and the more accurate the machining.
11
A100 A63
Stock
A100
Stock
Page12
標準切削条件表
Recommended Cut t ing Condi t ions
ae
ARS ARL ARE
レギュラー形 ロング形 エキストラロング形
Regular Long Extra Long
ap
BT40
被削材 推奨材種 切削速度 りの送り φ25(2枚刃)φ3(2 3枚刃)φ40(3枚刃) φ50(4枚刃) φ40(2枚刃) φ50(3枚刃) φ63(3枚刃)
th 工具径DCX φ20(2枚刃)
Work material Recommended Cutting speed 使用機械 一刃当
Feed per too
inserts grade Vc( m/min) Machine fz( mm/t) Tool dia. ( 2 Flutes) r4 ( 2 Flutes) r5 ( 3 Flutes) r5(3 Flutes) r6 (4 Flutes) r6 (2 Flutes) r8 (3 Flutes) r8 (3 Flutes) r8
n (min-1) 3,180 2,550 1,990 1,590 1,270 1,590 1,270 1,010
炭素鋼 Vc(m/min) 200 200 200 200 200 200 200 200
合金鋼
( ※ V f (mm/min) 2,540 2,040 2,390 1,910 2,030 1,270 1,520 1,210
30HRC以下) 120 ~ 230 BT40 0.3 ~ 0.8 fz(mm/t) 0.4 0.4 0.4 0.4 0.4 0.4 0.4 0.4
Carbon steels JS4160
Alloy steels ap(mm) 1.5 1.5 1.5 2.0 2.0 2.0 2.0 2.0
(30HRC or less) ae(mm) 6 8 10 12 15 12 15 19
Q(cm3/min) 23 24 36 46 61 30 46 46
n (min-1) 2,390 1,910 1,490 1,190 950 1,190 950 760
合金鋼 Vc(m/min) 150 150 150 150 150 150 150 150
(焼入れ焼戻し材) Vf(mm/min) 960 760 890 710 760 480 570 460
(35HRC以下) JS4160 100 ~ 200 BT40 0.2 ~ 0.6 fz(mm/t) 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2
Alloy steels
(Quenched and tempered steels) ap(mm) 1.5 1.5 1.5 2.0 2.0 2.0 2.0 2.0
(35HRC or less) ae(mm) 6 8 10 12 15 12 15 19
Q(cm3/min) 8.6 9.1 13 17 23 12 17 17
n (min-1) 1,590 1,270 990 800 640 800 640 510
プリハードン鋼・合金鋼 Vc(m/min) 100 100 100 100 100 100 100 100
(焼入れ焼戻し材) V f (mm/min) 480 380 450 360 380 240 290 230
(45HRC以下)
Pre-hardened steels JP4120 60 ~ 150 BT40 0.15 ~ 0.3 fz(mm/t) 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15
Alloy steels ap(mm) 1.0 1.0 1.0 1.5 1.5 1.5 1.5 1.5
(Quenched and tempered steels)
(45HRC or less) ae(mm) 6 8 10 12 15 12 15 19
Q(cm3/min) 2.9 3.0 4.5 6.5 8.6 4.3 6.5 6.6
n (min-1) 1,270 1,020 800 640 510 640 510 400
Vc(m/min) 80 80 80 80 80 80 80 80
焼入れ鋼 290 310 220 260 200
(55HRC以下) JP4105 Vf(mm/min) 380 310 360
60 ~ 100 BT40 0.15 ~ 0.3 fz(mm/t) 0.15 0.15 0.15 0.15 0.15 0.17 0.17 0.17
Hardened steels JP4120
(55HRC or less) ap(mm) 1.0 1.0 1.0 1.0 1.0 1.5 1.5 1.5
ae(mm) 6 8 10 12 15 12 15 19
Q(cm3/min) 2.3 2.5 3.6 3.5 4.7 4.0 5.9 5.7
n (min-1) 1,110 890 690 550 440 550 440 350
Vc(m/min) 70 70 70 70 70 70 70 70
焼入れ鋼 Vf(mm/min) 220 170 200 160 170 110 130 100
(62HRC以下) JP4105 50 ~ 100 BT40 0.05 ~ 0.2 fz(mm/t) 0.1 0.1 0.1 0.1 0.1 0.1 0.1 0.1
Hardened steels
(62HRC or less) ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
ae(mm) 6 8 10 12 15 12 15 19
Q(cm3/min) 1.3 1.4 2.0 1.9 2.6 1.3 2.0 1.9
n (min-1) 3,180 2,550 1,990 1,590 1,270 1,590 1,270 1,010
Vc(m/min) 200 200 200 200 200 200 200 200
ステンレス鋼 JM4160 V f (mm/min) 1,590 1,280 1,490 1,430 1,520 950 1,140 910
Stainless steels 150 ~ 240 BT40 0.2 ~ 0.8 fz(mm/t) 0.25 0.25 0.25 0.3 0.3 0.3 0.3 0.3
SUS JP4120 ap(mm) 1.5 1.5 1.5 2.0 2.0 2.0 2.0 2.0
ae(mm) 6 8 10 12 15 12 15 19
Q(cm3/min) 14 15 22 34 46 23 34 35
n (min-1) 2,860 2,290 1,790 1,430 1,150 1,430 1,150 910
Vc(m/min) 180 180 180 180 180 180 180 180
鋳鉄 V f (mm/min) 2,290 1,830 2,150 2,150 2,300 1,430 1,730 1,370
Cast irons
FC JP4120 100 ~ 220 BT40 0.3 ~ 1.0 fz(mm/t) 0.4 0.4 0.4 0.5 0.5 0.5 0.5 0.5
FCD ap(mm) 1.5 1.5 1.5 2.0 2.0 2.0 2.0 2.0
ae(mm) 6 8 10 12 15 12 15 19
Q(cm3/min) 21 22 32 52 69 34 52 52
※1:「JP4105」は高硬度鋼専用材種で、生材には適しません。
※1:「JP4105」 insert's grade specialized in High hardened steel is not suitable for Non-heat-treated steel material. 傾斜切削・ヘリカル切削・Z方向切込み Ramping, Helical Milling, Feeding toward Z-AXIS
【注意】 【Note】
①JSコートは通電式タッチセンサーに反応しませんのでご注意ください。 ① Please note that the JS Coating does not cause a reaction in conductive touch 中心まで切れ刃がないため傾斜角度(θ)やZ軸方向切込み深さ(ap)に制限があります。
②不水溶性切削油は、火災の恐れがありますので使用しないでください。 sensors. There are restrictions to ramp angle (θ) and cutting depth (ap) toward Z-axis because of designs of cutting edge.
③排出した切りくずは飛散し作業者を切傷させ、火傷あるいは目に入って ② Due to fire risks do not use neat cutting oil as a coolant. (mm)
③ The evacuation of swarf can cause burns, cuts or damage to the eyes please 傾斜切削 ヘリカル切削
負傷させる恐れがありますので、ご使用に際してはその周囲に安全カ ensure the correct safety cover is fitted around the machine, and necessary 工具径DCX
Ramping Helical milling Tool dia. φ20(r4) φ25(r5) φ32(r5) φ40(r6) φ50(r8) φ63(r8)
バーを取り付け保護めがね等の保護具を着用して、安全な環境で作業 personal protection equipment is worn by the machine operator.
される事をお願い致します。 ④ These conditions are for general guidance; in actual machining conditions 推奨θ 3°以下
Recommended Below 3 degrees
④この切削条件表は切削条件の目安を示すものです。実際の加工では加 adjust the parameters according to your actual machine and work-piece 穴径φ
工形状、目的、使用機械等により条件を調整してください。 conditions. h 1 2 2 2.5 2.5 2.5
⑤ Hole Dia.
If vibrations are a concern due to the cutting conditions, adjust conditions by h
⑤加工状況により振動が懸念される場合は、1.切り込み深さ(ap)を低減 1.reducing cutting depth (ap) or 2.reducing per-flute feed rate (fz). θ ap 2 3 3 3.7 4.5 5.5
する 2.一刃当りの送り(fz)を低減する方法で調整ください。 ⑥ In the case of slotting, feed speed could be down to 70% of the whole.
⑥溝切削の場合、送り量は70%を目安としてください。 ⑦ In steel exceeding 60HRC, such as dice steel between the colds, ヘリカル穴径
傾斜切込み角 a Hole Dia. 28~38 34~48 48~62 60~78 75~98 101~124
p
⑦冷間ダイス鋼など60HRCを超える鋼種の場合は、1刃当りの送り(fz) please set the sending (fz) value per one edge about to 1/2. Ramp milling angle
値を1/2程度に設定して下さい。 ⑧ This table is based on the overhang of regular type (L1). 【注意】切りくずが飛散することがあります。切りくずカバーを設置してください。
工具径DCX 【Note】Due to swarf evacuation wear safety glasses in the vicinity of the operation.
⑧工具突き出し量は標準形の首下長さ(L1)です。 Tool dia.
12
Page13
標準切削条件表
Recommended Cut t ing Condi t ions
ARS ARL ARE
レギュラー形 ロング形 エキストラロング形
Regular Long Extra Long
BT50 ※赤字は第 1推奨材種です。 Red indicates primary recommended insert grade.
被削材 推奨材種 切削速度 径DCX φ20(2枚刃)φ25(2枚刃)φ3(2 3枚刃)φ40(3枚刃) φ50(4枚刃) φ40(2枚刃) φ50(3枚刃) φ63(3枚刃)
Work material Recommended Cutting speed 使用機械 一刃当りの送り
Feed per tooth 工具 (3 Flutes) r8
inserts grade Vc( m/min) Machine fz( mm/t) Tool dia. ( 2 Flutes) r4 ( 2 Flutes) r5 ( 3 Flutes) r5(3 Flutes) r6 (4 Flutes) r6 (2 Flutes) r8 (3 Flutes) r8
n (min-1) 3,180 2,550 1,990 1,590 1,270 1,590 1,270 1,010
炭素鋼 Vc(m/min) 200 200 200 200 200 200 200 200
合金鋼 V f (mm/min) 2,540 2,040 2,390 2,860 3,050 1,910 2,290 2,120
( ※
30HRC以下) 120 ~ 230 BT50 0.3 ~ 0.8 fz(mm/t) 0.4 0.4 0.4 0.6 0.6 0.6 0.6 0.7
Carbon steels JS4160
Alloy steels ap(mm) 1.5 1.5 1.5 2.0 2.0 2.5 2.5 2.5
(30HRC or less) ae(mm) 10 13 16 20 25 20 25 32
Q(cm3/min) 38 40 57 114 153 96 143 170
n (min-1) 2,390 1,910 1,490 1,190 950 1,190 950 760
合金鋼 Vc(m/min) 150 150 150 150 150 150 150 150
(焼入れ焼戻し材) Vf(mm/min) 1,430 1,150 1,340 1,070 1,140 950 1,140 910
(35HRC以下) JS4160 100 ~ 200 BT50 0.2 ~ 0.6 fz(mm/t) 0.3 0.3 0.3 0.3 0.3 0.4 0.4 0.4
Alloy steels
(Quenched and tempered steels) ap(mm) 1.5 1.5 1.5 2.0 2.0 2.5 2.5 2.5
(35HRC or less) ae(mm) 10 13 16 20 25 20 25 32
Q(cm3/min) 21 22 32 43 57 48 71 73
n (min-1) 1,590 1,270 990 800 640 800 640 510
プリハードン鋼・合金鋼 Vc(m/min) 100 100 100 100 100 100 100 100
(焼入れ焼戻し材) V f (mm/min) 640 510 590 480 510 320 380 310
(45HRC以下)
Pre-hardened steels JP4120 60 ~ 150 BT50 0.15 ~ 0.3 fz(mm/t) 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2
Alloy steels ap(mm) 1.0 1.0 1.0 1.5 1.5 2.0 2.0 2.0
(Quenched and tempered steels)
(45HRC or less) ae(mm) 10 13 16 20 25 20 25 32
Q(cm3/min) 6.4 6.6 9.4 14 19 13 19 20
n (min-1) 1,270 1,020 800 640 510 640 510 400
Vc(m/min) 80 80 80 80 80 80 80 80
焼入れ鋼 Vf(mm/min) 380 310 360 330 350 260 310 240
(55HRC以下) JP4105
60 ~ 100 BT50 0.15 ~ 0.3 fz(mm/t) 0.15 0.15 0.15 0.17 0.17 0.2 0.2 0.2
Hardened steels JP4120
(55HRC or less) ap(mm) 1.0 1.0 1.0 1.0 1.0 1.5 1.5 1.5
ae(mm) 10 13 16 20 25 20 25 32
Q(cm3/min) 3.8 4.0 5.8 6.6 8.8 7.8 12 12
n (min-1) 1,110 890 690 550 440 550 440 350
Vc(m/min) 70 70 70 70 70 70 70 70
焼入れ鋼 Vf(mm/min) 220 170 200 160 170 110 130 100
(62HRC以下) JP4105 50 ~ 100 BT50 0.05 ~ 0.2 fz(mm/t) 0.1 0.1 0.1 0.1 0.1 0.1 0.1 0.1
Hardened steels
(62HRC or less) ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
ae(mm) 10 13 16 20 25 20 25 32
Q(cm3/min) 2.2 2.2 3.2 3.2 4.3 2.2 3.3 3.2
n (min-1) 2,860 2,290 1,790 1,430 1,150 1,430 1,150 910
Vc(m/min) 180 180 180 180 180 180 180 180
ステンレス鋼 JM4160 V f (mm/min) 1,720 1,370 1,610 2,150 2,300 1,720 2,070 1,640
Stainless steels 150 ~ 240 BT50 0.2 ~ 0.8 fz(mm/t) 0.3 0.3 0.3 0.5 0.5 0.6 0.6 0.6
SUS JP4120 ap(mm) 1.5 1.5 1.5 2.0 2.0 2.5 2.5 2.5
ae(mm) 10 13 16 20 25 20 25 32
Q(cm3/min) 26 27 39 86 115 86 129 131
n (min-1) 2,860 2,290 1,790 1,430 1,150 1,430 1,150 910
Vc(m/min) 180 180 180 180 180 180 180 180
鋳鉄 V f (mm/min) 2,860 2,290 2,690 3,430 3,680 2,290 2,760 2,180
Cast irons
FC JP4120 100 ~ 220 BT50 0.3 ~ 1.0 fz(mm/t) 0.5 0.5 0.5 0.8 0.8 0.8 0.8 0.8
FCD ap(mm) 1.5 1.5 1.5 2.0 2.0 2.5 2.5 2.5
ae(mm) 10 13 16 20 25 20 25 32
Q(cm3/min) 43 45 65 137 184 115 173 174
※1:「JP4105」は高硬度鋼専用材種で、生材には適しません。
※1:「JP4105」 insert's grade specialized in High hardened steel is not suitable for Non-heat-treated steel material. 傾斜切削・ヘリカル切削・Z方向切込み Ramping, Helical Milling, Feeding toward Z-AXIS
【注意】 【Note】
①JSコートは通電式タッチセンサーに反応しませんのでご注意ください。 ① Please note that the JS Coating does not cause a reaction in conductive touch 中心まで切れ刃がないため傾斜角度(θ)やZ軸方向切込み深さ(ap)に制限があります。
②不水溶性切削油は、火災の恐れがありますので使用しないでください。 sensors. There are restrictions to ramp angle (θ) and cutting depth (ap) toward Z-axis because of designs of cutting edge.
③排出した切りくずは飛散し作業者を切傷させ、火傷あるいは目に入って ② Due to fire risks do not use neat cutting oil as a coolant. (mm)
③ The evacuation of swarf can cause burns, cuts or damage to the eyes please 傾斜切削 ヘリカル切削
負傷させる恐れがありますので、ご使用に際してはその周囲に安全カ ensure the correct safety cover is fitted around the machine, and necessary 工具径DCX
Ramping Helical milling Tool dia. φ20(r4) φ25(r5) φ32(r5) φ40(r6) φ50(r8) φ63(r8)
バーを取り付け保護めがね等の保護具を着用して、安全な環境で作業 personal protection equipment is worn by the machine operator.
される事をお願い致します。 ④ These conditions are for general guidance; in actual machining conditions 推奨θ 3°以下
Recommended Below 3 degrees
④この切削条件表は切削条件の目安を示すものです。実際の加工では加 adjust the parameters according to your actual machine and work-piece 穴径φ
工形状、目的、使用機械等により条件を調整してください。 conditions. h 1 2 2 2.5 2.5 2.5
⑤ Hole Dia.
If vibrations are a concern due to the cutting conditions, adjust conditions by h
⑤加工状況により振動が懸念される場合は、1.切り込み深さ(ap)を低減 1.reducing cutting depth (ap) or 2.reducing per-flute feed rate (fz). θ ap 2 3 3 3.7 4.5 5.5
する 2.一刃当りの送り(fz)を低減する方法で調整ください。 ⑥ In the case of slotting, feed speed could be down to 70% of the whole.
⑥溝切削の場合、送り量は70%を目安としてください。 ⑦ In steel exceeding 60HRC, such as dice steel between the colds, ヘリカル穴径
傾斜切込み角 a Hole Dia. 28~38 34~48 48~62 60~78 75~98 101~124
p
⑦冷間ダイス鋼など60HRCを超える鋼種の場合は、1刃当りの送り(fz) please set the sending (fz) value per one edge about to 1/2. Ramp milling angle
値を1/2程度に設定して下さい。 ⑧ This table is based on the overhang of regular type (L1). 【注意】切りくずが飛散することがあります。切りくずカバーを設置してください。
工具径DCX 【Note】Due to swarf evacuation wear safety glasses in the vicinity of the operation.
⑧工具突き出し量は標準形の首下長さ(L1)です。 Tool dia.
13
Page14
標準切削条件表
Recommended Cut t ing Condi t ions
ae
ARB AR
ボア形 ボア形
Bore type Bore type
ap
BT40
被削材 推奨材種 切削速度
Cutting speed 使用機械 一刃当りの送り 枚刃) φ50(5枚刃) φ63(6枚刃) φ80(6枚刃) φ100(5枚刃) φ63(3枚刃)
ed per tooth 工具径DCX φ40(3
Fe
Work material Recommended
inserts grade Vc( m/min) Machine fz( mm/t) Tool dia. (3 Flutes) r6 (5 Flutes) r6 (6 Flutes) r6 (6 Flutes) r6 (5 Flutes) r6 (3 Flutes) r8
n (min-1) 1,590 1,270 1,010 ― ― 1,010
炭素鋼 Vc(m/min) 200 200 200 ― ― 200
合金鋼 V f (mm/min) 1,910 2,540 2,420 ― ― 1,210
( ※
30HRC以下) 120 ~ 230 BT40 0.3 ~ 0.8 fz(mm/t) 0.4 0.4 0.4 ― ― 0.4
Carbon steels JS4160
Alloy steels ap(mm) 2.0 2.0 2.0 ― ― 2.0
(30HRC or less) ae(mm) 12 15 19 ― ― 19
Q(cm3/min) 46 76 92 ― ― 46
n (min-1) 1,190 950 760 ― ― 760
合金鋼 Vc(m/min) 150 150 150 ― ― 150
(焼入れ焼戻し材) Vf(mm/min) 710 950 910 ― ― 460
(35HRC以下) JS4160 100 ~ 200 BT40 0.2 ~ 0.6 fz(mm/t) 0.2 0.2 0.2 ― ― 0.2
Alloy steels
(Quenched and tempered steels) ap(mm) 2.0 2.0 2.0 ― ― 2.0
(35HRC or less) ae(mm) 12 15 19 ― ― 19
Q(cm3/min) 17 29 35 ― ― 17
n (min-1) 800 640 510 ― ― 510
プリハードン鋼・合金鋼 Vc(m/min) 100 100 100 ― ― 100
(焼入れ焼戻し材) V f (mm/min) 360 480 460 ― ― 230
(45HRC以下)
Pre-hardened steels JP4120 60 ~ 150 BT40 0.15 ~ 0.3 fz(mm/t) 0.15 0.15 0.15 ― ― 0.15
Alloy steels ap(mm) 1.5 1.5 1.5 ― ― 1.5
(Quenched and tempered steels)
(45HRC or less) ae(mm) 12 15 19 ― ― 19
Q(cm3/min) 6.5 11 13 ― ― 6.6
n (min-1) 640 510 400 ― ― 400
Vc(m/min) 80 80 80 ― ― 80
焼入れ鋼 Vf(mm/min) 290 380 360 ― ― 200
(55HRC以下) JP4105
60 ~ 100 BT40 0.15 ~ 0.3 fz(mm/t) 0.15 0.15 0.15 ― ― 0.17
Hardened steels JP4120
(55HRC or less) ap(mm) 1.0 1.0 1.0 ― ― 1.5
ae(mm) 12 15 19 ― ― 19
Q(cm3/min) 3.5 5.7 6.8 ― ― 5.7
n (min-1) 550 440 350 270 220 350
Vc(m/min) 70 70 70 70 70 70
焼入れ鋼 Vf(mm/min) 160 220 210 160 110 100
(62HRC以下) JP4105 50 ~ 100 BT40 0.05 ~ 0.2 fz(mm/t) 0.1 0.1 0.1 0.1 0.1 0.1
Hardened steels
(62HRC or less) ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0
ae(mm) 12 15 19 24 30 19
Q(cm3/min) 1.9 3.3 4.0 3.8 3.3 1.9
n (min-1) 1,590 1,270 1,010 ― ― 1,010
Vc(m/min) 200 200 200 ― ― 200
ステンレス鋼 JM4160 V f (mm/min) 1,430 1,910 1,820 ― ― 910
Stainless steels 150 ~ 240 BT40 0.2 ~ 0.8 fz(mm/t) 0.3 0.3 0.3 ― ― 0.3
SUS JP4120 ap(mm) 2.0 2.0 2.0 ― ― 2.0
ae(mm) 12 15 19 ― ― 19
Q(cm3/min) 34 57 69 ― ― 35
n (min-1) 1,430 1,150 910 ― ― 910
Vc(m/min) 180 180 180 ― ― 180
鋳鉄 V f (mm/min) 2,150 2,880 2,730 ― ― 1,370
Cast irons
FC JP4120 100 ~ 220 BT40 0.3 ~ 1.0 fz(mm/t) 0.5 0.5 0.5 ― ― 0.5
FCD ap(mm) 2.0 2.0 2.0 ― ― 2.0
ae(mm) 12 15 19 ― ― 19
Q(cm3/min) 52 86 104 ― ― 52
※1:「JP4105」は高硬度鋼専用材種で、生材には適しません。
※1:「JP4105」 insert's grade specialized in High hardened steel is not suitable for Non-heat-treated steel material.
【注意】 【Note】 傾斜切削・ヘリカル切削・Z方向切込み Ramping, Helical Milling, Feeding toward Z-AXIS
①JSコートは通電式タッチセンサーに反応しませんのでご注意ください。 ① Please note that the JS Coating does not cause a reaction in conductive touch 中心まで切れ刃がないため傾斜角度(θ)やZ軸方向切込み深さ(ap)に制限があります。
②不水溶性切削油は、火災の恐れがありますので使用しないでください。 sensors.
② There are restrictions to ramp angle (θ) and cutting depth (ap) toward Z-axis because of designs of cutting edge.
Due to fire risks do not use neat cutting oil as a coolant.
③排出した切りくずは飛散し作業者を切傷させ、火傷あるいは目に入って ③ The evacuation of swarf can cause burns, cuts or damage to the eyes please (mm)
負傷させる恐れがありますので、ご使用に際してはその周囲に安全カ ensure the correct safety cover is fitted around the machine, and necessary 傾斜切削 ヘリカル切削 工具径DCX
バーを取り付け保護めがね等の保護具を着用して、安全な環境で作業 personal protection equipment is worn by the machine operator. Ramping Helical milling Tool dia. φ40(r6) φ50(r6) φ63(r8) φ80(r8) φ100(r8) φ125(r8)
される事をお願い致します。 ④ These conditions are for general guidance; in actual machining conditions 推奨θ 3°以下 2°以下
adjust the parameters according to your actual machine and work-piece 穴径φ Recommended Below 3 degrees Below 2 degrees
④この切削条件表は切削条件の目安を示すものです。実際の加工では加 conditions. Hole Dia. h 2.5 2.5 2.5 2.5 2.5 2.5
工形状、目的、使用機械等により条件を調整してください。 ⑤ If vibrations are a concern due to the cutting conditions, adjust conditions by h
⑤加工状況により振動が懸念される場合は、1.切り込み深さ(ap)を低減 1.reducing cutting depth (ap) or 2.reducing per-flute feed rate (fz). ap 3.7 3.3 5.5 5.5 5.5 5.5
する 2.一刃当りの送り(fz)を低減する方法で調整ください。 ⑥ In the case of slotting, feed speed could be down to 70% of the whole. θ ap
⑦ In steel exceeding 60HRC, such as dice steel between the colds, ヘリカル穴径
⑥溝切削の場合、送り量は70%を目安としてください。 Hole Dia. 60~78 77~100 101~124 135~158 175~198 248~255
please set the sending (fz) value per one edge about to 1/2. 傾斜切込み角
⑦冷間ダイス鋼など60HRCを超える鋼種の場合は、1刃当りの送り(fz) ⑧ This table is based on the overhang of regular type (L1). Ramp milling angle 【注意】切りくずが飛散することがあります。切りくずカバーを設置してください。
値を1/2程度に設定して下さい。 工具径DCX Tool dia.
【Note】Due to swarf evacuation wear safety glasses in the vicinity of the operation.
⑧工具突き出し量は標準形の首下長さ(L1)です。
14
Page15
標準切削条件表
Recommended Cut t ing Condi t ions
ARB AR
ボア形 ボア形
Bore type Bore type
BT50 ※赤字は第 1推奨材種です。 Red indicates primary recommended insert grade.
被削材 推奨材種 切削速度 送り ) φ50(5枚刃) φ63(6枚刃)φ80(6枚刃) φ100(5枚刃) φ63(3枚刃) φ80(4枚刃) φ100(5枚刃) φ125(6枚刃)
Cutting speed 使用機械 一刃当りの
Feed per tooth 工具径DCX φ40(3枚刃
Work material Recommended (3 Flutes) r6(5 Flutes) r6 (4 Flutes) r8(5 Flutes) r8(6 Flutes) r8
inserts grade Vc( m/min) Machine fz( mm/t) Tool dia. ( 6 Flutes) r6(6 Flutes) r6(5 Flutes) r6(3 Flutes) r8
n (min-1) 1,590 1,270 1,010 800 640 1,010 800 640 510
炭素鋼 Vc(m/min) 200 200 200 200 200 200 200 200 200
合金鋼 V f (mm/min) 2,860 3,810 3,640 2,880 1,920 2,120 2,240 2,240 2,140
( ※
30HRC以下) 120 ~ 230 BT50 0.3 ~ 0.8 fz(mm/t) 0.6 0.6 0.6 0.6 0.6 0.7 0.7 0.7 0.7
Carbon steels JS4160
Alloy steels ap(mm) 2.0 2.0 2.0 2.0 2.0 2.5 2.5 2.5 2.5
(30HRC or less) ae(mm) 20 25 32 40 50 32 40 50 63
Q(cm3/min) 114 191 233 230 192 170 224 280 337
n (min-1) 1,190 950 760 600 480 760 600 480 380
合金鋼 Vc(m/min) 150 150 150 150 150 150 150 150 150
(焼入れ焼戻し材) Vf(mm/min) 1,070 1,430 1,370 1,080 720 910 960 960 910
(35HRC以下) JS4160 100 ~ 200 BT50 0.2 ~ 0.6 fz(mm/t) 0.3 0.3 0.3 0.3 0.3 0.4 0.4 0.4 0.4
Alloy steels
(Quenched and tempered steels) ap(mm) 2.0 2.0 2.0 2.0 2.0 2.5 2.5 2.5 2.5
(35HRC or less) ae(mm) 20 25 32 40 50 32 40 50 63
Q(cm3/min) 43 72 88 86 72 73 96 120 143
n (min-1) 800 640 510 400 320 510 400 320 250
プリハードン鋼・合金鋼 Vc(m/min) 100 100 100 100 100 100 100 100 100
(焼入れ焼戻し材) V f (mm/min) 480 640 610 480 320 310 320 320 300
(45HRC以下)
Pre-hardened steels JP4120 60 ~ 150 BT50 0.15~0.3 fz(mm/t) 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2
Alloy steels ap(mm) 1.5 1.5 1.5 1.5 1.5 2.0 2.0 2.0 2.0
(Quenched and tempered steels)
(45HRC or less) ae(mm) 20 25 32 40 50 32 40 50 63
Q(cm3/min) 14 24 29 29 24 20 26 32 38
n (min-1) 640 510 400 320 250 400 320 250 200
Vc(m/min) 80 80 80 80 80 80 80 80 80
焼入れ鋼 Vf(mm/min) 330 430 410 330 210 240 260 250 240
(55HRC以下) JP4105
60 ~ 100 BT50 0.15~0.3 fz(mm/t) 0.17 0.17 0.17 0.17 0.17 0.2 0.2 0.2 0.2
Hardened steels JP4120
(55HRC or less) ap(mm) 1.0 1.0 1.0 1.0 1.0 1.5 1.5 1.5 1.5
ae(mm) 20 25 32 40 50 32 40 50 63
Q(cm3/min) 6.6 11 13 13 11 12 16 19 23
n (min-1) 550 440 350 270 220 350 270 220 170
Vc(m/min) 70 70 70 70 70 70 70 70 70
焼入れ鋼 Vf(mm/min) 160 220 210 160 110 100 100 110 100
(62HRC以下) JP4105 50 ~ 100 BT50 0.05~0.2 fz(mm/t) 0.1 0.1 0.1 0.1 0.1 0.1 0.1 0.1 0.1
Hardened steels
(62HRC or less) ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
ae(mm) 20 25 32 40 50 32 40 50 63
Q(cm3/min) 3.2 5.5 6.7 6.4 5.5 3.2 4.0 5.5 6.3
n (min-1) 1,430 1,150 910 720 570 910 720 570 460
Vc(m/min) 180 180 180 180 180 180 180 180 180
ステンレス鋼 JM4160 V f (mm/min) 2,150 2,880 2,730 2,160 1,430 1,640 1,730 1,710 1,660
Stainless steels 150 ~ 240 BT50 0.2 ~ 0.8 fz(mm/t) 0.5 0.5 0.5 0.5 0.5 0.6 0.6 0.6 0.6
SUS JP4120 ap(mm) 2.0 2.0 2.0 2.0 2.0 2.5 2.5 2.5 2.5
ae(mm) 20 25 32 40 50 32 40 50 63
Q(cm3/min) 86 144 175 173 143 131 173 214 261
n (min-1) 1,430 1,150 910 720 570 910 720 570 460
Vc(m/min) 180 180 180 180 180 180 180 180 180
鋳鉄 V f (mm/min) 3,430 4,600 4,370 3,460 2,280 2,180 2,300 2,280 2,210
Cast irons
FC JP4120 100 ~ 220 BT50 0.3 ~ 1.0 fz(mm/t) 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8
FCD ap(mm) 2.0 2.0 2.0 2.0 2.0 2.5 2.5 2.5 2.5
ae(mm) 20 25 32 40 50 32 40 50 63
Q(cm3/min) 137 230 280 277 228 174 230 285 348
※1:「JP4105」は高硬度鋼専用材種で、生材には適しません。
※1:「JP4105」 insert's grade specialized in High hardened steel is not suitable for Non-heat-treated steel material.
【注意】 【Note】 傾斜切削・ヘリカル切削・Z方向切込み Ramping, Helical Milling, Feeding toward Z-AXIS
①JSコートは通電式タッチセンサーに反応しませんのでご注意ください。 ① Please note that the JS Coating does not cause a reaction in conductive touch 中心まで切れ刃がないため傾斜角度(θ)やZ軸方向切込み深さ(ap)に制限があります。
②不水溶性切削油は、火災の恐れがありますので使用しないでください。 sensors.
② There are restrictions to ramp angle (θ) and cutting depth (ap) toward Z-axis because of designs of cutting edge.
Due to fire risks do not use neat cutting oil as a coolant.
③排出した切りくずは飛散し作業者を切傷させ、火傷あるいは目に入って ③ The evacuation of swarf can cause burns, cuts or damage to the eyes please (mm)
負傷させる恐れがありますので、ご使用に際してはその周囲に安全カ ensure the correct safety cover is fitted around the machine, and necessary 傾斜切削 ヘリカル切削 工具径DCX
バーを取り付け保護めがね等の保護具を着用して、安全な環境で作業 personal protection equipment is worn by the machine operator. Ramping Helical milling Tool dia. φ40(r6) φ50(r6) φ63(r8) φ80(r8) φ100(r8) φ125(r8)
される事をお願い致します。 ④ These conditions are for general guidance; in actual machining conditions 推奨θ 3°以下 2°以下
adjust the parameters according to your actual machine and work-piece 穴径φ Recommended Below 3 degrees Below 2 degrees
④この切削条件表は切削条件の目安を示すものです。実際の加工では加 conditions. Hole Dia. h 2.5 2.5 2.5 2.5 2.5 2.5
工形状、目的、使用機械等により条件を調整してください。 ⑤ If vibrations are a concern due to the cutting conditions, adjust conditions by h
⑤加工状況により振動が懸念される場合は、1.切り込み深さ(ap)を低減 1.reducing cutting depth (ap) or 2.reducing per-flute feed rate (fz). ap 3.7 3.3 5.5 5.5 5.5 5.5
する 2.一刃当りの送り(fz)を低減する方法で調整ください。 ⑥ In the case of slotting, feed speed could be down to 70% of the whole. θ ap
⑦ In steel exceeding 60HRC, such as dice steel between the colds, ヘリカル穴径
⑥溝切削の場合、送り量は70%を目安としてください。 Hole Dia. 60~78 77~100 101~124 135~158 175~198 248~255
please set the sending (fz) value per one edge about to 1/2. 傾斜切込み角
⑦冷間ダイス鋼など60HRCを超える鋼種の場合は、1刃当りの送り(fz) ⑧ This table is based on the overhang of regular type (L1). Ramp milling angle 【注意】切りくずが飛散することがあります。切りくずカバーを設置してください。
値を1/2程度に設定して下さい。 工具径DCX Tool dia.
【Note】Due to swarf evacuation wear safety glasses in the vicinity of the operation.
⑧工具突き出し量は標準形の首下長さ(L1)です。
15
Page16
標準切削条件表
Recommended Cut t ing Condi t ions
ae
ARM
モジュラー形
Modular ap
BT40
被削材 推奨材種 切削速度 φ16(2枚刃) φ20(2枚刃) φ25(2枚刃) φ32(3枚刃) φ40(4枚刃)
Cutting speed 使用機械 一刃当りの送り
Feed per tooth 工具径DCX φ12(3枚刃)
Work material Recommended
inserts grade Vc( m/min) Machine fz( mm/t) Tool dia. ( 3 Flutes) r2.5 ( 2 Flutes) r3.5 ( 2 Flutes) r4 (2 Flutes) r5 (3 Flutes) r5 (4 Flutes) r5
n (min-1) 5,310 3,980 3,180 2,550 1,990 1,590
炭素鋼 Vc(m/min) 200 200 200 200 200 200
合金鋼 V f (mm/min) 1,590 1,590 2,540 2,040 2,390 2,540
( ※
30HRC以下) 120 ~ 230 BT40 0.1 ~ 0.8 fz(mm/t) 0.1 0.2 0.4 0.4 0.4 0.4
Carbon steels JS4160
Alloy steels ap(mm) 0.5 1.0 1.5 1.5 1.5 1.5
(30HRC or less) ae(mm) 6 8 6 8 10 12
Q(cm3/min) 4.8 13 23 24 36 46
n (min-1) 3,980 2,980 2,390 1,910 1,490 1,190
合金鋼 Vc(m/min) 150 150 150 150 150 150
(焼入れ焼戻し材) Vf(mm/min) 960 890 960 760 890 950
(35HRC以下) JS4160 100 ~ 200 BT40 0.08 ~ 0.6 fz(mm/t) 0.08 0.15 0.2 0.2 0.2 0.2
Alloy steels
(Quenched and tempered steels) ap(mm) 0.5 1.0 1.5 1.5 1.5 1.5
(35HRC or less) ae(mm) 6 8 6 8 10 12
Q(cm3/min) 2.9 7.1 8.6 9.1 13 17
n (min-1) 2,650 1,990 1,590 1,270 990 800
プリハードン鋼・合金鋼 Vc(m/min) 100 100 100 100 100 100
(焼入れ焼戻し材) V f (mm/min) 640 600 480 380 450 480
(45HRC以下)
Pre-hardened steels JP4120 60 ~ 150 BT40 0.08 ~ 0.3 fz(mm/t) 0.08 0.15 0.15 0.15 0.15 0.15
Alloy steels ap(mm) 0.5 0.6 1.0 1.0 1.0 1.0
(Quenched and tempered steels)
(45HRC or less) ae(mm) 6 8 6 8 10 12
Q(cm3/min) 1.9 2.9 2.9 3.0 4.5 5.8
n (min-1) 2,120 1,590 1,270 1,020 800 640
Vc(m/min) 80 80 80 80 80 80
焼入れ鋼 0 360 380
(55HRC以下) JP4105 Vf(mm/min) 510 320 380 31
60 ~ 100 BT40 0.05 ~ 0.3 fz(mm/t) 0.08 0.1 0.15 0.15 0.15 0.15
Hardened steels JP4120
(55HRC or less) ap(mm) 0.3 0.5 1.0 1.0 1.0 1.0
ae(mm) 6 8 6 8 10 12
Q(cm3/min) 0.9 1.3 2.3 2.5 3.6 4.6
n (min-1) 1,850 1,390 1,110 890 690 550
Vc(m/min) 70 70 70 70 70 70
焼入れ鋼 Vf(mm/min) 270 270 220 170 200 220
(62HRC以下) JP4105 50 ~ 100 BT40 0.05 ~ 0.2 fz(mm/t) 0.05 0.1 0.1 0.1 0.1 0.1
Hardened steels
(62HRC or less) ap(mm) 0.3 0.3 1.0 1.0 1.0 1.0
ae(mm) 6 8 6 8 10 12
Q(cm3/min) 0.5 0.6 1.3 1.4 2.0 2.6
n (min-1) 4,770 3,580 3,180 2,550 1,990 1,590
Vc(m/min) 180 180 200 200 200 200
ステンレス鋼 JM4160 V f (mm/min) 1,430 1,430 1,590 1,280 1,490 1,590
Stainless steels 150 ~ 240 BT40 0.1 ~ 0.8 fz(mm/t) 0.1 0.2 0.25 0.25 0.25 0.25
SUS JP4120 ap(mm) 0.5 1.0 1.5 1.5 1.5 1.5
ae(mm) 6 8 6 8 10 12
Q(cm3/min) 4.3 11 14 15 22 29
n (min-1) 4,770 3,580 2,860 2,290 1,790 1,430
Vc(m/min) 180 180 180 180 180 180
鋳鉄 V f (mm/min) 1,430 1,430 2,290 1,830 2,150 2,290
Cast irons
FC JP4120 100 ~ 220 BT40 0.1 ~ 1.0 fz(mm/t) 0.1 0.2 0.4 0.4 0.4 0.4
FCD ap(mm) 0.5 1.0 1.5 1.5 1.5 1.5
ae(mm) 6 8 6 8 10 12
Q(cm3/min) 4.3 11 21 22 32 41
※1:「JP4105」は高硬度鋼専用材種で、生材には適しません。
※1:「JP4105」 insert's grade specialized in High hardened steel is not suitable for Non-heat-treated steel material.
【注意】 【Note】 傾斜切削・ヘリカル切削・Z方向切込み Ramping, Helical Milling, Feeding toward Z-AXIS
①JSコーティングは通電式タッチセンサーに反応しませんのでご注意く ① Please note that the JS Coating does not cause a reaction in conductive touch
ださい。 sensors. 中心まで切れ刃がないため傾斜角度(θ)やZ軸方向切込み深さ(ap)に制限があります。
② Due to fire risks do not use neat cutting oil as a coolant.
②不水溶性切削油は、火災の恐れがありますので使用しないでください。 ③ The evacuation of swarf can cause burns, cuts or damage to the eyes please There are restrictions to ramp angle (θ) and cutting depth (ap) toward Z-axis because of designs of cutting edge.
③排出した切りくずは飛散し作業者を切傷させ、火傷あるいは目に入って ensure the correct safety cover is fitted around the machine, and necessary (mm)
負傷させる恐れがありますので、ご使用に際してはその周囲に安全カ personal protection equipment is worn by the machine operator. 傾斜切削 ヘリカル切削 工具径DCX
Tool dia. φ12(r2.5) φ16(r3.5) φ20(r4) φ22(r4) φ25(r5) φ28(r5) φ30(r5) φ32(r5) φ40(r5)
バーを取り付け保護めがね等の保護具を着用して、安全な環境で作業 ④ These conditions are for general guidance; in actual machining conditions Ramping Helical milling
adjust the parameters according to your actual machine and work-piece
される事をお願い致します。 推奨θ 2°以下 3°以下
conditions. 穴径φ Recommended Below 2 degrees Below 3 degrees
④この切削条件表は切削条件の目安を示すものです。実際の加工では加 ⑤ If vibrations are a concern due to the cutting conditions, adjust conditions by Hole Dia.
工形状、目的、使用機械等により条件を調整してください。 h
1.reducing cutting depth (ap) or 2.reducing per-flute feed rate (f 1 1 2 2 2 0.5 1.5 2
z). 0.8
⑥ In the case of slotting, feed speed could be down to 70% of the whole. h
⑤加工状況により振動が懸念される場合は、1.切り込み深さ(ap)を低減 ap
⑦ In steel exceeding 60HRC, such as dice steel between the colds, θ 0.8 1 2 3 3 3 3 3 3
する 2.一刃当りの送り(fz)を低減する方法で調整ください。 please set the sending (fz) value per one edge about to 1/2. ヘリカル穴径
⑥溝切削の場合、送り量は70%を目安としてください。 Hole Dia. 17~22 22~30 28~38 32~42 34~48 40~54 44~58 48~62 64~78
傾斜切込み角 ap
⑦冷間ダイス鋼など60HRCを超える鋼種の場合は、1刃当りの送り(f Ramp milling angle
z) 【注意】切りくずが飛散することがあります。切りくずカバーを設置してください。
値を1/2程度に設定して下さい。 【Note】Due to swarf evacuation wear safety glasses in the vicinity of the operation.
工具径DCX Tool dia.
16
Page17
標準切削条件表
Recommended Cut t ing Condi t ions
ARM
モジュラー形
Modular
BT50 ※赤字は第 1推奨材種です。 Red indicates primary recommended insert grade.
被削材 推奨材種 切削速度 ) φ25(2枚刃) φ32(3枚刃) φ40(4枚刃)
Work material Recommended Cutting speed 使用機械 一刃当りの送り
Feed per tooth 工具径DCX φ12(3枚刃) φ16(2枚刃) φ20(2枚刃
inserts grade Vc( m/min) Machine fz( mm/t) Tool dia. ( 3 Flutes) r2.5 ( 2 Flutes) r3.5 ( 2 Flutes) r4 (2 Flutes) r5 (3 Flutes) r5 (4 Flutes) r5
n (min-1) 5,310 3,980 3,180 2,550 1,990 1,590
炭素鋼 Vc(m/min) 200 200 200 200 200 200
合金鋼 V f (mm/min) 1,590 1,590 2,540 2,040 2,390 2,540
(30HRC以下) ※
120 ~ 230 BT50 0.1 ~ 0.8 fz(mm/t) 0.1 0.2 0.4 0.4 0.4 0.4
Carbon steels JS4160
Alloy steels ap(mm) 0.5 1.0 1.5 1.5 1.5 1.5
(30HRC or less) ae(mm) 6 8 10 13 16 20
Q(cm3/min) 4.8 13 38 40 57 76
n (min-1) 3,980 2,980 2,390 1,910 1,490 1,190
合金鋼 Vc(m/min) 150 150 150 150 150 150
(焼入れ焼戻し材) Vf(mm/min) 960 890 1,430 1,150 1,340 1,430
(35HRC以下) JS4160 100 ~ 200 BT50 0.08 ~ 0.6 fz(mm/t) 0.08 0.15 0.3 0.3 0.3 0.3
Alloy steels
(Quenched and tempered steels) ap(mm) 0.5 1.0 1.5 1.5 1.5 1.5
(35HRC or less) ae(mm) 6 8 10 13 16 20
Q(cm3/min) 2.9 7.1 21 22 32 43
n (min-1) 2,650 1,990 1,590 1,270 990 800
プリハードン鋼・合金鋼 Vc(m/min) 100 100 100 100 100 100
(焼入れ焼戻し材) V f (mm/min) 640 600 640 510 590 640
(45HRC以下)
Pre-hardened steels JP4120 60 ~ 150 BT50 0.08 ~ 0.3 fz(mm/t) 0.08 0.15 0.2 0.2 0.2 0.2
Alloy steels ap(mm) 0.5 0.6 1.0 1.0 1.0 1.0
(Quenched and tempered steels)
(45HRC or less) ae(mm) 6 8 10 13 16 20
Q(cm3/min) 1.9 2.9 6.4 6.6 9.4 13
n (min-1) 2,120 1,590 1,270 1,020 800 640
Vc(m/min) 80 80 80 80 80 80
焼入れ鋼
(55HRC以下) JP4105 Vf(mm/min) 510 320 380 310 360 380
60 ~ 100 BT50 0.05 ~ 0.3 fz(mm/t) 0.08 0.1 0.15 0.15 0.15 0.15
Hardened steels JP4120
(55HRC or less) ap(mm) 0.3 0.5 1.0 1.0 1.0 1.0
ae(mm) 6 8 10 13 16 20
Q(cm3/min) 0.9 1.3 3.8 4.0 5.8 7.6
n (min-1) 1,850 1,390 1,110 890 690 550
Vc(m/min) 70 70 70 70 70 70
焼入れ鋼 Vf(mm/min) 270 270 220 170 200 220
(62HRC以下) JP4105 50 ~ 100 BT50 0.05 ~ 0.2 fz(mm/t) 0.05 0.1 0.1 0.1 0.1 0.1
Hardened steels
(62HRC or less) ap(mm) 0.3 0.3 1.0 1.0 1.0 1.0
ae(mm) 6 8 10 13 16 20
Q(cm3/min) 0.5 0.6 2.2 2.2 3.2 4.4
n (min-1) 4,770 3,580 2,860 2,290 1,790 1,430
Vc(m/min) 180 180 180 180 180 180
ステンレス鋼 JM4160 V f (mm/min) 1,430 1,430 1,720 1,370 1,610 1,720
Stainless steels 150 ~ 240 BT50 0.1 ~ 0.8 fz(mm/t) 0.1 0.2 0.3 0.3 0.3 0.3
SUS JP4120 ap(mm) 0.5 1.0 1.5 1.5 1.5 1.5
ae(mm) 6 8 10 13 16 20
Q(cm3/min) 4.3 11 26 27 39 52
n (min-1) 4,770 3,580 2,860 2,290 1,790 1,430
Vc(m/min) 180 180 180 180 180 180
鋳鉄 V f (mm/min) 1,430 1,430 2,860 2,290 2,690 2,860
Cast irons
FC JP4120 100 ~ 220 BT50 0.1 ~ 1.0 fz(mm/t) 0.1 0.2 0.5 0.5 0.5 0.5
FCD ap(mm) 0.5 1.0 1.5 1.5 1.5 1.5
ae(mm) 6 8 10 13 16 20
Q(cm3/min) 4.3 11 43 45 65 86
※1:「JP4105」は高硬度鋼専用材種で、生材には適しません。
※1:「JP4105」 insert's grade specialized in High hardened steel is not suitable for Non-heat-treated steel material.
【注意】 【Note】 傾斜切削・ヘリカル切削・Z方向切込み Ramping, Helical Milling, Feeding toward Z-AXIS
①JSコーティングは通電式タッチセンサーに反応しませんのでご注意く ① Please note that the JS Coating does not cause a reaction in conductive touch
ださい。 sensors. 中心まで切れ刃がないため傾斜角度(θ)やZ軸方向切込み深さ(ap)に制限があります。
② Due to fire risks do not use neat cutting oil as a coolant.
②不水溶性切削油は、火災の恐れがありますので使用しないでください。 ③ The evacuation of swarf can cause burns, cuts or damage to the eyes please There are restrictions to ramp angle (θ) and cutting depth (ap) toward Z-axis because of designs of cutting edge.
③排出した切りくずは飛散し作業者を切傷させ、火傷あるいは目に入って ensure the correct safety cover is fitted around the machine, and necessary (mm)
負傷させる恐れがありますので、ご使用に際してはその周囲に安全カ personal protection equipment is worn by the machine operator. 傾斜切削 ヘリカル切削 工具径DCX
④ These conditions are for general guidance; in actual machining conditions Ramping Helical milling Tool dia. φ12(r2.5) φ16(r3.5) φ20(r4) φ22(r4) φ25(r5) φ28(r5) φ30(r5) φ32(r5) φ40(r5)
バーを取り付け保護めがね等の保護具を着用して、安全な環境で作業 adjust the parameters according to your actual machine and work-piece
される事をお願い致します。 推奨θ 2°以下 3°以下
conditions. 穴径φ Recommended Below 2 degrees Below 3 degrees
④この切削条件表は切削条件の目安を示すものです。実際の加工では加 ⑤ If vibrations are a concern due to the cutting conditions, adjust conditions by Hole Dia.
工形状、目的、使用機械等により条件を調整してください。 h
1.reducing cutting depth (ap) or 2.reducing per-flute feed rate (fz). 0.8 1 1 2 2 2 0.5 1.5 2
⑥ In the case of slotting, feed speed could be down to 70% of the whole. h
⑤加工状況により振動が懸念される場合は、1.切り込み深さ(ap)を低減 ⑦ In steel exceeding 60HRC, such as dice steel between the colds, θ ap 0.8 1 2 3 3 3 3 3 3
する 2.一刃当りの送り(fz)を低減する方法で調整ください。 please set the sending (fz) value per one edge about to 1/2. ヘリカル穴径
Hole Dia. 17~22 22~30 28~38 32~42 34~48 40~54 44~58 48~62 64~78
⑥溝切削の場合、送り量は70%を目安としてください。 傾斜切込み角 ap
⑦冷間ダイス鋼など60HRCを超える鋼種の場合は、1刃当りの送り(fz) Ramp milling angle 【注意】切りくずが飛散することがあります。切りくずカバーを設置してください。
値を1/2程度に設定して下さい。 【Note】Due to swarf evacuation wear safety glasses in the vicinity of the operation.
工具径DCX Tool dia.
17
Page18
切削性能
Cutt ing performance
特長 Features
<2>φ20(レギュラー・ロング・エキストラロング)の切削領域
ンサートにより高送りが可能 Milling range of the φ20 (Regular, Long, Extra Long)
01 丸駒イ 02 強固なダブルクランプ機構
High-feed machining is possible by using the round-insert. Strong double-Clamping Structure
被削材:S50C(220HB)
● 従来工具の2倍~3倍の送り量が可能です。 ● クサビまたはクランプねじ1本では、インサートが動いた Work material
・It is able to feed two or three times faster than conventional one. りねじが緩んだりなどのトラブルが発生していましたが、 5 vc =200m/min(n=3,200min-1) レギュラー
v Regular
f = 144mm/min(fz =0.22mm/t) ARS0020R
2 fz=0.3~0.6mm/t クランプねじとクランプ駒による強固なダブルクランプ
4
方式により解決しました。 レギュラーの溝切削でap=3mm可能に対し、
ロング
・There could be some troubles 3 Long エキストラロングはap=0.2mmとなり
1 like moving of the inserts or ARL0020R 大幅に使用領域が狭くなることにご注意ください。
fz=0.1~0.2mm/t loosening of the screws, in case 切削可能領域
of single clamping l ike only 2 Milling range Please be careful that application range of slotting
0
快削形 wedges or screws. By strong
アルファ ラジアス クランプ駒 エキストラロング Extra Long becomes narrow.
alpha Radius Mill double-clamping structure using Clamp piece ARE0020R ap=3mm is possible by regular,but ap=0.2mm is maximum.
both clamp screws and clamp 1 by extra-long.
従来工具(刃先交換式エンドミル) pieces, those troubles have クランプねじ
Conventional tool (Indexable End Mill) Clamp screw
been solved.
0 5 10 15 20 25
03 傾斜切削・ヘリカル切削・Z方向切込み Ramping, Helical Milling, Feeding toward Z-AXIS 切込み幅 ae Cutting width (mm)
● 中心まで切れ刃がないため傾斜角度 傾斜切削 ヘリカル切削
(θ)やZ軸方向切込み深さ(ap)に Ramping 穴径φ Helical milling <3>φ25(レギュラー・ロング・エキストラロング)の切削領域 <4>φ32(レギュラー・ロング・エキストラロング)の切削領域
Hole diameter
制限があります。 h Milling range of the φ25 (Regular, Long, Extra Long) Milling range of the φ32 (Regular, Long, Extra Long)
・There are restrictions to Ramp angle (θ) and
cutting depth (ap) toward Z-axis because of θ 被削材:S50C(220HB) レギュラー 被削材:S50C(220HB) レギュラー
designs of cutting edge. ap
傾斜切込み角 Work material egular
Regular Work material R
S3025R 5 vc =200m/min(n=2,000min-1)
Ramp milling angle
工具径DCX 5 vc =200m/min(n=2,550min-1) AR ARS3032R
Tool dia. vf =1,350mm/min(fz =0.26mm/t) vf =1,350mm/min(fz =0.3mm/t)
ロング
Long
04 ダイレクトに彫り込み加工が可能 RL3025R
Direct machining is possible 4 A 4
ロング
● 傾斜切削の応用例で下穴がなくてもダイレクトに切込み、ポケットの繰り広げ加工ができます。 3 3 Long
ARL3032R
従って、従来のドリル下穴加工が省略でき、工具本数の削減がはかれます。 切削可能領域
・By application of slant milling, if there is no pilot hole, direct milling and expanding of pocket are possible, So that, there is no need to make pilot hole by 2 2 Milling range
using drills. Consequently, reduction of tools are possible. 切削可能領域 エキストラロング
Milling range Extra Long
アルファ ラジアスミル加工法 従来加工法 1 ARE3025R 1
エキストラロング Extra Long
alpha Radius Milling Conventional milling ARE3032R
①干渉物ない場合 ②多少スペースあり ③干渉物がある場合 0
No interference Some spaces Some interferences 5 10 15 20 25 0 5 10 15 20 25 30
4辺連続傾斜 往復傾斜 下穴あり 切込み幅 ae Cutting width (mm) 切込み幅 ae Cutting width (mm)
4 times serial slant Two ways slant pilot hole
実績は語る Field Data
(傾斜+繰広げ) (傾斜+繰広げ) (傾斜+繰広げ) (ドリル+繰広げ)
Slant + expand Slant + expand Slant + expand Drilling + expand 工具径DCX 使用条件 Cutting conditions
No. ユーザー インサート材種 被削材 結 果
Tool dia. User Insert grade Work material vc m/min vf mm/min Result
n(min-1) fz(mm/t) ap × ae:mm
切削領域 Cutting region
1 JS4160相当 SCM 188 2,500
50 A社 ap=1.0 中仕上げ加工で約10時間加工し安定した加工が可能。
Company A Equivalent to
JS4160 (35HRC)(1,200)(0.69) ae=1.0~2.0 Enabled stable semi-finishing processing approx. 10 hours.
<1>r8丸駒インサートとr10丸駒インサート(従来品 アルファ ラジアスミルRD形)の領域比較
Range comparison between r 8 round-insert and r 10 round-insert (conventional alpha Radius Mill RD type). 2 32 B社 JP4120相当 P21 200 3,000 ap=0.5 従来品に比べ1.5倍の長寿命。
Company B Equivalent to
JP4120 (40HRC)(2,000)(0.5) ae=15 1.5× the tool life of conventional products.
形状加工における溝切削や彫り下げ加工等のびびりを生じ易い個所にr8丸駒インサートが有効です。
r 8 round-insert is useful on the unstable cutting like Slotting or Die-Sinking. 3 80 C社 JS4160相当 S50C 120 1,150 ap=1.2 従来品に比べ2倍の長寿命。
Company C Equivalent to
JS4160 (220HB)(480) (0.6) ae=50 2× the tool life of conventional products.
被削材:S50C(220HB)
6 Work material
工具径:φ63×3NT
5 アルファ ラジアスミル Tool dia.
alpha Radius Mill 従来品工具に対する特長 Features comparing with conventional product
4 ARS5063R vc =168m/min(n =850min-1)
(r8インサート使用) vf =800mm/min(fz =0.314mm/t) AR形 従来品A Conventional A 従来品B Conventional B
r 8 insert use
3 面削り Face milling ○ ○ ○
従来品 ap =5mm溝切削
Conventional 肩削り Side milling ○ ○ ○
(r10インサート使用) Slotting
2 r 10 insert use 溝削り Slotting ○ ○ × (N/A)
ヘリカル加工 Helical milling ○ △ × (N/A)
1 従来品は、軸方向の切込み回数が2回目以降になるとびびりを生じます。
これに対し、r8インサートは6回まで軽快に切削できました。 走査線加工 Scanning path ○ △ × (N/A)
等高線加工 Contouring path ○ ○ ○
0 10 20 30 40 50 60 70 Conventional products experience chatter starting from the second axial cut onward.
切りくず排出性 Chip removal ○ △ × (N/A)
a In contrast, the r 8 insert was able to cut smoothly for up to six cuts.
切込み幅 e Cutting width (mm) 難削材に対する特性 For difficult to cut material ○ △ △
18
軸方向切込み回数(回)
Cutting times (times)
切削能率(×倍)
Milling Efficiency(×times)
切込み深さ ap 切込み深さ ap
Depth of Cut (mm) Depth of Cut (mm)
切込み深さ ap
Depth of Cut (mm)
Page19
切削性能
Cutt ing performance
特長 Features
<2>φ20(レギュラー・ロング・エキストラロング)の切削領域
ンサートにより高送りが可能 Milling range of the φ20 (Regular, Long, Extra Long)
01 丸駒イ 02 強固なダブルクランプ機構
High-feed machining is possible by using the round-insert. Strong double-Clamping Structure
被削材:S50C(220HB)
● 従来工具の2倍~3倍の送り量が可能です。 ● クサビまたはクランプねじ1本では、インサートが動いた Work material
・It is able to feed two or three times faster than conventional one. りねじが緩んだりなどのトラブルが発生していましたが、 5 vc =200m/min(n=3,200min-1) レギュラー
v Regular
f = 144mm/min(fz =0.22mm/t) ARS0020R
2 fz=0.3~0.6mm/t クランプねじとクランプ駒による強固なダブルクランプ
4
方式により解決しました。 レギュラーの溝切削でap=3mm可能に対し、
ロング
・There could be some troubles 3 Long エキストラロングはap=0.2mmとなり
1 like moving of the inserts or ARL0020R 大幅に使用領域が狭くなることにご注意ください。
fz=0.1~0.2mm/t loosening of the screws, in case 切削可能領域
of single clamping l ike only 2 Milling range Please be careful that application range of slotting
0
快削形 wedges or screws. By strong
アルファ ラジアス クランプ駒 エキストラロング Extra Long becomes narrow.
alpha Radius Mill double-clamping structure using Clamp piece ARE0020R ap=3mm is possible by regular,but ap=0.2mm is maximum.
both clamp screws and clamp 1 by extra-long.
従来工具(刃先交換式エンドミル) pieces, those troubles have クランプねじ
Conventional tool (Indexable End Mill) Clamp screw
been solved.
0 5 10 15 20 25
03 傾斜切削・ヘリカル切削・Z方向切込み Ramping, Helical Milling, Feeding toward Z-AXIS 切込み幅 ae Cutting width (mm)
● 中心まで切れ刃がないため傾斜角度 傾斜切削 ヘリカル切削
(θ)やZ軸方向切込み深さ(ap)に Ramping 穴径φ Helical milling <3>φ25(レギュラー・ロング・エキストラロング)の切削領域 <4>φ32(レギュラー・ロング・エキストラロング)の切削領域
Hole diameter
制限があります。 h Milling range of the φ25 (Regular, Long, Extra Long) Milling range of the φ32 (Regular, Long, Extra Long)
・There are restrictions to Ramp angle (θ) and
cutting depth (ap) toward Z-axis because of θ 被削材:S50C(220HB) レギュラー 被削材:S50C(220HB) レギュラー
designs of cutting edge. ap
傾斜切込み角 Work material egular
Regular Work material R
S3025R 5 vc =200m/min(n=2,000min-1)
Ramp milling angle
工具径DCX 5 vc =200m/min(n=2,550min-1) AR ARS3032R
Tool dia. vf =1,350mm/min(fz =0.26mm/t) vf =1,350mm/min(fz =0.3mm/t)
ロング
Long
04 ダイレクトに彫り込み加工が可能 RL3025R
Direct machining is possible 4 A 4
ロング
● 傾斜切削の応用例で下穴がなくてもダイレクトに切込み、ポケットの繰り広げ加工ができます。 3 3 Long
ARL3032R
従って、従来のドリル下穴加工が省略でき、工具本数の削減がはかれます。 切削可能領域
・By application of slant milling, if there is no pilot hole, direct milling and expanding of pocket are possible, So that, there is no need to make pilot hole by 2 2 Milling range
using drills. Consequently, reduction of tools are possible. 切削可能領域 エキストラロング
Milling range Extra Long
アルファ ラジアスミル加工法 従来加工法 1 ARE3025R 1
エキストラロング Extra Long
alpha Radius Milling Conventional milling ARE3032R
①干渉物ない場合 ②多少スペースあり ③干渉物がある場合 0
No interference Some spaces Some interferences 5 10 15 20 25 0 5 10 15 20 25 30
4辺連続傾斜 往復傾斜 下穴あり 切込み幅 ae Cutting width (mm) 切込み幅 ae Cutting width (mm)
4 times serial slant Two ways slant pilot hole
実績は語る Field Data
(傾斜+繰広げ) (傾斜+繰広げ) (傾斜+繰広げ) (ドリル+繰広げ)
Slant + expand Slant + expand Slant + expand Drilling + expand 工具径DCX 使用条件 Cutting conditions
No. ユーザー インサート材種 被削材 結 果
Tool dia. User Insert grade Work material vc m/min vf mm/min Result
n(min-1) fz(mm/t) ap × ae:mm
切削領域 Cutting region
1 JS4160相当 SCM 188 2,500
50 A社 ap=1.0 中仕上げ加工で約10時間加工し安定した加工が可能。
Company A Equivalent to
JS4160 (35HRC)(1,200)(0.69) ae=1.0~2.0 Enabled stable semi-finishing processing approx. 10 hours.
<1>r8丸駒インサートとr10丸駒インサート(従来品 アルファ ラジアスミルRD形)の領域比較
Range comparison between r 8 round-insert and r 10 round-insert (conventional alpha Radius Mill RD type). 2 32 B社 JP4120相当 P21 200 3,000 ap=0.5 従来品に比べ1.5倍の長寿命。
Company B Equivalent to
JP4120 (40HRC)(2,000)(0.5) ae=15 1.5× the tool life of conventional products.
形状加工における溝切削や彫り下げ加工等のびびりを生じ易い個所にr8丸駒インサートが有効です。
r 8 round-insert is useful on the unstable cutting like Slotting or Die-Sinking. 3 80 C社 JS4160相当 S50C 120 1,150 ap=1.2 従来品に比べ2倍の長寿命。
Company C Equivalent to
JS4160 (220HB)(480) (0.6) ae=50 2× the tool life of conventional products.
被削材:S50C(220HB)
6 Work material
工具径:φ63×3NT
5 アルファ ラジアスミル Tool dia.
alpha Radius Mill 従来品工具に対する特長 Features comparing with conventional product
4 ARS5063R vc =168m/min(n =850min-1)
(r8インサート使用) vf =800mm/min(fz =0.314mm/t) AR形 従来品A Conventional A 従来品B Conventional B
r 8 insert use
3 面削り Face milling ○ ○ ○
従来品 ap =5mm溝切削
Conventional 肩削り Side milling ○ ○ ○
(r10インサート使用) Slotting
2 r 10 insert use 溝削り Slotting ○ ○ × (N/A)
ヘリカル加工 Helical milling ○ △ × (N/A)
1 従来品は、軸方向の切込み回数が2回目以降になるとびびりを生じます。
これに対し、r8インサートは6回まで軽快に切削できました。 走査線加工 Scanning path ○ △ × (N/A)
等高線加工 Contouring path ○ ○ ○
0 10 20 30 40 50 60 70 Conventional products experience chatter starting from the second axial cut onward.
切りくず排出性 Chip removal ○ △ × (N/A)
a In contrast, the r 8 insert was able to cut smoothly for up to six cuts.
切込み幅 e Cutting width (mm) 難削材に対する特性 For difficult to cut material ○ △ △
19
軸方向切込み回数(回)
Cutting times (times)
切削能率(×倍)
Milling Efficiency(×times)
切込み深さ ap 切込み深さ ap
Depth of Cut (mm) Depth of Cut (mm)
切込み深さ ap
Depth of Cut (mm)
Page20
図、表等のデータは試験結果の一例であり、保証値ではありません。
「 」は株式会社MOLDINOの登録商標です。
The diagrams and table data are examples of test results, and are not guaranteed values.
“ ” is a registered trademark of MOLDINO Tool Engineering, Ltd.
安 全 上 の ご 注 意 Attentions on Safety
1. 取扱上のご注意 1. Attentions regarding handling
(1)工具をケース(梱包)から取り出す際は、足元への落下あるいは素手の指先へ落して怪我をしないよ (1) When removing the tool from the case (package), be careful not to drop it on your foot or
うに十分なご注意をお願いします。 drop it onto the tips of your bare fingers.
(2)インサートをセットして実際にご使用する場合は、切れ刃を素手で直接触れないように注意してください。 (2) When actually setting the inserts, be careful not to touch the cutting flute directly with
2. 取付け時のご注意 your bare hands.
(1)ご使用にあたって、インサートのセッティングは確実に行っていただき、アーバ等への取付けも確実に 2. Attentions regarding mounting
行ってください。 (1) When preparing for use, be sure that the inserts are firmly mounted in place and that they
(2)ご使用中に、異常な振動等が発生した場合は、直ちに機械を停止させて、その振動の原因を除いて are firmly mounted on the arbor, etc.
ください。 (2) If abnormal chattering occurs during use, stop the machine immediately and remove the
cause of the chattering.
3. 使用上のご注意
(1)切削工具あるいは被削材の寸法・回転の方向は、あらかじめ確認しておいてください。 3. Attentions during use
(1) Before use, confirm the dimensions and direction of rotation of the tool and milling work
(2)標準切削条件表の数値は、新しい作業の立上げの目安としてご利用ください。切込みが大きい場合、 material.
使用機械の剛性が小さい場合あるいは被加工物の性状に応じて切削条件を適正に調整してご使用 (2) The numerical values in the standard cutting conditions table should be used as criteria when
ください。 starting new work. The cutting conditions should be adjusted as appropriate when the cutting
(3)インサートは硬質の材料です。ご使用中に破損して飛散する場合があります。また、切りくずが飛散す depth is large, the rigidity of the machine being used is low, or according to the conditions of
ることがあります。これらの飛散物等は作業者を切傷させ、火傷あるいは目に入って負傷させる恐れが the work material.
ありますので、工具をご使用中はその周囲に安全カバーを取付け、保護めがね等の保護具を着用し (3) The inserts are made of a hard material. During use, they may break and fly off. In addition,
て安全な環境下での作業をお願いいたします。 cutting chips may also fly off. Since there is a danger of injury to workers, fire, or eye damage
・引火や爆発の危険のあるところでは使用しないでください。 from such flying pieces, a safety cover should be installed and safety equipment such as
・不水溶性切削油は、火災の恐れがありますので使用しないでください。 safety glasses should be worn to create a safe environment for work.
(4)工具を本来の目的以外に使用したり、改造したりしないでください。 ・Do not use where there is a risk of fire or explosion.
・Do not use non-water-soluble cutting oils. Such oils may result in fire.
4. 工具に関して、安全上の問題点・不明の点・その他ご相談がありましたら フリーダイヤル技術相談 へ (4) Do not use the tool for any purpose other than that for which it is intended, and do not modify it.
お問い合わせください。
ホームページ フリーダイヤル技術相談
https://www.moldino.com
MOLDINO Tool Engineering, Ltd.
本社 〒130-0026 東京都墨田区両国4-31-11(ヒューリック両国ビル8階) 工具選定データベース【 TOOLSEARCH】
03-6890-5101 FAX 03-6890-5134
International Sales Dept .: +81-3-6890-5103 FAX +81-3-6890-5128
営業企画部 ☎03-6890-5102 FAX03-6890-5134 海外営業部 ☎03-6890-5103 FAX03-6890-5128
東京営業所 ☎03-6890-5110 FAX03-6890-5133 静岡営業所 ☎054-273-0360 FAX054-273-0361
東北営業所 ☎022-208-5100 FAX022-208-5102 名古屋営業所 ☎052-687-9150 FAX052-687-9144
新潟営業所 ☎0258-87-1224 FAX0258-87-1158 大阪営業所 ☎06-7668-0190 FAX06-7668-0194
東関東営業所 ☎0294-88-9430 FAX0294-88-9432 中四営業所 ☎082-536-2001 FAX082-536-2003
長野営業所 ☎0276-59-6001 FAX0276-59-6005 九州営業所 ☎092-289-7010 FAX092-289-7012
北関東営業所 ☎0276-59-6001 FAX0276-59-6005
神奈川営業所 ☎046-400-9429 FAX046-400-9435
ヨーロッパ/MOLDINO Tool Engineering Europe GmbH Itterpark 12, 40724 Hilden, Germany. TEL : +49-(0)2103-24820, FAX : +49-(0)2103-248230
アメリカ/MITSUBISHI MATERIALS U.S.A. CORPORATION Detroit office c/o RFM Inc. Customer service 2001 Orndorf Drive, Brighton, MI 48116 U.S.A. TEL : +1(248)308-2620, FAX :+1(248)308-2627
メキシコ/MITSUBISHI MATERIALS MÉXICO S.A. DE C.V. Av. La Cañada No.16, Parque Industrial Bernardo Quintana, El Marques, Querétaro, CP 76246, México TEL : +52-442-1926800
ブラジル/MITSUBISHI MATERIALS BRASIL LTDA. Rua Cincinato Braga, 340 13° andar.Bela Vista – CEP 01333-010 São Paulo – SP ., Brasil TEL : +55(11)3506-5600 FAX : +55(11)3506-5677
タ イ/MITSUBISHI MATERIALS (THAILAND) CO., LTD. 139/3 Moo 2, Tambon Khlong Chik, Amphoe Bang Pa-in, Phra Nakhon Si Ayutthaya 13160, Thailand TEL:+66-3525-8024
イ ン ド/Mitsubishi Materials India Private Limited H.O.: Prasad Enclave, #118/119, 1st Floor, 2nd Stage, 5th main, BBMP Ward #11, (New #38), Industrial Suburb, Yeshwanthpura, Bengaluru, 560 022, Karnataka, India. Tel : +91-80-2204-3600
予告なく、改良・改善のために仕様変更することがあります。
Specifications for the products listed in this catalog are subject to change without notice due to ベジタブルインクで印刷しています。 2026-10(ME)
replacement or modification. Printed using vegetable oil ink. Printed in JAPAN 2012-2:FP