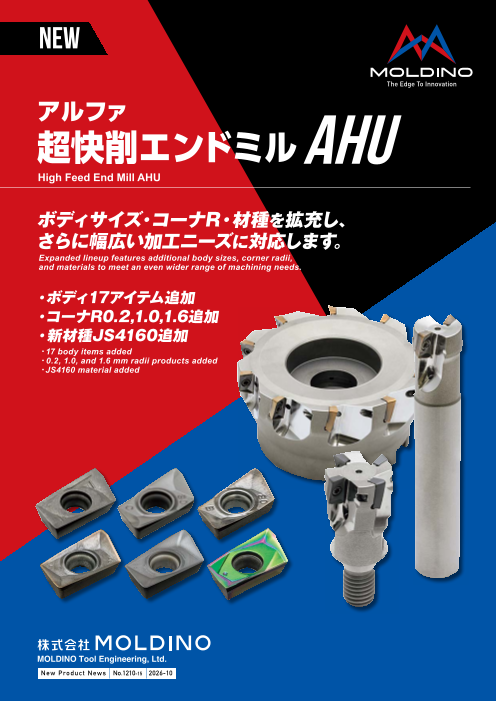


ボディサイズ・コーナR・材種を拡充し、さらに幅広い加工ニーズに対応します。
◆傾斜切削も可能な多機能形に進化しました。
◆一般鋼から難削材まで幅広く対応。タービンブレード加工に好適です。
◆詳細はカタログをダウンロードしご覧いただくか、お気軽にお問い合わせ下さい。
このカタログについて
| ドキュメント名 | アルファ 超快削エンドミル AHU |
|---|---|
| ドキュメント種別 | 製品カタログ |
| ファイルサイズ | 3.3Mb |
| 登録カテゴリ | |
| 取り扱い企業 | 株式会社MOLDINO (この企業の取り扱いカタログ一覧) |
この企業の関連カタログ

このカタログの内容
Page1
NEW
アルファ
超快削エンドミルAHU
High Feed End Mill AHU
ボディサイズ・コーナR・材種を拡充し、
さらに幅広い加工ニーズに対応します。
Expanded lineup features additional body sizes, corner radii,
and materials to meet an even wider range of machining needs.
・ボディ17アイテム追加
・コーナR0.2,1.0,1.6追加
・新材種JS4160追加
・17 body items added
・0.2, 1.0, and 1.6 mm radii products added
・JS4160 material added
MOLDINO Tool Engineering, Ltd.
New Produc t News No.1210-15 2026-10
Page2
テクノロジー
Technology
不安定加工
Unstable machining JM4160 荒 中仕上 FW刃形の特長と性能 FW Cutting Edge Features and Performance
安定加工 JS4160 JP4120 JP4120 JP4120 SJPD4510210 HD7010
Stable machining 加工 Roughing Semi
炭素鋼 合金鋼 プリハードン鋼 ステンレス鋼 SUS 鋳鉄 アルミニウム合金 グラファイト 用途 Finishing
合金鋼 (焼入れ焼戻し材) 合金鋼 耐熱合金 FC・FCD 銅合金 CFRP
(30HRC以下)(35HRC以下)(焼入れ焼戻し材) 超耐熱合金 Applications 良好な立壁加工面
(45HRC以下) チタン合金 Outstanding vertical wall machining surfaces
Carbon steels Alloy steels Pre-hardened steels Stainless steels Cast irons Aluminum alloys Graphite
Alloy steels (Quenched and tempered steels) Alloy steels Heat resistant alloys Copper alloys
(30HRC or less) (35HRC or less)(Quenched and tempered steels) Super heat resistant alloys
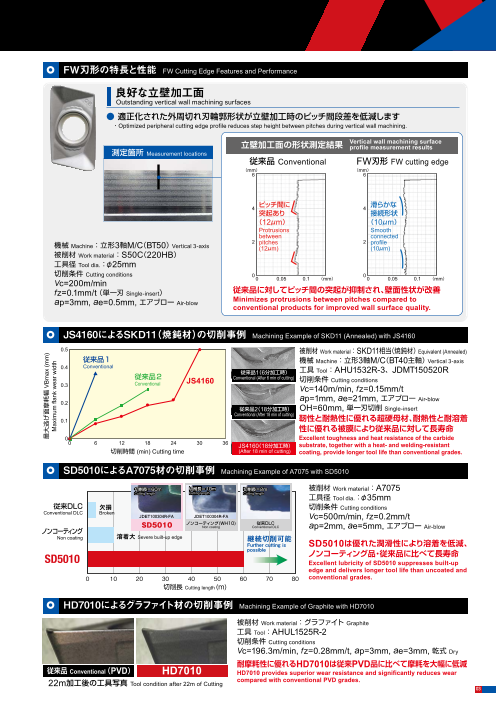
(45HRC or less) Titanium alloys ● 適正化された外周切れ刃輪郭形状が立壁加工時のピッチ間段差を低減します
・Optimized peripheral cutting edge profile reduces step height between pitches during vertical wall machining.
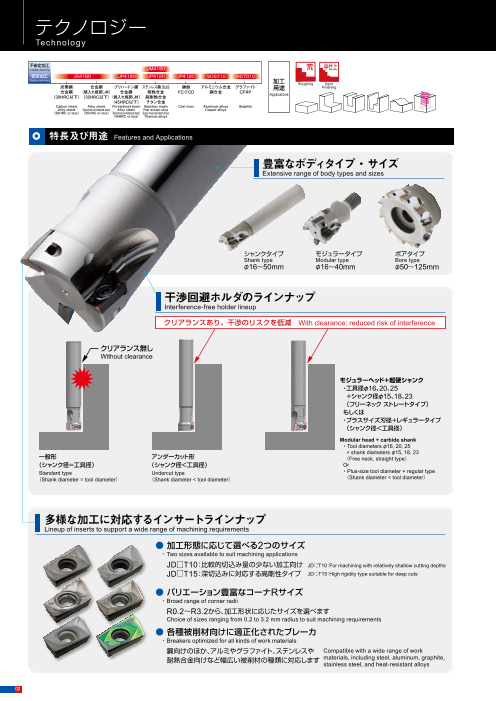
特長及び用途 Features and Applications
立壁加工面の形状測定結果 Vertical wall machining surface
profile measurement results
測定箇所 Measurement locations
豊富なボディタイプ・サイズ 従来品 Conventional FW刃形 FW cutting edge
Extensive range of body types and sizes (mm) (mm)
6 6
4 ピッチ間に 4 滑らかな
突起あり 接続形状
(12μm) (10μm)
Protrusions Smooth
between connected
機械 Machine:立形3軸M/C(BT50) 2
Vertical 3-axis pitches 2 profile
(12μm) (10μm)
シャンクタイプ モジュラータイプ ボアタイプ 被削材 Work material:S50C(220HB)
Shank type Modular type Bore type
φ16~50mm φ16~40mm φ50~125mm 工具径 Tool dia.:φ25mm
切削条件 Cutting conditions 0 0 0.05 0.1 (mm) 0 0 0.05 0.1 (mm)
Vc=200m/min
fz=0.1mm/t( 単一刃 Single-insert) 従来品に対してピッチ間の突起が抑制され、壁面性状が改善
干渉回避ホルダのラインナップ
Interference-free holder lineup ap=3mm, ae=0.5mm, エアブロー Air-blow Minimizes protrusions between pitches compared to
conventional products for improved wall surface quality.
クリアランスあり。干渉のリスクを低減 Wi th clearance: reduced risk of interference
JS4160によるSKD11(焼鈍材)の切削事例 Machining Example of SKD11 (Annealed) with JS4160
クリアランス無し 0.5 被削材 Work material:SKD11相当(焼鈍材) Equivalent (Annealed)
Without clearance 従来品1 機械 Machine:立形3軸M/C(BT40主軸) Vertical 3-axis
0.4 Conventional
従来品1(6分加工時) 工具 Tool:AHU1532R-3、JDMT150520R
モジュラーヘッド+超硬シャンク 従来品2
0.3 Conventional JS4160 Conventional (After 6 min of cutting) 切削条件 Cutting conditions
・工具径φ16、20、25 Vc=140m/min, fz=0.15mm/t
+シャンク径φ15、18、23 ap=1mm, ae=21mm, エアブロー Air-blow
(フリーネック ストレートタイプ) 0.2
もしくは 従来品2(18分加工時) OH=60mm, 単一刃切削 Single-insert
Conventional (After 18 min of cutting)
・プラスサイズ刃径+レギュラータイプ 0.1 靭性と耐熱性に優れる超硬母材、耐熱性と耐溶着
(シャンク径<工具径) 性に優れる被膜により従来品に対して長寿命
Modular head + carbide shank 0 Excellent toughness and heat resistance of the carbide
・Tool diameters φ16, 20, 25 0 6 12 18 24 30 36 JS4160(18分加工時) substrate, together with a heat- and welding-resistant
+ shank diameters φ15, 18, 23 切削時間 (min) Cutting time (After 18 min of cutting) coating, provide longer tool life than conventional grades.
一般形 アンダーカット形 (Free neck, straight type)
(シャンク径=工具径) (シャンク径<工具径) Or
Standard type Undercut type ・Plus-size tool diameter + regular type SD5010によるA7075材の切削事例 Machining Example of A7075 with SD5010
(Shank diameter = tool diameter) (Shank diameter < tool diameter) (Shank diameter < tool diameter)
切削長=60m 切削長=10m 切削長=2m 被削材 Work material:A7075
Cutting length Cutting length Cutting length
工具径 Tool dia.:φ35mm
従来DLC 欠損 切削条件 Cutting conditions
Conventional DLC Broken
多様な加工に対応するインサートラインナップ JDET100304R-FA JDET100304R-FA Vc=500m/min, fz=0.2mm/t
SD5010 ノンコーティング(WH10) 従来DLC
Lineup of inserts to support a wide range of machining requirements Non coating Conventional DLC ap=2mm, ae=5mm, エアブロー Air-blow
ノンコーティング
Non coating 溶着大 Severe built-up edge 継続切削可能
● 加工形態に応じて選べる2つのサイズ Further cutting is SD5010は優れた潤滑性により溶着を低減、
possible
・Two sizes available to suit machining applications ノンコーティング品・従来品に比べて長寿命
JD T10:比較的切込み量の少ない加工向け JD T10:For machining with relatively shallow cutting depths Excellent lubricity of SD5010 suppresses built-up
JD T15:深切込みに対応する高剛性タイプ edge and delivers longer tool life than uncoated and
JD T15:High rigidity type suitable for deep cuts
0 10 20 30 40 50 60 70 80 conventional grades.
切削長 Cutting length (m)
● バリエーション豊富なコーナRサイズ
・Broad range of corner radii HD7010によるグラファイト材の切削事例 Machining Example of Graphite with HD7010
R0.2~R3.2から、加工形状に応じたサイズを選べます
Choice of sizes ranging from 0.2 to 3.2 mm radius to suit machining requirements 被削材 Work material:グラファイト Graphite
● 各種被削材向けに適正化されたブレーカ 工具 Tool:AHUL1525R-2
・Breakers optimized for all kinds of work materials 切削条件 Cutting conditions
鋼向けのほか、アルミやグラファイト、ステンレスや Compatible with a wide range of work Vc=196.3m/min, fz=0.28mm/t, ap=3mm, ae=3mm, 乾式 Dry
耐熱合金向けなど幅広い被削材の種類に対応します materials, including steel, aluminum, graphite,
stainless steel, and heat-resistant alloys 耐摩耗性に優れるHD7010は従来PVD品に比べて摩耗を大幅に低減
従来品 Conventiona(l PVD) HD7010 HD7010 provides superior wear resistance and significantly reduces wear
22m加工後の工具写真 compared with conventional PVD grades.
Tool condition after 22m of Cutting
02
最大逃げ面摩耗幅 VBmax (mm)
Maximum flank wear width
Page3
テクノロジー
Technology
不安定加工
Unstable machining JM4160 荒 中仕上 FW刃形の特長と性能 FW Cutting Edge Features and Performance
安定加工 JS4160 JP4120 JP4120 JP4120 SJPD4510210 HD7010
Stable machining 加工 Roughing Semi
炭素鋼 合金鋼 プリハードン鋼 ステンレス鋼 SUS 鋳鉄 アルミニウム合金 グラファイト 用途 Finishing
合金鋼 (焼入れ焼戻し材) 合金鋼 耐熱合金 FC・FCD 銅合金 CFRP
(30HRC以下)(35HRC以下)(焼入れ焼戻し材) 超耐熱合金 Applications 良好な立壁加工面
(45HRC以下) チタン合金 Outstanding vertical wall machining surfaces
Carbon steels Alloy steels Pre-hardened steels Stainless steels Cast irons Aluminum alloys Graphite
Alloy steels (Quenched and tempered steels) Alloy steels Heat resistant alloys Copper alloys
(30HRC or less) (35HRC or less)(Quenched and tempered steels) Super heat resistant alloys
(45HRC or less) Titanium alloys ● 適正化された外周切れ刃輪郭形状が立壁加工時のピッチ間段差を低減します
・Optimized peripheral cutting edge profile reduces step height between pitches during vertical wall machining.
特長及び用途 Features and Applications
立壁加工面の形状測定結果 Vertical wall machining surface
profile measurement results
測定箇所 Measurement locations
豊富なボディタイプ・サイズ 従来品 Conventional FW刃形 FW cutting edge
Extensive range of body types and sizes (mm) (mm)
6 6
4 ピッチ間に 4 滑らかな
突起あり 接続形状
(12μm) (10μm)
Protrusions Smooth
between connected
機械 Machine:立形3軸M/C(BT50) 2
Vertical 3-axis pitches 2 profile
(12μm) (10μm)
シャンクタイプ モジュラータイプ ボアタイプ 被削材 Work material:S50C(220HB)
Shank type Modular type Bore type
φ16~50mm φ16~40mm φ50~125mm 工具径 Tool dia.:φ25mm
切削条件 Cutting conditions 0 0 0.05 0.1 (mm) 0 0 0.05 0.1 (mm)
Vc=200m/min
fz=0.1mm/t( 単一刃 Single-insert) 従来品に対してピッチ間の突起が抑制され、壁面性状が改善
干渉回避ホルダのラインナップ
Interference-free holder lineup ap=3mm, ae=0.5mm, エアブロー Air-blow Minimizes protrusions between pitches compared to
conventional products for improved wall surface quality.
クリアランスあり。干渉のリスクを低減 Wi th clearance: reduced risk of interference
JS4160によるSKD11(焼鈍材)の切削事例 Machining Example of SKD11 (Annealed) with JS4160
クリアランス無し 0.5 被削材 Work material:SKD11相当(焼鈍材) Equivalent (Annealed)
Without clearance 従来品1 機械 Machine:立形3軸M/C(BT40主軸) Vertical 3-axis
0.4 Conventional
従来品1(6分加工時) 工具 Tool:AHU1532R-3、JDMT150520R
モジュラーヘッド+超硬シャンク 従来品2
0.3 Conventional JS4160 Conventional (After 6 min of cutting) 切削条件 Cutting conditions
・工具径φ16、20、25 Vc=140m/min, fz=0.15mm/t
+シャンク径φ15、18、23 ap=1mm, ae=21mm, エアブロー Air-blow
(フリーネック ストレートタイプ) 0.2
もしくは 従来品2(18分加工時) OH=60mm, 単一刃切削 Single-insert
Conventional (After 18 min of cutting)
・プラスサイズ刃径+レギュラータイプ 0.1 靭性と耐熱性に優れる超硬母材、耐熱性と耐溶着
(シャンク径<工具径) 性に優れる被膜により従来品に対して長寿命
Modular head + carbide shank 0 Excellent toughness and heat resistance of the carbide
・Tool diameters φ16, 20, 25 0 6 12 18 24 30 36 JS4160(18分加工時) substrate, together with a heat- and welding-resistant
+ shank diameters φ15, 18, 23 切削時間 (min) Cutting time (After 18 min of cutting) coating, provide longer tool life than conventional grades.
一般形 アンダーカット形 (Free neck, straight type)
(シャンク径=工具径) (シャンク径<工具径) Or
Standard type Undercut type ・Plus-size tool diameter + regular type SD5010によるA7075材の切削事例 Machining Example of A7075 with SD5010
(Shank diameter = tool diameter) (Shank diameter < tool diameter) (Shank diameter < tool diameter)
切削長=60m 切削長=10m 切削長=2m 被削材 Work material:A7075
Cutting length Cutting length Cutting length
工具径 Tool dia.:φ35mm
従来DLC 欠損 切削条件 Cutting conditions
Conventional DLC Broken
多様な加工に対応するインサートラインナップ JDET100304R-FA JDET100304R-FA Vc=500m/min, fz=0.2mm/t
SD5010 ノンコーティング(WH10) 従来DLC
Lineup of inserts to support a wide range of machining requirements Non coating Conventional DLC ap=2mm, ae=5mm, エアブロー Air-blow
ノンコーティング
Non coating 溶着大 Severe built-up edge 継続切削可能
● 加工形態に応じて選べる2つのサイズ Further cutting is SD5010は優れた潤滑性により溶着を低減、
possible
・Two sizes available to suit machining applications ノンコーティング品・従来品に比べて長寿命
JD T10:比較的切込み量の少ない加工向け JD T10:For machining with relatively shallow cutting depths Excellent lubricity of SD5010 suppresses built-up
JD T15:深切込みに対応する高剛性タイプ edge and delivers longer tool life than uncoated and
JD T15:High rigidity type suitable for deep cuts
0 10 20 30 40 50 60 70 80 conventional grades.
切削長 Cutting length (m)
● バリエーション豊富なコーナRサイズ
・Broad range of corner radii HD7010によるグラファイト材の切削事例 Machining Example of Graphite with HD7010
R0.2~R3.2から、加工形状に応じたサイズを選べます
Choice of sizes ranging from 0.2 to 3.2 mm radius to suit machining requirements 被削材 Work material:グラファイト Graphite
● 各種被削材向けに適正化されたブレーカ 工具 Tool:AHUL1525R-2
・Breakers optimized for all kinds of work materials 切削条件 Cutting conditions
鋼向けのほか、アルミやグラファイト、ステンレスや Compatible with a wide range of work Vc=196.3m/min, fz=0.28mm/t, ap=3mm, ae=3mm, 乾式 Dry
耐熱合金向けなど幅広い被削材の種類に対応します materials, including steel, aluminum, graphite,
stainless steel, and heat-resistant alloys 耐摩耗性に優れるHD7010は従来PVD品に比べて摩耗を大幅に低減
従来品 Conventiona(l PVD) HD7010 HD7010 provides superior wear resistance and significantly reduces wear
22m加工後の工具写真 compared with conventional PVD grades.
Tool condition after 22m of Cutting
03
最大逃げ面摩耗幅 VBmax (mm)
Maximum flank wear width
Page4
テクノロジー ラインナップ
Technology Line Up
難削材加工用インサート 特長と性能
Features and Performance of Inserts for Difficult-to-Machine Materials
B5/B7形ブレーカ 強スクイ低抵抗ブレーカ
B5/B7 type breaker High-rake low cutting force breaker
ステンレス鋼系材料、チタン合金、耐熱合金・超耐熱合金の加工向け
For machining stainless steel materials, titanium alloys, heat resistant alloys, and super heat resistant alloys.
C5/C7形ブレーカ 弱スクイ低抵抗ブレーカ
C5/C7 type breaker Low-rake low cutting force breaker
ステンレス鋼系材料、耐熱合金・超耐熱合金の加工向け
For machining stainless steel materials, heat resistant alloys, and super heat resistant alloys.
特長① Features 1 特長② Features 2
● 軸方向スクイ角を従来より大きくすることで低抵抗 ● 外周切れ刃を短くすること
化を実現しました。 で、突出し量が長い場合で
・Increased axial rake angle compared to conventional designs のビビり振動を抑制します。
for reduced cutting force
・Reduced peripheral flute length
従来インサート:15度 B/C形:18度 minimizes chattering vibration with
Conventional insert: 15° B/C type: 18° long overhang lengths.
10形 10 type 15形 15 type
APMX=5mm APMX=7mm
B5/C5、B7/C7 ブレーカをご使用の場合は、最大切込みAPMXに
制約があります。加工条件をあらかじめご確認の上ご使用ください。
APMX restrictions apply when using B5/C5 or B7/C7 breakers.
Check machining conditions before use.
切削抵抗の比較 Cutting force comparison
従来ブレーカ
Conventional breaker 従来ブレーカに対して切削抵抗
C5/C7ブレーカは19%
C5/C7ブレーカ
C5/C7 breaker B5/B7ブレーカは25%削減!
B5/B7 Compared with the conventional breaker,
ブレーカ
B5/B7 breaker cutting force is reduced by 19% with C5/C7 breakers
and by 25% with B5/B7 breakers!
0 100 200 300 400
切削抵抗合力 Resultant cutting force( kgf)
B5ブレーカの切削事例 Machining example using B5 breaker
0.4 機械 Machine:立形3軸M/C(BT50) Vertical 3-axis
従来品① JM4160相当 FWブレーカ
FW breaker equivalent to JM4160 被削材 Work material:SUS630(36.6HRC)
Conventional product ①
0.3 工具径 Tool dia.:φ25mm
従来品②
Conventional product ② 【切削条件 Cutting conditions】
0.2 Vc=78.5m/min
(n=1,000min-1)
0.1 JM4160相当 B5ブレーカ
B breaker equivalent to JM4160 fz=0.075mm/t
(Vf = 300 mm/min)
0 ap×ae=2.5×22mm、水溶性 Wet
0 2 4 6 8
切削時間 (min)
Cutting time
低抵抗ブレーカの快削性により、従来品に比べて長い工具寿命を実現
Free-cutting performance of low cutting force breaker for longer tool life than conventional products
04
最大逃げ面摩耗幅 VBmax (mm)
Maximum flank wear width
5mm
7mm
Page5
テクノロジー ラインナップ
Technology Line Up
難削材加工用インサート 特長と性能 シャンクタイプ Shank type AHU(L) R(S )- は数字が入ります。
Circles ( ) indicate digits.
Features and Performance of Inserts for Difficult-to-Machine Materials
B5/B7形ブレーカ 強スクイ低抵抗ブレーカ
B5/B7 type breaker High-rake low cutting force breaker APMX APMX
LH LS LH LS
ステンレス鋼系材料、チタン合金、耐熱合金・超耐熱合金の加工向け LF LF
For machining stainless steel materials, titanium alloys, heat resistant alloys, and super heat resistant alloys.
Aタイプ(一般形 Standard type) Bタイプ(アンダーカット形 Undercut type)
C5/C7形ブレーカ 弱スクイ低抵抗ブレーカ
C5/C7 type breaker Low-rake low cutting force breaker タイプ 商品コード 在庫 刃数 寸 法 Size (mm) 形状 適用インサート 備考
Type Item code Stock No.of
ステンレス鋼系材料、耐熱合金・超耐熱合金の加工向け flutes DC LF APMX LH LS DCONMS Shape Recommended insert Note
For machining stainless steel materials, heat resistant alloys, and super heat resistant alloys. AHU1016R-2 ● 2 16 100 30 70 16 A
AHU1016RS15-2 ★ 2 16 100 30 70 15 B
特長① JDMT1003 R
Features 1 特長② Features 2 AHU1018RS16-2 ★ 2 18 100 30 70 16 B JDMT1003 R-FW
● 軸方向スクイ角を従来より大きくすることで低抵抗 ● 外周切れ刃を短くすること AHU1020R-3 ● 3 20 110 9 30 80 20 A JDMT100308R-TFW
AHU1020RS18-2 ★ 2 20 110 (5) ※ 30 80 18 B JDMT1003 R-B5/C5※
化を実現しました。 で、突出し量が長い場合で
・ AHU1025R-4
Increased axial rake angle compared to conventional designs ● 4 25 120 35 85 25 A JDET1003 R-FF
のビビり振動を抑制します。 標
for reduced cutting force 準 AHU1030R-5 ● 5 30 120 45 75 32 A JDET100304R-FA
・Reduced peripheral flute length 形
minimizes chattering vibration with AHU1032R-5 ● 5 32 130 45 85 32 A
従来インサート:15度 B/C形:18度
Conventional insert: 15° B/C type: 18° long overhang lengths. AHU1525R-2 ● 2 25 125 40 85 25 A
AHU1525RS23-2 ★ 2 25 125 40 85 23 B
10形 10 type 15形 15 type AHU1530R-2 ● 2 30 130 45 85 25 B
APMX=5mm APMX=7mm AHU1532R-3 ● 3 32 140 45 95 32 A JDMT1505 R
AHU1532RS30-2 ★ 2 32 140 45 95 30 B JDMT1505 R-FW
B5/C5、B7/C7 ブレーカをご使用の場合は、最大切込みAPMXに AHU1535R-3 ● 3 35 140 14 45 95 32 B JDMT150508R-TFW
制約があります。加工条件をあらかじめご確認の上ご使用ください。 (7) ※ JDMT1505 R-B7/C7※
AHU1540R-2 ● 2 40 140 45 95 32 B
APMX restrictions apply when using B5/C5 or B7/C7 breakers. JDET1505 R-FF
Check machining conditions before use. AHU1540R-3 ● 3 40 140 45 95 32 B JDET1505 R-FA
AHU1540R-4 ● 4 40 140 45 95 32 B
切削抵抗の比較 AHU1550R-3 ● 3 50 140 45 95 32 B
Cutting force comparison AHU1550R-5 ● 5 50 140 45 95 32 B
AHUL1016R-2 ● 2 16 150 50 100 16 A
従来ブレーカ
Conventional breaker 従来ブレーカに対して切削抵抗 AHUL1016RS15-2 ★ 2 16 150 30 120 15 B
C5/C7ブレーカは19% AHUL1018RS16-2 ★ 2 18 150 30 120 16 B
C5/C7ブレーカ
C5/C7 breaker B5/B7ブレーカは25% AHUL1020R-2 ● 2 20 160 60 100 20 A
削減! AHUL1020R-3 ● 3 20 160 60 100 20 A
B5/B7 Compared with the conventional breaker,
ブレーカ
B5/B7 breaker cutting force is reduced by 19% with C5/C7 breakers AHUL1020RS18-2 ★ 2 20 160 30 130 18 B
and by 25% with B5/B7 breakers! AHUL1021R-3 ● 3 21 160 30 130 20 B JDMT1003 R
0 100 200 300 400 AHUL1025R-2 ● 2 25 180 75 105 25 A JDMT1003 R-FW
切削抵抗合力 Resultant cutting force( kgf) ロ AHUL1025R-3 ● 3 25 180 9 75 105 25 A JDMT100308R-TFW
(5) ※ JDMT1003 R-B5/C5※
ン
グ AHUL1025RS23-3 ★ 3 25 180 35 145 23 B JDET1003 R-FF
シ AHUL1026R-3 ● 3 26 180 35 145 25 B JDET100304R-FA
ャ
ン AHUL1030R-2 ● 2 30 180 45 135 25 B
B5ブレーカの切削事例 Machining example using B5 breaker ク AHUL1030R-3 ● 3 30 180 45 135 25 B
形 AHUL1032R-4 ● 4 32 200 90 110 32 A
0.4 機械 Machine:立形3軸M/C(BT50) AHUL1032RS30-4 ★ 4 32 200 45 155 30 B
Vertical 3-axis
従来品① JM4160相当 FWブレーカ AHUL1035R-2 ● 2 35 200 45 155 32 B
FW breaker equivalent to JM4160 被削材 Work material:SUS630(36.6HRC)
Conventional product ① AHUL1035R-4 ● 4 35 200 45 155 32 B
0.3 工具径 Tool dia.:φ25mm AHUL1525R-2 ● 2 25 180 75 105 25 A
従来品②
Conventional product ② 【切削条件 Cutting conditions】 AHUL1525RS23-2 ★ 2 25 180 35 145 23 B
0.2 Vc=78.5m/min AHUL1530R-2 ● 2 30 180 45 135 25 B
AHUL1532R-3 ● 3 32 200 90 110 32 A
(n=1,000min-1) JDMT1505 R
AHUL1532RS30-2
0.1 JM4160相当 B5 ★ 2 32 200 45 155 30 B
ブレーカ JDMT1505 R-FW
B breaker equivalent to JM4160 fz=0.075mm/t AHUL1535R-2 ● 2 35 200 14 45 155 32 B JDMT150508R-TFW
(Vf = 300 mm/min) AHUL1535R-3 ● 3 35 200 (7) ※ 45 155 32 B JDMT1505 R-B7/C7※
AHUL1540R-2 ● 2 40 220 45 175 32 B JDET1505 R-FF
0 ap×ae=2.5×22mm、水溶性 Wet AHUL1540R-3 ● 3 40 220 45 175 32 B JDET1505 R-FA
0 2 4 6 8
切削時間 (min) AHUL1540R-4 ● 4 40 220 45 175 32 B
Cutting time AHUL1540R-5 ● 5 40 220 45 175 32 B
AHUL1550R-4 ● 4 50 220 45 175 42 B
低抵抗ブレーカの快削性により、従来品に比べて長い工具寿命を実現 【注意】※JDMT1003 R-B5/C5、JDMT1505 R-B7/C7をご使用の場合は最大切込みAPMXは( )寸法になります。
Free-cutting performance of low cutting force breaker for longer tool life than conventional products 【Note】※ Values in parentheses indicate APMX when using JDMT1003 R-B5/C5 and JDMT1505 R-B7/C7.
★印:新商品の標準在庫品です。★:Stocked Items of New products. ●印:標準在庫品です。●:Stocked items.
05
最大逃げ面摩耗幅 VBmax (mm)
Maximum flank wear width
5mm
7mm
Long shank type Regular shank type
DC
DCONMS
DC
DCONMS
Page6
ラインナップ
Line Up
モジュラータイプ 入ります。
Modular type AHUM1 R-(-M ) は数字が
Circles ( ) indicate digits.
LF THSZMS
APMX DRVS(二面幅)
L1
L2
商品コード 在庫 刃数 寸 法 Size (mm) 適用インサート 備考
Item code Stock No.of
flutes DC LF APMX DCONMS THSZMS DHUB L1 L2 DRVS Recommended Insert Note
AHUM1016R-2 ● 2 16 25 8.5 M8 12.8 5.5 17 10
※ 1 AHUM1017R-2 ★ 2 17 25 8.5 M8 12.8 5.5 17 10
※ 1 AHUM1018R-2 ● 2 18 25 8.5 M8 14.5 5.5 17 10
※ 1 AHUM1020R-2-M8 ● 2 20 25 8.5 M8 14.5 5.5 17 10
AHUM1020R-3 ● 3 20 30 10.5 M10 17.8 5.5 19 15
※ 1 AHUM1021R-3 ★ 3 21 30 10.5 M10 17.8 5.5 19 15
※ 1 AHUM1022R-3 ● 3 22 30 10.5 M10 17.8 5.5 19 15
※ 1 AHUM1025R-2-M10 ● 2 25 30 10.5 M10 17.8 5.5 19 15 JDMT1003○○R
JDMT1003○○R-FW
AHUM1025R-4 ● 4 25 35 9 12.5 M12 20.8 5.5 22 17 JDMT100308R-TFW
※ 1 AHUM1026R-4 ★ 4 26 35 (5) ※
12.5 M12 20.8 5.5 22 17 JDMT1003○○R-B5/C5※
JDET1003○○R-FF
※ 1 AHUM1028R-4 ● 4 28 35 12.5 M12 23 5.5 22 17 JDET100304R-FA
※ 1 AHUM1030R-2-M12 ● 2 30 35 12.5 M12 23 5.5 22 17
AHUM1030R-5 ● 5 30 40 17 M16 28.8 6 23 22
AHUM1032R-5 ● 5 32 40 17 M16 28.8 6 23 22
※ 1 AHUM1033R-5 ★ 5 33 40 17 M16 28.8 6 23 22
※ 1 AHUM1035R-2 ● 2 35 40 17 M16 28.8 6 23 22
※ 1 AHUM1035R-5 ● 5 35 40 17 M16 28.8 6 23 22
※ 1 AHUM1040R-6 ● 6 40 40 17 M16 28.8 6 23 22
AHUM1525R-2 ● 2 25 35 12.5 M12 20.8 5.5 22 17
※ 1 AHUM1528R-2 ● 2 28 35 12.5 M12 23 5.5 22 17 JDMT1505○○R
JDMT1505○○R-FW
※ 1 AHUM1528R-3 ● 3 28 35 14 12.5 M12 23 5.5 22 17 JDMT150508R-TFW
※ 1 AHUM1530R-2-M12 ● 2 30 35 (7) ※
12.5 M12 23 5.5 22 17 JDMT1505○○R-B7/C7※
JDET1505○○R-FF
AHUM1530R-3 ● 3 30 40 17 M16 28.8 6 23 22 JDET1505○○R-FA
AHUM1532R-3 ● 3 32 40 17 M16 28.8 6 23 22
【注意】①※JDMT1003 R-B5/C5、JDMT1505 R-B7/C7をご使用の場合は最大切込みAPMXは( )寸法になります。
②AHUM R- -M のモジュラーミルによる溝加工は工具破損の恐れがあります。P14記載のモジュラーミル切削領域線図を参考に加工条件を
調整してください。
③モジュラーミル及び専用シャンク、専用アーバの「工具端面」「モジュラーねじ部」にグリースなどの潤滑剤は塗布しないでください。
④※1と超硬シャンクをセットで使用すると干渉がありません。
⑤AHUM R- -M のモジュラーミルと超硬シャンクの組合せで使用すると干渉がありません。
【Note】①※Values in parentheses indicate APMX when using JDMT1003 R-B5/C5 and JDMT1505 R-B7/C7.
②Slotting using AHUM R- -M modular mills may result in tool damage. Adjust cutting conditions while referring to the modular mill
cutting range diagram on page 14.
③Do not apply grease or other lubricants to the tool end face or modular screw threads of modular mills, dedicated shanks, or dedicated arbors.
④No interference when carbide shank is used with ※1 as a set
⑤No interference when AHUM R- -M modular mills are used in conjunction with modular mills
★印:新商品の標準在庫品です。★:Stocked Items of New products. ●印:標準在庫品です。●:Stocked items.
06
DC
DCONMS
DHUB
Page7
ボアタイプ Bore type AHUB15 R(M)- は数字が入ります。
Circles ( ) indicate digits.
DHUB DHUB
DCONMS DCONMS
KWW KWW
DCCB DCCB
DC DC
Cタイプ C type Dタイプ D type
DHUB
DCONMS
KWW
DHUB
DCONMS
KWW
DCCB DCCB
DC DC
Eタイプ E type Fタイプ F type
商品コード 在庫 刃数 寸 法 Size (mm) 形状 適用インサート 備考
Item code Stock No.of
flutes DC APMX LF DCONMS DCCB DHUB CBDP KWW b Shape Recommended insert Note
AHUB1550R-3 ● 3 50 50 22.225 17 47 20 8.4 5 E
AHUB1550R-5 ● 5 50 50 22.225 17 47 20 8.4 5 C
AHUB1550RM-3 ● 3 50 50 22 17 47 20 10.4 6.3 E
AHUB1550RM-5 ● 5 50 50 22 17 47 20 10.4 6.3 C JDMT1505 ○○ R
AHUB1563R-3 ● 3 63 50 22.225 17 45 20 8.4 5 E JDMT1505 ○○ R-FW
AHUB1563R-6 ● 6 63 14 50 22.225 17 45 20 8.4 5 C JDMT150508R-TFW
AHUB1563RM-3 ● 3 63 (7) ※ 50 22 17 45 20 10.4 6.3 E JDMT1505 ○○ R-B7/C7 ※
AHUB1563RM-6 ● 6 63 50 22 17 45 20 10.4 6.3 C JDET1505 ○○ R-FF
AHUB1580R-4 ● 4 80 50 25.4 20 50 26 9.5 6 E JDET1505 ○○ R-FA
AHUB1580R-7 ● 7 80 50 25.4 20 50 26 9.5 6 C
AHUB15100R-8 ● 8 100 50 31.75 45 60 32 12.7 8 D
AHUB15125R-10 ★ 10 125 63 38.1 60 100 36 15.9 10 F
【注意】 Dタイプ、Fタイプを当社ボアタイプ用アーバに取付けるには、市販のフェースミル用締め付けボルトが必要となります。
※JDMT1505 R-B7/C7をご使用の場合は最大切込みAPMXは( )寸法となります。
【Note】A commercially available face mill clamping bolt is required to mount D type or F type tools into a Moldino bore type arbor.
※Values in parentheses indicate APMX when using JDMT1505 R-B7/C7.
部品番号 Parts
部品名 クランプねじ アーバ用ねじ ドライバー レンチ ねじ焼き付き防止剤
Parts Clamp screw Arbor screw Screw driver Wrench Screw anti-seizure agent
a a
形状
Shape
d d
f c f c
Fig.1 Fig.2
締付トルク
適用カッタ (N・m) 型番 a φb c d f 形状
Fastening Model No. Shape
Cutter body torque
AHU(L)1016R-2 250-141 1.1 - - - - - - -
AHU(L)1020R- ~ 1035R- 251-141 1.1 - - - - - - - 104-T8 -
AHU(L)15 R- - - - - - - - 104-T15 -
AHUB1550R(M)-3~ 1563R(M)-3 100-178 M10×1.5 16 35 25 8 Fig.1
AHUB1550R(M)-5~ 1563R(M)-6 100-175 M10×1.5 16 35 25 8 Fig.2
AHUB1580R-4 412-141 2.9 100-179 M12×1.75 18 42 30 10 Fig.1 - 105-T15 P-37
AHUB1580R-7 100-212 M12×1.75 18 42 30 10 Fig.2
AHUB15100R-8 - - - - - - -
AHUB15125R-10 - - - - - - -
AHUM10 R- (-M ) 250-141 1.1 - - - - - - - 104-T8 -
AHUM15 R- (-M ) 412-141 2.9 - - - - - - - 104-T15 -
【注意】 クランプねじは消耗品です。使用環境により交換寿命は変化しますので早めの交換をお願い致します。
【Note】 The clamp screw is a consumable item. Replacement intervals will depend on the operating environment. Replace promptly if necessary.
07
CBDP CBDP
b b
φb
APMX APMX
LF LF
φb
CBDP
b
CBDP
b
APMX
LF
APMX
LF
Page8
ラインナップ
Line Up
インサート Insert
INSL INSL
15°
【注意】コーナR2.0以上のインサートを使用する場合
RE RE はボデーコーナ部を追加工する必要があります。
【Note】 Additional body corner machining is
required when using inserts with a corner
Fig.1 Fig.2 radius of 2.0 mm or greater.
炭素鋼・合金鋼(30HRC以下)
Carbon steels, Alloy steels(30HRC or less)
合金鋼(焼入れ焼戻し材)
(35HRC以下)
P Alloy steels(Quenched and tempered steels)
(35HRC or less)
プリハードン鋼・合金鋼
(焼入れ焼戻し材)(45HRC以下)
Pre-hardened steels,Alloy steels :一般切削・第一推奨
(Quenched and tempered steels)(45HRC or less) General cutting, First recommendation
M ステンレス鋼 Stainless steels Wet Dry :一般切削・第二推奨
K 鋳鉄 Cast irons General cutting, Second recommendation
N アルミニウム合金・銅合金
Aluminum alloys, Copper alloys
グラファイト Graphite・CFRP
耐熱合金・超耐熱合金
S Heat resistant alloys, Super heat resistant alloys
チタン合金 Titanium alloys
寸 法 Size (mm)
商品コード 精度 形状 備考
Item code Tolerance
class Shape Note
INSL W1 S RE
汎JDMT100302R-FW ★ ★ ★ 0.2
用JDMT100304R-FW ● ★ ★ △ △ ● 0.4
/JDMT100308R-FW ● ● ★ △ △ ● 0.8
強
断JDMT100308R-TFW ★ ★ 0.8
JDMT100310R-FW ★ ★ ★ 1 Fig.1
続
切JDMT100316R-FW ★ ★ ★ 1.6
削JDMT100320R-FW ★ ★ ★ 2
用JDMT100330R-FW M 級 ★ ★ ★ 3
スJDMT100308R-B5 M ● ● 11 6.1 3.5 0.8
テ
ンJDMT100308R-C5 ● ● 0.8
レ
スJDMT100320R-B5 ● ● 2
鋼JDMT100320R-C5 ● ● 2
/JDMT100330R-B5 ● ● 3 Fig.2
超
耐
熱JDMT100330R-C5 ● ● 3
合
金JDMT100332R-B5 ● ● 3.2
用JDMT100332R-C5 ● ● 3.2
グア
ラル JDET100304R-FF △ ● ● 0.4
フミ
ァニウ JDET100308R-FF E 級
イ
トム E △ ● ● 11 6.1 3.5 0.8 Fig.1
用合金 JDET100304R-FA ● ● 0.4
JDMT100304R ● △ △ ● ● 0.4
JDMT100308R M 級 ● △ △ ● ● ●
M 11 6.1 3.5 0.8
JDMT100320R ● △ △ ● 2 Fig.1
JDMT100332R ● ● △ △ ● 3.2
※1 JDMT R-B ;JP4120の第一推奨被削材種はS:チタン合金、第二推奨被削材種はM:ステンレス合金(中仕上げ)となります。
※2 JDMT R-C ;JP4120の第一推奨被削材種はS:耐熱合金・超耐熱合金、第二推奨被削材種はP:鋼となります。
※3 推奨被削材種は目安を示すものです。実際の加工状況により適正な推奨材種が異なる場合があります。
【注意】GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。
刃先強度 Cutting edge strength
JDMT100308R-TFW JDMT1003 R(-FW) JDET1003 R-FF JDMT1003 R-C5
JDMT150508R-TFW JDMT1505 R(-FW) JDET1505 R-FF JDMT1505 R-C7
ステンレスのドライ加工や
黒皮や強断続切削向けの 超耐熱合金に適した
高剛性な刃形です 汎用的な使用に適した刃形です ポジランド(弱スクイ)刃形です
High rigidity cutting edge for scale Cutting edge suitable for general purpose use Positive land (low rake angle) cutting edge suitable
and heavy interrupted cutting for dry machining of stainless steel and superalloys
★印:新商品の標準在庫品です。 ●印:標準在庫品です。 △印:在庫がなくなり次第販売を終了します。 無印:弊社営業にお問合せ下さい。
08 ★:Stocked Items of New products. ●:Stocked Items. △:The sale ends when all the stock is out. No mark:Contact with our sales office.
For aluminum alloys /
graphite For stainless steel / General purpose /
super heat-resistant alloys heavy interrupted cutting
S W1
JP4120 AJコーティング
JM4160 AJ Coating
GX2160 GXコーティング
GX Coating
JS4160
JS4045 JSコーティング
JS Coating
JS4060 W1
PTH30E S
PTH40H THコーティング
TH Coating
PTH13S
SD5010 DLCコーティング
DLC Coating
HD7010 HDコーティング
HD Coating 15°
WH10 超硬 Carbide
Page9
インサート Insert
INSL INSL
15°
【注意】コーナR2.0以上のインサートを使用する場合
RE RE はボデーコーナ部を追加工する必要があります。
【Note】 Additional body corner machining is
required when using inserts with a corner
Fig.1 Fig.2 radius of 2.0 mm or greater.
炭素鋼・合金鋼(30HRC以下)
Carbon steels, Alloy steels(30HRC or less)
合金鋼(焼入れ焼戻し材)
(35HRC以下)
P Alloy steels(Quenched and tempered steels)
(35HRC or less)
プリハードン鋼・合金鋼
(焼入れ焼戻し材)(45HRC以下)
Pre-hardened steels,Alloy steels :一般切削・第一推奨
(Quenched and tempered steels)(45HRC or less) General cutting, First recommendation
M ステンレス鋼 Stainless steels Wet Dry :一般切削・第二推奨
K 鋳鉄 Cast irons General cutting, Second recommendation
N アルミニウム合金・銅合金
Aluminum alloys, Copper alloys
グラファイト Graphite・CFRP
耐熱合金・超耐熱合金
S Heat resistant alloys, Super heat resistant alloys
チタン合金 Titanium alloys
寸 法 Size (mm)
商品コード 精度 形状 備考
Item code Tolerance
class Shape Note
INSL W1 S RE
汎JDMT150502R-FW ★ ★ ★ 0.2
用JDMT150504R-FW ● ★ ★ △ △ ● 0.4
/JDMT150508R-FW ● ● ★ △ △ ● 0.8
強
断JDMT150508R-TFW ● ● ★ △ △ ● 0.8
JDMT150510R-FW ★ ★ ★ 1 Fig.1
続
切JDMT150516R-FW ★ ★ ★ 1.6
削JDMT150520R-FW M 級 ★ ★ ★ 2
用JDMT150530R-FW M ★ ★ ★ 16 9.12 5 3
JDMT150508R-B7 ● ● 0.8
超ス JDMT150508R-C7 ● ● 0.8
耐テ
熱ンレ JDMT150520R-B7 ● ● 2
合 JDMT150520R-C7 ● ● 2 Fig.2
金ス
用鋼/ JDMT150530R-B7 ● ● 3
JDMT150530R-C7 ● ● 3
グア JDET150504R-FF △ ● ● 0.4
ラル
フミ JDET150508R-FF △ ● ● 0.8
ァニウ JDET150502R-FA E 級 ● ● 0.2
イ E 16 9.12 5 Fig.1
トム合 JDET150504R-FA ● ● 0.4
用金 JDET150530R-FA ● ● 3
JDMT150504R ● △ ● ● 0.4
JDMT150508R M 級 ● △ △ ● ● ● 0.8
JDMT150520R M ● △ △ ● 16 9.12 5 2 Fig.1
JDMT150530R ● △ △ ● ● 3
※1 JDMT R-B : The primary recommended work material grade for JP4120 is S: titanium alloy. The secondary recommended work material grade is M: stainless steel alloy (semi-finishing).
※2 JDMT R-C : The primary recommended work material grade for JP4120 is S: heat resistant alloys, super heat resistant alloys The secondary recommended work material grade is P: steel.
※3 The recommended work material grades are a guideline. The appropriate grade may differ depending on actual machining conditions.
【Note】Note that GX and JS coatings do not respond to conductive touch sensors.
快削 Easy cutting
JDMT1003 R-C5 JDMT1003 R-B5 JDET100304R-FA
JDMT1505 R-C7 JDMT1505 R-B7 JDET1505 R-FA
ステンレスのWet 加工や超耐熱合金に アルミニウム合金の加工に適した
適したポジランド( 強スクイ)刃形です シャープエッジ刃形です
Positive land (low rake angle) cutting edge suitable Positive land (high rake angle) cutting edge suitable for wet machining of Sharp cutting edge suitable for
for dry machining of stainless steel and superalloys stainless steel and superalloys machining aluminum alloys
09
For aluminum alloys / For stainless steel /
graphite super heat-resistant alloys General purpose /
heavy interrupted cutting
S W1
JP4120 AJコーティング
JM4160 AJ Coating
GX2160 GXコーティング
GX Coating
JS4160
JS4045 JSコーティング
JS Coating
JS4060 W1
PTH30E S
PTH40H THコーティング
TH Coating
PTH13S
SD5010 DLCコーティング
DLC Coating
HD7010 HDコーティング
HD Coating 15°
WH10 超硬 Carbide
Page10
ラインナップ
Line Up
モジュラーミル専用シャンク The Shanks for Modular Mill
■ フリーネック超硬シャンク Free-neck carbide shank - 干渉を気にせず突き出し量が調整できる
Adjustable overhang length eliminates interference concerns.
LF
LB1 LS
THSZWS
テーパタイプ Tapered type
寸 法 Size (mm)
商品コード 在庫 適用カッタ エアー穴有無 備考
Item code Stock DCONWS THSZWS LF LB1 LS BD1 DCONMS 対象壁角度 Cutter body With/without
air hole Note
Supported wall angle
ASC20T-8.5-250-120Z-09 ● φ8.5 M8 250 120 130 14.5 φ20 0.9°以上
or more φ16
ASC20T-8.5-250-75Z-14 ● φ8.5 M8 250 75 175 14.5 φ20 1.4°以上
or more φ17 〇
φ18
ASC25T-8.5-250-80Z-29 ● φ8.5 M8 250 80 170 14.5 φ25 2.9°以上
or more
ASC25T-10.5-300-150Z-09 ● φ10.5 M10 300 150 150 18.5 φ25 0.9°以上
or more φ20
ASC25T-10.5-300-95Z-14 ● φ10.5 M10 300 95 205 18.5 φ25 1.4°以上
or more φ21 〇
φ2
ASC32T-10.5-300-105Z-29 ● φ10.5 M10 300 105 195 18.5 φ32 2.9°以上 2
or more
LF
THSZWS
ストレートタイプ Straight type
商品コード 在庫 寸 法 Size (mm) 適用カッタ エアー穴有無 備考
Item code Stock DCONWS THSZWS LF DCONMS Cutter body With/without
air hole Note
ASC15-8.5-210-0Z ● φ8.5 M8 210 φ15 φ16、φ17、φ18
ASC16-8.5-130-0Z ● φ8.5 M8 130
φ16 φ16※ 〇
、φ17、φ18
ASC16-8.5-210-0Z ● φ8.5 M8 210
ASC18-10.5-240-0Z ● φ10.5 M10 240 φ18 φ20、φ21、φ22
ASC20-10.5-150-0Z ● φ10.5 M10 150 〇
φ20 φ20※、φ21、φ22
ASC20-10.5-250-0Z ● φ10.5 M10 250
ASC23-12.5-300-0Z ● φ12.5 M12 300 φ23 φ25、φ26、φ28
ASC25-12.5-175-0Z ● φ12.5 M12 175 〇
φ25 φ25※、φ26、φ28
ASC25-12.5-300-0Z ● φ12.5 M12 300
【注意】 ①市販のミーリングチャック、焼ばめホルダーにて使用できます。
②<φ40><φ42>寸法は、突き出し長さ 200以下を目安にご使用ください。
③専用アーバ(HSK-A63)、鋼シャンクタイプも標準在庫しています。
④※ではカッタ径がシャンク径より小さいため、シャンク首部の干渉が生じます。
【Note】①Compatible with commercially available milling chucks and shrink-fit holders.
②Use the φ40 and φ42 dimensions with overhang lengths not exceeding 200 mm.
③Dedicated arbor (HSK-A63) and steel shank types are available as standard items.
④The cutter diameter for items marked “※” is smaller than the shank diameter, which will cause interference at the shank.
●印:標準在庫品です。 ●:Stocked Items.
10
DCONWS
DCONWS
BD1
DCONMS
DCONMS
Page11
モジュラーミル専用シャンク The Shanks for Modular Mill
■ 超硬シャンク レギュラータイプ Carbide Shank Regular Type
Cタイプ C Type Eタイプ E Type
LF LF
LB1 LS LB1 LS
THSZWS THSZWS
商品コード 在庫 寸 法 Size(mm) タイプ 適用カッタ 備考
Item code Stock DCONWS THSZWS LF LB1 LS BD1 DCONMS D1 Type Cutter body Note
ASC16-8.5-95-30Z ● 95 30 65
ASC16-8.5-120-55Z ● 120 55 65 φ16※3
ASC16-8.5-140-75Z ● 8.5 M8 140 75 65 14.5 16 15.5 C φ18
ASC16-8.5-160-95Z ● 160 95 65 AHUM
1020R-2-M8
※2 ASC16-8.5-160-30Z ● 160 30 130
ASC20-10.5-120-50Z ● 120 50 70
ASC20-10.5-170-90Z ● 170 90 80
ASC20-10.5-220-120Z ● 10.5 M10 220 120 100 18.5 20 19.5 C φ20※3
φ22
ASC20-10.5-270-150Z ● 270 150 120 AHUM
※2 ASC20-10.5-220-50Z ● 220 170 1025R-2-M10
※2 ASC20-10.5-270-50Z ● 10.5 M10 270 50 220 18.5 20 19.5 C
ASC25-12.5-145-65 ● 145 65 80 エアー
ASC25-12.5-215-115 ● 215 115 100 φ25※3 穴付
ASC25-12.5-265-145 ● 12.5 M12 φ28 With
265 145 120 23 25 - E Air hole
● AHUM
ASC25-12.5-315-195 315 195 120 1030R-2-M12
※2 ASC25-12.5-265-65 ● 265 200 AHUM
- 1530R-2-M12
※2 ASC25-12.5-315-65 ● 12.5 M12 315 65 250 23 25 E
ASC32-17-160-80 ● 160 80 80
ASC32-17-210-110 ● 210 110 100
ASC32-17-260-140 ● 17 M16 260 140 120 28 32 - E φ30※3
ASC32-17-310-190 ● 310 190 120 φ32※3
ASC32-17-360-240 ● 360 240 120 φ35
ASC32-17-260-80 ● 260 〈φ40〉
※2 180
※2 ASC32-17-310-80 ● 17 M16 310 80 230 28 32 - E
※2 ASC32-17-360-80 ● 360 280
【注意】 ①※2と※1(P6)をセットで使用すると干渉がありません。
②市販のミ-リングチャック、焼ばめホルダーにて使用できます。
③〈φ40〉寸法は、突き出し長さ 200mm以下を目安にご使用下さい。
④※3ではカッタ径がシャンク径より小さいため、シャンク首部の干渉が生じます。
【Note】①No interference will occur when ※2 and ※1 (page 6) are used together as a set.
②Compatible with commercially available milling chucks and shrink-fit holders.
③Use the φ40 dimension with overhang lengths not exceeding 200 mm.
④The cutter diameter for items marked “※3” is smaller than the shank diameter, which will cause interference at the shank.
11
DCONWS
BD1
D1
DCONMS
DCONWS
BD1
DCONMS
Page12
標準切削条件表
Recommended Cut t ing Condi t ions
※赤字は第1推奨材種です。 ※ Text in red indicates the primary recommended grade.
工具径 DC Tool dia. 工具径 DC Tool dia.
被削材 推奨材種 切削条件 AHU/AHUM 10形 AHU/AHUM/AHUB 15形 被削材
Work material Recommended
grade Cutting conditions Work material
φ16(2枚刃) φ20(3枚刃) φ25(4枚刃) φ32(5枚刃) φ35(5枚刃) φ40(6枚刃) φ25(2枚刃)φ32(3枚刃)φ35(3枚刃)φ40(4枚刃) φ50(5枚刃) φ63(6枚刃) φ80(7枚刃) φ100(8枚刃) φ12(5 10枚刃)
( 2 Flutes) ( 3 Flutes) ( 4 Flutes) (5 Flutes) (5 Flutes) (6 Flutes) ( 2 Flutes) ( 3 Flutes) ( 3 Flutes) (4 Flutes) (5 Flutes) (6 Flutes) (7 Flutes) (8 Flutes) (10 Flutes)
n (min-1) 3,180 2,390 1,910 1,490 1,360 1,190 1,910 1,490 1,360 1,190 950 760 600 480 380
炭素鋼 Vc(m/min) 160 150 150 150 150 150 150 150 150 150 150 150 150 150 150 炭素鋼
合金鋼 V f (mm/min) 570 1,080 1,150 1,120 1,020 1,070 760 890 820 950 950 910 840 770 760 合金鋼
(30HRC以下) JS4160 (30HRC以下)
Carbon steels fz(mm/t) 0.09 0.15 0.15 0.15 0.15 0.15 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Carbon steels
Alloy steels ap(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5 Alloy steels
(30HRC or less) (30HRC or less)
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 2,980 2,230 1,780 1,390 1,270 1,110 1,780 1,390 1,270 1,110 890 710 560 450 360
合金鋼 Vc(m/min) 150 140 140 140 140 140 140 140 140 140 140 140 140 140 140 合金鋼
(焼入れ焼戻し材)
(35HRC以下) Vf(mm/min) 420 940 1,000 970 890 930 710 830 760 890 890 850 780 720 720 (焼入れ焼戻し材)
JS4160 (35HRC以下)
Alloy steels fz(mm/t) 0.07 0.14 0.14 0.14 0.14 0.14 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Alloy steels
(Quenched and tempered steels)
(35HRC or less) a (Quenched and tempered steels)
p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5 (35HRC or less)
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 1,990 1,590 1,270 990 910 800 1,270 990 910 800 640 510 400 320 250
プリハードン鋼・合金鋼
(焼入れ焼戻し材) Vc(m/min) 100 100 100 100 100 100 100 100 100 100 100 100 100 100 100 プリハードン鋼・合金鋼
(焼入れ焼戻し材)
(45HRC以下) V f (mm/min)
JP4120 280 670 710 690 640 670 380 450 410 480 480 460 420 380 380 (45HRC以下)
Pre-hardened steels
Alloy steels fz(mm/t) 0.07 0.14 0.14 0.14 0.14 0.14 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 Pre-hardened steels
Alloy steels
(Quenched and tempered steels) ap(mm)
(45HRC or less) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5 (Quenched and tempered steels)
(45HRC or less)
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 4,970 3,980 3,180 2,490 2,270 1,990 3,180 2,490 2,270 1,990 1,590 1,260 990 800 640
Vc(m/min) 250 250 250 250 250 250 250 250 250 250 250 250 250 250 250
ステンレス鋼
(Dry加工) GX2160 Vf(mm/min) 1,190 2,030 2,160 2,120 1,930 2,030 1,270 1,490 1,360 1,590 1,590 1,510 1,390 1,280 1,280 ステンレス鋼
(Dry加工)
Stainless steels JM4160 fz(mm/t) 0.12 0.17 0.17 0.17 0.17 0.17 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Stainless steels
(Dry cutting) a (Dry cutting)
p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 1,990 1,590 1,270 990 910 800 1,270 990 910 800 640 510 400 320 250
Vc(m/min) 100 100 100 100 100 100 100 100 100 100 100 100 100 100 100
ステンレス鋼
(Wet加工) JM4160 V f (mm/min) 480 810 860 840 770 820 510 590 550 640 640 610 560 510 500 ステンレス鋼
(Wet加工)
Stainless steels PTH30E fz(mm/t) 0.12 0.17 0.17 0.17 0.17 0.17 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Stainless steels
(Wet cutting) a (Wet cutting)
p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 2,980 2,230 1,780 1,390 1,270 1,110 1,780 1,390 1,270 1,110 890 710 560 450 360
Vc(m/min) 150 140 140 140 140 140 140 140 140 140 140 140 140 140 140
鋳鉄 V f (mm/min)
JP4120 540 1,000 1,070 1,040 950 1,000 710 830 760 890 890 850 780 720 720 鋳鉄
Cast irons fz(mm/t) 0.09 0.15 0.15 0.15 0.15 0.15 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Cast irons
ap(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 6,960 6,370 5,090 3,980 3,640 3,180 5,090 3,980 3,640 3,180 2,550 2,020 1,590 1,270 1,020
Vc(m/min) 350 400 400 400 400 400 400 400 400 400 400 400 400 400 400
アルミニウム合金
銅合金 V f (mm/min) 1,670 2,870 3,050 2,990 2,730 2,860 1,730 2,030 1,860 2,160 2,170 2,060 1,890 1,730 1,730 アルミニウム合金
SD5010 銅合金
Aluminum alloys fz(mm/t) 0.12 0.15 0.15 0.15 0.15 0.15 0.17 0.17 0.17 0.17 0.17 0.17 0.17 0.17 0.17 Aluminum alloys
Copper alloys a Copper alloys
p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 4,970 3,980 3,180 2,490 2,270 1,990 3,180 2,490 2,270 1,990 1,590 1,260 990 800 640
Vc(m/min) 250 250 250 250 250 250 250 250 250 250 250 250 250 250 250
グラファイト V f (mm/min) 1,490 1,790 1,910 1,870 1,700 1,790 1,080 1,270 1,160 1,350 1,350 1,290 1,180 1,090 1,090 グラファイト
Graphite HD7010 Graphite
CFRP fz(mm/t) 0.15 0.15 0.15 0.15 0.15 0.15 0.17 0.17 0.17 0.17 0.17 0.17 0.17 0.17 0.17 CFRP
ap(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 800 640 510 400 360 320 510 400 360 320 250 200 160 130 100
Vc(m/min) 40 40 40 40 40 40 40 40 40 40 40 40 40 40 40
耐熱合金
超耐熱合金 V f (mm/min) 140 290 310 300 270 290 150 180 160 190 190 180 170 160 150 耐熱合金
JM4160 超耐熱合金
Heat resistant alloys fz(mm/t) 0.09 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 Heat resistant alloys
Super heat resistant alloys a Super heat resistant alloys
p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 900 720 570 450 410 360 570 450 410 360 290 230 180 140 110
Vc(m/min) 45 45 45 45 45 45 45 45 45 45 45 45 45 45 45
チタン合金 V f (mm/min)
JP4120 160 320 340 340 310 320 170 200 180 220 220 210 190 170 170 チタン合金
Titanium alloys fz(mm/t) 0.09 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 Titanium alloys
ap(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
【注意】GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。
【Note】Note that GX and JS coatings do not respond to conductive touch sensors.
12
Page13
工具径 DC Tool dia. 工具径 DC Tool dia.
被削材 推奨材種 切削条件 AHU/AHUM 10形 AHU/AHUM/AHUB 15形 被削材
Work material Recommended
grade Cutting conditions Work material
φ16(2枚刃) φ20(3枚刃) φ25(4枚刃) φ32(5枚刃) φ35(5枚刃) φ40(6枚刃) φ25(2枚刃)φ32(3枚刃)φ35(3枚刃)φ40(4枚刃) φ50(5枚刃) φ63(6枚刃) φ80(7枚刃) φ100(8枚刃) φ12(5 10枚刃)
( 2 Flutes) ( 3 Flutes) ( 4 Flutes) (5 Flutes) (5 Flutes) (6 Flutes) ( 2 Flutes) ( 3 Flutes) ( 3 Flutes) (4 Flutes) (5 Flutes) (6 Flutes) (7 Flutes) (8 Flutes) (10 Flutes)
n (min-1) 3,180 2,390 1,910 1,490 1,360 1,190 1,910 1,490 1,360 1,190 950 760 600 480 380
炭素鋼 Vc(m/min) 160 150 150 150 150 150 150 150 150 150 150 150 150 150 150 炭素鋼
合金鋼 V f (mm/min) 570 1,080 1,150 1,120 1,020 1,070 760 890 820 950 950 910 840 770 760 合金鋼
(30HRC以下) JS4160 (30HRC以下)
Carbon steels fz(mm/t) 0.09 0.15 0.15 0.15 0.15 0.15 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Carbon steels
Alloy steels ap(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5 Alloy steels
(30HRC or less) (30HRC or less)
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 2,980 2,230 1,780 1,390 1,270 1,110 1,780 1,390 1,270 1,110 890 710 560 450 360
合金鋼 Vc(m/min) 150 140 140 140 140 140 140 140 140 140 140 140 140 140 140 合金鋼
(焼入れ焼戻し材) Vf(mm/min) 420 940 1,000 970 890 930 710 830 760 890 890 850 780 720 720 (焼入れ焼戻し材)
(35HRC以下) JS4160 (35HRC以下)
Alloy steels fz(mm/t) 0.07 0.14 0.14 0.14 0.14 0.14 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Alloy steels
(Quenched and tempered steels) a (Quenched and tempered steels)
(35HRC or less) p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5 (35HRC or less)
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 1,990 1,590 1,270 990 910 800 1,270 990 910 800 640 510 400 320 250
プリハードン鋼・合金鋼
(焼入れ焼戻し材) Vc(m/min) 100 100 100 100 100 100 100 100 100 100 100 100 100 100 100 プリハードン鋼・合金鋼
(焼入れ焼戻し材)
(45HRC以下) V f (mm/min)
JP4120 280 670 710 690 640 670 380 450 410 480 480 460 420 380 380 (45HRC以下)
Pre-hardened steels
Alloy steels fz(mm/t) 0.07 0.14 0.14 0.14 0.14 0.14 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 Pre-hardened steels
Alloy steels
(Quenched and tempered steels) ap(mm)
( 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5 (Quenched and tempered steels)
45HRC or less) (45HRC or less)
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 4,970 3,980 3,180 2,490 2,270 1,990 3,180 2,490 2,270 1,990 1,590 1,260 990 800 640
Vc(m/min) 250 250 250 250 250 250 250 250 250 250 250 250 250 250 250
ステンレス鋼
(Dry加工) GX2160 Vf(mm/min) 1,190 2,030 2,160 2,120 1,930 2,030 1,270 1,490 1,360 1,590 1,590 1,510 1,390 1,280 1,280 ステンレス鋼
(Dry加工)
Stainless steels JM4160 fz(mm/t) 0.12 0.17 0.17 0.17 0.17 0.17 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Stainless steels
(Dry cutting) a (Dry cutting)
p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 1,990 1,590 1,270 990 910 800 1,270 990 910 800 640 510 400 320 250
Vc(m/min) 100 100 100 100 100 100 100 100 100 100 100 100 100 100 100
ステンレス鋼
(Wet加工) JM4160 V f (mm/min) 480 810 860 840 770 820 510 590 550 640 640 610 560 510 500 ステンレス鋼
(Wet加工)
Stainless steels PTH30E fz(mm/t) 0.12 0.17 0.17 0.17 0.17 0.17 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Stainless steels
(Wet cutting) a (Wet cutting)
p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 2,980 2,230 1,780 1,390 1,270 1,110 1,780 1,390 1,270 1,110 890 710 560 450 360
Vc(m/min) 150 140 140 140 140 140 140 140 140 140 140 140 140 140 140
鋳鉄 V f (mm/min)
JP4120 540 1,000 1,070 1,040 950 1,000 710 830 760 890 890 850 780 720 720 鋳鉄
Cast irons fz(mm/t) 0.09 0.15 0.15 0.15 0.15 0.15 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 Cast irons
ap(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 6,960 6,370 5,090 3,980 3,640 3,180 5,090 3,980 3,640 3,180 2,550 2,020 1,590 1,270 1,020
Vc(m/min) 350 400 400 400 400 400 400 400 400 400 400 400 400 400 400
アルミニウム合金 V f (mm/min) 1,670 2,870 3,050 2,990 2,730 2,860 1,730 2,030 1,860 2,160 2,170 2,060 1,890 1,730 1,730 アルミニウム合金
銅合金 SD5010 銅合金
Aluminum alloys fz(mm/t) 0.12 0.15 0.15 0.15 0.15 0.15 0.17 0.17 0.17 0.17 0.17 0.17 0.17 0.17 0.17 Aluminum alloys
Copper alloys a Copper alloys
p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 4,970 3,980 3,180 2,490 2,270 1,990 3,180 2,490 2,270 1,990 1,590 1,260 990 800 640
Vc(m/min) 250 250 250 250 250 250 250 250 250 250 250 250 250 250 250
グラファイト V f (mm/min) 1,490 1,790 1,910 1,870 1,700 1,790 1,080 1,270 1,160 1,350 1,350 1,290 1,180 1,090 1,090 グラファイト
Graphite HD7010 Graphite
CFRP fz(mm/t) 0.15 0.15 0.15 0.15 0.15 0.15 0.17 0.17 0.17 0.17 0.17 0.17 0.17 0.17 0.17 CFRP
ap(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 800 640 510 400 360 320 510 400 360 320 250 200 160 130 100
Vc(m/min) 40 40 40 40 40 40 40 40 40 40 40 40 40 40 40
耐熱合金 V f (mm/min) 140 290 310 300 270 290 150 180 160 190 190 180 170 160 150 耐熱合金
超耐熱合金 JM4160 超耐熱合金
Heat resistant alloys fz(mm/t) 0.09 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 Heat resistant alloys
Super heat resistant alloys a Super heat resistant alloys
p(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
n (min-1) 900 720 570 450 410 360 570 450 410 360 290 230 180 140 110
Vc(m/min) 45 45 45 45 45 45 45 45 45 45 45 45 45 45 45
チタン合金 V f (mm/min)
JP4120 160 320 340 340 310 320 170 200 180 220 220 210 190 170 170 チタン合金
Titanium alloys fz(mm/t) 0.09 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 0.15 Titanium alloys
ap(mm) 3 3 3 3 3 3 5 5 5 5 5 5 5 5 5
ae(mm) 8 10 12 16 17 20 12 16 17 20 25 31 40 50 62
13
Page14
切削領域・切削条件
Cutting Range / Cutting Conditions
突き出し量と切削領域 ・切削速度:vc=120m/min ・被削材:S50C(220HB) ・使用機械:BT50 M/C
Overhang and cutting range Cutting Speed Work material Machine
AHU(L) 10形 type AHU(L) 15形 type
突き出し量:2DC
9 3DC 突き出し量:3DC
Overhang 14 Overhang
8 AHU1016R-2 12 AHU1525R-2
7 4DC
6 突き出し量:3DC、4DC 10 突き出し量:4DC
φ16 Overhang
5 φ Overhang
2DC AHUL1016R-2 25 8 AHUL1525R-2
f 4
z=0.1 3DC fz=0.15 6
3
(mm/t) DC:工具径 4
2 Tool Dia. (mm/t) DC:工具径
Tool Dia.
4DC
1 2
0 4 8 12 16 0 5 10 15 20 25
切込み幅 ae Cutting Width(mm) 切込み幅 ae Cutting Width(mm)
2DC
9 突き出し量:2DC、3DC 1.4DC 突き出し量:1.4DC
Overhang 14 Overhang
8
4DC 3DC AHU1020R-3 12 AHU1532R-3
7
6 突き出し量:4DC、5DC 3DC
10 突き出し量:3DC、4DC
φ20 5 5DC Overhang φ32 Overhang
8
AHUL1020R-3 4DC AHUL1532R-3
f 4
z=0.15 fz=0.15 6
3
(mm/t) DC:工具径 (mm/t) 4 DC:工具径
2 Tool Dia. Tool Dia.
1 2
0 5 10 15 20 0 8 16 24 32
切込み幅 ae Cutting Width(mm) 切込み幅 ae Cutting Width(mm)
3DC
9 突き出し量:3DC 1.5DC 突き出し量:1.5DC、2DC
Overhang 14 Overhang
8 AHU1025R-4 12 AHU1540R-4
7 2DC
6 突き出し量:4DC 10 突き出し量:3DC
φ25 5 Overhang φ40 Overhang
4DC 8
AHUL1025R-3 3DC AHUL1540R-4
f 4
z=0.15 fz=0.15 6
3
(mm/t) DC:工具径 (mm/t) 4 DC:工具径
2 Tool Dia. Tool Dia.
1 2
0 5 10 15 20 25 0 10 20 30 40
切込み幅 ae Cutting Width(mm) 切込み幅 ae Cutting Width(mm)
3DC 突き出し量:
9 3DC 2DC 突き出し量:2DC
Overhang 14 Overhang
8 AHU1032R-5 12 AHU1550R-5
7
6 突き出し量:4DC 10 突き出し量:3DC
φ32 5 4DC Overhang φ50 3DC Overhang
AHUL1032R-4 8 AHUL1550R-4
f 4
z=0.15 DC fz=0.15 6
3
(mm/t) :工具径 (mm/t) 4 DC:工具径
2 Tool Dia. Tool Dia.
1 2
0 8 16 24 32 0 10 20 30 40 50
切込み幅 ae Cutting Width(mm) 切込み幅 ae Cutting Width(mm)
【注意】実際の加工では上記領域図を参考に、加工形状や使用機械に合わせて条件を調整してください。
【Note】For actual machining, refer to the range diagrams above and adjust conditions to suit the machining profile and machine used.
・被削材 Work material:S50C(220HB) ・切削速度 Cutting speed:vc=100m/min
モジュラーミル切削領域 Modular mill cutting range ・一刃当りの送り Feed rate:fz=0.1mm/t ・使用機械 Machine:BT50
突出し量 Overhang 120mm 突出し量 Overhang 150mm 突出し量 Overhang 200mm
9 9 9
8 8 8 φ25シャンク+φ25ヘッド
7 7 7 φ25 shank + φ25 head
AHUM1025R-4
6 φ16シャンク+φ16ヘッド 6 φ20シャンク+φ20ヘッド 6 ASC25-12.5-265-145
φ16 shank + φ16 head φ20 shank + φ20 head
5 AHUM1016R-2 5
φ16 AHUM1020R-3 5
4 ASC16-8.5-160-30 φ20 4 ASC20-10.5-220-50Z φ25 4
3 3 3
2 2 2
1 1 1
0 5 10 15 0 5 10 15 20 0 5 10 15 20 25
切込み幅 ae Cutting width(mm) 切込み幅 ae Cutting width(mm) 切込み幅 ae Cutting width(mm)
9 9 9
φ32シャンク+φ30ヘッド
8 φ20シャンク+φ20ヘッド 8 φ25シャンク+φ25ヘッド 8 φ32 shank + φ30 head
φ20 shank + φ20 head φ25 shank + φ25 head
7 AHUM1020R-3 7 AHUM1025R-4 7 AHUM1030R-5
ASC20-10.5-170-90Z ASC25-12.5-215-115 ASC32-17-260-140
6 6 6
φ25シャンク+φ30ヘッド
5 5 φ20シャンク+φ25ヘッド 5
φ16シャンク+φ20ヘッド φ25 shank + φ30 head
φ20 φ25 φ20 shank + φ25 head
4 φ16 shank + φ20 head 4 AHUM1025R-2-M10 φ30 4 AHUM1030R-2-M12
AHUM1020R-2-M8 ASC20-10.5-220-50Z ASC25-12.5-265-145
3 ASC16-8.5-160-30 3 3
2 2 2
1 1 1
0 5 10 15 20 0 5 10 15 20 25 0 5 10 15 20 25 30
切込み幅 ae Cutting width(mm) 切込み幅 ae Cutting width(mm) 切込み幅 ae Cutting width(mm)
【注意】実際の加工では上記領域図を参考に、加工形状や使用機械に合わせて条件を調整してください。
14 【Note】For actual machining, refer to the range diagrams above and adjust conditions to suit the machining profile and machine used.
切込み深さ ap Cutting depth(mm) 切込み深さ ap Cutting depth(mm)
切込み深さ ap 切込み深さ ap 切込み深さ ap 切込み深さ ap
Cutting Depth(mm) Cutting Depth(mm) Cutting Depth(mm) Cutting Depth(mm)
切込み深さ ap Cutting depth(mm) 切込み深さ ap Cutting depth(mm)
切込み深さ ap 切込み深さ ap 切込み深さ ap 切込み深さ ap
Cutting Depth(mm) Cutting Depth(mm) Cutting Depth(mm) Cutting Depth(mm)
切込み深さ ap Cutting depth(mm) 切込み深さ ap Cutting depth(mm)
Page15
切削条件の調整 Adjusting cutting conditions
●工具突出し量、加工状況に合わせて送り速度と回転数の調整が必要となります。
・ The feed rate and spindle rotation speed must be adjusted to suit the tool overhang and machining conditions.
●標準切削条件を100%として、下記表を参考に加工条件の調整を行ってください。
・ Adjust the cutting conditions referring to the percentages in the table below based on the standard cutting conditions at 100%.
突出し量 Overhang
<3DC 3DC~5DC 5DC<
面加工 Face milling 回転数 n Rotation speed 100% 70% 50%
肩削り加工 Shoulder milling 送り速度 vf Feed rate 100% 70% 50%
回転数 n Rotation speed 100% 70% 50%
溝加工 Slotting
送り速度 vf Feed rate 70% 50% 35%
回転数 n Rotation speed 100% 70% 50%
傾斜切削 Ramping
送り速度 vf Feed rate 80% 55% 40%
傾斜切削 Ramping
中心まで切れ刃がないため傾斜角度に制限がありますが、下図に示しますように傾斜切削やヘリカル切削にて下穴がなくてもダイレクトに彫り込み加工が可能です。
Since the cutting flute do not extend to the center, there are limitations on the ramp angle and hole diameter, but as shown below, cutting by direct milling without a pilot hole is possible for
ramping and helical milling.
傾斜角θRamp Angle ヘリカル穴径
Hole Dia.
傾斜切削 Ramping ヘリカル切削 Helical milling
1 AHU(L)/AHUM 10形 type (mm)
工具径DC Tool dia. φ16 φ17 φ18 φ20 φ21 φ22 φ25 φ26 φ28 φ30 φ32 φ33 φ35 φ40
最大傾斜角θ Maximum
ramp angle 4° 4° 4° 3° 3° 3° 2.5° 2.5° 2.5° 2° 2° 2° 1.5° 1°
ヘリカル穴径 Hole Dia. 21~29 23~31 25~33 29~37 31~39 33~41 39~47 41~49 45~53 49~56 53~61 55~63 59~66 69~76
2 AHU(L)/AHUM 15形 type (mm)
工具径DC Tool dia. φ25 φ28 φ30 φ32 φ35 φ40 φ50
最大傾斜角θ Maximum
ramp angle 5° 5° 4° 4° 3.5° 3° 2°
ヘリカル穴径 Hole Dia. 34~47 40~53 43~56 47~60 54~66 64~76 83~96
3 AHUB15形 type (mm)
工具径DC Tool dia. φ50 φ63 φ80 φ100 φ125
最大傾斜角θ Maximum
ramp angle 2° 1.5° 1.0° 0.5° 0.2°
ヘリカル穴径 Hole Dia. 83~96 100~120 135~152 168~192 218~242
【注意】①傾斜角θは上記範囲を超えない様に設定してください。1°以下での使用を推奨します。
②穴径が上記範囲外の場合は下穴を開けて加工してください。
【Note】①Set ramp angle θ within the ranges listed above. We recommend a ramp angle of 1° or less.
② If the hole diameter falls outside the range listed above, drill a pilot hole before milling.
15
Page16
図、表等のデータは試験結果の一例であり、保証値ではありません。
「 」は株式会社MOLDINOの登録商標です。
The diagrams and table data are examples of test results, and are not guaranteed values.
“ ” is a registered trademark of MOLDINO Tool Engineering, Ltd.
安 全 上 の ご 注 意 Attentions on Safety
1. 取扱上のご注意 1. Attentions regarding handling
(1)工具をケース(梱包)から取り出す際は、足元への落下あるいは素手の指先へ落して怪我をしないよ (1) When removing the tool from the case (package), be careful not to drop it on your foot or
うに十分なご注意をお願いします。 drop it onto the tips of your bare fingers.
(2)インサートをセットして実際にご使用する場合は、切れ刃を素手で直接触れないように注意してください。 (2) When actually setting the inserts, be careful not to touch the cutting flute directly with
2. 取付け時のご注意 your bare hands.
(1)ご使用にあたって、インサートのセッティングは確実に行っていただき、アーバ等への取付けも確実に 2. Attentions regarding mounting
行ってください。 (1) When preparing for use, be sure that the inserts are firmly mounted in place and that they
(2)ご使用中に、異常な振動等が発生した場合は、直ちに機械を停止させて、その振動の原因を除いて are firmly mounted on the arbor, etc.
ください。 (2) If abnormal chattering occurs during use, stop the machine immediately and remove the
cause of the chattering.
3. 使用上のご注意
(1)切削工具あるいは被削材の寸法・回転の方向は、あらかじめ確認しておいてください。 3. Attentions during use
(1) Before use, confirm the dimensions and direction of rotation of the tool and milling work
(2)標準切削条件表の数値は、新しい作業の立上げの目安としてご利用ください。切込みが大きい場合、 material.
使用機械の剛性が小さい場合あるいは被加工物の性状に応じて切削条件を適正に調整してご使用 (2) The numerical values in the standard cutting conditions table should be used as criteria when
ください。 starting new work. The cutting conditions should be adjusted as appropriate when the cutting
(3)インサートは硬質の材料です。ご使用中に破損して飛散する場合があります。また、切りくずが飛散す depth is large, the rigidity of the machine being used is low, or according to the conditions of
ることがあります。これらの飛散物等は作業者を切傷させ、火傷あるいは目に入って負傷させる恐れが the work material.
ありますので、工具をご使用中はその周囲に安全カバーを取付け、保護めがね等の保護具を着用し (3) The inserts are made of a hard material. During use, they may break and fly off. In addition,
て安全な環境下での作業をお願いいたします。 cutting chips may also fly off. Since there is a danger of injury to workers, fire, or eye damage
・引火や爆発の危険のあるところでは使用しないでください。 from such flying pieces, a safety cover should be installed and safety equipment such as
・不水溶性切削油は、火災の恐れがありますので使用しないでください。 safety glasses should be worn to create a safe environment for work.
(4)工具を本来の目的以外に使用したり、改造したりしないでください。 ・Do not use where there is a risk of fire or explosion.
・Do not use non-water-soluble cutting oils. Such oils may result in fire.
4. 工具に関して、安全上の問題点・不明の点・その他ご相談がありましたら フリーダイヤル技術相談 へ (4) Do not use the tool for any purpose other than that for which it is intended, and do not modify it.
お問い合わせください。
ホームページ フリーダイヤル技術相談
https://www.moldino.com
MOLDINO Tool Engineering, Ltd.
本社 〒130-0026 東京都墨田区両国4-31-11(ヒューリック両国ビル8階) 工具選定データベース【 TOOLSEARCH】
03-6890-5101 FAX 03-6890-5134
International Sales Dept .: +81-3-6890-5103 FAX +81-3-6890-5128
営業企画部 ☎03-6890-5102 FAX03-6890-5134 海外営業部 ☎03-6890-5103 FAX03-6890-5128
東京営業所 ☎03-6890-5110 FAX03-6890-5133 静岡営業所 ☎054-273-0360 FAX054-273-0361
東北営業所 ☎022-208-5100 FAX022-208-5102 名古屋営業所 ☎052-687-9150 FAX052-687-9144
新潟営業所 ☎0258-87-1224 FAX0258-87-1158 大阪営業所 ☎06-7668-0190 FAX06-7668-0194
東関東営業所 ☎0294-88-9430 FAX0294-88-9432 中四営業所 ☎082-536-2001 FAX082-536-2003
長野営業所 ☎0276-59-6001 FAX0276-59-6005 九州営業所 ☎092-289-7010 FAX092-289-7012
北関東営業所 ☎0276-59-6001 FAX0276-59-6005
神奈川営業所 ☎046-400-9429 FAX046-400-9435
ヨーロッパ/MOLDINO Tool Engineering Europe GmbH Itterpark 12, 40724 Hilden, Germany. TEL : +49-(0)2103-24820, FAX : +49-(0)2103-248230
アメリカ/MITSUBISHI MATERIALS U.S.A. CORPORATION Detroit office c/o RFM Inc. Customer service 2001 Orndorf Drive, Brighton, MI 48116 U.S.A. TEL : +1(248)308-2620, FAX :+1(248)308-2627
メキシコ/MITSUBISHI MATERIALS MÉXICO S.A. DE C.V. Av. La Cañada No.16, Parque Industrial Bernardo Quintana, El Marques, Querétaro, CP 76246, México TEL : +52-442-1926800
ブラジル/MITSUBISHI MATERIALS BRASIL LTDA. Rua Cincinato Braga, 340 13° andar.Bela Vista – CEP 01333-010 São Paulo – SP ., Brasil TEL : +55(11)3506-5600 FAX : +55(11)3506-5677
タ イ/MITSUBISHI MATERIALS (THAILAND) CO., LTD. 139/3 Moo 2, Tambon Khlong Chik, Amphoe Bang Pa-in, Phra Nakhon Si Ayutthaya 13160, Thailand TEL:+66-3525-8024
イ ン ド/Mitsubishi Materials India Private Limited H.O.: Prasad Enclave, #118/119, 1st Floor, 2nd Stage, 5th main, BBMP Ward #11, (New #38), Industrial Suburb, Yeshwanthpura, Bengaluru, 560 022, Karnataka, India. Tel : +91-80-2204-3600
予告なく、改良・改善のために仕様変更することがあります。
Specifications for the products listed in this catalog are subject to change without notice due to ベジタブルインクで印刷しています。 2026-10(ME)
replacement or modification. Printed using vegetable oil ink. Printed in JAPAN 2012-2:FP