

シャンクタイプ / インサート
◆耐摩耗性と靱性のバランスに優れた微粒超硬母材と新コーティング「AJコーティング」の採用により耐摩耗性と耐チッピング性を向上させました。
◆汎用性が高く、30~50HRCの鋼材の切削加工で耐摩耗性と耐チッピング性に優れます。
◆詳細はカタログをダウンロードしご覧いただくか、お気軽にお問い合わせ下さい。
このカタログについて
| ドキュメント名 | アルファ 快削ショルダーミル4コーナ SS4P |
|---|---|
| ドキュメント種別 | 製品カタログ |
| ファイルサイズ | 889.2Kb |
| 登録カテゴリ | |
| 取り扱い企業 | 株式会社MOLDINO (この企業の取り扱いカタログ一覧) |
この企業の関連カタログ


このカタログの内容
Page1
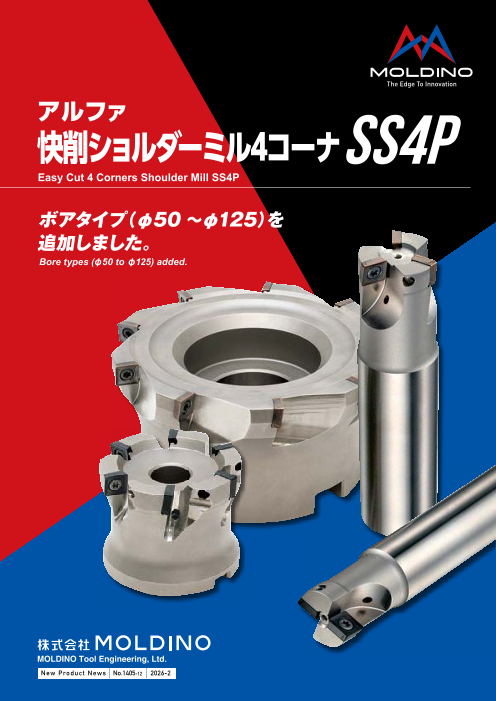
アルファ
快削ショルダーミル4コーナSS4P
Easy Cut 4 Corners Shoulder Mill SS4P
ボアタイプ(φ50~φ125)を
追加しました。
Bore types (φ50 to φ125) added.
MOLDINO Tool Engineering, Ltd.
New Produc t News No.1405-12 2026-2
Page2
切削性能
Cutt ing per formance
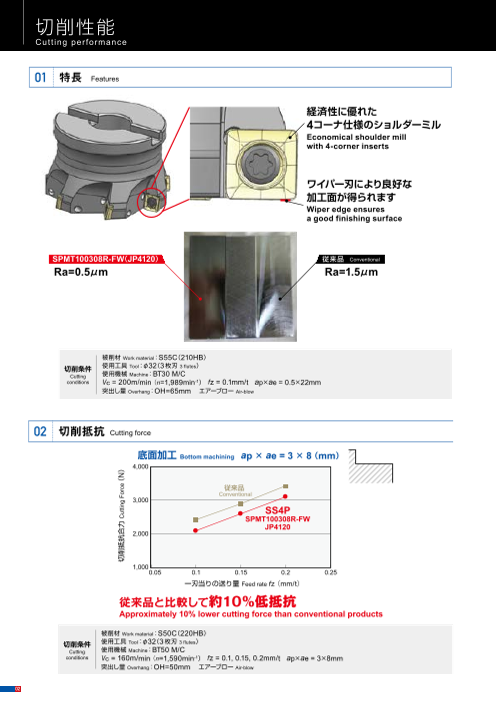
01 特長 Features
経済性に優れた
4コーナ仕様のショルダーミル
Economical shoulder mill
with 4-corner inserts
ワイパー刃により良好な
加工面が得られます
Wiper edge ensures
a good finishing surface
SPMT100308R-FW(JP4120) 従来品 Conventional
Ra=0.5μm Ra=1.5μm
被削材 Work material:S55C(210HB)
切削条件 使用工具 Tool:φ32(3枚刃 3 flutes)
Cutting 使用機械 Machine:BT30 M/C
conditions Vc = 200m/min( n=1,989min-1) fz = 0.1mm/t ap×ae = 0.5×22mm
突出し量 Overhang:OH=65mm エアーブロー Air-blow
02 切削抵抗 Cutting force
底面加工 Bottom machining ap × ae = 3 × 8( mm)
4,000
従来品
Conventional
3,000
SS4P
SPMT100308R-FW
JP4120
2,000
1,000
0.05 0.1 0.15 0.2 0.25
一刃当りの送り量 Feed rate fz( mm/t)
従来品と比較して約10%低抵抗
Approximately 10% lower cutting force than conventional products
被削材 Work material:S50C(220HB)
切削条件 使用工具 Tool:φ32(3枚刃 3 flutes)
Cutting 使用機械 Machine:BT50 M/C
conditions Vc = 160m/min( n=1,590min-1) fz = 0.1, 0.15, 0.2mm/t ap×ae = 3×8mm
突出し量 Overhang:OH=50mm エアーブロー Air-blow
02
切削抵抗合力 Cutting Force( N)
Page3
PVD プリハードン鋼・焼入れ鋼加工用材種 CVD
Technology JP4120 鋼一般加工用材種
Grade for machining pre-hardened or hardened materials Technology General purpose for steel GX2140
特長 Features 特長 Features
● 耐摩耗性と靱性のバランスに優れた微粒超硬母材と新コーティ ●溶着性と耐チッピング性に優れる平滑化α-Al2O3膜の採用に
ング「AJコーティング」の採用により耐摩耗性と耐チッピング性 より、工具刃先の突発チッピングを抑制しました。
を向上させました。 ●微細化柱状組織硬質皮膜の採用により、耐摩耗性に優れ高速
● 汎用性が高く、30~50HRCの鋼材の切削加工で耐摩耗性と耐 乾式加工で加工能率の改善が図れます。
チッピング性に優れます。 ・Smooth surfaced α-Al2O3 layer with improved chipping / welding resistance
・Employs a fine carbide substrate with an excellent balance between wear resistance and brings less sudden-tool-edge-chipping.
toughness and the new "AJ Coating" to provide improved wear resistance and chipping resistance.
・ Highly versatile with excellent wear resistance and chipping resistance when machining steel ・Machining efficiency is improved for high-speed,high-feed-rate rough machining
materials with hardnesses of 30 to 50 HRC. by using the hard-layer with fine columnar structure.
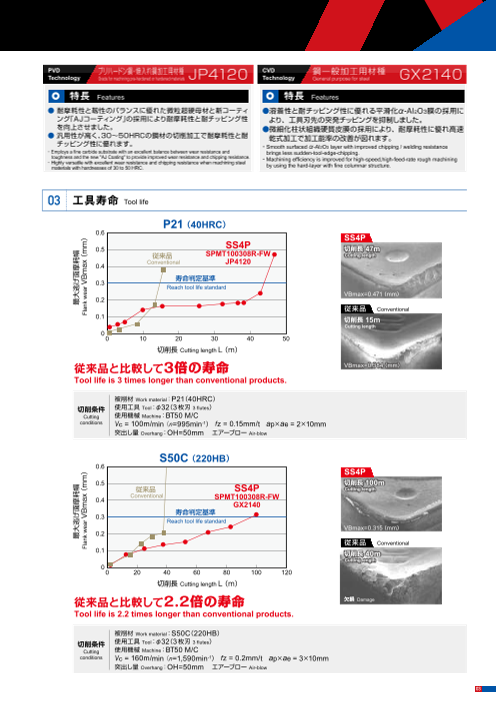
03 工具寿命 Tool life
P21( 40HRC)
0.6
SS4P
0.5 SS4P 切削長 47m
従来品 SPMT100308R-FW Cutting length
Conventional JP4120
0.4
寿命判定基準
0.3
Reach tool life standard
VBmax=0.471( mm)
0.2
従来品 Conventional
0.1 切削長 15m
Cutting length
0
0 10 20 30 40 50
切削長 Cutting length L( m)
従来品と比較して3倍の寿命 VBmax=0.384( mm)
Tool life is 3 times longer than conventional products.
被削材 Work material:P21(40HRC)
切削条件 使用工具 Tool:φ32(3枚刃 3 flutes)
Cutting 使用機械 Machine:BT50 M/C
conditions Vc = 100m/min( n=995min-1) fz = 0.15mm/t ap×ae = 2×10mm
突出し量 Overhang:OH=50mm エアーブロー Air-blow
S50C( 220HB)
0.6
SS4P
0.5
従来品 SS4P 切削長 100m
Cutting length
Conventional
0.4 SPMT100308R-FW
GX2140
寿命判定基準
0.3
Reach tool life standard
VBmax=0.315( mm)
0.2
従来品 Conventional
0.1 切削長 40m
Cutting length
0
0 20 40 60 80 100 120
切削長 Cutting length L( m)
従来品と比較して2.2倍の寿命 欠損 Damage
Tool life is 2.2 times longer than conventional products.
被削材 Work material:S50C(220HB)
切削条件 使用工具 Tool:φ32(3枚刃 3 flutes)
Cutting 使用機械 Machine:BT50 M/C
conditions Vc = 160m/min( n=1,590min-1) fz = 0.2mm/t ap×ae = 3×10mm
突出し量 Overhang:OH=50mm エアーブロー Air-blow
03
最大逃げ面摩耗幅 最大逃げ面摩耗幅
Flank wear VBmax( mm) Flank wear VBmax( mm)
Page4
ラインナップ
Lineup
JP4120 荒 中仕上
GX2140 加工
用途 Roughing Semi
鋳鉄 炭素鋼 ステンレス鋼 プリハードン鋼 焼入れ鋼 焼入れ鋼 Applications Finishing
合金鋼 45~55HRC 55~62HRC
Cast irons Carbon steels Stainless steels Pre-hardened steels Hardened steels Hardened steels
Alloy steels 45̃55HRC 55̃62HRC
シャンクタイプ Shank type SS4P30 S - は数字が入ります。 Numeric figure in a circle .
APMX APMX
LH LS LH LS
LF LF
Aタイプ(一般形 Standard type) Bタイプ(アンダーカット形 Undercut type)
商品コード 在庫 刃数 寸法 Size(mm) 形状 適用インサート 備考
Item code No. of
Stock flutes DC LF APMX LH LS DCONMS Shape Inserts Note
シ SS4P3025S25-2 ● 2 25 120 8 35 85 25 A
ャ SS4P3032S32-3 ● 3 32 130 8 45 SPMT10030 R-FW
ン 85 32 A SPMT100308R-TFW
ク SS4P3040S32-4 ● 4 40 130 8 45 85 32 B
ボアタイプ Bore type SS4P30 B - は数字、 は英文字が入ります。
Numeric figure in a circle and Alphabetical character comes in a square .
DHUB DHUB
DCONMS DCONMS
KWW KWN
DCCB DCCB
DC DC
Aタイプ(エアー穴付き) Bタイプ(エアー穴無し)
with air hole without air hole
商品コード 在庫 刃数 寸法 Size(mm) 形状 適用インサート 備考
Item code Stock No.of
flutes DC APMX DCONMS DCCB DHUB CBDP KWN b LF Shape Inserts Note
SS4P3050B-6 ● 6 50 8 22.225 17 47 19 8.4 5 50 A
内径インチ SS4P3063B-6 ● 6 63 8 22.225 17 60 19 8.4 5 50 A
サイズ
Internal SS4P3080B-7 ● 7 80 8 25.4 20 70 26 9.5 6 50 A
diameter
inch size SS4P3100B-8 ● 8 100 8 31.75 26 96 32 12.7 8 63 A
SS4P3125B-9 ● 9 125 8 38.1 60 100 38 15.9 10 63 B SPMT10030 R-FW
SS4P3050BM-6 ● 6 50 8 22 17 47 20 10.4 6.3 50 A SPMT100308R-TFW
内径ミリ SS4P3063BM-6 ● 6 63 8 22 17 60 20 10.4 6.3 50 A
サイズ
Internal SS4P3080BM-7 ● 7 80 8 27 20 76 22 12.4 7 50 A
diameter
mm size SS4P3100BM-8 ● 8 100 8 32 26 96 25.5 14.4 8 63 A
SS4P3125BM-9 ● 9 125 8 40 60 100 38 16.4 9 63 B
コーナチェンジ時のお願い Attention for the corner change
●コーナチェンジを行う際には、インサートを反時計回りに
回転させてください。
・Please turn the insert counterclockwise upon corner change of insert.
04 ●印:標準在庫品です。●:Stocked items.
Shank type
b
DC
APMX CBDP
LF
CBDP
b DCONMS
DC
APMX DCONMS
LF
Page5
ラインナップ
Lineup
JP4120 荒 中仕上
GX2140 加工 インサート Insert
用途 Roughing Semi
鋳鉄 炭素鋼 ステンレス鋼 プリハードン鋼 焼入れ鋼 焼入れ鋼 Applications Finishing
合金鋼 45~55HRC 55~62HRC FW形 TFW形
Cast irons Carbon steels Stainless steels Pre-hardened steels Hardened steels Hardened steels FW type TFW type
Alloy steels 45̃55HRC 55̃62HRC
インサート
断面形状
シャンクタイプ Shank type SS4P30 S - は数字が入ります。 Insert
Numeric figure in a circle . cross-section
shape Fig.1 Fig.2
黒皮切削、
用途 汎用 強断続切削
Application General purpose Forged surface cutting;
S Strong interrupted cutting
P 鋼 Carbon steels
:一般切削・第一推奨
M SUS等 SUS, etc. General cutting, First recommendation
Aタイプ(一般形 Standard type) Bタイプ(アンダーカット形 Undercut type) K FC・FCD Cast irons :一般切削・第二推奨
General cutting, Second recommendation
商品コード 在庫 刃数 寸法 Size(mm) 形状 適用インサート 備考 S チタン合金 Hardened steels
Item code No. of
Stock flutes DC LF APMX LH LS DCONMS Shape Inserts Note
AJコーティング GXコーティング インサート
シ SS4P3025S25-2 ● 2 25 120 8 35 85 25 A 商品コード ノーズ R 精度 AJ Coating GX Coating 寸 法 Size (mm) 断面形状 備考
ャ Item code Nose radius Tolerance
ン SS4P3032S32-3 ● 3 32 130 8 45 85 32 A SPMT10030 R-FW
class Insert cross-section Note
SPMT100308R-TFW JP4120 GX2140 IC S shape
ク SS4P3040S32-4 ● 4 40 130 8 45 85 32 B
SPMT100304R-FW 0.4 ● ● Fig.1
SPMT100308R-FW 0.8 M 級
M ● ● 10 3.5 Fig.1
SPMT100308R-TFW 0.8 ● ● Fig.2
【注意】GX2140は通電式タッチセンサーに反応しませんのでご注意ください。
【Note】Please note that the GX2140 does not cause a reaction in conductive touch sensors.
部品番号 Parts
部品名 クランプねじ アーバ用ねじ ドライバー ねじ焼き付き防止剤
Parts Clamp screw Arbor screw Screw Driver Screw anti-seizure agent
形状 a
Shape
d
f c エアー穴付き
with air hole
締付トルク
適用カッタ Fastening torque 商品コード φ f
Cutter body (N・m) Item code a b c d
シャンク
Shank type SS4P30 S - - - - - - -
SS4P3050B-6
内径インチ 100-178 M10×1.5 16 35 25 8
SS4P3063B-6
サイズ
Internal SS4P3080B-7 100-179 M12×1.75 18 42 30 10
diameter SS4P3100B-8 100-180 M16×2.0 24 51 35 14
inch size
SS4P3125B-9 412-141 2.9 - - - - - - 104-T15 P-37
SS4P3050BM-6
内径ミリ 100-178 M10×1.5 16 35 25 8
SS4P3063BM-6
サイズ
Internal SS4P3080BM-7 100-179 M12×1.75 18 42 30 10
diameter SS4P3100BM-8 100-180 M16×2.0 24 51 35 14
mm size
SS4P3125BM-9 - - - - - -
【注意】 クランプねじは消耗品です。使用環境により交換寿命は変化しますので早めの交換をお願い致します。
【Note】 The clamp screw is a consumable part. Since replacement life depends on the use environment, it is recommended that it be replaced at an early stage.
傾斜切削について Regarding ramping
傾斜角 θ Ramp angle θ
工具径 DC(mm)
Tool dia. φ25 φ32 φ40~125
傾斜、ヘリカル加工は
最大傾斜角(θ) 推奨いたしません
Maximum ramp angle θ 0.2° 0.2°
Ramping or helical milling is not
recommended.
傾斜切削 Ramping
05
Shank type
φb
IC
Page6
標準切削条件表
Recommended Cut t ing Condi t ions
φ25(2枚刃) (2 Flutes) φ32(3枚刃) (3 Flutes) φ40(4枚刃) (4 Flutes) φ50(6枚刃) (6 Flutes) φ63(6枚刃) (6 Flutes) φ80(7枚刃) (7 Flutes) φ100(8枚刃) (8 Flutes) φ125(9枚刃) (9 Flutes)
被削材 推奨材種 切削速度 一刃当りの送り
ate 被削材
Work material Recommended Cutting speed Feed r 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf
inserts grade Vc(m/min) fz(mm/t) Work material
Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed
min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min
一般構造用鋼 2,290 920 1,790 1,070 1,430 1,140 1,150 1,380 910 1,090 720 1,000 570 920 460 830 一般構造用鋼
Mild steels Mild steels
SS GX2140 150~ 200 0.15 ~ 0.25 SS
(200HB以下) 180m/min, e=0.5DC (200HB以下)
(200HB or less) Vc= fz=0.2mm/t, ap=3mm, a Vc=180m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC (200HB or less)
炭素鋼・合金鋼
Carbon steels 2,040 820 1,590 950 1,270 1,020 1,020 1,220 810 970 640 890 510 810 410 730 炭素鋼・合金鋼
Carbon steels
Alloy steels Alloy steels
S-C SCM GX2140 120~ 180 0.15 ~ 0.25 S-C SCM
(300HB以下) Vc=160m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC Vc=160m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC (300HB以下)
(300HB or less) (300HB or less)
1,270 380 1,000 450 800 480 640 570 510 450 400 420 320 380 250 340
プリハードン鋼 プリハードン鋼
Pre-hardened steels JP4120 80~ 120 0.1 ~ 0.2 Pre-hardened steels
(30~ 40HRC) (30~ 40HRC)
Vc=100m/min, fz=0.15mm/t, ap=2mm, ae=0.5DC Vc=100m/min, fz=0.15mm/t, ap=2mm, ae=0.5DC
プリハードン鋼 890 270 700 310 560 330 450 400 350 320 280 290 220 270 180 240 プリハードン鋼
合金鋼 合金鋼
Pre-hardened steels JP4120 60~80 0.1~0.2 Pre-hardened steels
Alloy steels Alloy steels
(40~ 50HRC) Vc=70m/min, fz=0.15mm/t, ap=2mm, ae=0.5DC Vc=70m/min, fz=0.15mm/t, ap=2mm, ae=0.5DC (40~ 50HRC)
1,270 510 1,000 600 800 640 640 760 510 610 400 560 320 510 250 450
ステンレス鋼 ステンレス鋼
Stainless steels JP4120 80~ 120 0.15 ~ 0.25 Stainless steels
SUS SUS
Vc=100m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC Vc=100m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC
1,780 710 1,390 830 1,110 890 890 1,070 710 850 560 780 450 710 360 640
鋳鉄 鋳鉄
Cast irons JP4120 Cast irons
FC, FCD GX2140 120~ 160 0.15 ~ 0.25
FC, FCD
Vc=140m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC Vc=140m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC
チタン合金 570 170 450 200 360 220 290 260 230 210 180 190 140 170 110 150 チタン合金
(湿式切削) (湿式切削)
Titanium alloys( wet) JP4120 30~ 60 0.1 ~ 0.2 Titanium alloys( wet)
Ti-6Al-4V Vc=45m/min, fz=0.15mm/t, ap=3mm, ae=0.5DC Vc=45m/min, fz=0.15mm/t, ap=3mm, ae=0.5DC Ti-6Al-4V
【注意】①被削材、加工形状に合わせて、適切なクーラントを使用してください。
②この切削条件表は切削条件の目安を示すものです。実際の加工では加工形状、目的、使用機械等により条件を調整してください。
③ GX2140は、通電式タッチセンサーに反応しませんのでご注意ください。
④溝切削の場合、送り速度は 70%を目安として下さい。
⑤インサートの交換は早めに行い、過度の使用による破損を防止して下さい。
⑥排出した切りくずは飛散し作業者を切傷させ、火傷あるいは目に入って負傷させる恐れがありますので、ご使用に際してはその周囲に安全カバーを取り付け保護めがね等の保護
具を着用して、安全な環境で作業される事をお願い致します。
⑦不水溶性切削油は、火災の恐れがありますので使用しないで下さい。
06
Page7
φ25(2枚刃) (2 Flutes) φ32(3枚刃) (3 Flutes) φ40(4枚刃) (4 Flutes) φ50(6枚刃) (6 Flutes) φ63(6枚刃) (6 Flutes) φ80(7枚刃) (7 Flutes) φ100(8枚刃) (8 Flutes) φ125(9枚刃) (9 Flutes)
被削材 推奨材種 切削速度 一刃当りの送り 被削材
Work material Recommended Cutting speed Feed rate 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf 回転数 n 送り速度 Vf n
inserts grade Vc(m/min) fz(mm/t 回転数 送り速度 Vf
) Work material
Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed Revolution Feed speed
min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min min-1 mm/min
一般構造用鋼 2,290 920 1,790 1,070 1,430 1,140 1,150 1,380 910 1,090 720 1,000 570 920 460 830 一般構造用鋼
Mild steels Mild steels
SS GX2140 150~ 200 0.15 ~ 0.25 SS
(200HB以下)
(200HB or less) c=180m/min, 0.5DC (200HB以下)
V fz=0.2mm/t, ap=3mm, ae= Vc=180m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC (200HB or less)
炭素鋼・合金鋼
Carbon steels 2,040 820 1,590 950 1,270 1,020 1,020 1,220 810 970 640 890 510 810 410 730 炭素鋼・合金鋼
Carbon steels
Alloy steels Alloy steels
S-C SCM GX2140 120~ 180 0.15 ~ 0.25 S-C SCM
(300HB以下) Vc=160m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC Vc=160m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC (300HB以下)
(300HB or less) (300HB or less)
1,270 380 1,000 450 800 480 640 570 510 450 400 420 320 380 250 340
プリハードン鋼 プリハードン鋼
Pre-hardened steels JP4120 80~ 120 0.1 ~ 0.2 Pre-hardened steels
(30~ 40HRC) (30~ 40HRC)
Vc=100m/min, fz=0.15mm/t, ap=2mm, ae=0.5DC Vc=100m/min, fz=0.15mm/t, ap=2mm, ae=0.5DC
プリハードン鋼 890 270 700 310 560 330 450 400 350 320 280 290 220 270 180 240 プリハードン鋼
合金鋼 合金鋼
Pre-hardened steels JP4120 60~80 0.1~0.2 Pre-hardened steels
Alloy steels Alloy steels
(40~ 50HRC) Vc=70m/min, fz=0.15mm/t, ap=2mm, ae=0.5DC Vc=70m/min, fz=0.15mm/t, ap=2mm, ae=0.5DC (40~ 50HRC)
1,270 510 1,000 600 800 640 640 760 510 610 400 560 320 510 250 450
ステンレス鋼 ステンレス鋼
Stainless steels JP4120 80~ 120 0.15 ~ 0.25 Stainless steels
SUS SUS
Vc=100m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC Vc=100m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC
1,780 710 1,390 830 1,110 890 890 1,070 710 850 560 780 450 710 360 640
鋳鉄
Cast irons JP4120 鋳鉄
~160 0.15 ~ 0.25 Cast irons
FC, FCD GX2140 120
FC, FCD
Vc=140m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC Vc=140m/min, fz=0.2mm/t, ap=3mm, ae=0.5DC
チタン合金 570 170 450 200 360 220 290 260 230 210 180 190 140 170 110 150 チタン合金
(湿式切削) (湿式切削)
Titanium alloys( wet) JP4120 30~ 60 0.1 ~ 0.2 Titanium alloys( wet)
Ti-6Al-4V Vc=45m/min, fz=0.15mm/t, ap=3mm, ae=0.5DC Vc=45m/min, fz=0.15mm/t, ap=3mm, ae=0.5DC Ti-6Al-4V
【Note】① Use the appropriate coolant for the work material and machining shape.
② These conditions are for general guidance; in actual machining conditions adjust the parameters according to your actual machine and work-piece conditions.
③ Please note that the GX2140 does not cause a reaction in conductive touch sensors.
④ Please reduce feed rate 30% from above table for slotting.
⑤ In order to avoid of insert breakage, please change insert earlier.
⑥ The steel chips may cause cuts, burns or damages to eyes. Be sure to install the safty cover around the tool and wear the safty glasses when carring out any
works.
⑦ Please donʼt use cutting oil as coolant.(It may be cause of fire.)
07
Page8
図、表等のデータは試験結果の一例であり、保証値ではありません。
「 」は株式会社MOLDINOの登録商標です。
The diagrams and table data are examples of test results, and are not guaranteed values.
“ ” is a registered trademark of MOLDINO Tool Engineering, Ltd.
安 全 上 の ご 注 意 Attentions on Safety
1. 取扱上のご注意 1. Attentions regarding handling
(1)工具をケース(梱包)から取り出す際は、足元への落下あるいは素手の指先へ落して怪我をしないよ (1) When removing the tool from the case (package), be careful not to drop it on your foot or
うに十分なご注意をお願いします。 drop it onto the tips of your bare fingers.
(2)インサートをセットして実際にご使用する場合は、切れ刃を素手で直接触れないように注意してください。 (2) When actually setting the inserts, be careful not to touch the cutting flute directly with
2. 取付け時のご注意 your bare hands.
(1)ご使用にあたって、インサートのセッティングは確実に行っていただき、アーバ等への取付けも確実に 2. Attentions regarding mounting
行ってください。 (1) When preparing for use, be sure that the inserts are firmly mounted in place and that they
(2)ご使用中に、異常な振動等が発生した場合は、直ちに機械を停止させて、その振動の原因を除いて are firmly mounted on the arbor, etc.
ください。 (2) If abnormal chattering occurs during use, stop the machine immediately and remove the
cause of the chattering.
3. 使用上のご注意
(1)切削工具あるいは被削材の寸法・回転の方向は、あらかじめ確認しておいてください。 3. Attentions during use
(1) Before use, confirm the dimensions and direction of rotation of the tool and milling work
(2)標準切削条件表の数値は、新しい作業の立上げの目安としてご利用ください。切込みが大きい場合、 material.
使用機械の剛性が小さい場合あるいは被加工物の性状に応じて切削条件を適正に調整してご使用 (2) The numerical values in the standard cutting conditions table should be used as criteria when
ください。 starting new work. The cutting conditions should be adjusted as appropriate when the cutting
(3)インサートは硬質の材料です。ご使用中に破損して飛散する場合があります。また、切りくずが飛散す depth is large, the rigidity of the machine being used is low, or according to the conditions of
ることがあります。これらの飛散物等は作業者を切傷させ、火傷あるいは目に入って負傷させる恐れが the work material.
ありますので、工具をご使用中はその周囲に安全カバーを取付け、保護めがね等の保護具を着用し (3) The inserts are made of a hard material. During use, they may break and fly off. In addition,
て安全な環境下での作業をお願いいたします。 cutting chips may also fly off. Since there is a danger of injury to workers, fire, or eye damage
・引火や爆発の危険のあるところでは使用しないでください。 from such flying pieces, a safety cover should be installed and safety equipment such as
・不水溶性切削油は、火災の恐れがありますので使用しないでください。 safety glasses should be worn to create a safe environment for work.
(4)工具を本来の目的以外に使用したり、改造したりしないでください。 ・Do not use where there is a risk of fire or explosion.
・Do not use non-water-soluble cutting oils. Such oils may result in fire.
4. 工具に関して、安全上の問題点・不明の点・その他ご相談がありましたら フリーダイヤル技術相談 へ (4) Do not use the tool for any purpose other than that for which it is intended, and do not modify it.
お問い合わせください。
ホームページ フリーダイヤル技術相談
https://www.moldino.com
MOLDINO Tool Engineering, Ltd.
本社 〒130-0026 東京都墨田区両国4-31-11(ヒューリック両国ビル8階) 工具選定データベース【 TOOLSEARCH】
03-6890-5101 FAX 03-6890-5134
International Sales Dept .: +81-3-6890-5103 FAX +81-3-6890-5128
営業企画部 ☎03-6890-5102 FAX03-6890-5134 海外営業部 ☎03-6890-5103 FAX03-6890-5128
東京営業所 ☎03-6890-5110 FAX03-6890-5133 静岡営業所 ☎054-273-0360 FAX054-273-0361
東北営業所 ☎022-208-5100 FAX022-208-5102 名古屋営業所 ☎052-687-9150 FAX052-687-9144
新潟営業所 ☎0258-87-1224 FAX0258-87-1158 大阪営業所 ☎06-7668-0190 FAX06-7668-0194
東関東営業所 ☎0294-88-9430 FAX0294-88-9432 中四営業所 ☎082-536-2001 FAX082-536-2003
長野営業所 ☎0276-59-6001 FAX0276-59-6005 九州営業所 ☎092-289-7010 FAX092-289-7012
北関東営業所 ☎0276-59-6001 FAX0276-59-6005
神奈川営業所 ☎046-400-9429 FAX046-400-9435
ヨーロッパ/MOLDINO Tool Engineering Europe GmbH Itterpark 12, 40724 Hilden, Germany. TEL : +49-(0)2103-24820, FAX : +49-(0)2103-248230
アメリカ/MITSUBISHI MATERIALS U.S.A. CORPORATION Detroit office c/o RFM Inc. Customer service 2001 Orndorf Drive, Brighton, MI 48116 U.S.A. TEL : +1(248)308-2620, FAX :+1(248)308-2627
メキシコ/MITSUBISHI MATERIALS MÉXICO S.A. DE C.V. Av. La Cañada No.16, Parque Industrial Bernardo Quintana, El Marques, Querétaro, CP 76246, México TEL : +52-442-1926800
ブラジル/MITSUBISHI MATERIALS BRASIL LTDA. Rua Cincinato Braga, 340 13° andar.Bela Vista – CEP 01333-010 São Paulo – SP ., Brasil TEL : +55(11)3506-5600 FAX : +55(11)3506-5677
タ イ/MITSUBISHI MATERIALS (THAILAND) CO., LTD. 139/3 Moo 2, Tambon Khlong Chik, Amphoe Bang Pa-in, Phra Nakhon Si Ayutthaya 13160, Thailand TEL:+66-3525-8024
イ ン ド/Mitsubishi Materials India Private Limited H.O.: Prasad Enclave, #118/119, 1st Floor, 2nd Stage, 5th main, BBMP Ward #11, (New #38), Industrial Suburb, Yeshwanthpura, Bengaluru, 560 022, Karnataka, India. Tel : +91-80-2204-3600
予告なく、改良・改善のために仕様変更することがあります。
Specifications for the products listed in this catalog are subject to change without notice due to ベジタブルインクで印刷しています。 2026-2(ME)
replacement or modification. Printed using vegetable oil ink. Printed in JAPAN 2014-12:FP