

TR4F形が切り拓く2mm切込み×2mm1刃当り送り量の領域
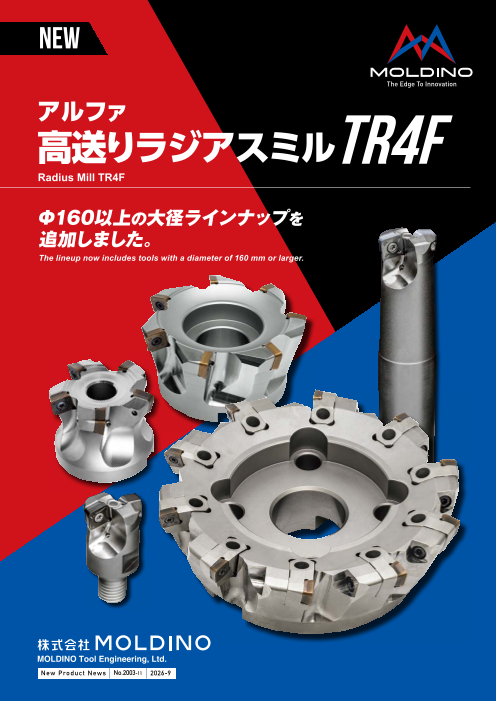
・Φ160以上の大径ラインナップを追加しました。
・インサートに切れ味を重視したLFブレーカを追加しました。
・炭素鋼や合金鋼の切削に優れる材種JS4160を追加しました。
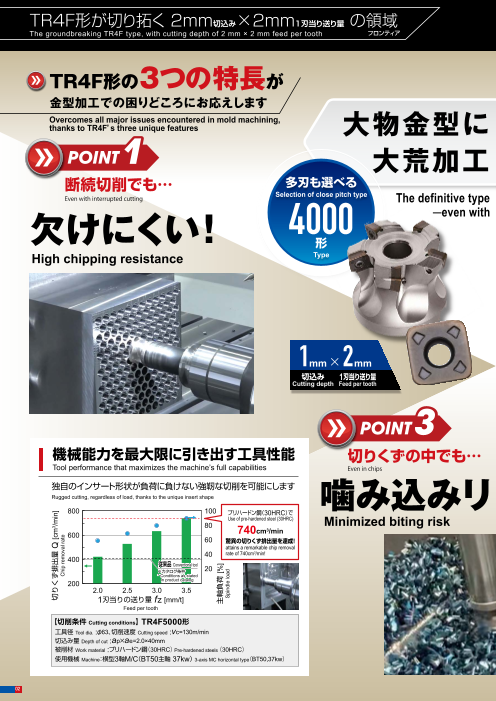
◆断続切削でも欠けにくい!
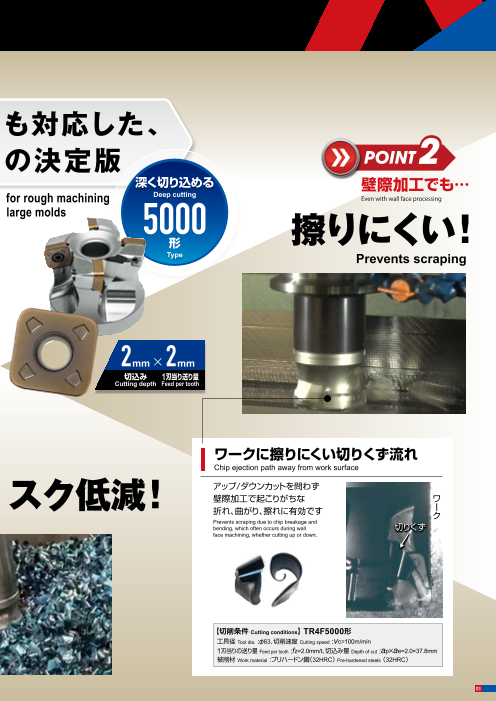
◆壁際加工でも擦りにくい!
◆独自のインサート形状とボディ形状が導く、ひと味違う高能率加工
このカタログについて
| ドキュメント名 | アルファ 高送りラジアスミル TR4F |
|---|---|
| ドキュメント種別 | 製品カタログ |
| ファイルサイズ | 4.9Mb |
| 登録カテゴリ | |
| 取り扱い企業 | 株式会社MOLDINO (この企業の取り扱いカタログ一覧) |
この企業の関連カタログ


このカタログの内容
Page1
NEW
アルファ
高送りラジアスミルTR4F
Radius Mill TR4F
Φ160以上の大径ラインナップを
追加しました。
The lineup now includes tools with a diameter of 160 mm or larger.
MOLDINO Tool Engineering, Ltd.
New Produc t News No.2003-11 2026-9
Page2
TR4F形が切り拓く 2mm切込み × 2mm1刃当り送り量 の領域
The groundbreaking TR4F type, with cutting depth of 2 mm × 2 mm feed per tooth フロンティア
TR4F形の3つの特長が
金型加工での困りどころにお応えします
Overcomes all major issues encountered in mold machining,
thanks to TR4F’s three unique features 大物金型に も対応した、
POINT1 大荒加工 の決定版 POINT2
断続切削でも… 多刃も選べる 深く切り込める 壁際加工でも…
Even with interrupted cutting Selection of close pitch type The definitive type for rough machining Deep cutting Even with wall face processing
̶even with large molds
欠けにくい! 4000 5000
形 形 擦りにくい!
High chipping resistance Type Type Prevents scraping
1mm × 2mm 2mm × 2mm
切込み 1刃当り送り量 切込み 1刃当り送り量
Cutting depth Feed per tooth Cutting depth Feed per tooth
POINT3
機械能力を最大限に引き出す工具性能 切りくずの中でも… ワークに擦りにくい切りくず流れ
Tool performance that maximizes the machine’s full capabilities Even in chips Chip ejection path away from work surface
独自のインサート形状が負荷に負けない強靭な切削を可能にします 噛み込みリ スク低減! アップ/ダウンカットを問わず
Rugged cutting, regardless of load, thanks to the unique insert shape 壁際加工で起こりがちな ワ
800 100 ー
プリハードン鋼(30HRC)で 折れ、曲がり、擦れに有効です
Use of pre-hardened steel (30HRC) ク
80 Minimized biting risk Prevents scraping due to chip breakage and
740cm3/min bending, which often occurs during wall 切りくず
600 face machining, whether cutting up or down.
60 驚異の切りくず排出量を達成!
attains a remarkable chip removal
40 rate of 740cm3/min!
400
従来品 Conventional tool
※カタログ条件 20
* Conditions as stated
in product catalog
200
2.0 2.5 3.0 3.5
1刃当りの送り量 fz [mm/t]
Feed per tooth
【切削条件 Cutting conditions】 TR4F5000形
工具径 Tool dia. :φ63、切削速度 Cutting speed :vc=130m/min 【切削条件 Cutting conditions】 TR4F5000形
切込み量 Depth of cut :ap×ae=2.0×40mm 工具径 Tool dia. :φ63、切削速度 Cutting speed :vc=100m/min
被削材 Work material :プリハードン鋼(30HRC) Pre-hardened steels( 30HRC) 1刃当りの送り量 Feed per tooth :fz=2.0mm/t、切込み量 Depth of cut :ap×ae=2.0×37.8mm
使用機械 Machine:横型3軸M/C(BT50主軸 37kw) 3-axis MC horizontal typ(e BT50,37kw) 被削材 Work material :プリハードン鋼(32HRC) Pre-hardened steels( 32HRC)
02
切りくず排出量 Q [cm3/min]
Chip removal rate
主軸負荷 [%]
Spindle load
Page3
TR4F形が切り拓く 2mm切込み × 2mm1刃当り送り量 の領域
The groundbreaking TR4F type, with cutting depth of 2 mm × 2 mm feed per tooth フロンティア
TR4F形の3つの特長が
金型加工での困りどころにお応えします
Overcomes all major issues encountered in mold machining,
thanks to TR4F’s three unique features 大物金型に も対応した、
POINT1 大荒加工 の決定版 POINT2
断続切削でも… 多刃も選べる 深く切り込める 壁際加工でも…
Even with interrupted cutting Selection of close pitch type The definitive type for rough machining Deep cutting Even with wall face processing
̶even with large molds
欠けにくい! 4000 5000
形 形 擦りにくい!
High chipping resistance Type Type Prevents scraping
1mm × 2mm 2mm × 2mm
切込み 1刃当り送り量 切込み 1刃当り送り量
Cutting depth Feed per tooth Cutting depth Feed per tooth
POINT3
機械能力を最大限に引き出す工具性能 切りくずの中でも… ワークに擦りにくい切りくず流れ
Tool performance that maximizes the machine’s full capabilities Even in chips Chip ejection path away from work surface
独自のインサート形状が負荷に負けない強靭な切削を可能にします 噛み込みリ スク低減! アップ/ダウンカットを問わず
Rugged cutting, regardless of load, thanks to the unique insert shape 壁際加工で起こりがちな ワ
800 100 ー
プリハードン鋼(30HRC)で 折れ、曲がり、擦れに有効です
Use of pre-hardened steel (30HRC) ク
80 Minimized biting risk Prevents scraping due to chip breakage and
740cm3/min bending, which often occurs during wall 切りくず
600 face machining, whether cutting up or down.
60 驚異の切りくず排出量を達成!
attains a remarkable chip removal
40 rate of 740cm3/min!
400
従来品 Conventional tool
※カタログ条件 20
* Conditions as stated
in product catalog
200
2.0 2.5 3.0 3.5
1刃当りの送り量 fz [mm/t]
Feed per tooth
【切削条件 Cutting conditions】 TR4F5000形
工具径 Tool dia. :φ63、切削速度 Cutting speed :vc=130m/min 【切削条件 Cutting conditions】 TR4F5000形
切込み量 Depth of cut :ap×ae=2.0×40mm 工具径 Tool dia. :φ63、切削速度 Cutting speed :vc=100m/min
被削材 Work material :プリハードン鋼(30HRC) Pre-hardened steels( 30HRC) 1刃当りの送り量 Feed per tooth :fz=2.0mm/t、切込み量 Depth of cut :ap×ae=2.0×37.8mm
使用機械 Machine:横型3軸M/C(BT50主軸 37kw) 3-axis MC horizontal typ(e BT50,37kw) 被削材 Work material :プリハードン鋼(32HRC) Pre-hardened steels( 32HRC)
03
切りくず排出量 Q [cm3/min]
Chip removal rate
主軸負荷 [%]
Spindle load
Page4
荒加工は“超”高送りの世界へ
Roughing technique achieves “super” high-feed cutting.
独自のインサート形状とボディ形状が導く、 不安定加工
Unstable machining JS4160 JP4120 JM4160 荒
安定加工 GX2140 JP4105 JP4120 JP4120 加工
ひと味違う高能率加工。 Stable machining 用途 Roughing
炭素鋼 合金鋼 プリハードン鋼 焼入れ鋼 焼入れ鋼 ステンレス鋼 SUS 鋳鉄
合金鋼 (焼入れ焼戻し材) 合金鋼 (55HRC以下)(62HRC以下) 耐熱合金 FC・FCD
Exclusive high-efficiency cutting, (30HRC以下)(35HRC以下)(焼入れ焼戻し材) 超耐熱合金
(45HRC以下) チタン合金
Carbon steels Alloy steels Pre-hardened steels Hardened steels Hardened steels Stainless steels Cast irons
resulting from unique insert and body shapes Alloy steels (Quenched and tempered steels) Alloy steels (55HRC or less)(62HRC or less) Heat resistant alloys
(30HRC or less) (35HRC or less)(Quenched and tempered steels) Super heat resistant alloys
(45HRC or less) Titanium alloys
TR4F形が高能率加工ならではの課題にお応えします。
TR4F type to meet specific challenges posed by high-efficiency cutting 課題 荒加工工程の効率化のために新たな工作機械を導入した。
Issue 高送り加工で加工時間を短縮したいが、送り速度を速めると
02 工具が短寿命になってしまい、機械の能力を発揮できない。
課題 高送り加工で形状加工を行っているが、 New equipment installed to improve the efficiency of the roughing process.
Issue 切りくず詰まりや噛み込みがひどくて能率が上げられない。 The goal is to reduce machining times with high-feed cutting. But higher feed rates reduce tool life
and keep the machine away from delivering its full potential.
01 Although high-feed cutting is performed for shaping,
resulting severe chip clogging and biting may reduce shaping efficiency.
課題解決のご提案!
Proposed solutions
課題解決のご提案! ●独自のインサート形状を開発。広い断面積と拘束面積で高能率加工時の切削負荷に対応します。
Developed a unique insert shape. Performs stable machining despite large cutting load generated during high-feed cutting with large cross-sectional and constraint areas.
Proposed solutions
●独自の不等分割方式を採用し、切削時のびびり振動を抑制します。
●切りくず排出性を高めたボディ形状を採用。 Adopts unique unequal pitch method to reduce chattering during cutting.
突出し量の長い形状部の加工でも切りくず詰まり・噛み込みを抑えます。 ■ねじれのないスムーズな切りくず生成
Generation of smooth twist-free chips 従来品 TR4F形 各分割方法での限界切込深さ(L/D=6)
Adopts new body shape to enhance chip removal. Conventional tool TR4F type Comparison of the maximum depth of cut (L/D=6).
Suppresses chip clogging, even when cutting long overhangs. 従来品 TR4F形 1.4
Conventional tool TR4F type
Point 1 1.2
1
広く開放したポケットによる優 断面積
Cross-sectional 0.8
れた切りくず排出性。 area びびり振動を抑制して
100% 110% 0.6
0.4 約20%の能率向上
Offers excellent chip removal performance thanks 従来品(等分割)
Reduces chatter to improve Conventional tool (equal pitch)
to large open pocket. 0.2 efficiency by roughly 20%. 不等分割品 Unequal pitch
0
600 650 700 750 800 850 900
Point 2 【切削条件 Cutting conditions】
拘束面積 主軸回転数 [min-1]
独自のくびれ形状を採用。 工具径 Tool dia.:φ63
Constraint Spindle speed
切削速度 Cutting speed:vc =130m/min area
工具と壁面の間での切りくず噛み込みを 1刃当りの送り量 Feed per tooth: fz=1.0mm/t 【切削条件 Cutting conditions】
抑制します。 切込み量 Depth of cut:ap×ae=1.0×38mm 100% 135% 工具径 Tool dia.:φ50、刃数 No. of Flutes:4枚刃 4 Flutes、
被削材Work material:S50C(220HB) fz=1.0mm/t、ae=35mm、OH=300mm
Adopts unique constricted shape.
Suppresses chip clogging between tools and wall surfaces. ●インサートの断面積と拘束面積を拡大することにより、 被削材Work material:S50C(220HB)
高負荷な加工においても、インサート強度と拘束力を確保 ●インサートを不等分割ピッチで配列することにより、
します。 びびり振動の主要因である自励振動を抑制します。
ここがポイント! 切りくず流れをコントロールする切れ刃設計 Secures insert strength and constraint force by enlarging cross-sectional and Unequal pitch reduces a vibration, a major factor of chattering.
Point Cutting edge designed to control chip flow constraint areas even in high-load cutting.
●切れ刃設計を適正化し、壁面側へ向かいにくい切りくず流れを実現しました。
切りくずの生成時から詰まりと噛み込みを抑えます。 ここがポイント! 多用途・多鋼種に対応
Optimizes cutting edge design to achieve smooth chip removal flow; keeps chips away from wall surfaces. Point Meets the requirements of various applications and steel types.
Suppresses clogging from the time chip generation starts.
外周方向(壁面側)へ 渦巻き状に ●独自のインサート断面形状と切れ刃設計により幅広い加工形態に対応します。 面削
切りくずを生成 Face milling
らせん状に伸びる切りくず ・The unique cross-sectional shape and cutting edge design of a single insert meets the needs of a wide
Generates helical-shaped chips
Helical chips spreading in range of cutting modes.
peripheral direction 溝 彫込み
(on wall surface side) Slotting Die-sinking
向
外周
方
Peripheral direction
外周
方向
Peripheral direction ●豊富な材種ラインナップで幅広い被削材に対応します。
・Diverse lineup of insert grades to meet the demands posed by a wide range of work materials.
傾斜 バーチカル
Ramping Vertical
従来品 Conventional tool TR4F形 TR4F type
04
軸方向切込み量 [mm]
Axial depth of cut
Page5
荒加工は“超”高送りの世界へ
Roughing technique achieves “super” high-feed cutting.
独自のインサート形状とボディ形状が導く、 不安定加工
Unstable machining JS4160 JP4120 JM4160 荒
安定加工 GX2140 JP4105 JP4120 JP4120 加工
ひと味違う高能率加工。 Stable machining 用途 Roughing
炭素鋼 合金鋼 プリハードン鋼 焼入れ鋼 焼入れ鋼 ステンレス鋼 SUS 鋳鉄
合金鋼 (焼入れ焼戻し材) 合金鋼 (55HRC以下)(62HRC以下) 耐熱合金 FC・FCD
Exclusive high-efficiency cutting, (30HRC以下)(35HRC以下)(焼入れ焼戻し材) 超耐熱合金
(45HRC以下) チタン合金
Carbon steels Alloy steels Pre-hardened steels Hardened steels Hardened steels Stainless steels Cast irons
resulting from unique insert and body shapes Alloy steels (Quenched and tempered steels) Alloy steels (55HRC or less)(62HRC or less) Heat resistant alloys
(30HRC or less) (35HRC or less)(Quenched and tempered steels) Super heat resistant alloys
(45HRC or less) Titanium alloys
TR4F形が高能率加工ならではの課題にお応えします。
TR4F type to meet specific challenges posed by high-efficiency cutting 課題 荒加工工程の効率化のために新たな工作機械を導入した。
Issue 高送り加工で加工時間を短縮したいが、送り速度を速めると
02 工具が短寿命になってしまい、機械の能力を発揮できない。
課題 高送り加工で形状加工を行っているが、 New equipment installed to improve the efficiency of the roughing process.
Issue 切りくず詰まりや噛み込みがひどくて能率が上げられない。 The goal is to reduce machining times with high-feed cutting. But higher feed rates reduce tool life
and keep the machine away from delivering its full potential.
01 Although high-feed cutting is performed for shaping,
resulting severe chip clogging and biting may reduce shaping efficiency.
課題解決のご提案!
Proposed solutions
課題解決のご提案! ●独自のインサート形状を開発。広い断面積と拘束面積で高能率加工時の切削負荷に対応します。
Developed a unique insert shape. Performs stable machining despite large cutting load generated during high-feed cutting with large cross-sectional and constraint areas.
Proposed solutions
●独自の不等分割方式を採用し、切削時のびびり振動を抑制します。
●切りくず排出性を高めたボディ形状を採用。 Adopts unique unequal pitch method to reduce chattering during cutting.
突出し量の長い形状部の加工でも切りくず詰まり・噛み込みを抑えます。 ■ねじれのないスムーズな切りくず生成
Generation of smooth twist-free chips 従来品 TR4F形 各分割方法での限界切込深さ(L/D=6)
Adopts new body shape to enhance chip removal. Conventional tool TR4F type Comparison of the maximum depth of cut (L/D=6).
Suppresses chip clogging, even when cutting long overhangs. 従来品 TR4F形 1.4
Conventional tool TR4F type
Point 1 1.2
1
広く開放したポケットによる優 断面積
Cross-sectional 0.8
れた切りくず排出性。 area びびり振動を抑制して
100% 110% 0.6
0.4 約20%の能率向上
Offers excellent chip removal performance thanks 従来品(等分割)
Reduces chatter to improve Conventional tool (equal pitch)
to large open pocket. 0.2 efficiency by roughly 20%. 不等分割品 Unequal pitch
0
600 650 700 750 800 850 900
Point 2 【切削条件 Cutting conditions】
拘束面積 主軸回転数 [min-1]
独自のくびれ形状を採用。 工具径 Tool dia.:φ63
Constraint Spindle speed
切削速度 Cutting speed:vc =130m/min area
工具と壁面の間での切りくず噛み込みを 1刃当りの送り量 Feed per tooth: fz=1.0mm/t 【切削条件 Cutting conditions】
抑制します。 切込み量 Depth of cut:ap×ae=1.0×38mm 100% 135% 工具径 Tool dia.:φ50、刃数 No. of Flutes:4枚刃 4 Flutes、
被削材Work material:S50C(220HB) fz=1.0mm/t、ae=35mm、OH=300mm
Adopts unique constricted shape.
Suppresses chip clogging between tools and wall surfaces. ●インサートの断面積と拘束面積を拡大することにより、 被削材Work material:S50C(220HB)
高負荷な加工においても、インサート強度と拘束力を確保 ●インサートを不等分割ピッチで配列することにより、
します。 びびり振動の主要因である自励振動を抑制します。
ここがポイント! 切りくず流れをコントロールする切れ刃設計 Secures insert strength and constraint force by enlarging cross-sectional and Unequal pitch reduces a vibration, a major factor of chattering.
Point Cutting edge designed to control chip flow constraint areas even in high-load cutting.
●切れ刃設計を適正化し、壁面側へ向かいにくい切りくず流れを実現しました。
切りくずの生成時から詰まりと噛み込みを抑えます。 ここがポイント! 多用途・多鋼種に対応
Optimizes cutting edge design to achieve smooth chip removal flow; keeps chips away from wall surfaces. Point Meets the requirements of various applications and steel types.
Suppresses clogging from the time chip generation starts.
外周方向(壁面側)へ 渦巻き状に ●独自のインサート断面形状と切れ刃設計により幅広い加工形態に対応します。 面削
切りくずを生成 Face milling
らせん状に伸びる切りくず ・The unique cross-sectional shape and cutting edge design of a single insert meets the needs of a wide
Generates helical-shaped chips
Helical chips spreading in range of cutting modes.
peripheral direction 溝 彫込み
(on wall surface side) Slotting Die-sinking
向
外周
方
Peripheral direction
外周
方向
Peripheral direction ●豊富な材種ラインナップで幅広い被削材に対応します。
・Diverse lineup of insert grades to meet the demands posed by a wide range of work materials.
傾斜 バーチカル
Ramping Vertical
従来品 Conventional tool TR4F形 TR4F type
05
軸方向切込み量 [mm]
Axial depth of cut
Page6
ラインナップ
Line Up
シャンクタイプ 4F40 32- は数字、 は英文字が入ります。
Shank type TR Numeric figure in a circle and Alphabetical character comes in a square .
LH LS LH LS
LF LF
Fig.1( 一般形) Fig.2( アンダーカット形) エアー穴付き
(Standard type) (Undercut type) With air hole
タイプ 商品コード 在庫 刃数 寸 法 Size (mm) 形状 適用インサート 備考
Type Item code Stock No.of
flutes DCX LF LH LS DCONMS Shape Recommended insert Note
レギュラー TR4F4032S32-2 ● 2 32 150 70 80 32 Fig.1
Regular TR4F4040S32-3 ● 3 40 150 50 100 32 Fig.2 SDNW120520TR(-P)
SDMT120520TR
ロング TR4F4032L32-2 ● 2 32 200 120 80 32 Fig.1 SDMT120520ER-LF
Long TR4F4040L32-3 ● 3 40 250 50 200 32 Fig.2
モジュラータイプ ular type TR4F40 M- は数字が入ります。
Mod Numeric figure comes in a circle .
LF DRVS
THSZMS (
( 切
N 欠
otc 部
h 幅
wid )
th)
L1 エアー穴付き
L2 With air hole
商品コード 在庫 刃数 寸 法 Size (mm) 適用インサート 備考
Item code Stock No.of
flutes DCX LF L1 L2 DCONMS DHUB THSZMS DRVS Recommended Insert Note
TR4F4032M-2 ● 2 32 40 6 23 17 28.8 M16 22 SDNW120520TR(-P)
SDMT120520TR
TR4F4040M-3 ● 3 40 40 6 23 17 28.8 M16 22 SDMT120520ER-LF
【注意】 モジュラーミル及び専用シャンク、専用アーバの「工具端面」「モジュラーねじ部」にグリースなどの潤滑剤は塗布しないでください。
【Note】 Do not apply lubricants such as grease,etc. to the "contact faces" and "modular screws" of the "modular mill","dedicated shanks" and "dedicated arbor".
部品番号 Parts サポータタイプ構造
Locater type configuration
部品名 Parts クランプねじ Clamp screw レンチ Wrench ねじ焼き付き防止剤
Screw anti-seizure agent ワッシャ
形状 Washer
Shape 締付トルク
適用カッタ (N・m) 形状
Fastening Shape
Cutter body torque A B C
TR4F40 S/L/M(32)-
TR4F4050B - サポータ引きねじ
Locater draw screw
TR4F4063B - クランプねじ
Clamp screw
TR4F4080BM- 105-T15 A サポータ
Locater
TR4F4080B- 262-141 2.9
TR4F4100B - サポータ止めねじ
TR4F4160B -8 Locater screw
TR4F4200B -10 104-T15 B P-37 【注意】 クランプねじは消耗品です。使用環境により交換寿
TR4F5063B -4 命は変化しますので早めの交換をお願い致します。
TR4F5080BM-5 ワッシャは消耗品です。取り外した際は交換
TR4F5080B-5 105-T20 A を推奨いたします。
TR4F5100B -6 555-141 4.9 【Note】 The c lamp screw is a consumable par t . S ince
TR4F5125B - replacement life depends on the use environment, it is
TR4F5160B -8 recommended that it be replaced at an early stage.
TR4F5200B -10 105-T20L C The washer is a consumable part. It should be replaced
when it is removed.
部品名 Parts アーバ用ねじ Arbor screw サポータ サポータ止めねじ サポータ引きねじ ワッシャ
Locater Locater screw Locater draw screw Washer
a
形状
Shape
適用カッタ a φb c d f
d
Cutter body f c
TR4F40 S/L/M(32)- - - - - - -
TR4F4050B -
TR4F4063B - 100-178 M10×1.5 16 35 25 8
TR4F4080BM- 100-179 M12×1.75 18 42 30 10 - - - -
TR4F4080B-
TR4F4100B - 100-180 M16×2.0 24 51 35 14
TR4F4160B -8
TR4F4200B -10 - - - - - - SD12F-P1 156-161 H04-0520 0905M5
TR4F5063B -4 100-178 M10×1.5 16 35 25 8
TR4F5080BM-5 100-179 M12×1.75 18 42 30 10
TR4F5080B-5 - - - -
TR4F5100B -6 100-180 M16×2.0 24 51 35 14
TR4F5125B - 600-211 M20×2.5 50 50 36 17
TR4F5160B -8
TR4F5200B -10 - - - - - - SD15F-P1 156-161 H04-0520 0905M5
★印:新商品の標準在庫品です。★:Stocked Items of New products. ●印:標準在庫品です。●:Stocked items.
06
φb
DCX
DCONMS
DCX
DCX
DCONMS
DHUB
DCONMS
Page7
ボアタイプ Bore type TR4F B - は数字、 は英文字が入ります。
Numeric figure in a circle and Alphabetical character comes in a square .
DHUB
DHUB
DCONMS
DCONMS
KWW KWW
DCCB DCCB
DCX DCX
Fig.1( エアー穴付き) With air hole Fig.2( エアー穴無し) Without air hole
DHUB DHUB
DCONMS DCONMS
KWW KWW
DCCB DCCB
DCX DCX
Fig.3( エアー穴付き) With air hole Fig.4( エアー穴無し) Without air hole
タイプ 商品コード 在庫 刃数 寸 法 Size (mm)
Type Item code Stock No.of 形状 適用インサート 備考
flutes DCX DHUB LF CBDP KWW b DCONMS DCCB Shape Recommended insert Note
TR4F4050B-3 ● 3
TR4F4050B-4 ● 4 50 47 50 19 8.4 5 22.225 17
TR4F4050B-5 ● 5
TR4F4063B-4 ● 4
TR4F4063B-5 ● 5 63 60 50 19 8.4 5 22.225 17
TR4F4063B-6 ● 6 Fig.1 SDNW120520TR(-P)
TR4F4080B-5 ● 5 SDMT120520TR
内
径 TR4F4080B-7 ● 7 80 76 70 32 12.7 8 31.75 26 SDMT120520ER-LF
イ TR4F4100B-6 ● 6
ン
チ TR4F4100B-8 ● 8 100 96 70 32 12.7 8 31.75 26
サ TR4F4160B-8 ★ 8 160 105 63 43 19.1 11 50.8 72 Fig.3
イ TR4F4200B-10 ★ 10 200 150 63 38 25.4 14 47.625 105 Fig.4
ズ TR4F5063B-4 ● 4 63 60 50 19 8.4 5 22.225 17
TR4F5080B-5 ● 5 80 76 70 32 12.7 8 31.75 26 Fig.1
ボ TR4F5100B-6 ● 6 100 96 70 32 12.7 8 31.75 26 SDNW150525ZTR
ア TR4F5125B-6 ● 6 SDMT150525ZTR
タ TR4F5125B-7 ● 7 125 100 63 38 15.9 10 38.1 60 Fig.2 SDMT150525ZER-LF
イ
プ TR4F5160B-8 ★ 8 160 105 63 43 19.1 11 50.8 72 Fig.3
TR4F5200B-10 ★ 10 200 150 63 38 25.4 14 47.625 105 Fig.4
TR4F4050BM-3 ● 3
TR4F4050BM-4 ● 4 50 47 50 20 10.4 6.3 22 17
TR4F4050BM-5 ● 5
TR4F4063BM-4 ● 4
TR4F4063BM-5 ● 5 63 60 50 20 10.4 6.3 22 17
TR4F4063BM-6 ● 6 Fig.1 SDNW120520TR(-P)
TR4F4080BM-5 ● 5 SDMT120520TR
内 80 76 70 22 12.4 7 27 20 SDMT120520ER-LF
径 TR4F4080BM-7 ● 7
ミ TR4F4100BM-6 ● 6
リ TR4F4100BM-8 ● 8 100 96 70 25.5 14.4 8 32 26
サ TR4F4160BM-8 ★ 8 160 105 63 40 16.4 9 40 56 Fig.3
イ
ズ TR4F4200BM-10 ★ 10 200 150 63 32 25.7 14 60 105 Fig.4
TR4F5063BM-4 ● 4 63 60 50 20 10.4 6.3 22 17
TR4F5080BM-5 ● 5 80 76 70 22 12.4 7 27 20 Fig.1
TR4F5100BM-6 ● 6 100 96 70 25.5 14.4 8 32 26 SDNW150525ZTR
TR4F5125BM-6 ● 6 125 100 63 38 16.4 9 40 60 Fig.2 SDMT150525ZTR
TR4F5125BM-7 ● 7 SDMT150525ZER-LF
TR4F5160BM-8 ★ 8 160 105 63 40 16.4 9 40 56 Fig.3
TR4F5200BM-10 ★ 10 200 150 63 32 25.7 14 60 105 Fig.4
【注意】アーバ用ねじは付属しません。 【Note】Arbor screw is not included.
φ160以上はサポータタイプとなります。φ160でセンタースルーをご使用の場合、アーバ側接続端面にクーラントの供給口をもつアーバをご使用ください。
φ250、φ315は弊社営業所にお問合せください。
Tools with a diameter of 160 mm or larger are locater-type tools. When using a 160 mm diameter hollow-center tool, use an arbor with a coolant feed port on the
arbor side connection end face.
Contact our sales office for more information on 250 and 315 mm diameter tools.
07
Bore type
Internal diameter mm size Internal diameter inch size
b
b
CBDP
LF
CBDP
LF
b
b
CBDP
LF
CBDP
LF
Page8
ラインナップ
Line Up
インサート Insert
S
炭素鋼・合金鋼(30HRC以下)
Carbon steels, Alloy steels(30HRC or less)
P 合金鋼(焼入れ焼戻し材)(35HRC以下)
Alloy steels(Quenched and tempered steels)(35HRC or less)
プリハードン鋼・合金鋼(焼入れ焼戻し材)(45HRC以下)
Pre-hardened steels,Alloy steels(Quenched and tempered steels)(45HRC or less) :一般切削・第一推奨
M ステンレス鋼 Stainless steels SUS General cutting, First recommendation
K 鋳鉄 Cast irons FC・FCD :一般切削・第二推奨
耐熱合金・超耐熱合金 General cutting, Second recommendation
S Heat resistant alloys, Super heat resistant alloys
チタン合金 Titanium alloys
焼入れ鋼(55HRC以下) Hardened steels(55HRC or less)
H
焼入れ鋼(62HRC以下) Hardened steels(62HRC or less)
商品コード 精度 AJコーティング JSコーティング GXコーティング
Coating 寸 法 Size (mm) 備考
Item code Tolerance AJ Coating JS Coating GX
class JP4105 JP4120 JM4160 JS4160 GX2140 IC S Note
SDNW120520TR ● ● ● ● ●
R-P N 級 12.7
SDNW120520T N ●※ 1 5.56
SDNW150525ZTR ● ● ● ● ● 15.875
SDMT120520TR ● ● ● ● 5.76
12.7
SDMT120520ER-LF M 級 ● ● ● 5.596
SDMT150525ZTR M ● ● ● ● 5.61
15.875
SDMT150525ZER-LF ● ● ● 5.596
※ 1:析出硬化系ステンレス鋼の加工にもご使用頂けます。 ※ 1:Can be used to process the precipitation hardening stainless steel.
【注意】GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。
【Note】Please note that the GX Coating and JS Coating do not cause a reaction in conductive touch sensors.
インサートの使い分け Proper use of inserts
刃先強度 Toughness of cutting edge 快削 Easy cutting
SDNW120520TR SDNW120520TR-P SDMT120520TR SDMT120520ER-LF
SDNW150525ZTR SDMT150525ZTR SDMT150525ZER-LF
突き出し量が短く、
断続の少ない加工に推奨 ブレーカ付きインサート シャープな刃先と
刃先強度に優れた第一推奨インサート 特にプリハードン鋼(P20、P21 材)に 低剛性なワークや低馬力なM/C での ねじれ切れ刃形状により低抵抗を実現
一般的な高送り加工に適します 適します 荒加工に適します ※等高線加工によるご使用を推奨いたします
Recommended for relatively continuous
The recommended default insert offers (uninterrupted) cutting with short overhangs. Breaker type insert. Sharp, helical cutting edge ensures low cutting
superior cutting edge strength. Ideal for Ideal for pre-hardened steels (P20 and P21 Ideal for rough machining with low-rigidity resistance.
general high-feed cutting. materials). work materials and low-horsepower M/C. ※Recommended using contour milling.
材種マップ(35HRC未満の鋼材) 被削材別推奨材種マップ
Grade map for less than 35HRC Grade map for work materials
◀耐チッピング性 耐摩耗性▶ 不
Chipping resistance Wear resistance 安
定
加
工
安
定
◀湿式加工 乾式加工▶ 加
Wet cutting Dry cutting 工
炭素鋼 合金鋼 プリハードン鋼 焼入れ鋼 焼入れ鋼 ステンレス鋼 SUS 鋳鉄
合金鋼 (焼入れ焼戻し材) 合金鋼 (55HRC以下) (62HRC以下) 耐熱合金 FC・FCD
(30HRC以下) (35HRC以下) (焼入れ焼戻し材) Hardened steels Hardened steels 超耐熱合金 Cast irons
Carbon steels Alloy steels
teels (Quenched and tempered steels) (45HRC以下)
(55HRC or less) (62HRC or less)
Alloy s チタン合金
0HRC or less)(35HRC or less) Pre-hardened steels Stainless steels
(3
Alloy steels Heat resistant alloys
(Quenched and tempered steels) Super heat resistant alloys
(45HRC or less) Titanium alloys
●印:標準在庫品です。●:Stocked items. 無印:弊社営業へお問合せください。 No mark:Contact with our sales department.
08
Stable Unstable
machining machining
IC
Page9
標準切削条件表
Recommended Cut t ing Condi t ions
ae ap
①シャンクタイプ・モジュラータイプ Shank type TR4F4000形(TR4F40 S/M/(L 32)- )
/ Modular type は数字が入ります。 Numeric figure in a circle .
等高線荒加工標準切削条件 Standard cutting conditions for contour roughing
タイプ Type シャンクタイプ Shank Type モジュラータイプ Modular Type
工具径 DCX
推奨 φ32(2枚刃) (2 Flutes) φ40(3枚刃) (3 Flutes) φ32(2枚刃) (2 Flutes) φ40(3枚刃) (3 Flutes)
Tool dia.
被削材 材種 <3DCX <3DCX <3DCX <3DCX
Work material Recommended 突出し量
inserts grade Overhang 汎用 高速加工 汎用 高速加工 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX
General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting
炭素鋼 n (min-1) 1490 1990 1190 1590 1490 1990 1490 1190 1590 1190
Vc(m/min) 150 200 150 200 150 200 150 150 200 150
合金鋼 V f (mm/min) 5360 7960 6430 9540 5360 7960 5360 6430 9540 6430
( GX2140
30HRC 以下) fz(mm/t) 1.8 2.0 1.8 2.0 1.8 2.0 1.8 1.8 2.0 1.8
Carbon steels JS4160 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
Alloy steels ae(mm) 14 14 22 22 14 14 14 22 22 22
(30HRC or less) Q(cm3/min) 75 111 141 210 75 111 75 141 210 141
合金鋼 n (min-1) 1490 1990 1190 1590 1490 1990 1490 1190 1590 1190
Vc(m/min) 150 200 150 200 150 200 150 150 200 150
(焼入れ焼戻し材) Vf(mm/min) 5360 7960 6430 9540 5360 7960 5360 6430 9540 6430
(35HRC 以下) JS4160
fz(mm/t) 1.8 2.0 1.8 2.0 1.8 2.0 1.8 1.8 2.0 1.8
Alloy steels GX2140 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
(Quenched and tempered steels) a
( e(mm) 14 14 22 22 14 14 14 22 22 22
35HRC or less) Q(cm3/min) 75 111 141 210 75 111 75 141 210 141
プリハードン鋼・合金鋼 n (min-1) 1290 1490 1030 1190 1290 1490 1290 1030 1190 1030
(焼入れ焼戻し材) Vc(m/min) 130 150 130 150 130 150 130 130 150 130
(45HRC以下) V f (mm/min) 4640 5960 5560 7140 4640 5960 4640 5560 7140 5560
Pre-hardened steels JP4120 fz(mm/t) 1.8 2.0 1.8 2.0 1.8 2.0 1.8 1.8 2.0 1.8
Alloy steels ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
(Quenched and tempered steels) ae(mm) 14 14 22 22 14 14 14 22 22 22
(45HRC or less) Q(cm3/min) 65 83 122 157 65 83 65 122 157 122
n (min-1) 800 900 640 720 800 900 800 640 720 640
焼入れ鋼 Vc(m/min) 80 90 80 90 80 90 80 80 90 80
(55HRC以下) JP4105 Vf(mm/min) 800 1440 960 1730 800 1440 800 960 1730 960
fz(mm/t) 0.5 0.8 0.5 0.8 0.5 0.8 0.5 0.5 0.8 0.5
Hardened steels JP4120 ap(mm) 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8
(55HRC or less) ae(mm) 14 14 22 22 14 14 14 22 22 22
Q(cm3/min) 9 16 17 30 9 16 9 17 30 17
n (min-1) 600 600 480 480 600 600 600 480 480 480
焼入れ鋼 Vc(m/min) 60 60 60 60 60 60 60 60 60 60
Vf(mm/min) 360 600 430 720 360 600 360 430 720 430
(62HRC以下) JP4105 fz(mm/t) 0.3 0.5 0.3 0.5 0.3 0.5 0.3 0.3 0.5 0.3
Hardened steels ap(mm) 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5
(62HRC or less) ae(mm) 14 14 22 22 14 14 14 22 22 22
Q(cm3/min) 3 4 5 8 3 4 3 5 8 5
n (min-1) 990 1990 800 1590 990 1990 990 800 1590 800
Vc(m/min) 100 200 100 200 100 200 100 100 200 100
ステンレス鋼 JM4160 V f (mm/min) 1980 3980 2400 4770 1980 3980 1980 2400 4770 2400
Stainless steels fz(mm/t) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
SUS JP4120 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
ae(mm) 14 14 22 22 14 14 14 22 22 22
Q(cm3/min) 28 56 53 105 28 56 28 53 105 53
n (min-1) 1490 1990 1190 1590 1490 1990 1490 1190 1590 1190
鋳鉄 Vc(m/min) 150 200 150 200 150 200 150 150 200 150
Cast irons V f (mm/min) 5960 7960 7140 9540 5960 7960 5960 7140 9540 7140
FC JP4120 fz(mm/t) 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0
ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
FCD ae(mm) 14 14 22 22 14 14 14 22 22 22
Q(cm3/min) 83 111 157 210 83 111 83 157 210 157
n (min-1) 350 ― 280 ― 350 ― 350 280 ― 280
耐熱合金 Vc(m/min) 35 ― 35 ― 35 ― 35 35 ― 35
280 ― 280 340 ― 340
超耐熱合金 JM4160 V f (mm/min) 280 ― 340 ―
fz(mm/t) 0.4 ― 0.4 ― 0.4 ― 0.4 0.4 ― 0.4
Heat resistant alloys JP4120 ap(mm) 1.0 ― 1.0 ― 1.0 ― 1.0 1.0 ― 1.0
Super heat resistant alloys ae(mm) 14 ― 22 ― 14 ― 14 22 ― 22
Q(cm3/min) 4 ― 7 ― 4 ― 4 7 ― 7
n (min-1) 500 ― 400 ― 500 ― 500 400 ― 400
Vc(m/min) 50 ― 50 ― 50 ― 50 50 ― 50
チタン合金 JM4160 V f (mm/min) 400 ― 480 ― 400 ― 400 480 ― 480
fz(mm/t) 0.4 ― 0.4 ― 0.4 ― 0.4 0.4 ― 0.4
Titanium alloys JP4120 ap(mm) 1.0 ― 1.0 ― 1.0 ― 1.0 1.0 ― 1.0
ae(mm) 14 ― 22 ― 14 ― 14 22 ― 22
Q(cm3/min) 6 ― 11 ― 6 ― 6 11 ― 11
バーチカル荒加工標準切削条件 【注意】
Standard cutting conditions for vertical roughing ①本表は切削条件の目安を示すものです。機械剛性やツーリング、加工物の状態に
バーチカル加工には、型番の末尾に「-P」「-LF」が付かないタイプのインサートのご使用を推奨いたします。 合わせて調整してください。
For vertical machining, we recommend using inserts without the "-P" or "-LF" suffixes 特に、溝切削を伴う、またはそれに近い切込み幅の加工などで、切りくずの噛み込みやビ
appended to the product code. ビり振動が発生し、トラブルに至る場合がありますので下記を参考に調整してください。
・回転数、テーブル送り量を 50~ 70%下げる。
推奨 工具径 DCX ・切込み深さapを 50~ 70%下げる。
被削材 φ 32(2枚刃) (2 Flutes) φ 40(3枚刃) (3 Flutes)
材種 Tool dia. ・切込み幅 aeを 50~ 70%下げる。
Work material Recommended 突出し量 ② GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんので
inserts grade <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX
Overhang ご注意ください。
n (min-1) 1990 1990 1590 1590
鋳鉄 ③「JP4105」は高硬度鋼専用材種で、生材には適しません。
Vc(m/min) 200 200 200 200 ④焼入れ鋼(50~62HRC) は、鋼種や工具突き出し量によって被削性が大きく異な
Cast irons V f (mm/min) 600 600 720 720 る場合があります。加工状況に合わせて、テーブル送り量と切込み深さapを調
FC JP4120 fz(mm/t) 0.15 0.15 0.15 0.15 整してください。
FCD pf(mm) ≦ 0.5DCX ≦ 0.5DCX
a ⑤強断続切削、突出しが長い場合及び湿式切削には「JM4160」を推奨します。
e(mm) ≦ 9.0 ≦ 9.0 ⑥切りくず噛み込みによる工具損傷防止のため、必ずエアーブロー等による切りく
pf ず除去を行ってください。
⑦排出した切りくずは、飛散し作業者を切傷させ、火傷あるいは目に入って負傷さ
せる恐れがありますので、ご使用に際してはその周囲に安全カバーを取付け、保
ae 護メガネ等の保護具を着用し、安全な環境で作業されることをお願い致します。
⑧インサートの交換は早めに行い、過度の使用による破損を防止してください。
⑨突出し量 5DCX 以上の場合は、弊社防振アーバの適用を推奨致します。
⑩右記に単位時間当たりの切りくず排出量Qを示します。
Q(cm3/min)=ap(mm)×ae(mm)×Vf(mm/min)/1000 09
Page10
標準切削条件表
Recommended Cut t ing Condi t ions
②ボアタイプ は数字、 は英文字が入ります。
Bore type TR4F4000形(TR4F4 B - ) Numeric figure in a circle and Alphabetical character comes in a square .
等高線荒加工標準切削条件 Standard cutting conditions for contour roughing
工具径 DCX
被削材 推奨材種 Tool dia. φ 50(3枚刃) (3 Flutes) φ 50(4枚刃) (4 Flutes) φ 50(5枚刃) (5 Flutes) φ 63(4枚刃) (4 Flutes) φ 63(5枚刃) (5 Flutes) φ 63(6枚刃) (6 Flutes)
被削材
Work material Recommended <3DCX <3DCX <3DCX <3DCX <3DCX <3DCX
inserts grade 突出し量 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX Work material
Overhang 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX
General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting
炭素鋼 n (min-1) 950 1270 950 950 1270 950 950 1270 950 760 1010 760 760 1010 760 760 1010 760
Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 炭素鋼
合金鋼
( GX2140 V f (mm/min) 5130 7620 5130 6840 10160 6840 8550 12700 8550 5470 8080 5470 6840 10100 6840 8210 12120 8210 合金鋼
30HRC 以下) fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (30HRC 以下)
Carbon steels JS4160 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Carbon steels
Alloy steels ae(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 Alloy steels
(30HRC or less) Q(cm3/min) 154 229 154 205 305 205 257 381 257 241 356 241 301 444 301 361 533 361 (30HRC or less)
合金鋼 n (min-1) 950 1270 950 950 1270 950 950 1270 950 760 1010 760 760 1010 760 760 1010 760
Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 合金鋼
(焼入れ焼戻し材)
(35HRC 以下) JS4160 Vf(mm/min) 5130 7620 5130 6840 10160 6840 8550 12700 8550 5470 8080 5470 6840 10100 6840 8210 12120 8210 (焼入れ焼戻し材)
fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (35HRC 以下)
Alloy steels GX2140 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Alloy steels
(Quenched and tempered steels) a
( e(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 (Quenched and tempered steels)
35HRC or less) Q(cm3/min) 154 229 154 205 305 205 257 381 257 241 356 241 301 444 301 361 533 361 (35HRC or less)
プリハードン鋼・合金鋼 n (min-1) 830 950 830 830 950 830 830 950 830 660 760 660 660 760 660 660 760 660 プリハードン鋼・合金鋼
(焼入れ焼戻し材) Vc(m/min) 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 (焼入れ焼戻し材)
(45HRC以下) V f (mm/min) 4480 5700 4480 5980 7600 5980 7470 9500 7470 4750 6080 4750 5940 7600 5940 7130 9120 7130
Pre-hardened steels JP4120 fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (45HRC以下)
a Pre-hardened steels
Alloy steels p(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
a Alloy steels
(Quenched and tempered steels) e(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 (Quenched and tempered steels)
(45HRC or less) Q(cm3/min) 134 171 134 179 228 179 224 285 224 209 268 209 261 334 261 314 401 314 (45HRC or less)
n (min-1) 510 570 510 510 570 510 510 570 510 400 450 400 400 450 400 400 450 400
焼入れ鋼 Vc(m/min) 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80
Vf(mm/min) 770 1370 770 1020 1820 1020 1280 2280 1280 800 1440 800 1000 1800 1000 1200 2160 1200
(55HRC以下) JP4105 焼入れ鋼
fz(mm/t) 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 (55HRC以下)
Hardened steels JP4120 ap(mm) 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 Hardened steels
(55HRC or less) ae(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 (55HRC or less)
Q(cm3/min) 18 33 18 24 44 24 31 55 31 28 51 28 35 63 35 42 76 42
n (min-1) 380 380 380 380 380 380 380 380 380 300 300 300 300 300 300 300 300 300
焼入れ鋼 Vc(m/min) 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60
V f (mm/min) 340 570 340 460 760 460 570 950 570 360 600 360 450 750 450 540 900 540 焼入れ鋼
(62HRC以下) JP4105 fz(mm/t) 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 (62HRC以下)
Hardened steels ap(mm) 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 Hardened steels
(62HRC or less) ae(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 (62HRC or less)
Q(cm3/min) 5 9 5 7 11 7 9 14 9 8 13 8 10 17 10 12 20 12
n (min-1) 640 1270 640 640 1270 640 640 1270 640 510 1010 510 510 1010 510 510 1010 510
Vc(m/min) 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100
ステンレス鋼 JM4160 V f (mm/min) 1920 3810 1920 2560 5080 2560 3200 6350 3200 2040 4040 2040 2550 5050 2550 3060 6060 3060 ステンレス鋼
Stainless steels fz(mm/t) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Stainless steels
SUS JP4120 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
a SUS
e(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44
Q(cm3/min) 58 114 58 77 152 77 96 191 96 90 178 90 112 222 112 135 267 135
n (min-1) 950 1270 950 950 1270 950 950 1270 950 760 1010 760 760 1010 760 760 1010 760
鋳鉄 Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 鋳鉄
Cast irons V f (mm/min) 5700 7620 5700 7600 10160 7600 9500 12700 9500 6080 8080 6080 7600 10100 7600 9120 12120 9120 Cast irons
FC JP4120 fz(mm/t) 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0
ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 FC
FCD ae(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 FCD
Q(cm3/min) 171 229 171 228 305 228 285 381 285 268 356 268 334 444 334 401 533 401
n (min-1) 220 ― 220 220 ― 220 220 ― 220 180 ― 180 180 ― 180 180 ― 180
耐熱合金 Vc(m/min) 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35
JM4160 V f (mm/min) 260 ― 260 350 ― 350 440 ― 440 290 ― 290 360 ― 360 430 ― 430 耐熱合金
超耐熱合金 fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 超耐熱合金
Heat resistant alloys JP4120 ap(mm) 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 Heat resistant alloys
Super heat resistant alloys ae(mm) 30 ― 30 30 ― 30 30 ― 30 44 ― 44 44 ― 44 44 ― 44 Super heat resistant alloys
Q(cm3/min) 8 ― 8 11 ― 11 13 ― 13 13 ― 13 16 ― 16 19 ― 19
n (min-1) 320 ― 320 320 ― 320 320 ― 320 250 ― 250 250 ― 250 250 ― 250
Vc(m/min) 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50
チタン合金 JM4160 V f (mm/min) 380 ― 380 510 ― 510 640 ― 640 400 ― 400 500 ― 500 600 ― 600
fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 チタン合金
Titanium alloys JP4120 ap(mm) 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 Titanium alloys
ae(mm) 30 ― 30 30 ― 30 30 ― 30 44 ― 44 44 ― 44 44 ― 44
Q(cm3/min) 11 ― 11 15 ― 15 19 ― 19 18 ― 18 22 ― 22 26 ― 26
バーチカル荒加工標準切削条件 Standard cutting conditions for vertical roughing
バーチカル加工には、型番の末尾に「-P」「-LF」が付かないタイプのインサートのご使用を推奨いたします。
For vertical machining, we recommend using inserts without the "-P" or "-LF" suffixes appended to the product code.
被削材 推奨材種 工具径 DCX
Tool dia. φ 50(3枚刃) (3 Flutes) φ 50(4枚刃) (4 Flutes) φ 50(5枚刃) (5 Flutes) φ 63(4枚刃) (4 Flutes) φ 63(5枚刃) (5 Flutes) φ 63(6枚刃) (6 Flutes)
被削材
Work material Recommended
inserts grade 突出し量 <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX Work material
Overhang
鋳鉄 n (min-1) 1270 1270 1270 1270 1270 1270 1010 1010 1010 1010 1010 1010
Vc(m/min) 200 200 200 200 200 200 200 200 200 200 200 200 鋳鉄
Cast irons V f (mm/min) 760 760 1020 1020 1270 1270 810 810 1010 1010 1210 1210 Cast irons
FC JP4120 fz(mm/t) 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 FC
FCD pf(mm) ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX
ae(mm) ≦ 9.0 ≦ 9.0 ≦ 9.0 ≦ 9.0 ≦ 9.0 ≦ 9.0 FCD
【注意】①本表は切削条件の目安を示すものです。機械剛性やツーリング、加工物の状態に合わせて調整してください。
特に、溝切削を伴う、またはそれに近い切込み幅の加工などで、切りくずの噛み込みやビビり振動が発生し、トラブルに至る場合がありますので下記を参考に調整してください。
・回転数、テーブル送り量を 50~ 70%下げる。
・切込み深さapを 50~ 70%下げる。
・切込み幅 aeを 50~ 70%下げる。
② GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。
③「JP4105」は高硬度鋼専用材種で、生材には適しません。
④焼入れ鋼(50~62HRC) は、鋼種や工具突き出し量によって被削性が大きく異なる場合があります。加工状況に合わせて、テーブル送り量と切込み深さapを調整してください。
⑤強断続切削、突出しが長い場合及び湿式切削には「JM4160」を推奨します。
⑥切りくず噛み込みによる工具損傷防止のため、必ずエアーブロー等による切りくず除去を行ってください。
⑦排出した切りくずは、飛散し作業者を切傷させ、火傷あるいは目に入って負傷させる恐れがありますので、ご使用に際してはその周囲に安全カバーを取付け、保護メガネ等の保
護具を着用し、安全な環境で作業されることをお願い致します。
⑧インサートの交換は早めに行い、過度の使用による破損を防止してください。
⑨突出し量 5DCX 以上の場合は、弊社防振アーバの適用を推奨致します。
10 ⑩右記に単位時間当たりの切りくず排出量Qを示します。 Q(cm3/min)=ap(mm)×ae(mm)×Vf(mm/min)/1000
Page11
※高能率条件は、ご使用の機械の動力・トルク線図をご確認いただき、主軸の定格動力を確保できる回転数での適用を推奨いたします。
・機械動力が不足する場合は、まず切込み深さを下げてください。次いで回転数およびテーブル送り量を下げてご使用ください。
※ To ensure high-efficiency conditions, we recommend checking the machineʼs power/torque chart and using a rotation ae ap
speed that can maintain the rated power of the spindle.
・If the machine lacks sufficient power, first reduce cutting depth, then reduce the rotation speed and table feed rate.
工具径 DCX 刃) (3 Flutes) φ 50(4枚刃) (4 Flutes) φ 50(5枚刃) (5 Flutes) φ 63(4枚刃) (4 Flutes) φ 63(5枚刃) (5 Flutes) φ 63(6枚刃) (6 Flutes)
被削材 推奨材種 Tool dia. φ 50(3枚
<3DCX <3DCX <3DCX <3DCX <3DCX <3DCX 被削材
Work material Recommended
inserts grade 突出し量 Work material
汎用 高速加工 3DCX-5DCX 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX
Overhang 汎用
General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting
炭素鋼 n (min-1) 950 1270 950 950 1270 950 950 1270 950 760 1010 760 760 1010 760 760 1010 760
Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 炭素鋼
合金鋼 V f (mm/min) 5130 7620 5130 6840 10160 6840 8550 12700 8550 5470 8080 5470 6840 10100 6840 8210 12120 8210 合金鋼
( GX2140
30HRC 以下) fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (30HRC 以下)
Carbon steels JS4160 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Carbon steels
Alloy steels ae(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 Alloy steels
(30HRC or less) Q(cm3/min) 154 229 154 205 305 205 257 381 257 241 356 241 301 444 301 361 533 361 (30HRC or less)
合金鋼 n (min-1) 950 1270 950 950 1270 950 950 1270 950 760 1010 760 760 1010 760 760 1010 760
Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 合金鋼
(焼入れ焼戻し材) Vf(mm/min) 5130 7620 5130 6840 10160 6840 8550 12700 8550 5470 8080 5470 6840 10100 6840 8210 12120 8210
(35HRC 以下) JS4160 (焼入れ焼戻し材)
fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (35HRC 以下)
Alloy steels GX2140 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Alloy steels
(Quenched and tempered steels) ae(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 (Quenched and tempered steels)
(35HRC or less) Q(cm3/min) 154 229 154 205 305 205 257 381 257 241 356 241 301 444 301 361 533 361 (35HRC or less)
プリハードン鋼・合金鋼 n (min-1) 830 950 830 830 950 830 830 950 830 660 760 660 660 760 660 660 760 660 プリハードン鋼・合金鋼
(焼入れ焼戻し材) Vc(m/min) 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 (焼入れ焼戻し材)
(45HRC以下) V f (mm/min) 4480 5700 4480 5980 7600 5980 7470 9500 7470 4750 6080 4750 5940 7600 5940 7130 9120 7130
Pre-hardened steels JP4120 fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (45HRC以下)
a Pre-hardened steels
Alloy steels p(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
a Alloy steels
(Quenched and tempered steels) e(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 (Quenched and tempered steels)
(45HRC or less) Q(cm3/min) 134 171 134 179 228 179 224 285 224 209 268 209 261 334 261 314 401 314 (45HRC or less)
n (min-1) 510 570 510 510 570 510 510 570 510 400 450 400 400 450 400 400 450 400
焼入れ鋼 Vc(m/min) 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80
Vf(mm/min) 770 1370 770 1020 1820 1020 1280 2280 1280 800 1440 800 1000 1800 1000 1200 2160 1200 焼入れ鋼
(55HRC以下) JP4105
fz(mm/t) 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 (55HRC以下)
Hardened steels JP4120 ap(mm) 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 Hardened steels
(55HRC or less) ae(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 (55HRC or less)
Q(cm3/min) 18 33 18 24 44 24 31 55 31 28 51 28 35 63 35 42 76 42
n (min-1) 380 380 380 380 380 380 380 380 380 300 300 300 300 300 300 300 300 300
焼入れ鋼 Vc(m/min) 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60
V f (mm/min) 340 570 340 460 760 460 570 950 570 360 600 360 450 750 450 540 900 540 焼入れ鋼
(62HRC以下) JP4105 fz(mm/t) 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 (62HRC以下)
Hardened steels ap(mm) 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 Hardened steels
(62HRC or less) ae(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 (62HRC or less)
Q(cm3/min) 5 9 5 7 11 7 9 14 9 8 13 8 10 17 10 12 20 12
n (min-1) 640 1270 640 640 1270 640 640 1270 640 510 1010 510 510 1010 510 510 1010 510
Vc(m/min) 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100
ステンレス鋼 JM4160 V f (mm/min) 1920 3810 1920 2560 5080 2560 3200 6350 3200 2040 4040 2040 2550 5050 2550 3060 6060 3060 ステンレス鋼
Stainless steels fz(mm/t) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Stainless steels
SUS JP4120 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
a SUS
e(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44
Q(cm3/min) 58 114 58 77 152 77 96 191 96 90 178 90 112 222 112 135 267 135
n (min-1) 950 1270 950 950 1270 950 950 1270 950 760 1010 760 760 1010 760 760 1010 760
鋳鉄 Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 鋳鉄
Cast irons V f (mm/min) 5700 7620 5700 7600 10160 7600 9500 12700 9500 6080 8080 6080 7600 10100 7600 9120 12120 9120 Cast irons
FC JP4120 fz(mm/t) 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0
ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 FC
FCD ae(mm) 30 30 30 30 30 30 30 30 30 44 44 44 44 44 44 44 44 44 FCD
Q(cm3/min) 171 229 171 228 305 228 285 381 285 268 356 268 334 444 334 401 533 401
n (min-1) 220 ― 220 220 ― 220 220 ― 220 180 ― 180 180 ― 180 180 ― 180
耐熱合金 Vc(m/min) 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35
超耐熱合金 JM4160 V f (mm/min) 260 ― 260 350 ― 350 440 ― 440 290 ― 290 360 ― 360 430 ― 430 耐熱合金
fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 超耐熱合金
Heat resistant alloys JP4120 ap(mm) 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 Heat resistant alloys
Super heat resistant alloys ae(mm) 30 ― 30 30 ― 30 30 ― 30 44 ― 44 44 ― 44 44 ― 44 Super heat resistant alloys
Q(cm3/min) 8 ― 8 11 ― 11 13 ― 13 13 ― 13 16 ― 16 19 ― 19
n (min-1) 320 ― 320 320 ― 320 320 ― 320 250 ― 250 250 ― 250 250 ― 250
Vc(m/min) 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50
チタン合金 JM4160 V f (mm/min) 380 ― 380 510 ― 510 640 ― 640 400 ― 400 500 ― 500 600 ― 600
fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 チタン合金
Titanium alloys JP4120 ap(mm) 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 Titanium alloys
ae(mm) 30 ― 30 30 ― 30 30 ― 30 44 ― 44 44 ― 44 44 ― 44
Q(cm3/min) 11 ― 11 15 ― 15 19 ― 19 18 ― 18 22 ― 22 26 ― 26
pf
ae
被削材 推奨材種 工具径 DCX (
Tool dia. φ 50(3枚刃) 3 Flutes) φ 50(4枚刃) (4 Flutes) φ 50(5枚刃) (5 Flutes) φ 63(4枚刃) (4 Flutes) φ 63(5枚刃) (5 Flutes) φ 63(6枚刃) (6 Flutes)
被削材
Work material Recommended
inserts grade 突出し量 <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX Work material
Overhang
鋳鉄 n (min-1) 1270 1270 1270 1270 1270 1270 1010 1010 1010 1010 1010 1010
Vc(m/min) 200 200 200 200 200 200 200 200 200 200 200 200 鋳鉄
Cast irons V f (mm/min) 760 760 1020 1020 1270 1270 810 810 1010 1010 1210 1210 Cast irons
FC JP4120 fz(mm/t) 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 FC
FCD pf(mm) ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX
ae(mm) ≦ 9.0 ≦ 9.0 ≦ 9.0 ≦ 9.0 ≦ 9.0 ≦ 9.0 FCD
【Note】① This table provides general guidelines for cutting conditions; in actual machining conditions adjust the parameters according to your actual machine and work-piece conditions.
In particular, when performing shoulder milling in combination with slotting or machining of cutting widths close to slots, etc., chattering vibrations may occur, which can lead
to trouble. Therefore, please consider the following when adjusting the conditions;
・Reduce rotation speed and table feed rate by 50 to 70%
・Reduce cutting depth ap by 50 to 70%
・Reduce cutting width ae by 50 to 70%
② Please note that the GX Coating and JS Coating do not cause a reaction in conductive touch sensors.
③ JP4105 is for the high-hardness steels. It is not suitable for Non-heat-treated steel material.
④ The machinability of hardened steels (50 - 62HRC) can vary significantly depending on the particular steel type and tool overhang. Adjust the table feed rate and cutting depth ap to suit machining conditions.
⑤ For strongly interrupted cutting, when unsupported length is long, or for wet cutting, JM4160 is recommended.
⑥ To prevent tool damage due to chip clogging, always use a chip removal method such as an air blower, etc.
⑦ Since there is a danger of the removed chips flying out and causing injury to workers, fire, or damage to eyes, during use be sure to cover the work area with a safety cover
and have workers wear protective equipment such as glasses, etc. to make the work area safe.
⑧ Perform insert replacement at an early stage to prevent chipping due to excessive use.
⑨ Use of the MOLDINO anti-vibration arbor is recommended for overhang of 5DCX or more.
⑩ The following equation can be used to determine the metal removal rate per unit time Q; Q(cm3/min)=ap(mm)×ae(mm)×vf(mm/min)/1000
11
Page12
標準切削条件表
Recommended Cut t ing Condi t ions
②ボアタイプ は数字、 は英文字が入ります。
Bore type TR4F4000形(TR4F4 B - ) Numeric figure in a circle and Alphabetical character comes in a square .
等高線荒加工標準切削条件 Standard cutting conditions for contour roughing
工具径 DCX
被削材 推奨材種 φ 80(5枚刃) (5 Flutes) φ 80(7枚刃) (7 Flutes) φ100(6枚刃) (6 Flutes) φ100(8枚刃) (8 Flutes) φ160(8枚刃) (8 Flutes) φ200(10枚刃) (10 Flutes)
Tool dia. 被削材
Work material Recommended
inserts grade 突出し量 <3DCX <3DCX <3DCX <3DCX <3DCX <3DCX
汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX Work material
Overhang 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX
General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting
炭素鋼 n (min-1) 600 800 600 600 800 600 480 640 480 480 640 480 300 400 300 240 320 240
Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 炭素鋼
合金鋼
( GX2140 V f (mm/min) 5400 8000 5400 7560 11200 7560 5180 7680 5180 6910 10240 6910 4320 6400 4320 4320 6400 4320 合金鋼
30HRC 以下) fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (30HRC 以下)
Carbon steels JS4160 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Carbon steels
Alloy steels ae(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 Alloy steels
(30HRC or less) Q(cm3/min) 324 480 324 454 672 454 414 614 414 553 819 553 588 870 588 778 1152 778 (30HRC or less)
合金鋼 n (min-1) 600 800 600 600 800 600 480 640 480 480 640 480 300 400 300 240 320 240
Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 合金鋼
(焼入れ焼戻し材)
(35HRC 以下) JS4160 Vf(mm/min) 5400 8000 5400 7560 11200 7560 5180 7680 5180 6910 10240 6910 4320 6400 4320 4320 6400 4320 (焼入れ焼戻し材)
fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (35HRC 以下)
Alloy steels GX2140 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Alloy steels
(Quenched and tempered steels) a
( e(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 (Quenched and tempered steels)
35HRC or less) Q(cm3/min) 324 480 324 454 672 454 414 614 414 553 819 553 588 870 588 778 1152 778 (35HRC or less)
プリハードン鋼・合金鋼 n (min-1) 520 600 520 520 600 520 410 480 410 410 480 410 260 300 260 210 240 210 プリハードン鋼・合金鋼
(焼入れ焼戻し材) Vc(m/min) 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 (焼入れ焼戻し材)
(45HRC以下) V f (mm/min) 4680 6000 4680 6550 8400 6550 4430 5760 4430 5900 7680 5900 3740 4800 3740 3780 4800 3780
Pre-hardened steels JP4120 fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (45HRC以下)
a Pre-hardened steels
Alloy steels p(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
a Alloy steels
(Quenched and tempered steels) e(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 (Quenched and tempered steels)
(45HRC or less) Q(cm3/min) 281 360 281 393 504 393 354 461 354 472 614 472 509 653 509 680 864 680 (45HRC or less)
n (min-1) 320 360 320 320 360 320 250 290 250 250 290 250 160 180 160 130 140 130
焼入れ鋼 Vc(m/min) 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80
Vf(mm/min) 800 1440 800 1120 2020 1120 750 1390 750 1000 1860 1000 640 1150 640 650 1120 650
(55HRC以下) JP4105 焼入れ鋼
fz(mm/t) 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 (55HRC以下)
Hardened steels JP4120 ap(mm) 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 Hardened steels
(55HRC or less) ae(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 (55HRC or less)
Q(cm3/min) 38 69 38 54 97 54 48 89 48 64 119 64 70 125 70 94 161 94
n (min-1) 240 240 240 240 240 240 190 190 190 190 190 190 120 120 120 100 100 100
焼入れ鋼 Vc(m/min) 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60
V f (mm/min) 360 600 360 500 840 500 340 570 340 460 760 460 290 480 290 300 500 300 焼入れ鋼
(62HRC以下) JP4105 fz(mm/t) 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 (62HRC以下)
Hardened steels ap(mm) 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 Hardened steels
(62HRC or less) ae(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 (62HRC or less)
Q(cm3/min) 11 18 11 15 25 15 14 23 14 18 30 18 20 33 20 27 45 27
n (min-1) 400 800 400 400 800 400 320 640 320 320 640 320 200 400 200 160 320 160
Vc(m/min) 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100
ステンレス鋼 JM4160 V f (mm/min) 2000 4000 2000 2800 5600 2800 1920 3840 1920 2560 5120 2560 1600 3200 1600 1600 3200 1600 ステンレス鋼
Stainless steels fz(mm/t) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Stainless steels
SUS JP4120 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
a SUS
e(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180
Q(cm3/min) 120 240 120 168 336 168 154 307 154 205 410 205 218 435 218 288 576 288
n (min-1) 600 800 600 600 800 600 480 640 480 480 640 480 300 400 300 240 320 240
鋳鉄 Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 鋳鉄
Cast irons V f (mm/min) 6000 8000 6000 8400 11200 8400 5760 7680 5760 7680 10240 7680 4800 6400 4800 4800 6400 4800 Cast irons
FC JP4120 fz(mm/t) 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0
ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 FC
FCD ae(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 FCD
Q(cm3/min) 360 480 360 504 672 504 461 614 461 614 819 614 653 870 653 864 1152 864
n (min-1) 140 ― 140 140 ― 140 110 ― 110 110 ― 110 70 ― 70 60 ― 60
耐熱合金 Vc(m/min) 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35
JM4160 V f (mm/min) 280 ― 280 390 ― 390 260 ― 260 350 ― 350 220 ― 220 240 ― 240 耐熱合金
超耐熱合金 fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 超耐熱合金
Heat resistant alloys JP4120 ap(mm) 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 Heat resistant alloys
Super heat resistant alloys ae(mm) 60 ― 60 60 ― 60 80 ― 80 80 ― 80 136 ― 136 180 ― 180 Super heat resistant alloys
Q(cm3/min) 17 ― 17 23 ― 23 21 ― 21 28 ― 28 30 ― 30 43 ― 43
n (min-1) 200 ― 200 200 ― 200 160 ― 160 160 ― 160 100 ― 100 80 ― 80
Vc(m/min) 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50
チタン合金 JM4160 V f (mm/min) 400 ― 400 560 ― 560 380 ― 380 510 ― 510 320 ― 320 320 ― 320
fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 チタン合金
Titanium alloys JP4120 ap(mm) 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 Titanium alloys
ae(mm) 60 ― 60 60 ― 60 80 ― 80 80 ― 80 136 ― 136 180 ― 180
Q(cm3/min) 24 ― 24 34 ― 34 30 ― 30 41 ― 41 44 ― 44 58 ― 58
バーチカル荒加工標準切削条件 Standard cutting conditions for vertical roughing
バーチカル加工には、型番の末尾に「-P」「-LF」が付かないタイプのインサートのご使用を推奨いたします。
For vertical machining, we recommend using inserts without the "-P" or "-LF" suffixes appended to the product code.
被削材 推奨材種 工具径 DCX
Tool dia. φ 80(5枚刃) (5 Flutes) φ 80(7枚刃) (7 Flutes) φ100(6枚刃) (6 Flutes) φ100(8枚刃) (8 Flutes)
被削材
Work material Recommended
inserts grade 突出し量 <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX Work material
Overhang
鋳鉄 n (min-1) 800 800 800 800 640 640 640 640
Vc(m/min) 200 200 200 200 200 200 200 200 鋳鉄
Cast irons V f (mm/min) 800 800 1120 1120 770 770 1020 1020 Cast irons
FC JP4120 fz(mm/t) 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 FC
FCD pf(mm) ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX
ae(mm) ≦ 9.0 ≦ 9.0 ≦ 9.0 ≦ 9.0 FCD
【注意】①本表は切削条件の目安を示すものです。機械剛性やツーリング、加工物の状態に合わせて調整してください。
特に、溝切削を伴う、またはそれに近い切込み幅の加工などで、切りくずの噛み込みやビビり振動が発生し、トラブルに至る場合がありますので下記を参考に調整してください。
・回転数、テーブル送り量を 50~ 70%下げる。
・切込み深さapを 50~ 70%下げる。
・切込み幅 aeを 50~ 70%下げる。
② GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。
③「JP4105」は高硬度鋼専用材種で、生材には適しません。
④焼入れ鋼(50~62HRC) は、鋼種や工具突き出し量によって被削性が大きく異なる場合があります。加工状況に合わせて、テーブル送り量と切込み深さapを調整してください。
⑤強断続切削、突出しが長い場合及び湿式切削には「JM4160」を推奨します。
⑥切りくず噛み込みによる工具損傷防止のため、必ずエアーブロー等による切りくず除去を行ってください。
⑦排出した切りくずは、飛散し作業者を切傷させ、火傷あるいは目に入って負傷させる恐れがありますので、ご使用に際してはその周囲に安全カバーを取付け、保護メガネ等の保
護具を着用し、安全な環境で作業されることをお願い致します。
⑧インサートの交換は早めに行い、過度の使用による破損を防止してください。
⑨突出し量 5DCX 以上の場合は、弊社防振アーバの適用を推奨致します。
12 ⑩右記に単位時間当たりの切りくず排出量Qを示します。 Q(cm3/min)=ap(mm)×ae(mm)×Vf(mm/min)/1000
Page13
※高能率条件は、ご使用の機械の動力・トルク線図をご確認いただき、主軸の定格動力を確保できる回転数での適用を推奨いたします。
・機械動力が不足する場合は、まず切込み深さを下げてください。次いで回転数およびテーブル送り量を下げてご使用ください。
※ To ensure high-efficiency conditions, we recommend checking the machineʼs power/torque chart and using a rotation ae ap
speed that can maintain the rated power of the spindle.
・If the machine lacks sufficient power, first reduce cutting depth, then reduce the rotation speed and table feed rate.
工具径 DCX tes) φ 80(7枚刃) (7 Flutes) φ100(6枚刃) (6 Flutes) φ100(8枚刃) (8 Flutes) φ160(8枚刃) (8 Flutes) φ200(10枚刃) (10 Flutes)
被削材 推奨材種 φ 80(5枚刃) (5 Flu
Tool dia. 被削材
Work material Recommended
inserts grade 突出し量 <3DCX <3DCX <3DCX <3DCX <3DCX <3DCX
DCX-5DCX 3DCX-5DCX Work material
汎用 高速加工 3DCX-5DCX 3 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX 汎用 高速加工 3DCX-5DCX
Overhang 汎用 高速加工 汎用 高速加工
General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting General purpose High-speed Cutting
炭素鋼 n (min-1) 600 800 600 600 800 600 480 640 480 480 640 480 300 400 300 240 320 240
Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 炭素鋼
合金鋼 V f (mm/min) 5400 8000 5400 7560 11200 7560 5180 7680 5180 6910 10240 6910 4320 6400 4320 4320 6400 4320 合金鋼
( GX2140
30HRC 以下) fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (30HRC 以下)
Carbon steels JS4160 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Carbon steels
Alloy steels ae(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 Alloy steels
(30HRC or less) Q(cm3/min) 324 480 324 454 672 454 414 614 414 553 819 553 588 870 588 778 1152 778 (30HRC or less)
合金鋼 n (min-1) 600 800 600 600 800 600 480 640 480 480 640 480 300 400 300 240 320 240
Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 合金鋼
(焼入れ焼戻し材) Vf(mm/min) 5400 8000 5400 7560 11200 7560 5180 7680 5180 6910 10240 6910 4320 6400 4320 4320 6400 4320
(35HRC 以下) JS4160 (焼入れ焼戻し材)
fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (35HRC 以下)
Alloy steels GX2140 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Alloy steels
(Quenched and tempered steels) ae(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 (Quenched and tempered steels)
(35HRC or less) Q(cm3/min) 324 480 324 454 672 454 414 614 414 553 819 553 588 870 588 778 1152 778 (35HRC or less)
プリハードン鋼・合金鋼 n (min-1) 520 600 520 520 600 520 410 480 410 410 480 410 260 300 260 210 240 210 プリハードン鋼・合金鋼
(焼入れ焼戻し材) Vc(m/min) 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 (焼入れ焼戻し材)
(45HRC以下) V f (mm/min) 4680 6000 4680 6550 8400 6550 4430 5760 4430 5900 7680 5900 3740 4800 3740 3780 4800 3780
Pre-hardened steels JP4120 fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (45HRC以下)
a Pre-hardened steels
Alloy steels p(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
a Alloy steels
(Quenched and tempered steels) e(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 (Quenched and tempered steels)
(45HRC or less) Q(cm3/min) 281 360 281 393 504 393 354 461 354 472 614 472 509 653 509 680 864 680 (45HRC or less)
n (min-1) 320 360 320 320 360 320 250 290 250 250 290 250 160 180 160 130 140 130
焼入れ鋼 Vc(m/min) 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80
Vf(mm/min) 800 1440 800 1120 2020 1120 750 1390 750 1000 1860 1000 640 1150 640 650 1120 650 焼入れ鋼
(55HRC以下) JP4105
fz(mm/t) 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 (55HRC以下)
Hardened steels JP4120 ap(mm) 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 0.8 Hardened steels
(55HRC or less) ae(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 (55HRC or less)
Q(cm3/min) 38 69 38 54 97 54 48 89 48 64 119 64 70 125 70 94 161 94
n (min-1) 240 240 240 240 240 240 190 190 190 190 190 190 120 120 120 100 100 100
焼入れ鋼 Vc(m/min) 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60
V f (mm/min) 360 600 360 500 840 500 340 570 340 460 760 460 290 480 290 300 500 300 焼入れ鋼
(62HRC以下) JP4105 fz(mm/t) 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 (62HRC以下)
Hardened steels ap(mm) 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 Hardened steels
(62HRC or less) ae(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 (62HRC or less)
Q(cm3/min) 11 18 11 15 25 15 14 23 14 18 30 18 20 33 20 27 45 27
n (min-1) 400 800 400 400 800 400 320 640 320 320 640 320 200 400 200 160 320 160
Vc(m/min) 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100
ステンレス鋼 JM4160 V f (mm/min) 2000 4000 2000 2800 5600 2800 1920 3840 1920 2560 5120 2560 1600 3200 1600 1600 3200 1600 ステンレス鋼
Stainless steels fz(mm/t) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Stainless steels
SUS JP4120 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0
a SUS
e(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180
Q(cm3/min) 120 240 120 168 336 168 154 307 154 205 410 205 218 435 218 288 576 288
n (min-1) 600 800 600 600 800 600 480 640 480 480 640 480 300 400 300 240 320 240
鋳鉄 Vc(m/min) 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 150 200 150 鋳鉄
Cast irons V f (mm/min) 6000 8000 6000 8400 11200 8400 5760 7680 5760 7680 10240 7680 4800 6400 4800 4800 6400 4800 Cast irons
FC JP4120 fz(mm/t) 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0
ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 FC
FCD ae(mm) 60 60 60 60 60 60 80 80 80 80 80 80 136 136 136 180 180 180 FCD
Q(cm3/min) 360 480 360 504 672 504 461 614 461 614 819 614 653 870 653 864 1152 864
n (min-1) 140 ― 140 140 ― 140 110 ― 110 110 ― 110 70 ― 70 60 ― 60
耐熱合金 Vc(m/min) 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35
超耐熱合金 JM4160 V f (mm/min) 280 ― 280 390 ― 390 260 ― 260 350 ― 350 220 ― 220 240 ― 240 耐熱合金
fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 超耐熱合金
Heat resistant alloys JP4120 ap(mm) 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 Heat resistant alloys
Super heat resistant alloys ae(mm) 60 ― 60 60 ― 60 80 ― 80 80 ― 80 136 ― 136 180 ― 180 Super heat resistant alloys
Q(cm3/min) 17 ― 17 23 ― 23 21 ― 21 28 ― 28 30 ― 30 43 ― 43
n (min-1) 200 ― 200 200 ― 200 160 ― 160 160 ― 160 100 ― 100 80 ― 80
Vc(m/min) 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50
チタン合金 JM4160 V f (mm/min) 400 ― 400 560 ― 560 380 ― 380 510 ― 510 320 ― 320 320 ― 320
fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 チタン合金
Titanium alloys JP4120 ap(mm) 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 1.0 ― 1.0 Titanium alloys
ae(mm) 60 ― 60 60 ― 60 80 ― 80 80 ― 80 136 ― 136 180 ― 180
Q(cm3/min) 24 ― 24 34 ― 34 30 ― 30 41 ― 41 44 ― 44 58 ― 58
pf
ae
工具径 DCX
被削材 推奨材種 Tool dia. φ 80(5枚刃) (5 Flutes) φ 80(7枚刃) (7 Flutes) φ100(6枚刃) (6 Flutes) φ100(8枚刃) (8 Flutes)
被削材
Work material Recommended
inserts grade 突出し量 <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX Work material
Overhang
鋳鉄 n (min-1) 800 800 800 800 640 640 640 640
Vc(m/min) 200 200 200 200 200 200 200 200 鋳鉄
Cast irons V f (mm/min) 800 800 1120 1120 770 770 1020 1020 Cast irons
FC JP4120 fz(mm/t) 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 FC
FCD pf(mm) ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX
ae(mm) ≦ 9.0 ≦ 9.0 ≦ 9.0 ≦ 9.0 FCD
【Note】① This table provides general guidelines for cutting conditions; in actual machining conditions adjust the parameters according to your actual machine and work-piece conditions.
In particular, when performing shoulder milling in combination with slotting or machining of cutting widths close to slots, etc., chattering vibrations may occur, which can lead
to trouble. Therefore, please consider the following when adjusting the conditions;
・Reduce rotation speed and table feed rate by 50 to 70%
・Reduce cutting depth ap by 50 to 70%
・Reduce cutting width ae by 50 to 70%
② Please note that the GX Coating and JS Coating do not cause a reaction in conductive touch sensors.
③ JP4105 is for the high-hardness steels. It is not suitable for Non-heat-treated steel material.
④ The machinability of hardened steels (50 - 62HRC) can vary significantly depending on the particular steel type and tool overhang. Adjust the table feed rate and cutting depth ap to suit machining conditions.
⑤ For strongly interrupted cutting, when unsupported length is long, or for wet cutting, JM4160 is recommended.
⑥ To prevent tool damage due to chip clogging, always use a chip removal method such as an air blower, etc.
⑦ Since there is a danger of the removed chips flying out and causing injury to workers, fire, or damage to eyes, during use be sure to cover the work area with a safety cover
and have workers wear protective equipment such as glasses, etc. to make the work area safe.
⑧ Perform insert replacement at an early stage to prevent chipping due to excessive use.
⑨ Use of the MOLDINO anti-vibration arbor is recommended for overhang of 5DCX or more.
⑩ The following equation can be used to determine the metal removal rate per unit time Q; Q(cm3/min)=ap(mm)×ae(mm)×vf(mm/min)/1000
13
Page14
標準切削条件表
Recommended Cut t ing Condi t ions
②ボアタイプ は数字、 は英文字が入ります。
Bore type TR4F5000形(TR4F5 B - ) Numeric figure in a circle and Alphabetical character comes in a square .
等高線荒加工標準切削条件 Standard cutting conditions for contour roughing
工具径 DCX φ 63(4枚刃) (4 Flutes) φ 80(5枚刃) (5 Flutes) φ100(6枚刃) (6 Flutes) φ125(6枚刃) (6 Flutes) φ125(7枚刃) (7 Flutes) φ160(8枚刃) (8 Flutes) φ200(10枚刃) (10 Flutes)
被削材 推奨材種 Tool dia.
CX <3DCX <3DCX <3DCX <3DCX 被削材
Work material Recommended
inserts grade 突出し量 <3DCX <3DCX <3D
汎用 高能率 3DCX-5DCX 汎用 高能率 3DCX-5DCX 汎用 高能率 3DCX-5DCX 汎用 高能率 3DCX-5DCX 汎用 高能率 3DCX-5DCX 汎用 高能率 3DCX-5DCX 汎用 高能率 3DCX-5DCX Work material
Overhang
General purpose High efficiency General purpose High efficiency General purpose High efficiency General purpose High efficiency General purpose High efficiency General purpose High efficiency General purpose High efficiency
炭素鋼 n (min-1) 760 910 760 600 720 600 480 570 480 380 460 380 380 460 380 300 360 300 240 290 240
Vc(m/min) 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 炭素鋼
合金鋼 X2140 V f (mm/min) 4560 7280 5470 4500 7200 5400 4320 6840 5180 3420 5520 4100 3990 6440 4790 3600 5760 4320 3600 5800 4320 合金鋼
(30HRC 以下) G
fz(mm/t) 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 (30HRC 以下)
Carbon steels JS4160 ap(mm) 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 Carbon steels
Alloy steels ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 Alloy steels
(30HRC or less) Q(cm3/min) 347 553 208 504 806 302 648 1026 389 684 1104 410 798 1288 479 979 1567 588 1224 1972 734 (30HRC or less)
合金鋼 n (min-1) 760 910 760 600 720 600 480 570 480 380 460 380 380 460 380 300 360 300 240 290 240
Vc(m/min) 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 合金鋼
(焼入れ焼戻し材)
(35HRC 以下) JS4160 Vf(mm/min) 4560 7280 5470 4500 7200 5400 4320 6840 5180 3420 5520 4100 3990 6440 4790 3600 5760 4320 3600 5800 4320 (焼入れ焼戻し材)
fz(mm/t) 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 (35HRC 以下)
Alloy steels GX2140 ap(mm) 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 Alloy steels
(Quenched and tempered steels) ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 (Quenched and tempered steels)
(35HRC or less) Q(cm3/min) 347 553 208 504 806 302 648 1026 389 684 1104 410 798 1288 479 979 1567 588 1224 1972 734 (35HRC or less)
プリハードン鋼・合金鋼 n (min-1) 660 760 660 520 600 520 410 480 410 330 380 330 330 380 330 260 300 260 210 240 210 プリハードン鋼・合金鋼
(焼入れ焼戻し材) Vc(m/min) 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 (焼入れ焼戻し材)
(45HRC以下) V f (mm/min) 4750 6080 4750 4680 6000 4680 4430 5760 4430 3560 4560 3560 4160 5320 4160 3740 4800 3740 3780 4800 3780
fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (45HRC以下)
Pre-hardened steels JP4120
a Pre-hardened steels
Alloy steels p(mm) 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0
a Alloy steels
(Quenched and tempered steels) e(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 (Quenched and tempered steels)
(45HRC or less) Q(cm3/min) 271 347 181 393 504 262 498 648 332 534 684 356 624 798 416 763 979 509 964 1224 643 (45HRC or less)
n (min-1) 400 450 400 320 360 320 250 290 250 200 230 200 200 230 200 160 180 160 130 140 130
焼入れ鋼 Vc(m/min) 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80
Vf(mm/min) 800 1440 800 800 1440 800 750 1390 750 600 1100 600 700 1290 700 640 1150 640 650 1120 650
(55HRC以下) JP4105 焼入れ鋼
fz(mm/t) 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 (55HRC以下)
Hardened steels JP4120 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Hardened steels
(55HRC or less) ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 (55HRC or less)
Q(cm3/min) 30 55 30 45 81 45 56 104 56 60 110 60 70 129 70 87 156 87 111 190 111
n (min-1) 300 300 300 240 240 240 190 190 190 150 150 150 150 150 150 120 120 120 100 100 100
焼入れ鋼 Vc(m/min) 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60
V f (mm/min) 360 600 360 360 600 360 340 570 340 270 450 270 320 530 320 290 480 290 300 500 300 焼入れ鋼
(62HRC以下) JP4105 fz(mm/t) 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 (62HRC以下)
Hardened steels ap(mm) 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 Hardened steels
(62HRC or less) ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 (62HRC or less)
Q(cm3/min) 7 11 7 10 17 10 13 21 13 14 23 14 16 27 16 20 33 20 26 43 26
n (min-1) 510 1010 510 400 800 400 320 640 320 250 510 250 250 510 250 200 400 200 160 320 160
Vc(m/min) 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100
ステンレス鋼 JM4160 V f (mm/min) 2040 4040 2040 2000 4000 2000 1920 3840 1920 1500 3060 1500 1750 3570 1750 1600 3200 1600 1600 3200 1600 ステンレス鋼
Stainless steels fz(mm/t) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Stainless steels
SUS JP4120 ap(mm) 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0
a SUS
e(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170
Q(cm3/min) 116 230 78 168 336 112 216 432 144 225 459 150 263 536 175 326 653 218 408 816 272
n (min-1) 760 910 760 600 720 600 480 570 480 380 460 380 380 460 380 300 360 300 240 290 240
鋳鉄 Vc(m/min) 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 鋳鉄
Cast irons V f (mm/min) 6080 8370 6080 6000 8280 6000 5760 7870 5760 4560 6350 4560 5320 7410 5320 4800 6620 4800 4800 6670 4800 Cast irons
FC JP4120 fz(mm/t) 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0
ap(mm) 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 FC
FCD ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 FCD
Q(cm3/min) 462 636 462 672 927 672 864 1181 864 912 1270 912 1064 1482 1064 1306 1801 1306 1632 2268 1632
n (min-1) 180 ― 180 140 ― 140 110 ― 110 90 ― 90 90 ― 90 70 ― 70 60 ― 60
耐熱合金 Vc(m/min) 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35
V f (mm/min) 290 ― 290 280 ― 280 260 ― 260 220 ― 220 250 ― 250 220 ― 220 240 ― 240 耐熱合金
超耐熱合金 JM4160
fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 超耐熱合金
Heat resistant alloys JP4120 ap(mm) 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 Heat resistant alloys
Super heat resistant alloys ae(mm) 38 ― 38 56 ― 56 75 ― 75 100 ― 100 100 ― 100 136 ― 136 170 ― 170 Super heat resistant alloys
Q(cm3/min) 17 ― 11 24 ― 16 29 ― 20 33 ― 22 38 ― 25 45 ― 30 61 ― 41
n (min-1) 250 ― 250 200 ― 200 160 ― 160 130 ― 130 130 ― 130 100 ― 100 80 ― 80
Vc(m/min) 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50
チタン合金 JM4160 V f (mm/min) 400 ― 400 400 ― 400 380 ― 380 310 ― 310 360 ― 360 320 ― 320 320 ― 320
fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 チタン合金
Titanium alloys JP4120 ap(mm) 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 Titanium alloys
ae(mm) 38 ― 38 56 ― 56 75 ― 75 100 ― 100 100 ― 100 136 ― 136 170 ― 170
Q(cm3/min) 23 ― 15 34 ― 22 43 ― 29 47 ― 31 54 ― 36 65 ― 44 82 ― 54
バーチカル荒加工標準切削条件 Standard cutting conditions for vertical roughing
バーチカル加工には、型番の末尾に「-P」「-LF」が付かないタイプのインサートのご使用を推奨いたします。
For vertical machining, we recommend using inserts without the "-P" or "-LF" suffixes appended to the product code.
工具径 DCX
被削材 推奨材種 Tool dia. φ 63(4枚刃) (4 Flutes) φ 80(5枚刃) (5 Flutes) φ100(6枚刃) (6 Flutes) φ125(6枚刃) (6 Flutes) φ125(7枚刃) (7 Flutes)
被削材
Work material Recommended
inserts grade 突出し量 <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX Work material
Overhang
10 1010 800 800 640 640 510 510 510 510
鋳鉄 n (min-1) 10
Vc(m/min) 200 200 200 200 200 200 200 200 200 200 鋳鉄
Cast irons V f (mm/min) 810 810 800 800 770 770 610 610 710 710 Cast irons
FC JP4120 fz(mm/t) 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 FC
FCD pf(mm) ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX
ae(mm) ≦ 11.0 ≦ 11.0 ≦ 11.0 ≦ 11.0 ≦ 11.0 FCD
【注意】①本表は切削条件の目安を示すものです。機械剛性やツーリング、加工物の状態に合わせて調整してください。
特に、溝切削を伴う、またはそれに近い切込み幅の加工などで、切りくずの噛み込みやビビり振動が発生し、トラブルに至る場合がありますので下記を参考に調整してください。
・回転数、テーブル送り量を 50~ 70%下げる。 ・切込み深さapを 50~ 70%下げる。 ・切込み幅 aeを 50~ 70%下げる。
②機械動力が不足する場合は、まず切込み深さを下げてください。次いで回転数およびテーブル送り量を下げてご使用ください。
③ GXコーティング、JSコーティングは通電式タッチセンサーに反応しませんのでご注意ください。
④「JP4105」は高硬度鋼専用材種で、生材には適しません。
⑤焼入れ鋼(50~62HRC) は、鋼種や工具突き出し量によって被削性が大きく異なる場合があります。加工状況に合わせて、テーブル送り量と切込み深さapを調整してください。
⑥強断続切削、突出しが長い場合及び湿式切削には「JM4160」を推奨します。
⑦切りくず噛み込みによる工具損傷防止のため、必ずエアーブロー等による切りくず除去を行ってください。
⑧排出した切りくずは、飛散し作業者を切傷させ、火傷あるいは目に入って負傷させる恐れがありますので、ご使用に際してはその周囲に安全カバーを取付け、保護メガネ等の保
護具を着用し、安全な環境で作業されることをお願い致します。
⑨インサートの交換は早めに行い、過度の使用による破損を防止してください。
⑩突出し量 5DCX 以上の場合は、弊社防振アーバの適用を推奨致します。
⑪右記に単位時間当たりの切りくず排出量Qを示します。 Q(cm3/min)=ap(mm)×ae(mm)×Vf(mm/min)/1000
14
Page15
※高能率条件は、ご使用の機械の動力・トルク線図をご確認いただき、主軸の定格動力を確保できる回転数での適用を推奨いたします。
・機械動力が不足する場合は、まず切込み深さを下げてください。次いで回転数およびテーブル送り量を下げてご使用ください。
※ To ensure high-efficiency conditions, we recommend checking the machineʼs power/torque chart and using a rotation ae ap
speed that can maintain the rated power of the spindle.
・If the machine lacks sufficient power, first reduce cutting depth, then reduce the rotation speed and table feed rate.
工具径 DCX φ 63(4枚刃) (4 Flutes) φ 80(5枚刃) (5 Flutes) φ100(6枚刃) (6 Flutes) φ125(6枚刃) (6 Flutes) φ125(7枚刃) (7 Flutes) φ160(8枚刃) (8 Flutes) φ200(10枚刃) (10 Flutes)
被削材 推奨材種 Tool dia. 被削材
Work material Recommended
inserts grade 突出し量 <3DCX <3DCX <3DCX <3DCX <3DCX <3DCX <3DCX
汎用 高能率 3DCX-5DCX 汎用 高能率 3DCX-5DCX 汎用 高能率 3DCX-5DCX Work material
汎用 高能率 3DCX-5DCX 汎用 高能率 3DCX-5DCX 3DCX-5DCX 3DCX-5DCX
Overhang 汎用 高能率 汎用 高能率
General purpose High efficiency General purpose High efficiency General purpose High efficiency General purpose High efficiency General purpose High efficiency General purpose High efficiency General purpose High efficiency
炭素鋼 n (min-1) 760 910 760 600 720 600 480 570 480 380 460 380 380 460 380 300 360 300 240 290 240
Vc(m/min) 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 炭素鋼
合金鋼
( GX2140 V f (mm/min) 4560 7280 5470 4500 7200 5400 4320 6840 5180 3420 5520 4100 3990 6440 4790 3600 5760 4320 3600 5800 4320 合金鋼
30HRC 以下) fz(mm/t) 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 (30HRC 以下)
Carbon steels JS4160 ap(mm) 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 Carbon steels
Alloy steels ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 Alloy steels
(30HRC or less) Q(cm3/min) 347 553 208 504 806 302 648 1026 389 684 1104 410 798 1288 479 979 1567 588 1224 1972 734 (30HRC or less)
合金鋼 n (min-1) 760 910 760 600 720 600 480 570 480 380 460 380 380 460 380 300 360 300 240 290 240
Vc(m/min) 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 合金鋼
(焼入れ焼戻し材) Vf(mm/min) 4560 7280 5470 4500 7200 5400 4320 6840 5180 3420 5520 4100 3990 6440 4790 3600 5760 4320 3600 5800 4320
(35HRC 以下) JS4160 (焼入れ焼戻し材)
fz(mm/t) 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 1.5 2.0 1.8 (35HRC 以下)
Alloy steels GX2140 ap(mm) 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 2.0 2.0 1.0 Alloy steels
(Quenched and tempered steels) ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 (Quenched and tempered steels)
(35HRC or less) Q(cm3/min) 347 553 208 504 806 302 648 1026 389 684 1104 410 798 1288 479 979 1567 588 1224 1972 734 (35HRC or less)
プリハードン鋼・合金鋼 n (min-1) 660 760 660 520 600 520 410 480 410 330 380 330 330 380 330 260 300 260 210 240 210 プリハードン鋼・合金鋼
(焼入れ焼戻し材) Vc(m/min) 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 130 150 130 (焼入れ焼戻し材)
(45HRC以下) V f (mm/min) 4750 6080 4750 4680 6000 4680 4430 5760 4430 3560 4560 3560 4160 5320 4160 3740 4800 3740 3780 4800 3780
Pre-hardened steels JP4120 fz(mm/t) 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 1.8 2.0 1.8 (45HRC以下)
a Pre-hardened steels
Alloy steels p(mm) 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0
a Alloy steels
(Quenched and tempered steels) e(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 (Quenched and tempered steels)
(45HRC or less) Q(cm3/min) 271 347 181 393 504 262 498 648 332 534 684 356 624 798 416 763 979 509 964 1224 643 (45HRC or less)
n (min-1) 400 450 400 320 360 320 250 290 250 200 230 200 200 230 200 160 180 160 130 140 130
焼入れ鋼 Vc(m/min) 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80 80 90 80
JP4105 Vf(mm/min) 800 1440 800 800 1440 800 750 1390 750 600 1100 600 700 1290 700 640 1150 640 650 1120 650 焼入れ鋼
(55HRC以下) fz(mm/t) 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 0.5 0.8 0.5 (55HRC以下)
Hardened steels JP4120 ap(mm) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Hardened steels
(55HRC or less) ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 (55HRC or less)
Q(cm3/min) 30 55 30 45 81 45 56 104 56 60 110 60 70 129 70 87 156 87 111 190 111
n (min-1) 300 300 300 240 240 240 190 190 190 150 150 150 150 150 150 120 120 120 100 100 100
焼入れ鋼 Vc(m/min) 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60 60
V f (mm/min) 360 600 360 360 600 360 340 570 340 270 450 270 320 530 320 290 480 290 300 500 300 焼入れ鋼
(62HRC以下) JP4105 fz(mm/t) 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 0.3 0.5 0.3 (62HRC以下)
Hardened steels ap(mm) 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 0.5 Hardened steels
(62HRC or less) ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 (62HRC or less)
Q(cm3/min) 7 11 7 10 17 10 13 21 13 14 23 14 16 27 16 20 33 20 26 43 26
n (min-1) 510 1010 510 400 800 400 320 640 320 250 510 250 250 510 250 200 400 200 160 320 160
Vc(m/min) 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100 100 200 100
ステンレス鋼 JM4160 V f (mm/min) 2040 4040 2040 2000 4000 2000 1920 3840 1920 1500 3060 1500 1750 3570 1750 1600 3200 1600 1600 3200 1600 ステンレス鋼
Stainless steels fz(mm/t) 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 1.0 Stainless steels
SUS JP4120 ap(mm) 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0 1.5 1.5 1.0
a SUS
e(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170
Q(cm3/min) 116 230 78 168 336 112 216 432 144 225 459 150 263 536 175 326 653 218 408 816 272
n (min-1) 760 910 760 600 720 600 480 570 480 380 460 380 380 460 380 300 360 300 240 290 240
鋳鉄 Vc(m/min) 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 150 180 150 鋳鉄
Cast irons V f (mm/min) 6080 8370 6080 6000 8280 6000 5760 7870 5760 4560 6350 4560 5320 7410 5320 4800 6620 4800 4800 6670 4800 Cast irons
FC JP4120 fz(mm/t) 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0 2.0 2.3 2.0
ap(mm) 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 2.0 FC
FCD ae(mm) 38 38 38 56 56 56 75 75 75 100 100 100 100 100 100 136 136 136 170 170 170 FCD
Q(cm3/min) 462 636 462 672 927 672 864 1181 864 912 1270 912 1064 1482 1064 1306 1801 1306 1632 2268 1632
n (min-1) 180 ― 180 140 ― 140 110 ― 110 90 ― 90 90 ― 90 70 ― 70 60 ― 60
耐熱合金 Vc(m/min) 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35 35 ― 35
JM4160 V f (mm/min) 290 ― 290 280 ― 280 260 ― 260 220 ― 220 250 ― 250 220 ― 220 240 ― 240 耐熱合金
超耐熱合金 fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 超耐熱合金
Heat resistant alloys JP4120 ap(mm) 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 Heat resistant alloys
Super heat resistant alloys ae(mm) 38 ― 38 56 ― 56 75 ― 75 100 ― 100 100 ― 100 136 ― 136 170 ― 170 Super heat resistant alloys
Q(cm3/min) 17 ― 11 24 ― 16 29 ― 20 33 ― 22 38 ― 25 45 ― 30 61 ― 41
n (min-1) 250 ― 250 200 ― 200 160 ― 160 130 ― 130 130 ― 130 100 ― 100 80 ― 80
Vc(m/min) 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50 50 ― 50
チタン合金 JM4160 V f (mm/min) 400 ― 400 400 ― 400 380 ― 380 310 ― 310 360 ― 360 320 ― 320 320 ― 320
fz(mm/t) 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 0.4 ― 0.4 チタン合金
Titanium alloys JP4120 ap(mm) 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 1.5 ― 1.0 Titanium alloys
ae(mm) 38 ― 38 56 ― 56 75 ― 75 100 ― 100 100 ― 100 136 ― 136 170 ― 170
Q(cm3/min) 23 ― 15 34 ― 22 43 ― 29 47 ― 31 54 ― 36 65 ― 44 82 ― 54
pf
ae
被削材 推奨材種 工具径 DCX
Tool dia. φ 63(4枚刃) (4 Flutes) φ 80(5枚刃) (5 Flutes) φ100(6枚刃) (6 Flutes) φ125(6枚刃) (6 Flutes) φ125(7枚刃) (7 Flutes)
被削材
Work material Recommended
inserts grade 突出し量 <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX <3DCX 3DCX-5DCX Work material
Overhang
鋳鉄 n (min-1) 1010 1010 800 800 640 640 510 510 510 510
Vc(m/min) 200 200 200 200 200 200 200 200 200 200 鋳鉄
Cast irons V f (mm/min) 810 810 800 800 770 770 610 610 710 710 Cast irons
FC JP4120 fz(mm/t) 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 0.2 FC
FCD pf(mm) ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX ≦ 0.5DCX
ae(mm) ≦ 11.0 ≦ 11.0 ≦ 11.0 ≦ 11.0 ≦ 11.0 FCD
【Note】① This table provides general guidelines for cutting conditions; in actual machining conditions adjust the parameters according to your actual machine and work-piece conditions.
In particular, when performing shoulder milling in combination with slotting or machining of cutting widths close to slots, etc., chattering vibrations may occur, which can lead
to trouble. Therefore, please consider the following when adjusting the conditions;
・Reduce rotation speed and table feed rate by 50 to 70% ・Reduce cutting depth ap by 50 to 70% ・Reduce cutting width ae by 50 to 70%
② If the machine has insufficient power, first try reducing the cutting depth. Next, try reducing the rotation speed and table feed rate.
③ Please note that the GX Coating and JS Coating do not cause a reaction in conductive touch sensors.
④ JP4105 is for the high-hardness steels. It is not suitable for Non-heat-treated steel material.
⑤ The machinability of hardened steels (50 - 62HRC) can vary significantly depending on the particular steel type and tool overhang. Adjust the table feed rate and cutting depth ap to suit machining conditions.
⑥ For strongly interrupted cutting, when unsupported length is long, or for wet cutting, JM4160 is recommended.
⑦ To prevent tool damage due to chip clogging, always use a chip removal method such as an air blower, etc.
⑧ Since there is a danger of the removed chips flying out and causing injury to workers, fire, or damage to eyes, during use be sure to cover the work area with a safety cover
and have workers wear protective equipment such as glasses, etc. to make the work area safe.
⑨ Perform insert replacement at an early stage to prevent chipping due to excessive use.
⑩ Use of the MOLDINO anti-vibration arbor is recommended for overhang of 5DCX or more.
⑪ The following equation can be used to determine the metal removal rate per unit time Q; Q(cm3/min)=ap(mm)×ae(mm)×vf(mm/min)/1000
15
Page16
工具使用上の注意点
Precaut ions for use
プログラミング Rと最大切込み深さ Programming R and maximum cutting depth
● 下記の表を参考に、CAM上の工具形状を定義してください。
・ Please define the tool shape in the CAM as indicated in the following table:
使用インサート プログラミング R 削り残し量(mm) 最大切込み深さ(mm)
Insert Programming R Remains Maximum
cutting depth
SDNW120520TR(-P)
SDMT120520TR R3.0 1.0 1.2
SDMT120520ER-LF 8.8 11.6
SDNW150525ZTR R3.0 1.47
SDMT150525ZTR 2.0 SDNW120520TR(-P) SDNW150525ZTR
SDMT150525ZER-LF R4.0 1.32 SDM T 120520TR SDM T 150525ZTR
SDM T 120520ER-LF SDM T 150525ZER-LF
最大傾斜角とヘリカル穴径 Maximum ramp angle and helical hole diameter
● 中心まで切れ刃がないため傾斜角度と穴径は制限されますが、下図に示すように傾斜切削やヘリカル切削にて、
下穴がなくてもダイレクトに彫り込み加工が可能です。
・ Since the cutting flute do not extend to the center, there are limitations on the ramp angle and hole diameter, but as shown below, cutting
by direct milling without a pilot hole is possible for ramping and helical milling.
ヘリカル穴径 Helical hole diameter.
傾斜角θ 傾斜切削 ヘリカル切削
Ramp angleθ Ramping Helical milling
● 傾斜切削・ヘリカル切削の場合、テーブル送り量は標準切削条件の 50%程度としてください。
・ For ramping and helical cutting, please set the “V f” to around 50% of recommended cutting condition.
モジュラー / シャンクタイプ
使用インサート Inserts Modular/Shank Type ボアタイプ Bore Type
SDNW120520TR(-P) 、SDMT120520TR、SDMT120520ER-LF
工具径(DCX) Tool dia(. mm) φ32 φ40 φ50 φ63 φ80 φ100 φ160 φ200
傾斜切削 推奨設定値
Ramping Recommendation 1° 0.2° 0.1°
ヘリカル穴径
ヘリカル切削 Helical hole diameter 46 〜60 62 〜76 82 〜96 108 〜 122 142 〜 156 182 〜 196 302 〜 316 382 〜 396
Helical milling ヘリカルピッチ
Helical pitch 1mm 以下 1 mm or less
ボアタイプ Bore Type
使用インサート Inserts
SDNW150525ZTR、SDMT150525ZTR、SDMT150525ZER-LF
工具径(DCX) Tool dia(. mm) φ63 φ80 φ100 φ125 φ160 φ200
傾斜切削 推奨設定値
Ramping Recommendation 2° 1° 0.5° 0.2° 0.1°
ヘリカル穴径
ヘリカル切削 Helical hole diameter 102 〜 121 136 〜 155 176 〜 195 226 〜 245 296 〜 315 376 〜 395
Helical milling ヘリカルピッチ
Helical pitch 1mm 以下 1 mm or less
【注意】 ①傾斜角θは上記範囲を超えないように設定して下さい。推奨設定値以下での使用を推奨いたします。
②穴径が上記範囲以外の場合は下穴を開けて加工して下さい。
③エアーブロー (センタースルー )による、切りくず除去を十分行い、異常な振動が無いことを確認の上、加工することをお勧めいたします。
【Note】 ① The ramp angle θ should be set within the ranges listed above. Do not exceed the recommended value.
② For hole diameters outside the ranges listed above, a pilot hole should be drilled before milling.
③ It is recommended that the tool be used while performing sufficient chip removal and checking that there are no abnormal vibrations.
コーナチェンジ時のお願い Attention for the corner change
● コーナチェンジを行う際には、インサートを反時計回りに回転させてください。
・ Turn the insert counterclockwise upon corner change.
16
削り残し量
Remains
プロ
グラ
ミン
グR
Pro
gra
mm
ing
R
削り残し量
Remains
プロ
グラ
ミン
グR
Prog
ram
im
ing
R
Page17
切削性能
Cutt ing performance
プリハードン鋼(40HRC)での寿命曲線 Tool life curve with pre-hardened steels (40 HRC)
切削条件 Cutting conditions
0.4
被 削 材 プリハードン鋼 (40HRC) Pre-hardened steels(40HRC)
従来品Y Work material
Conventional tool Y 工 具 型 番 TR4F4063BM-5
0.3 Tool
従来品G インサート型番 SDNW120520TR-P:JP4120
Insert model
Conventional tool G 切 削 速 度 vc = 140m/min
0.2 Cutting speed
SDNW120520TR-P 1刃当りの送り量 fz = 2.0mm/t
Feed per tooth
JP4120 切 込 み 量 ap×ae = 1.0×45mm
0.1 Cutting depth
突 出 し 量 200mm
継続可能 Overhang
Still usable エアーブロー、 単一刃切削0 Air-blow Single flute cutting
0 5 10 15 20
切削時間 (min)
Cutting time
fz = 2.0mm/t の高送り加工において従来品を超える長寿命
Surpasses life of conventional tools for high-feed cutting at fz=2.0mm/t.
焼入れ焼戻し鋼(52HRC)での寿命曲線 Tool life curve with quench-tempered steels (52 HRC)
切削条件 Cutting conditions
0.4
被 削 材 焼入れ焼戻し鋼 (52HRC)
SDNW120520TR Work material Quench-tempered steels (52 HRC)
※SUS420J2相当材 *Equivalent to SUS420J2
0.3 (JP4105)
工 具 型 番 TR4F4063BM-5
Tool
従来品G インサート型番 SDNW120520TR:JP4105
0.2 Insert model
Conventional tool G 切 削 速 度 vc = 90m/min
Cutting speed
1刃当りの送り量 fz = 1.0mm/t
0.1 Feed per tooth
切 込 み 量 ap×ae = 1.0×35mm
Cutting depth
突 出 し 量 200mm
0 Overhang
0 5 10 15 20
切削時間 エアーブロー、 単一刃切削
(min) Air-blow Single flute cutting
Cutting time
高硬度材の高能率加工において従来品を超える長寿命
Surpasses life of conventional tools for more efficient cutting of high-hardness materials
切削抵抗比較 Comparison of cutting force
切削条件 Cutting conditions
被 削 材 S50C(220HB)
Work material
工 具 型 番 TR4F4063B-6(φ63-6枚刃 6 flutes)
Tool
SDNW120520TR 切 削 速 度 vc = 150m/min
Cutting speed
1刃当りの送り量 fz = 1.0mm/t
Feed per tooth
切 込 み 量 ap×ae = 1.0×38mm
Cutting depth
SDMT120520TR Dry、フルセット
(ブレーカ付)(with breaker) Dry, with full set
(主軸負荷ー12%※SDNW比)
Spindle load -12% compared to SDNW
SDMT120520ER-LF 3,000 3,500 4,000 4,500 5,000
(LFブレーカ)(LF breaker)
切削抵抗( N)
Cutting force
(最大合力)
(Maximum resultant force)
17
逃げ面最大摩耗幅 VBmax (mm) 逃げ面最大摩耗幅 VBmax (mm)
Flank wear Flank wear
Page18
切削性能
Cutt ing performance
実績は語る Field data
切削条件 Cutting conditions
被 削 材 鋳鋼 Cast steels
Work material
工 具 型 番 TR4F4100BM-6
Tool model
インサート型番 SDMT120520ER-LF:JS4160
Insert model
切 削 速 度 vc = 207m/min
Cutting speed
1刃当りの送り量 fz = 1.5mm/t
Feed per tooth
切 込 み 量 ap×ae = 0.6~ 1.0×80~ 100mm
Cutting depth
従来品に対し加工音が静かで良好 突 出 し 量 450mm(L/D=4.5)
長い突き出し量でもビビり振動抑え能率2倍達成 Overhang
ク ー ラ ン ト Dry
Features lower machining noise levels compared to conventional products. Coolant
Minimizes chatter and vibration even with long overhangs to double efficiency.
従来品 Conventional LFブレーカ LF breaker 切削条件 Cutting conditions
被 削 材 Ti合金 Titanium alloys( 33HRC)
Work material
工 具 型 番 TR4F4050B-5
Tool model
インサート型番 SDMT120520ER-LF:JM4160
Insert model
5.0mm 切 削 速 度 vc = 64m/min
Cutting speed
従来品に対し主軸負荷を低減 1刃当りの送り量 fz = 0.89mm/t
Feed per tooth
サイズが小さい良好な切りくず形態かつ能率2倍、寿命3倍達成 切 込 み 量 ap×ae = 0.8×30mm
Cutting depth
Reduces spindle load compared to conventional products. ク ー ラ ン ト Wet(水溶性 Water base)
Produces smaller, well-formed chips. Coolant
Doubles based on the original efficiency and increases tool life threefold.
サポータタイプ加工事例 Machining example using locater type 切削条件 Cutting conditions
被 削 材 SS400
Work material
工 具 型 番 TR4F5250B-12(受注生産品 Order production)
Tool model
インサート型番 SDNW150525ZTR(JP4120)
Insert model
切 削 速 度 vc = 150m/min
Cutting speed
1刃当りの送り量 fz = 1.54mm/t
Feed per tooth
切 込 み 量 ap×ae = 1.5×170mm
Cutting depth
0.5mm 加 工 時 間 128min
Cutting time
最大逃げ面摩耗幅 Flank wear 0.184mm ク ー ラ ン ト Dry
Coolant
128min加工後も継続切削可能
TR4Fの高能率加工を大径でも実現
Machining can be continued even after 128 minutes
Allows large-diameter tools to achieve the typical high-efficiency machining with the TR4F.
PVD Technology 鋼一般加工用材種
General purpose for steel JS4160
特長 Features 図 切削性能 Cutting performance
● 耐熱性、耐溶着性に優れたコーティング膜の採用により 1,000
切削条件 Cutting Conditions
高能率加工で発生するクレータ摩耗を低減します。 被 削 材 SKD11(240HB)
● 靭性と耐熱性のバランスに優れた超硬母材の採用により Work Material
従来品 使用工具 ASRS2032R-5
高能率加工において安定した長寿命を発揮します。 Conventional Tool
JS4160 インサート EPNW0603TN-8
・Features a coating with outstanding heat and welding resistance, reducing Inserts
crater wear that occurs during high-efficiency cutting. 100 切 削 速 度 vc = 80,130,180m/min
Cutting Speed
・Features a carbide base metal that combines toughness with heat 1刃当りの送り量 fz = 1.3mm/t
resistance to ensure consistent long tool life and high efficiency in cutting. Feed per tooth
切り込 み ap×ae = 0.5 × 21mm
Cutting depth
得意分野 Strong fields 切 削 油 剤 乾式加工 単一刃切削
Coolant Dry cutting Single-flute cutting
● SS材、SC材、SCM材など35HRC未満の不安定~ 10
10 100 1,000
高能率加工および湿式加工 工具寿命T Tool life (min)
・From unstable to high-efficiency cutting, and wet cutting of materials like SS,
SC, SCM measuring less than 35 HRC in hardness.
18
切削速度 Cutting speed Vc (m/min)
Page19
当社高送り工具のラインナップ High-feed tools lineup
特長 ホルダ インサート
Feature Holder Insert
プログラ
型式 経済性 高精度 高硬度 能率 ミング R APMX
Type (コーナ数) (削り残し小) 対応 (刃数) 工具径 接円記号 Programming R (mm)
Tool dia. コーナ数 形状 内
conomical High accuracy Supports for high- Efficiency (mm)
(mm) No. of corners Shape Inscribed
E circle code
(No. of corners) (Less uncut remnants) hardened steel (No. of Flutes)
06 0.5
◎
TR2F ○ ○ 高能率多刃
〜62HRC φ16〜52 2 2.0
High Efficiency
multiflutes
06 1.0
○ ◎
TD4N ◎ ◎ 高能率多刃
〜62HRC φ16〜50 4 06 2.0 1.0
High Efficiency
multiflutes
◎
ASR 多刃 06 2.0 1.5
○ ○ 高能率多刃 66 2
Multi-Flutes 〜62HRC φ16〜
High Efficiency
multiflutes 12 3.0 2.0
○
ASRF mini ◎ ○
〜62HRC 汎用 φ20〜63 4 07 2.0 1.2
General
○
ASR ○ ○
〜62HRC 汎用 φ20〜100 2 08〜15
General
3.0
○
ASRT ○ ○ ○
〜62HRC 汎用 φ25〜100 3 09〜14 2.0
General
ASRF ◎ ○ ○
〜62HRC 汎用 φ32〜100 4 12 4.5
General
14 1.5
○
TD6N ○ 〜55HRC 汎用 φ50〜125 6
General
14 3.0 3.0
○ 12 1.2
TR4F ◎ ○
〜62HRC 汎用 φ32〜200 4
General 15 2.0
※上記以外にも荒加工用工具を多数ラインナップしております。
※工具仕様の詳細については総合カタログまたはホームページで確認をお願いします。
Various other tools for roughing are also available.
For more information on tool specifications, please refer to our general catalog or visit our website(. http://www.moldino.com)
切削動力に関して Notes about cutting power
切削動力Hpを求めるための計算式と比切 ap : 軸方向切込み(mm) Axial cutting depth
10,000
削抵抗Ksを次のグラフに示します。ご使用 ap×ae×v f×Ks ae : 径方向切込み(mm) Radial cutting depth
時の目安としてください。 9,000 Hp(kW)= v f : 送り速度(mm/min) Feed rate
尚、ご使用される加工機械の主軸回転域に 8,000 60×1,000×1,000×η(0.8) Ks: 比切削抵抗MPa(N/mm2) S pecific Cutting
Force
より本来の動力が出ない場合があります。 7,000 η : 機械の効率(0.8) Machine tools efficency
機械動力が不足する場合は、まずは切込み 6,000
深さを下げてください。次いで回転数およ 5,000 4,470
びテーブル送り量を下げてご使用ください。 プリハードン鋼・合金鋼( 45HRC)
4,000 4,130 Pre-hardened steels, Alloy steels
The formula for calculating cutting power Hp 3,440
3,780 3,120
and the specific cutting resistance Ks are 3,000 3,030 2,820 プリハードン鋼・合金鋼( 40HRC)
2,750 Pre-hardened steels, Alloy steels
shown in the following graph. 2,060 2,750 2,550
2,480
Use these values as guidelines. 2,000 1,790 2,340 S50C(220HB) Carbon steels
1,560 1,450
Depending on the range of spindle speeds of FC250 Cast Irons
1,000
the machine in use, full rated power may be
unavailable. If the machine lacks sufficient 0
0 0.5 1 1.5 2 2.5
power, first reduce the cutting depth, then
reduce the rotation speed and table feed rate. 1刃当りの送り量 fz Feed per tooth (mm/t)
19
比切削抵抗 Ks
Specific Cutting Force (N/mm2)
Page20
図、表等のデータは試験結果の一例であり、保証値ではありません。
「 」は株式会社MOLDINOの登録商標です。
The diagrams and table data are examples of test results, and are not guaranteed values.
“ ” is a registered trademark of MOLDINO Tool Engineering, Ltd.
安 全 上 の ご 注 意 Attentions on Safety
1. 取扱上のご注意 1. Attentions regarding handling
(1)工具をケース(梱包)から取り出す際は、足元への落下あるいは素手の指先へ落して怪我をしないよ (1) When removing the tool from the case (package), be careful not to drop it on your foot or
うに十分なご注意をお願いします。 drop it onto the tips of your bare fingers.
(2)インサートをセットして実際にご使用する場合は、切れ刃を素手で直接触れないように注意してください。 (2) When actually setting the inserts, be careful not to touch the cutting flute directly with
2. 取付け時のご注意 your bare hands.
(1)ご使用にあたって、インサートのセッティングは確実に行っていただき、アーバ等への取付けも確実に 2. Attentions regarding mounting
行ってください。 (1) When preparing for use, be sure that the inserts are firmly mounted in place and that they
(2)ご使用中に、異常な振動等が発生した場合は、直ちに機械を停止させて、その振動の原因を除いて are firmly mounted on the arbor, etc.
ください。 (2) If abnormal chattering occurs during use, stop the machine immediately and remove the
cause of the chattering.
3. 使用上のご注意
(1)切削工具あるいは被削材の寸法・回転の方向は、あらかじめ確認しておいてください。 3. Attentions during use
(1) Before use, confirm the dimensions and direction of rotation of the tool and milling work
(2)標準切削条件表の数値は、新しい作業の立上げの目安としてご利用ください。切込みが大きい場合、 material.
使用機械の剛性が小さい場合あるいは被加工物の性状に応じて切削条件を適正に調整してご使用 (2) The numerical values in the standard cutting conditions table should be used as criteria when
ください。 starting new work. The cutting conditions should be adjusted as appropriate when the cutting
(3)インサートは硬質の材料です。ご使用中に破損して飛散する場合があります。また、切りくずが飛散す depth is large, the rigidity of the machine being used is low, or according to the conditions of
ることがあります。これらの飛散物等は作業者を切傷させ、火傷あるいは目に入って負傷させる恐れが the work material.
ありますので、工具をご使用中はその周囲に安全カバーを取付け、保護めがね等の保護具を着用し (3) The inserts are made of a hard material. During use, they may break and fly off. In addition,
て安全な環境下での作業をお願いいたします。 cutting chips may also fly off. Since there is a danger of injury to workers, fire, or eye damage
・引火や爆発の危険のあるところでは使用しないでください。 from such flying pieces, a safety cover should be installed and safety equipment such as
・不水溶性切削油は、火災の恐れがありますので使用しないでください。 safety glasses should be worn to create a safe environment for work.
(4)工具を本来の目的以外に使用したり、改造したりしないでください。 ・Do not use where there is a risk of fire or explosion.
・Do not use non-water-soluble cutting oils. Such oils may result in fire.
4. 工具に関して、安全上の問題点・不明の点・その他ご相談がありましたら フリーダイヤル技術相談 へ (4) Do not use the tool for any purpose other than that for which it is intended, and do not modify it.
お問い合わせください。
ホームページ フリーダイヤル技術相談
https://www.moldino.com
MOLDINO Tool Engineering, Ltd.
本社 〒130-0026 東京都墨田区両国4-31-11(ヒューリック両国ビル8階) 工具選定データベース【 TOOLSEARCH】
03-6890-5101 FAX 03-6890-5134
International Sales Dept .: +81-3-6890-5103 FAX +81-3-6890-5128
営業企画部 ☎03-6890-5102 FAX03-6890-5134 海外営業部 ☎03-6890-5103 FAX03-6890-5128
東京営業所 ☎03-6890-5110 FAX03-6890-5133 静岡営業所 ☎054-273-0360 FAX054-273-0361
東北営業所 ☎022-208-5100 FAX022-208-5102 名古屋営業所 ☎052-687-9150 FAX052-687-9144
新潟営業所 ☎0258-87-1224 FAX0258-87-1158 大阪営業所 ☎06-7668-0190 FAX06-7668-0194
東関東営業所 ☎0294-88-9430 FAX0294-88-9432 中四営業所 ☎082-536-2001 FAX082-536-2003
長野営業所 ☎0276-59-6001 FAX0276-59-6005 九州営業所 ☎092-289-7010 FAX092-289-7012
北関東営業所 ☎0276-59-6001 FAX0276-59-6005
神奈川営業所 ☎046-400-9429 FAX046-400-9435
ヨーロッパ/MOLDINO Tool Engineering Europe GmbH Itterpark 12, 40724 Hilden, Germany. TEL : +49-(0)2103-24820, FAX : +49-(0)2103-248230
アメリカ/MITSUBISHI MATERIALS U.S.A. CORPORATION Detroit office c/o RFM Inc. Customer service 2001 Orndorf Drive, Brighton, MI 48116 U.S.A. TEL : +1(248)308-2620, FAX :+1(248)308-2627
メキシコ/MITSUBISHI MATERIALS MÉXICO S.A. DE C.V. Av. La Cañada No.16, Parque Industrial Bernardo Quintana, El Marques, Querétaro, CP 76246, México TEL : +52-442-1926800
ブラジル/MITSUBISHI MATERIALS BRASIL LTDA. Rua Cincinato Braga, 340 13° andar.Bela Vista – CEP 01333-010 São Paulo – SP ., Brasil TEL : +55(11)3506-5600 FAX : +55(11)3506-5677
タ イ/MITSUBISHI MATERIALS (THAILAND) CO., LTD. 139/3 Moo 2, Tambon Khlong Chik, Amphoe Bang Pa-in, Phra Nakhon Si Ayutthaya 13160, Thailand TEL:+66-3525-8024
イ ン ド/Mitsubishi Materials India Private Limited H.O.: Prasad Enclave, #118/119, 1st Floor, 2nd Stage, 5th main, BBMP Ward #11, (New #38), Industrial Suburb, Yeshwanthpura, Bengaluru, 560 022, Karnataka, India. Tel : +91-80-2204-3600
予告なく、改良・改善のために仕様変更することがあります。
Specifications for the products listed in this catalog are subject to change without notice due to ベジタブルインクで印刷しています。 2026-9(ME)
replacement or modification. Printed using vegetable oil ink. Printed in JAPAN 2020-4:FP